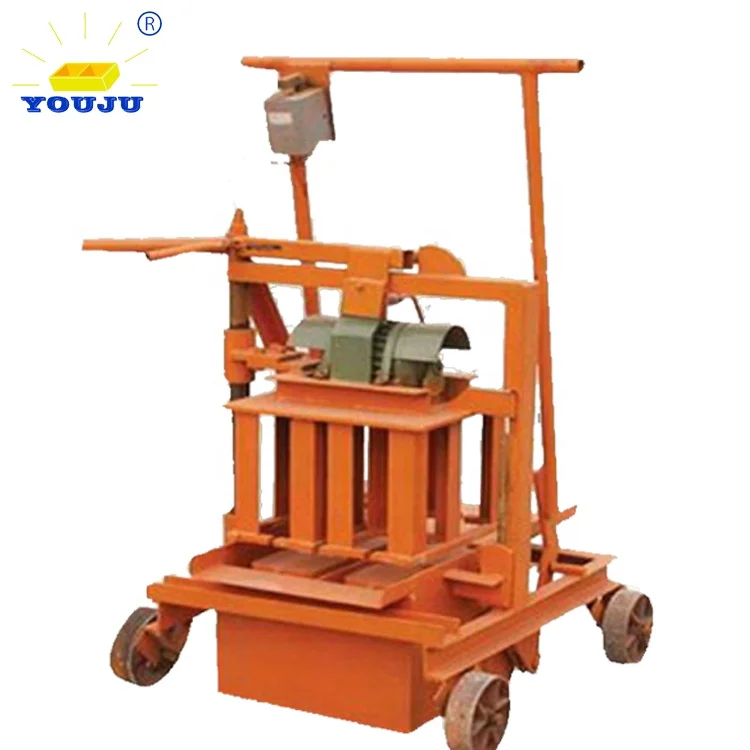
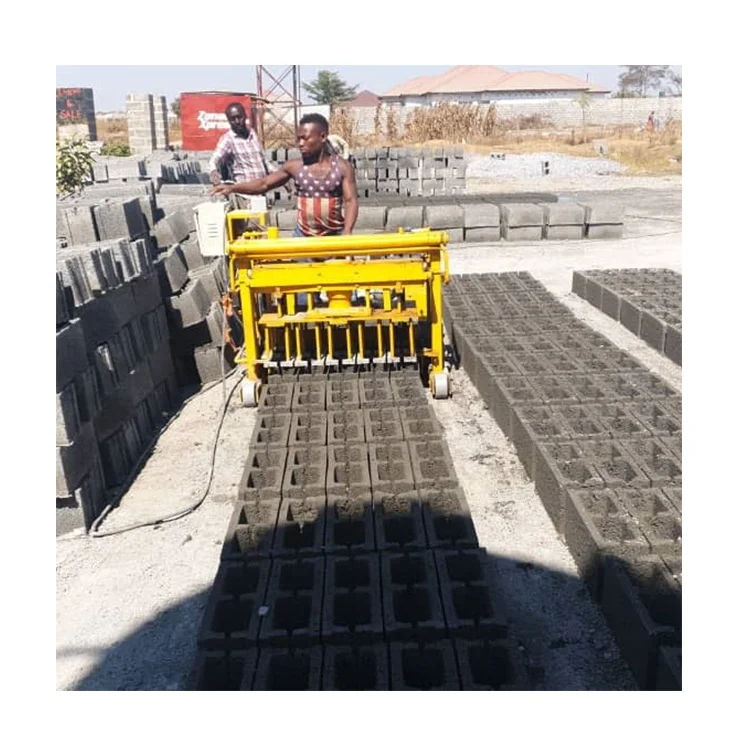
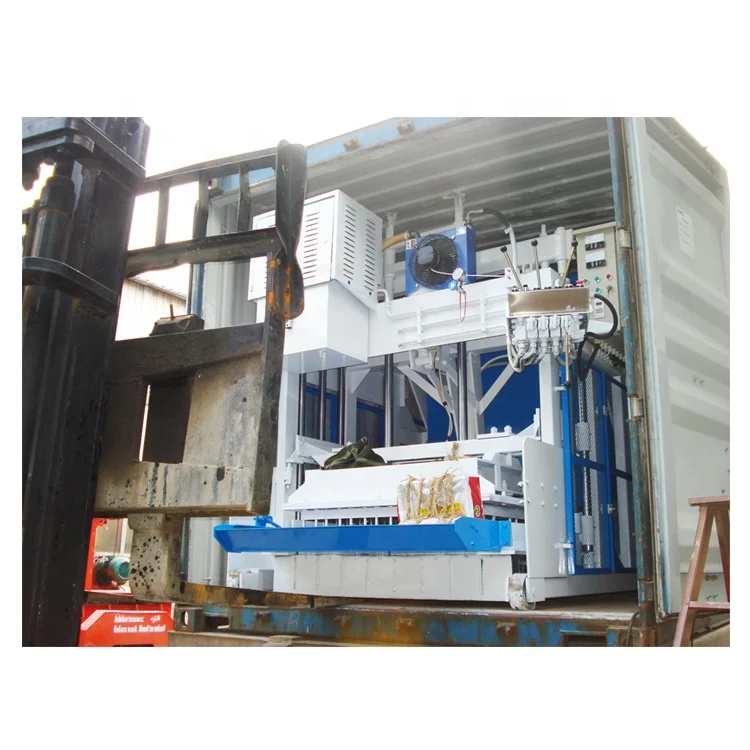
System-Sized Block Machinery — every QMJ2-45 mobile unit is configured against your actual hollow block format and local aggregate before dispatch, not shipped from a catalogue default.
Technical Specifications
| Parameter |
Value |
| Model |
QMJ2-45 |
| Product Type |
Mobile Concrete Block Making Machine |
| Machine Category |
Manual mobile egg-laying block machine |
| Mould Format & Output |
400×200×200mm hollow brick, 2 pcs/mould, 160 pcs/h, 1280 pcs/8hr (basis: 400×200×200mm hollow brick) |
| Mould Format & Output |
400×150×200mm hollow brick, 3 pcs/mould, 240 pcs/h, 4800 pcs/8hr (basis: 400×150×200mm hollow brick) |
| Mould Format & Output |
400×100×200mm hollow brick, 4 pcs/mould, 320 pcs/h, 2560 pcs/8hr (basis: 400×100×200mm hollow brick) |
| Molding Cycle |
25–30 s |
| Mould Change |
Supported, multiple hollow brick formats via mould swap |
| Pallet Requirement |
None (egg-laying / mobile type) |
| Power Source |
Electric motor (no diesel dependency) |
| Labor Requirement |
1 to 3 workers |
| Mobility |
Hand-pushed, free movement across site |
| Control System |
Manual operation |
| Hydraulic Pressure |
Not applicable (manual / motorized vibration type) |
| Automation Level |
Manual (hand-pushed mobile) |
| Stacking Method |
Not applicable (egg-laying, no pallet) |
| Mould Heat Treatment |
Carburization technology applied |
| Standards |
ISO 9001:2000, CE |
Application Suitability
| Application |
Material or Output |
| Small-scale hollow block production on construction sites |
Crushed stone, sand, cement blends without a fixed plant footprint |
| First-time block plant entrepreneurs |
Low-investment hollow brick startup using locally sourced aggregate |
| On-site block production for housing projects |
Multiple hollow brick formats produced directly where the build is happening |
| Building material distributors adding a mobile option |
Compact machine range complement to complement existing catalogue |
What "Pieces per Hour" Actually Means for a Mobile Block Making Machine for Sale
Quoted output means nothing unless the hollow brick format behind that number is named.
Buyers comparing a mobile block making machine for sale across suppliers often see a single headline capacity — and assume it applies to whatever block they plan to produce. With the QMJ2-45, the hourly figure shifts depending on which hollow brick format the mould is set for. A 400×200×200mm block yields a different throughput than a 400×100×200mm block, and the difference compounds across an eight-hour shift. I have seen contractors order a machine based on one number and then discover their actual product format delivers considerably less over a working day.
Positioning Within the Block Machine Range
Where the QMJ2-45 Sits Before You Commit to a Higher Tier
Before investing in a semi-automatic or fully automatic line, many first-time plant owners need to understand whether a manual mobile machine covers their near-term volume. The QMJ2-45 occupies the entry position in the block machine range, offering hollow brick production without a fixed plant, pallet inventory, or complex electrical infrastructure. For buyers surveying options, this mobile block making machine for sale represents the lowest capital threshold while still producing saleable hollow blocks across three standard formats.
Footprint and Site Flexibility Across the Range
A fixed plant requires a dedicated building, curing racks, and a pallet return system. The QMJ2-45 eliminates all of that by laying blocks directly on the ground and moving forward after each cycle. This egg-laying approach means the machine footprint is essentially the curing area itself, which expands or contracts with available land. For contractors who move between project sites, this mobility is something no stationary tier in the range can replicate [NEED_CITE: site preparation standards for mobile egg-laying block machines].
Reading the Specifications That Matter
Moulding Cycle, Format Switching, and Daily Reality
The 25–30 second moulding cycle applies across all three listed hollow brick formats, but the pieces-per-mould count is what actually determines shift output. Switching from a 400×200×200mm mould to a 400×100×200mm mould doubles the pieces per cycle without changing the cycle time. Carburization-treated mould surfaces resist abrasion from coarse aggregate, maintaining dimensional accuracy over extended production runs. Because the QMJ2-45 uses motorized vibration rather than hydraulic pressure, the forming force is constant regardless of format, which keeps block density predictable when operators stay within the recommended mix design.

The Hidden Cost of Ignoring Voltage and Frequency
Arriving machines that cannot run on local power sit idle while electricians source transformers or rewound motors.
Voltage and frequency mismatches are a recurring reason commissioning gets delayed after a mobile block making machine for sale arrives at its destination. A machine wired for a supply standard that does not match the local grid will either fail to start or burn out the motor within days [NEED_CITE: voltage and frequency standards by export market]. Confirming the exact supply specification at the inquiry stage — not after the proforma invoice — avoids weeks of idle equipment and unplanned electrical work on site.
Why Source the QMJ2-45 Through This Range
Block machinery is the single focus here, so the QMJ2-45 is specified as part of a matched system rather than assembled from unrelated suppliers. Each machine is configured against the buyer’s stated hollow brick format, local aggregate, and target daily output, not pulled from a default catalogue line. Mould design covers the formats the buyer’s market actually sells, and custom drawings are available when standard formats do not match local demand. The automation level is selectable within the broader range, so a buyer starting with a QMJ2-45 today can transition to a semi-automatic or automatic line later without changing suppliers. Factory testing runs the buyer’s actual mix design before dispatch, confirming that vibration parameters suit the material rather than assuming a generic blend will work.
Documentation & Verification
- Line layout and capacity calculation stating the hollow brick format assumed for each output tier
- Machine specification sheet with mould format list and cycle time per format
- Voltage and control language confirmation document signed before production begins
- Factory test record using the buyer’s aggregate blend before the machine leaves the workshop
- CE declaration of conformity supplied with shipping documentation
Installation, Commissioning & Support
- Flat concrete ground or compacted earth required; no fixed foundation needed for the hand-pushed QMJ2-45
- Electric motor supply must match confirmed voltage and frequency before the machine is energized on site
- Machine ships assembled; operator positions it on the curing area and begins production after a brief alignment check
- First-run moulding cycle observed with the buyer’s mix to verify block density and dimensions against the specification sheet
- Mould change demonstration included, covering removal, swap, and re-seating for each hollow brick format supplied
- Carburization-treated mould surfaces require periodic visual inspection; wear parts list provided at dispatch
Starting the Conversation
To size the right configuration within the range, share the hollow brick formats your market demands, the aggregate and cement available locally, and your target daily output. Include the voltage and frequency standard at your site and the language needed for any operational markings. If you already have curing space or plan to produce on open ground, note the dimensions so the egg-laying workflow can be planned around it.
Frequently Asked Questions
Q: How is the quoted hourly output verified, and which hollow brick format does each figure assume?
A: Every output figure for the QMJ2-45 is stated alongside the specific hollow brick format it applies to. The 160 pcs/h rate assumes a 400×200×200mm block at two pieces per mould, while the 320 pcs/h rate assumes a 400×100×200mm block at four pieces per mould, all based on a 25–30 second moulding cycle.
Q: What voltage and frequency options are available for my target market?
A: The electric motor on the QMJ2-45 is configured to the buyer’s confirmed voltage and frequency before production. Provide your local grid specification during the inquiry so the motor winding matches your supply, avoiding the need for on-site transformers or motor replacement after arrival.
Q: Where does the QMJ2-45 mobile machine sit compared to semi-automatic and automatic tiers in the range?
A: The QMJ2-45 is the entry-level manual mobile tier, producing hollow blocks without pallets or a fixed plant. Semi-automatic tiers add pallet-based forming and conveyor feeding, while automatic tiers include stacking and cubing. The range lets buyers start here and move up without switching suppliers.
Q: What site conditions and space are needed to operate a hand-pushed egg-laying machine?
A: The QMJ2-45 requires flat, compacted ground or a concrete slab large enough to serve as the curing area. No fixed foundation or building is needed. The machine is hand-pushed forward after each cycle, so the curing area grows with production volume and available land [NEED_CITE: ground preparation requirements for egg-laying block production].
Q: How long does a mould change take, and what formats can I add later?
A: Mould swap on the QMJ2-45 involves unbolting the current mould, lifting it out, and seating the replacement — a task operators typically complete within a single shift break. Additional hollow brick format moulds can be ordered separately, with carburization treatment applied to all mould surfaces for wear resistance.

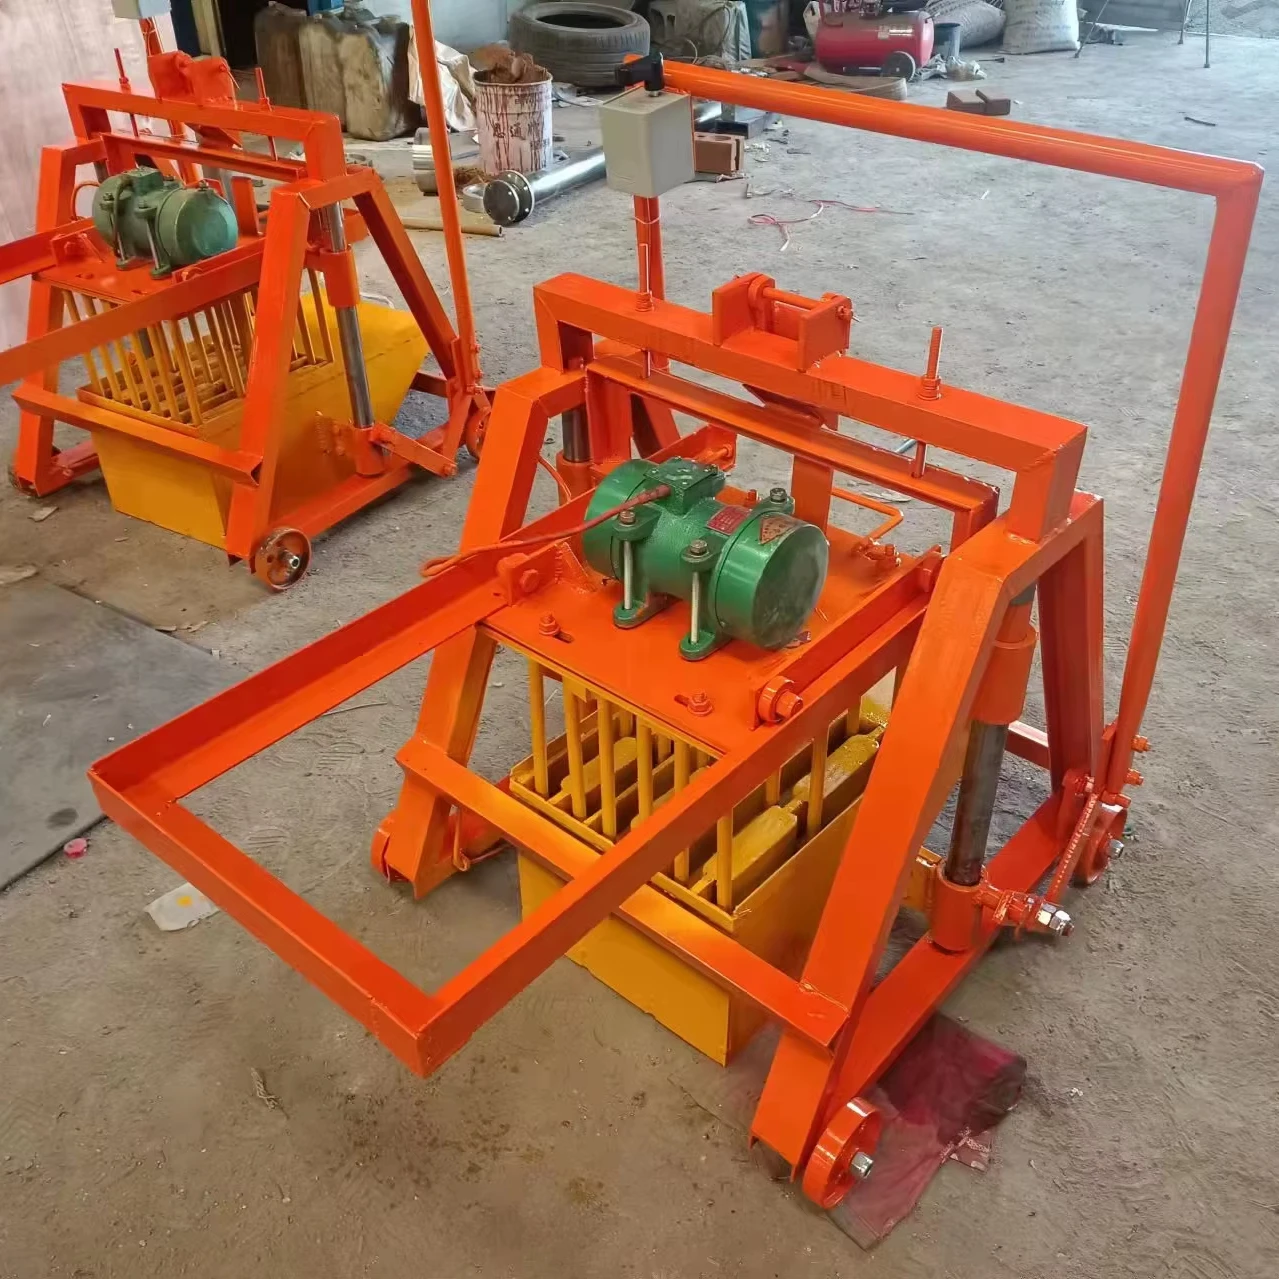
 Mobile block machine