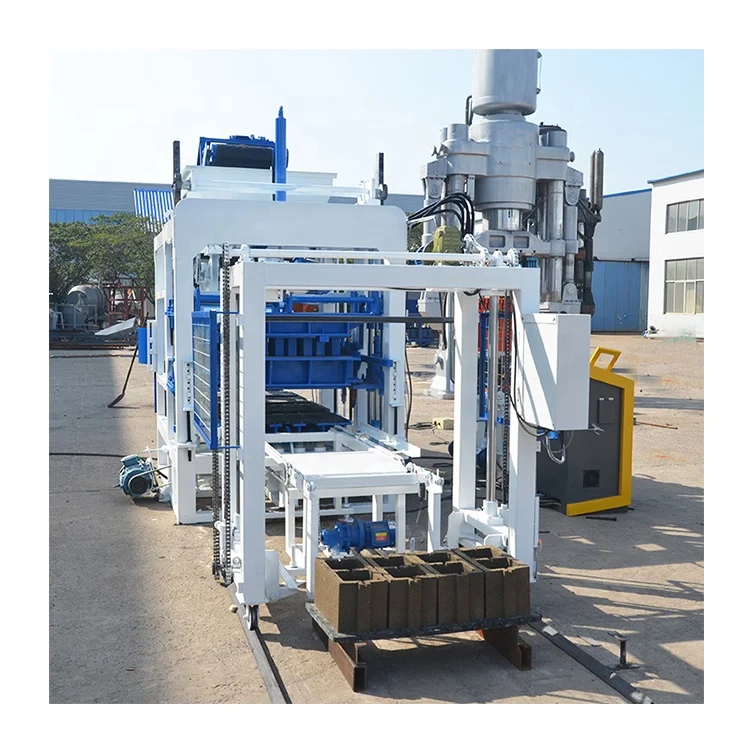
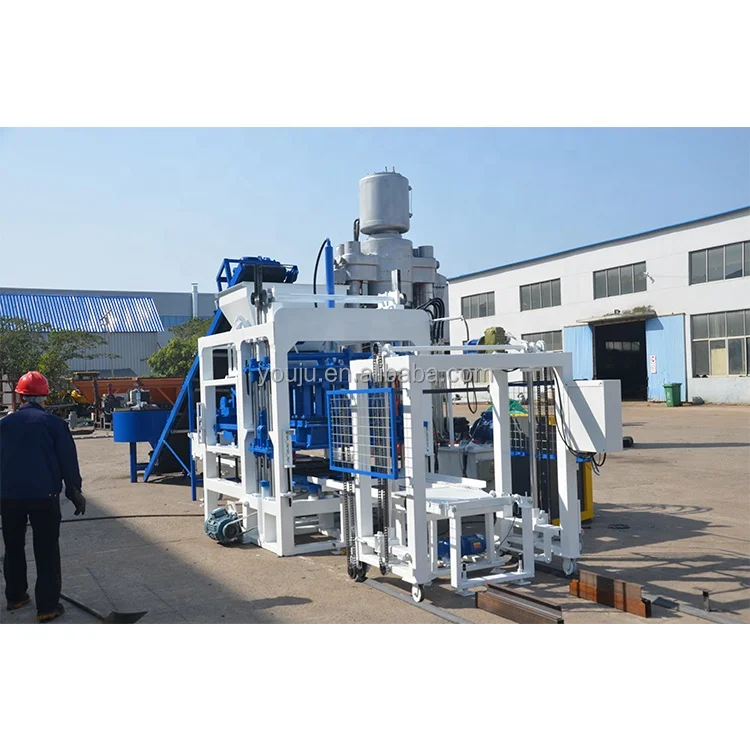
Configuration matched to your actual mix design — The QT12-15 is positioned at the high-capacity tier of our automatic block machine range, requiring buyers to evaluate plant footprint, pallet logistics, and supporting equipment before narrowing down from smaller semi-automatic alternatives.
Technical Specifications
| Parameter |
Value |
| Model |
QT12-15 |
| Product Type |
Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
9350 × 2520 × 2950 mm |
| Rated Pressure |
21 MPa |
| Main Vibration Form |
Platform Vibration |
| Vibration Frequency |
2800–4500 r/min |
| Vibration Acceleration |
15–20 g |
| Exciting Force |
120 kN |
| Block Height Range |
50–200 mm |
| Pallet Size |
1350 × 850 mm |
| Molding Cycle |
15–25 s |
| Storage Hopper Volume |
0.4 m³ |
| Feeding Device Volume |
0.31 m³ |
| Total Power |
50.7 kW |
| Total Weight |
12000 kg |
| Control System |
PLC controlled (basis not stated in source — confirm brand and language) |
| Voltage & Frequency |
Configurable (basis not stated in source — confirm with supplier) |
| Frame Structure |
Gantry frame type, super steel |
| Mould Type |
Cartridge type welding mould, manganese steel (carburizing and quenching) |
| Output — Hollow Block 390×190×190 mm |
12 pcs/mould, 1720–2160 pcs/h, 13700–17200 pcs/day (8h) |
| Output — Porous Block 240×115×90 mm |
35 pcs/mould, 5040–6300 pcs/h, 40300–50400 pcs/day (8h) |
| Output — Standard Block 240×115×53 mm |
62 pcs/mould, 13100–14800 pcs/h, 105000–119000 pcs/day (8h) |
| Compressive Strength of Blocks |
>15 MPa |
| Recommended Batching Line |
PL1200 batching machine, JS500 or JS750 mixer, 8 m conveyor belt, stacker |
Application Suitability
| Application |
Material or Output |
| Hollow block production for masonry walls |
Crushed stone, cement, sand and fly ash blends forming 390×190×190 mm units |
| Porous block manufacturing for partition walls |
Lightweight aggregate mixes shaped into 240×115×90 mm cellular formats |
| Standard solid block for load-bearing structures |
Dense aggregate and cement producing 240×115×53 mm units above 15 MPa |
| Interlocking brick and paving block runs |
Pigmented concrete mixes compressed in cartridge moulds for surface applications |
| Fly ash block production for cost-sensitive markets |
Industrial fly ash blended with binder and local aggregate in varying ratios |
What "1720 Pieces per Hour" Leaves Out When Sizing a Block Plant
Capacity figures are meaningless unless tied to a named block format and mould.
Every concrete block making machine manufacturer quotes cycles per hour, yet that number shifts dramatically depending on whether you are pressing a single 390 mm hollow block or sixty-two standard bricks per mould. I once supplied a high-output line to a Middle East contractor who signed off on catalogue capacity, only to discover that their local high-clay sand doubled the molding cycle and halved daily throughput. The machine was never at fault — the specification conversation stopped too early [NEED_CITE: effect of aggregate clay content on block cycle time and compressive strength].
Mapping the Full Range Before Committing to a Tier
Choosing a concrete block making machine manufacturer is less about picking the largest press and more about matching your current output target, site conditions, and capital envelope to the correct tier. The QT12-15 sits at the upper end of the automatic range, demanding a dedicated production hall, a curing yard sized for 1350 × 850 mm pallets, and a forklift fleet that can handle continuous pallet circulation. Buyers who have not yet secured these infrastructure elements often find a mid-tier semi-automatic model a more practical starting point.
Footprint and Infrastructure That This Tier Demands
A gantry-frame press of this class occupies a production bay that must accommodate the PL1200 batching machine, JS500 or JS750 mixer, and the 8 m conveyor feeding the storage hopper [NEED_CITE: typical plant layout requirements for high-output block production lines]. The 12000 kg machine weight requires a reinforced concrete foundation rather than a simple workshop slab. Curing racks must be planned around the pallet dimensions, because any mismatch between pallet size and existing racking or forklift capacity creates a bottleneck that no amount of press speed can resolve.
How Vibration Force and Hydraulic Pressure Shape Block Density
The 120 kN exciting force combined with 21 MPa rated pressure determines whether your blocks reach the stated compressive strength above 15 MPa. Vibration frequency between 2800 and 4500 r/min is adjustable, but the optimal setting depends entirely on your aggregate grading and cement ratio. Platform vibration transmits energy uniformly across the 1350 × 850 mm pallet area, which matters when you switch between a 12-cavity hollow block mould and a 62-cavity standard brick mould — each format demands a different frequency profile to avoid under-compaction at the edges or over-compaction in the centre.

The Cost of Overlooking Pallet and Voltage Details
I have watched entire commissioning schedules stall because the buyer’s curing area was designed for a different pallet size, forcing a forklift change and rack rebuild mid-project. Similarly, when voltage and frequency are left unconfirmed, the PLC cabinet arrives incompatible with the local grid and the electrician spends days rewiring before the first test cycle can run [NEED_CITE: voltage and frequency standards by export market]. These oversights do not reflect machine quality — they reflect gaps in the pre-order specification conversation that a thorough concrete block making machine manufacturer should close before production begins.
Why Source This Tier from Shandong Shiyue Intelligent Machinery
Our single focus on block machinery means the QT12-15 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate vendors. Configuration is set against your actual mix design and local aggregate report, not a catalogue default. Mould design covers every format your market sells, with custom drawings available when standard options do not fit. Automation level is selectable so you can begin semi-automatic and add stacking or cubing modules as volume grows. Factory testing runs your specific block format before dispatch, and the test record ships with the machine.
Documentation & Verification
- Line layout drawing stating output capacity for each block format included in your order
- Machine specification sheet with vibration force and hydraulic pressure matched to your target mix
- Mould drawing and format list covering every block type your market requires
- Pallet specification aligned with your existing curing racks and forklift capacity
- Voltage, frequency and PLC display language confirmation document signed before production
- Factory test record on your chosen block format and aggregate blend before dispatch
Installation, Commissioning & Support
- Foundation drawing for the 9350 × 2520 mm footprint and 12000 kg static load on reinforced concrete
- Dedicated electrical circuit specification for the 50.7 kW total power draw at your confirmed voltage
- Gantry frame dismantling and container loading plan with reassembly sequence at your site
- First-run parameter setting covering vibration frequency, hydraulic pressure and cycle time for your mix
- Operator training on mould change procedure using the cartridge-type welding mould system
- Wear parts and mould replenishment list covering manganese steel mould surfaces and hydraulic seals
What to Include in Your Inquiry
To receive a configuration that reflects your actual conditions rather than a catalogue default, share your target block formats with dimensions, your daily output requirement, the aggregate and cement types available locally, and any existing pallet or curing infrastructure. Confirming your site voltage, frequency, and preferred PLC display language at this stage avoids commissioning delays after the machine arrives. If you are evaluating this tier against a smaller model, let us know your current or planned production volume so we can map the range accordingly.
Frequently Asked Questions
Q: Where does the QT12-15 sit in the range compared to semi-automatic and mobile models?
A: The QT12-15 occupies the high-capacity automatic tier, requiring a dedicated production hall, reinforced foundation, and pallet-scaled curing area. Semi-automatic and mobile models serve smaller daily volumes with lower infrastructure demands. The right tier depends on your confirmed daily output target and site readiness, not simply on maximum catalogue figures.
Q: What plant footprint and curing area does this tier require?
A: The press alone measures 9350 × 2520 mm and weighs 12000 kg, needing a reinforced bay plus room for the PL1200 batcher, JS500 or JS750 mixer, and 8 m conveyor. Curing racks must accommodate 1350 × 850 mm pallets. Plan the curing yard around pallet circulation volume at your target daily output to avoid bottlenecks downstream of the press.
Q: How do I verify the quoted output figures against my own block format and mix design?
A: Request a capacity calculation that names each block format and its corresponding cycle time. Share your aggregate sieve analysis and cement ratio so the manufacturer can run a factory test on your actual mix before dispatch. The resulting test record confirms whether molding cycle and compressive strength meet your specification.
Q: Can I start with a lower tier and upgrade to this capacity later?
A: Automation modules such as automatic pallet feeding, stacking, and cubing can be added to a semi-automatic press as volume grows. However, upgrading the press itself to the QT12-15 tier means a larger gantry frame, heavier foundation, and different pallet size. Plan the initial purchase with your growth trajectory in mind to avoid duplicating infrastructure investments.
Q: What supporting equipment scale matches this press tier?
A: The recommended pairing includes a PL1200 batching machine, a JS500 or JS750 mixer, an 8 m conveyor belt, and a stacker sized for 1350 × 850 mm pallets. Undersizing any station forces the press to idle between cycles, reducing actual throughput below the stated per-format capacity. Specify the full line together to ensure cycle times align across every station.

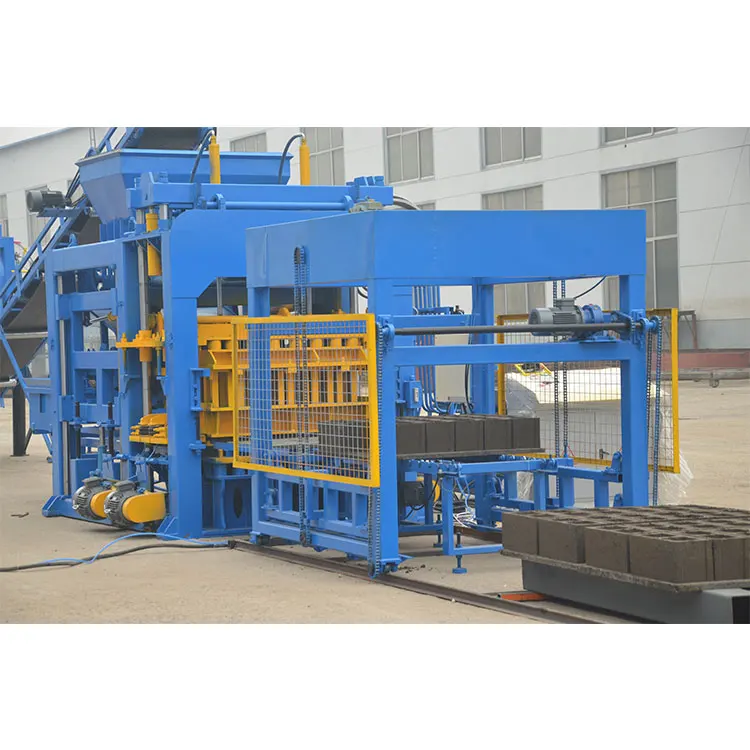
 Semi automatic block