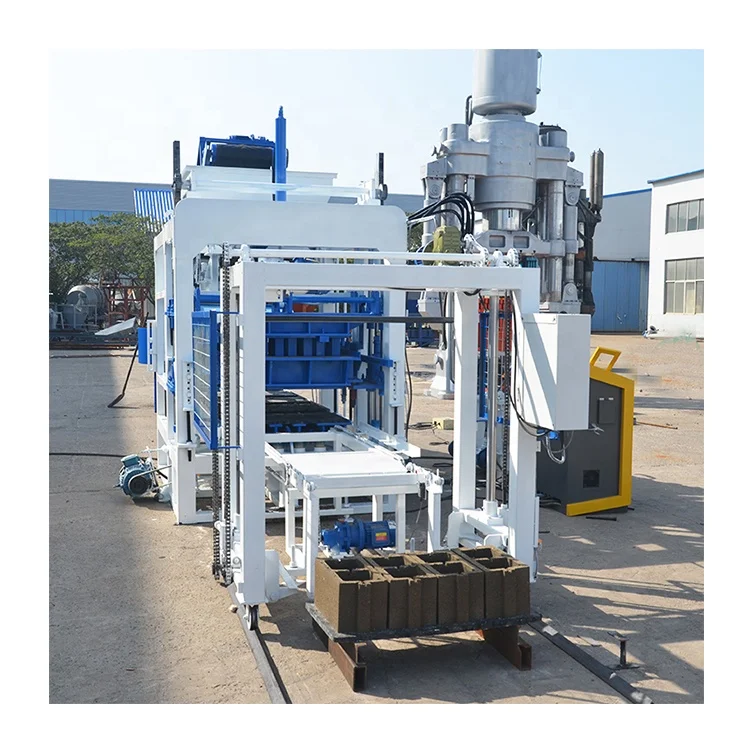
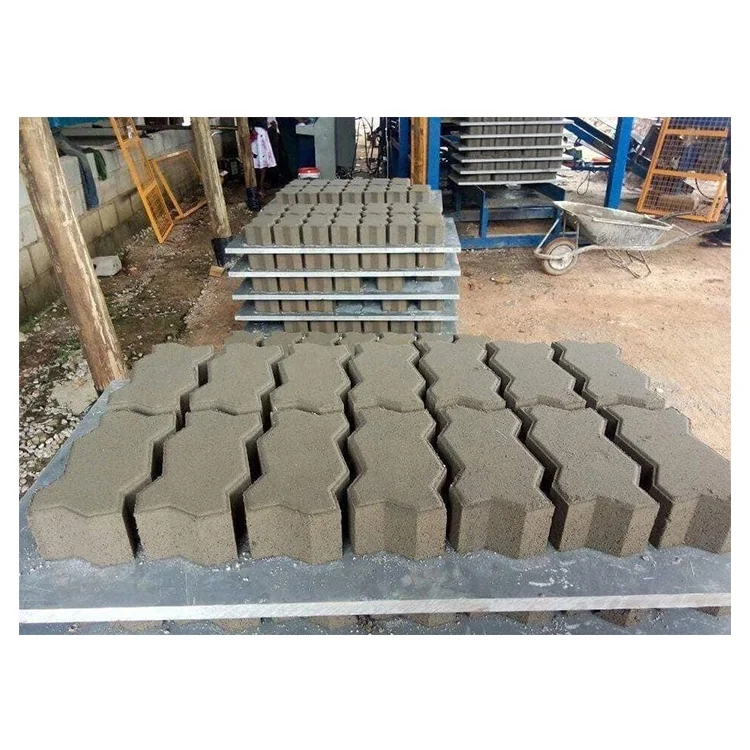
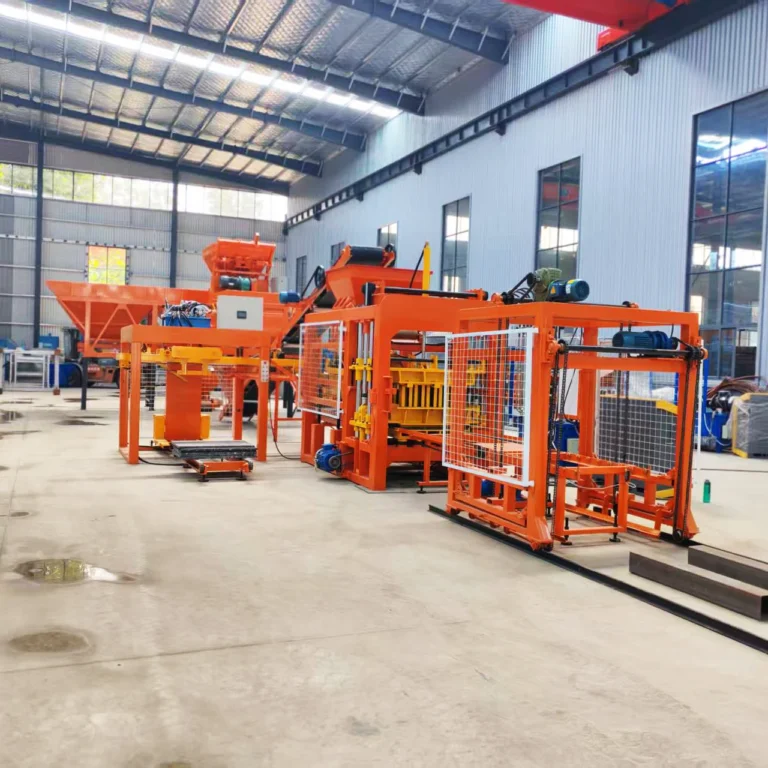
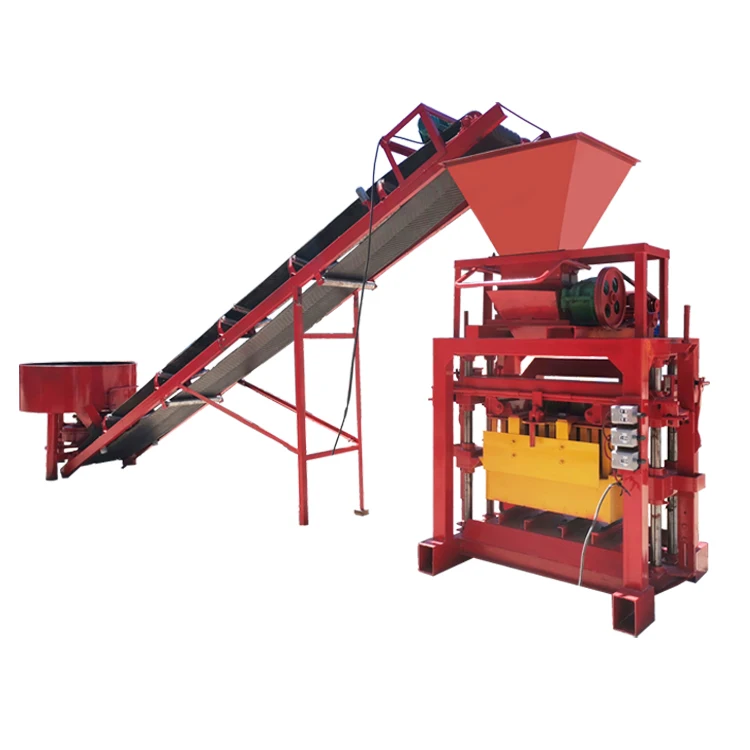
Matched System Configuration — the QT6-15 is specified as one integrated press, mould, pallet and handling package rather than assembled from separate component suppliers.
Technical Specifications
| Parameter |
Value |
| Model |
QT6-15 |
| Product Type |
Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) |
8200 × 1700 × 2950 mm |
| Total Mass |
7 T |
| Vibration Frequency |
0–60 Hz |
| Vibration Force |
45 KN |
| Vibration Form |
Platform Vibration |
| Moulding Mode |
Automatic loading, vibration moulding |
| Demolding Method |
Hydraulic |
| Hydraulic System |
Independent integrated hydraulic station |
| Pallet Size |
880 × 850 mm |
| Molding Cycle |
15–20 s (hollow/solid blocks); 20–25 s (pavers) |
| Overall Power |
37 kW |
| Control System |
PLC with touch screen, built-in fault diagnosis |
| Action Interlock |
Safe logic circuit |
| Block Compressive Strength |
More than 15 MPa |
| Factory Area |
1200 m² |
| Standards |
CE (where applicable) |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Crushed stone, sand, cement, fly ash aggregates |
| Solid brick production |
Concrete mix with local fine aggregate |
| Paving brick production |
High-density concrete for rectangular and zigzag formats |
| Porous and interlocking brick |
Adjusted mix designs with permeable aggregate |
| Waste ash and slag utilization |
Reduced cement dosage with industrial by-products |
Why "Pieces per Hour" Means Nothing Without the Block Format
Every output figure must name the exact block size, mould cavity count, and cycle time it assumes.
I learned this the hard way after a customer in West Africa signed for a block machine based on a single headline capacity number. When the local aggregate — high in clay content — could not compact properly under vibration, his daily output dropped significantly. The machine was not at fault; the quotation simply never stated which block format the capacity assumed, and no one had asked for a raw material sample before the order went into production. The QT6-15 block machine manufacturer approach is to state each output figure against a named format so there are no surprises on your shop floor [NEED_CITE: block format assumptions in capacity quotation standards].

Where the QT6-15 Sits in the Automatic Range
The QT6-15 occupies the mid-to-high output tier within the full machine range. It bridges the gap between semi-automatic presses that require manual pallet handling and the largest fully automatic lines with robotic cubing. For a buyer surveying options, this model represents the point where PLC-controlled consistency and hydraulic demolding become standard while the investment and plant footprint remain manageable for a growing operation.
Choosing Between Semi-Automatic and Fully Automatic
A semi-automatic press demands more operator involvement at the pallet feeding and stacking stations. The QT6-15 block machine manufacturer configuration offers a selectable automation level, meaning the press itself can be ordered with intelligent electronic control and later paired with automatic stacking and cubing modules as volume grows. This upgrade path matters because it lets a first-time plant owner enter at a lower capital point without painting themselves into a corner [NEED_CITE: automation upgrade paths in concrete block production].
What the Vibration and Hydraulic Numbers Actually Mean
The 45 KN vibration force combined with a 0–60 Hz frequency range is not a standalone figure — it works together with the independent integrated hydraulic station to determine how densely the concrete mix compacts before demolding. Platform vibration transmits energy through the mould table rather than the mould walls, which suits the 880 × 850 mm pallet size and the multi-cavity mould formats listed above. A molding cycle of 15–20 seconds for hollow and solid blocks, extending to 20–25 seconds for denser paving bricks, reflects the time needed for the vibration force and hydraulic pressure to reach target compressive strength of more than 15 MPa. The 37 kW overall power rating covers the hydraulic pump, vibration motors, and PLC control system running simultaneously.
When Capacity Quotations Omit the Fine Print
A quotation that lists a single output number without naming the block format, mould cavity count, and cycle time assumption sets up a mismatch between what the buyer expects and what the press delivers on day one. Pavers require longer cycle times than hollow blocks, so a capacity figure based on hollow blocks will never translate to a paving brick run. When the mould change itself consumes most of a shift, the format flexibility the buyer paid for is effectively cancelled out [NEED_CITE: impact of mould change duration on multi-format block plants].
Why Sourcing from This Range Makes Sense
Block machinery is the single focus here, which means the press, mould, pallet, and handling equipment are specified as one matched system. Configuration is set against the buyer’s actual mix design and local aggregate rather than a catalogue default. Mould design covers the formats the buyer’s market actually sells, including custom drawings. The automation level is selectable, so a buyer can start semi-automatic and add modules later. Installation, commissioning, and operator training are included in the scope rather than offered as optional extras.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with voltage, frequency, and PLC display language confirmed before production
- Mould drawing and format list showing every block size included in the quotation
- Hydraulic and electrical schematic for local maintenance reference
- Factory test record demonstrating cycle time under actual operating conditions
- Operation and maintenance manual with wear parts and mould replacement list
Installation, Commissioning & Support
- Foundation must accommodate the 8200 × 1700 mm footprint and 7 T operating mass with vibration isolation
- Dedicated 37 kW power circuit matching confirmed voltage and frequency before the press leaves the factory
- Hydraulic station arrives pre-filled and isolated from main frame vibration for immediate connection
- PLC touch screen configured to operator language prior to commissioning to eliminate translation delays
- First production run supervised on-site with cycle time verification across each mould format
- Wear parts list provided with recommended reorder intervals for hydraulic seals and vibration components
What to Prepare Before Your Inquiry
Share the block formats your market sells, the daily volume you need to hit, and the raw materials available locally — including aggregate type and any industrial by-products like fly ash or slag. Confirm your site voltage, frequency, and preferred PLC display language. If you have an existing curing area or forklift, note the pallet dimensions already in use so the 880 × 850 mm pallet specification can be evaluated against your layout.
Frequently Asked Questions
Q: How is QT6-15 capacity calculated and what block format does each figure assume?
A: Every output number ties to a specific block size, mould cavity count, and cycle time. For example, hollow blocks at 400 × 200 × 200 mm run six per mould at a 15–20 second cycle, while rectangular pavers at 200 × 100 × 60 mm run twenty-one per mould at a 20–25 second cycle. We state each figure with its full assumption so you can compare against your actual product mix.
Q: What voltage and PLC language options are available for my market?
A: Voltage and frequency are confirmed during the proposal stage to match your local grid. The PLC touch screen display language is set before the machine ships so operators can read fault codes and cycle parameters in their working language from the first production day, avoiding commissioning delays caused by untranslated interfaces.
Q: How does the automation level compare to semi-automatic models in the range?
A: The QT6-15 features PLC-controlled production with intelligent electronic control and a built-in fault diagnosis system, which places it above manual and relay-controlled semi-automatic presses. However, the automation level is selectable — buyers can begin with basic automatic operation and later integrate automatic pallet feeding, stacking, and cubing as production volume increases.
Q: What is the factory area requirement and how does pallet size affect curing layout?
A: The press itself requires space within a 1200 m² factory area, which must also accommodate raw material storage, curing racks, and forklift circulation. The 880 × 850 mm pallet size determines how many pallets fit on each curing rack tier and how your existing forklift handles loaded pallets, so confirming rack dimensions and forklift capacity early prevents layout conflicts.
Q: Can I start with this model and upgrade automation features later?
A: Yes. The QT6-15 block machine manufacturer design supports a modular upgrade path. The press, PLC, and hydraulic station remain in place while additional modules such as automatic stacking and cubing are added to the line. This lets you match capital spending to actual order volume rather than investing in full automation before demand justifies it.

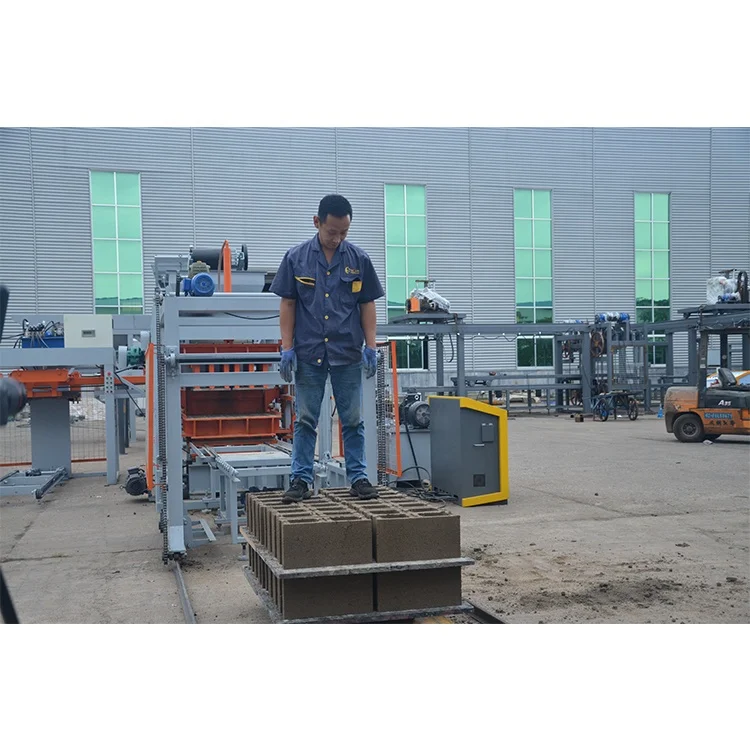
 High quality block machine