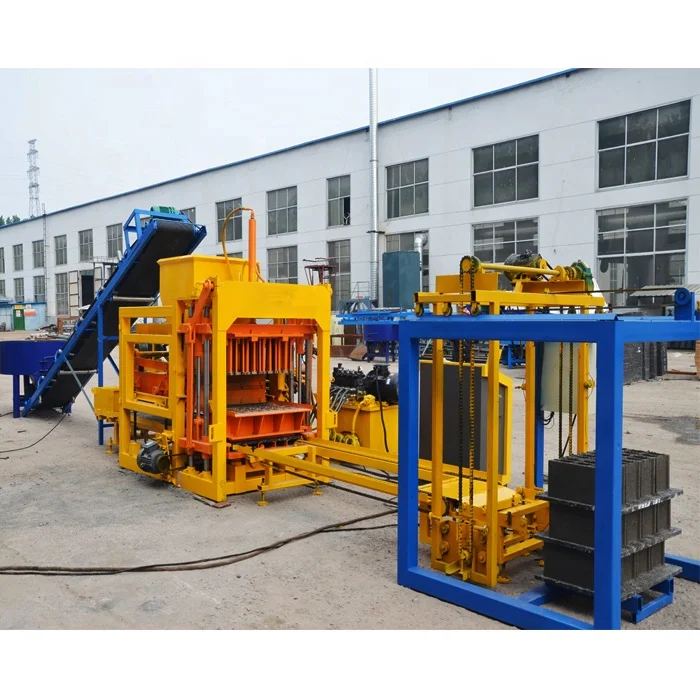
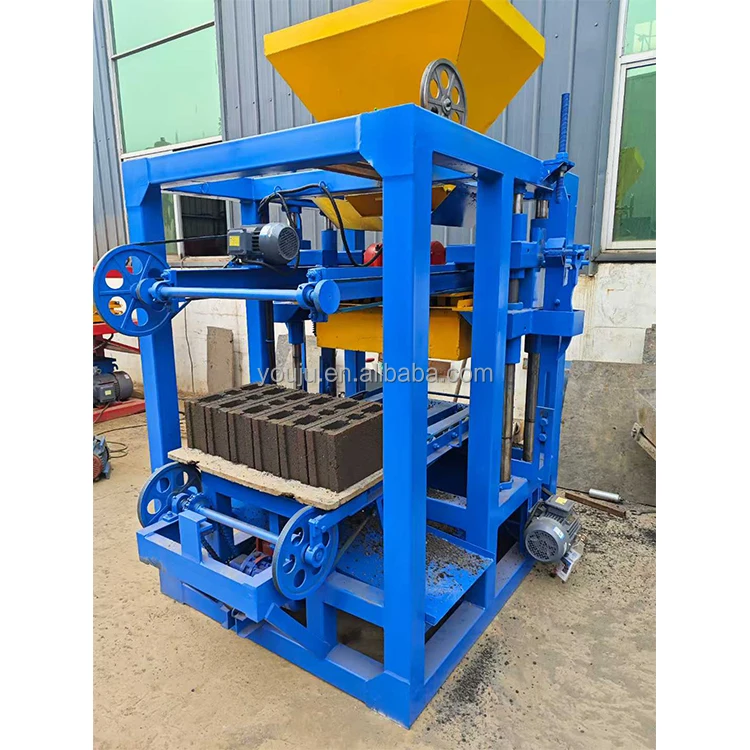
Matched System Specification — The QTJ4-25 semi-automatic block machine is configured as a complete press, mould, pallet and mixer set rather than a standalone unit, helping buyers see the full line requirement before committing.
Technical Specifications
| Parameter |
Value |
| Model |
QTJ4-25 |
| Product Type |
Semi-Automatic Concrete Block Making Machine |
| Rated Power |
17.9 kW |
| Overall Dimensions (L×W×H) |
6400 × 1500 × 2700 mm |
| Total Mass |
2500 kg |
| Molding Cycle |
25 s |
| Pallet Size |
850 × 550 × 20 mm |
| Vibration Frequency |
2800 r/min |
| Exciting Force |
60 kN |
| Output Capacity |
960 pcs/h, 7680 pcs/day (based on 400×200×200mm hollow block, 4 pcs/mould) |
| Mould Format |
Hollow, solid, paver (400×200×200mm hollow cited; other sizes available on request) |
| Automation Level |
Semi-automatic |
| Configuration Included |
Host machine 1 set, block mould 1 set, JQ350 mixer |
| Hydraulic Station |
Equipped |
| Stacking Method |
Manual (bricks placed on pallet, moved by trolley) |
| Voltage & Frequency |
To be confirmed before production |
| Control System |
To be confirmed (PLC or relay logic) |
Application Suitability
| Application |
Material or Output |
| Hollow block production for residential and commercial walls |
Crushed stone, sand, cement, water (8-inch, 6-inch formats) |
| Solid block manufacturing for load-bearing structures |
Dense aggregate mix designs requiring high compaction |
| Paving block and interlocking brick for driveways and walkways |
Fine aggregate and pigment mixes for surface finish |
| On-site contractor production for housing projects |
Local aggregate sourcing with portable semi-automatic setup |
| First-time block plant operations |
Small to medium daily output with manual pallet handling |
What "960 Pieces per Hour" Actually Means for Your Shift Plan
The quoted capacity assumes a specific block format, and switching moulds changes daily output significantly.
Many buyers receive a single hourly figure without understanding which block size it references, leading to production shortfalls when they switch to smaller solid blocks or pavers that require different cycle times. The QTJ4-25 semi-automatic block machine manufacturer specifications state 960 pieces per hour based on 400×200×200mm hollow blocks with four cavities per mould, but a 400×100×200mm solid block or a 200×100×60mm paver will yield different counts per cycle and may alter the molding rhythm. Without a capacity calculation document that breaks down output by format, buyers cannot plan curing space, pallet inventory, or shift labor accurately [NEED_CITE: block format impact on cycle time and daily throughput].

Where the QTJ4-25 Sits in the Semi-Automatic Range
The QTJ4-25 occupies the entry-to-mid tier of semi-automatic stationary block machines, positioned above mobile egg-laying models that produce directly on the ground without pallets, and below fully automatic lines with hydraulic stackers and cubing systems. Buyers evaluating their first block plant often start here because the investment covers the host machine, one mould set, and a JQ350 mixer without requiring automatic pallet feeders or stacking robots. The semi-automatic block machine manufacturer approach means the press, mould, pallet size, and mixer are specified together, so the buyer knows the complete line footprint before ordering.
Pallet Handling and Curing Area Alignment
At the semi-automatic tier, operators place finished blocks on pallets manually and move them via trolley to the curing area, which means pallet quantity and curing rack capacity must match the daily output expectation. The 850×550×20mm pallet size stated for the QTJ4-25 determines how many blocks fit per layer and how the pallets stack in the curing zone. If the buyer’s existing forklift or curing racks were sized for a different pallet dimension, mismatches cause bottlenecks that no press speed can overcome [NEED_CITE: pallet size and curing area planning for semi-automatic block lines]. Buyers should confirm pallet material (wood, bamboo, or composite) and total pallet count needed for continuous production before the machine ships.
Vibration Force, Hydraulic Pressure, and Block Density
The QTJ4-25 delivers 60 kN exciting force at 2800 r/min vibration frequency, combined with hydraulic station pressure to compact the concrete mix within the mould cavity. Block strength depends on how well the vibration force and hydraulic pressure match the buyer’s specific mix design and local aggregate gradation — a mix with higher fines content may require different vibration amplitude or duration than a coarse aggregate blend. The bed mould vertical vibration paired with upper mould compression vibration aims for uniform density throughout the block height, reducing weak layers that cause breakage during handling or curing. Mould change time is not stated in the source specifications, so buyers planning multiple block formats per shift should request this figure to assess format flexibility realistically.
The Hidden Cost of Unconfirmed Voltage and Control Language
When voltage, frequency, and PLC display language are not confirmed before production, the machine may arrive with incompatible electrical components or an interface the operator cannot read, delaying commissioning and requiring on-site rewiring or control panel replacement. The QTJ4-25 specifications list voltage and control system as "to be confirmed," which means the buyer must provide local power standards (such as 380V/50Hz, 440V/60Hz, or other regional variants) and preferred control language before the factory begins assembly. Skipping this step leads to multi-week delays while replacement transformers or PLC modules are sourced and shipped [NEED_CITE: voltage and frequency standards by export market].
Why Procurement Here Differs from Catalogue Ordering
Block machinery as a single focus means the QTJ4-25 is not assembled from separate suppliers’ components but specified as a matched system where the mould, pallet, mixer, and press are selected together based on the buyer’s target block format and local raw materials. Configuration is set against the buyer’s actual mix design and aggregate availability, not a default catalogue setting that may require costly material substitutions. Mould design covers the formats the buyer’s market actually sells, including custom drawings for non-standard sizes. The automation level is selectable, so a buyer can start semi-automatic with manual pallet handling and plan an upgrade path to automatic stacking later. Installation support includes operator training on the specific machine configuration delivered, not generic block production theory.
Documentation & Verification
- Line layout showing QTJ4-25 placement with mixer, pallet staging, and curing area flow
- Capacity calculation document stating output per block format, not a single hourly figure
- Mould drawing and format list confirming block dimensions match local market demand
- Voltage, frequency, and control language confirmation sheet signed before production
- Factory test record with photographs showing machine running with buyer’s specified mould
- Packing photographs documenting machine condition and component count before container loading
Installation, Commissioning & Support
- Foundation must support 2500 kg total mass with level tolerance for 6400×1500mm footprint
- Power supply requires dedicated circuit matching confirmed voltage and frequency, separate from other plant loads
- Machine arrives with host, mould, and JQ350 mixer; buyer provides trolley and curing racks
- Commissioning includes vibration frequency and hydraulic pressure adjustment to buyer’s mix design
- Operator training covers mould change procedure, pallet loading rhythm, and daily maintenance checkpoints
- Wear parts list identifies hydraulic seals, vibration motor bearings, and mould liner replacement intervals
What to Include in Your Inquiry
Provide the specific block formats your market demands (hollow, solid, paver dimensions), your target daily output, and the local aggregate types available for concrete mixing. Confirm your facility’s voltage, frequency, and preferred control display language so the electrical system matches your site conditions. State whether you need additional mould sets beyond the standard configuration, and indicate if you require pallet supply or will source them locally to match the 850×550×20mm specification.
Frequently Asked Questions
Q: How is the 960 pcs/h capacity calculated, and what happens when I switch to a smaller block format?
A: The 960 pieces per hour figure is based on 400×200×200mm hollow blocks with four cavities per mould and a 25-second molding cycle. When you switch to a smaller solid block or paver, the number of cavities per mould and the cycle time may differ, reducing or increasing hourly piece count. Request a capacity table showing output for each format you plan to produce.
Q: Where does the QTJ4-25 sit relative to fully automatic lines in terms of investment and footprint?
A: The QTJ4-25 is a semi-automatic stationary machine requiring manual pallet handling and trolley transport to curing areas, with lower capital cost and smaller footprint than automatic lines with stackers and cubing systems. Stepping up to full automation adds pallet feeders, automatic stackers, and curing rack handling equipment, increasing both investment and plant space requirements.
Q: What voltage and control language options must I confirm before the machine ships?
A: Voltage and frequency must match your local power grid (commonly 380V/50Hz or 440V/60Hz depending on region), and the control system language should match your operator’s preference. These are not pre-set defaults; you must confirm both before production begins to avoid commissioning delays.
Q: How many pallets do I need for continuous production, and can I source them locally?
A: Pallet quantity depends on your daily output, curing time, and how quickly pallets cycle back to the press. The 850×550×20mm size is specified for the QTJ4-25; you can source pallets locally if suppliers can match this dimension and material specification, or have them shipped with the machine.
Q: Which supporting equipment is included, and which items should I supply locally?
A: The standard configuration includes the QTJ4-25 host machine, one block mould set, and a JQ350 mixer. Buyers typically supply pallets, trolleys, curing racks, and raw material handling equipment locally to reduce shipping volume and match existing site infrastructure.

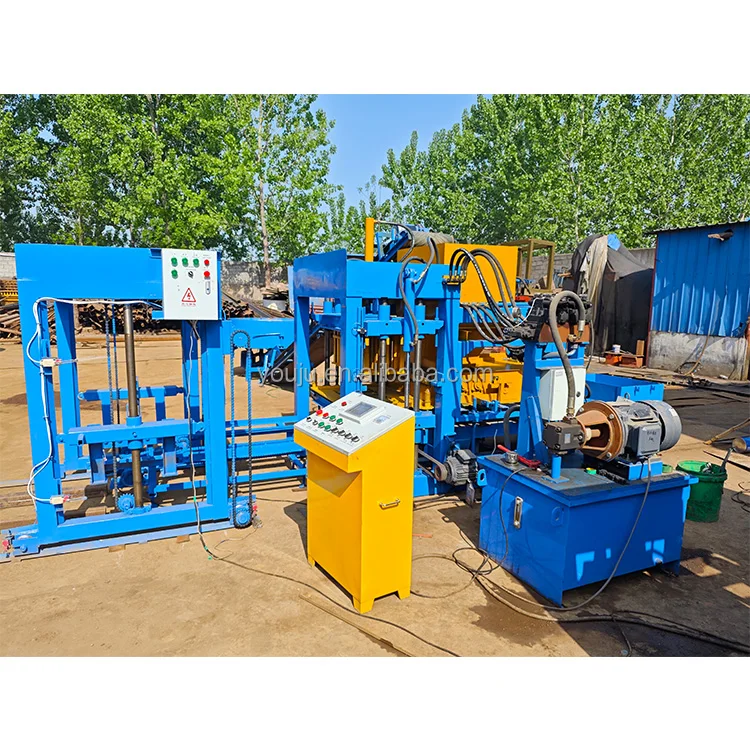
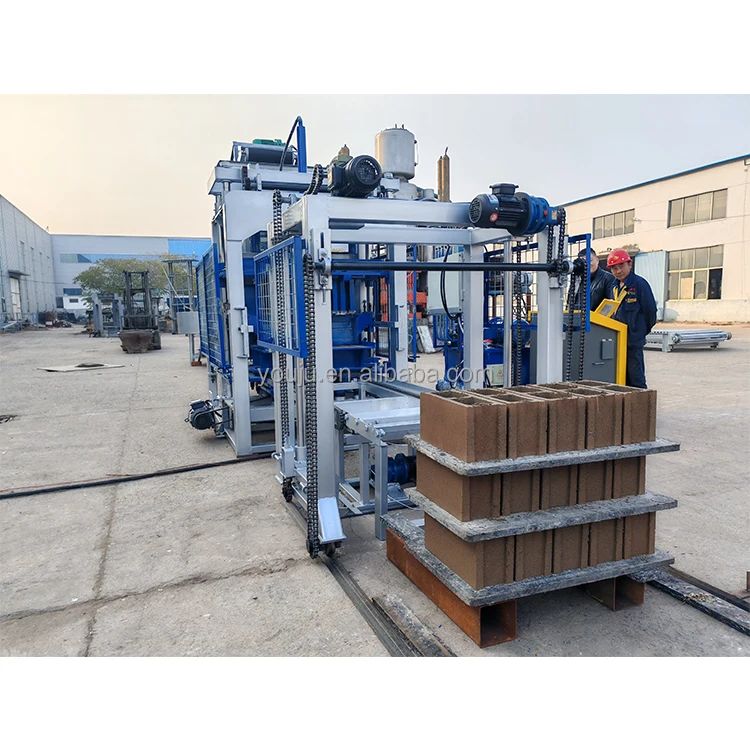 Stationary block machine