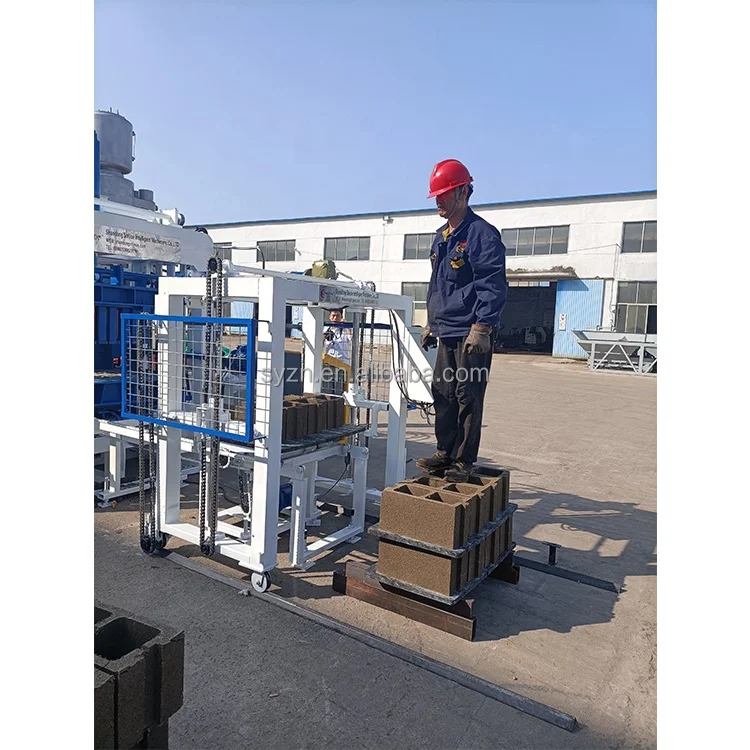
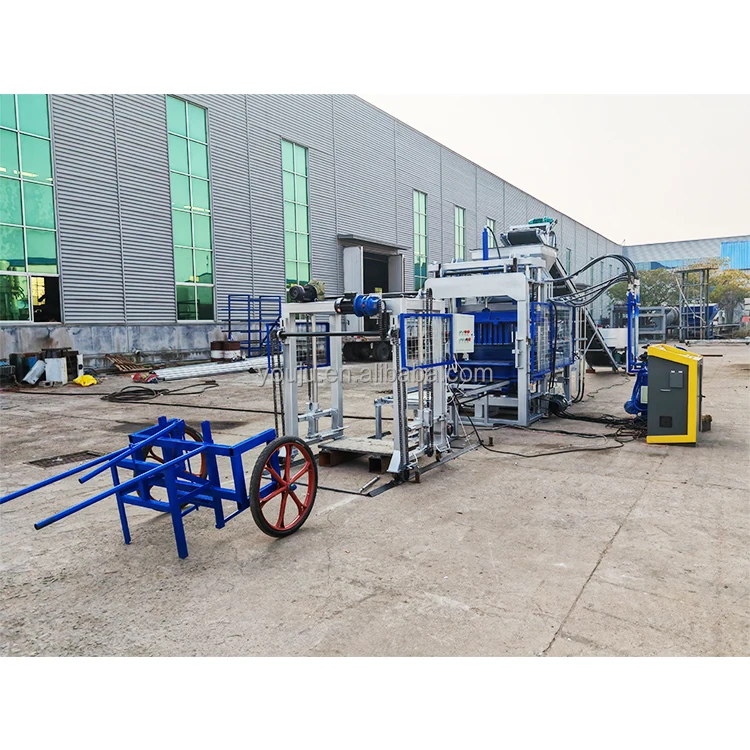
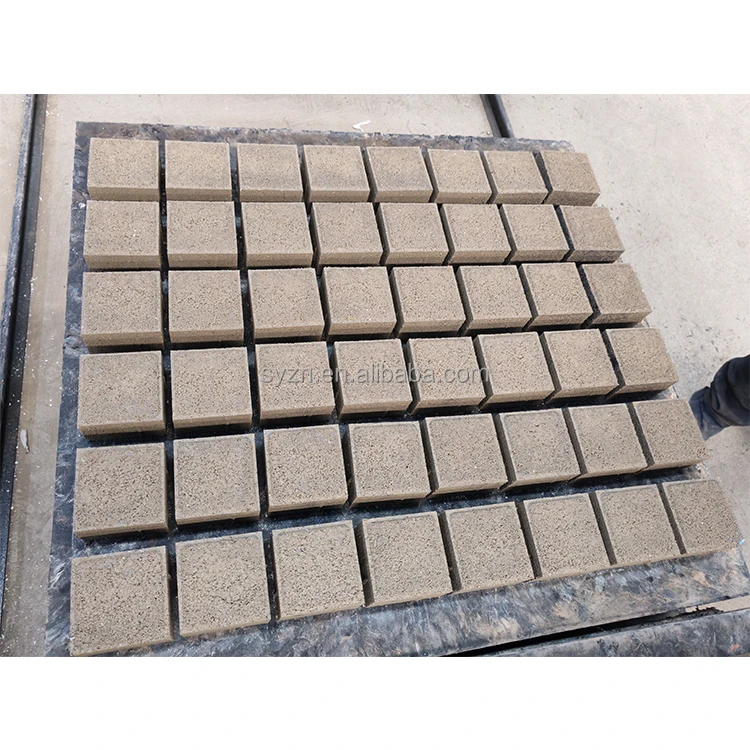
Matched System Configuration — The QT12-15 is specified as a complete line where mould, pallet, and handling equipment are configured together against your target block format, rather than assembled from separate suppliers.
Technical Specifications
| Parameter |
Value |
| Model |
QT12-15 |
| Product Type |
Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
9350 x 2520 x 2950 mm |
| Total Mass |
12000 kgs |
| Overall Power |
52 kW |
| Pallet Size |
1300 x 900 mm |
| Molding Cycle |
15-25 s (basis not stated in source — confirm block format / material / thickness) |
| Vibration Form |
Platform Vibration |
| Control System |
PLC cabinet |
| Hydraulic Station |
Included |
| Composition |
Pallet feeder, molding machine, storage hopper, block conveyor, hydraulic station, electrical PLC cabinet |
| Simple Production Line Configuration |
PL1200 batching machine, JS500 or JS750 mixer, 8m conveyor belt and stacker |
| Compatible Raw Materials |
Fly ash, slag, gangue, industrial wastes, river sand, gravel, cement |
| Mould Formats |
Hollow block, standard brick, pavement brick, road kerb, slope protection brick, planting grass brick (custom mould by buyer drawings available) |
Application Suitability
| Application |
Material or Output |
| Hollow block production plants |
Cement, fly ash, river sand, gravel mixes |
| Paving block and kerbstone manufacturing |
Crushed stone, slag, industrial waste aggregates |
| Porous and grass block formats |
Permeable concrete mixes for landscaping projects |
| Slope protection brick production |
Heavy-duty mixes for civil engineering applications |
Why Quoted Cycles Per Hour Rarely Match Site Output
The cycle time only becomes meaningful once your specific block format, mix design, and local aggregate are factored in.
Capacity figures for an automatic concrete block making machine manufacturer are often presented as a single number, but a 15–25 second cycle on a standard hollow block does not translate to the same throughput on a complex interlocking paver. I have seen buyers commit to a machine based on a catalogue number, only to find their local volcanic aggregate requires a different vibration frequency, cutting daily output significantly. The mismatch between quoted capacity and actual site performance remains one of the most common reasons for buyer dissatisfaction [NEED_CITE: common causes of block machine capacity shortfall].

Positioning Within the Full Block Machine Range
The QT12-15 sits at the high-capacity end of the stationary block machine lineup. Buyers surveying options for a first plant or a capacity replacement need to understand where this model fits relative to semi-automatic and mobile alternatives. The investment level, plant footprint, and automation degree all scale together at this tier, making it suitable for operations targeting consistent daily volumes across multiple block formats.
How the Six-Component Line Connects
A stationary block line is only as productive as its slowest station. The pallet feeder, molding machine, storage hopper, block conveyor, hydraulic station, and PLC cabinet must cycle in sequence so the press is never left waiting for a pallet or a mix charge. When any single component is underspecified, the entire automatic concrete block making machine manufacturer output drops regardless of the press rating [NEED_CITE: block production line bottleneck analysis]. This is why the QT12-15 is quoted as a matched system rather than a standalone press.
Reading the Specifications Against Your Site Conditions
The 52 kW overall power draw dictates the transformer and dedicated circuit you need on site before the machine arrives. The 1300 x 900 mm pallet size must align with your existing curing rack dimensions and forklift tine spacing, otherwise you face a costly pallet handling redesign. Platform vibration transfers energy through the pallet into the mix, meaning the vibration force and hydraulic pressure must be matched to your specific aggregate density and cement ratio to achieve consistent block strength. The PLC cabinet controls the 15–25 second moulding cycle, but that range assumes a material profile confirmed through sample testing.
The Hidden Cost of Skipping Material Sample Testing
When a buyer orders based on a brochure cycle time without sending local aggregate samples, the machine ships configured for a generic mix. On arrival, the vibration frequency may not compact the actual material properly, leading to weak blocks, high breakage during curing, and daily output far below expectation. Resolving this after installation means adjusting hydraulic pressure, modifying vibration parameters, and sometimes redesigning the mould, all of which delay production and erode buyer confidence [NEED_CITE: importance of raw material testing for block machines].
Why Procurement Through This Range Works
Block machinery is the single focus here, so the QT12-15 is specified alongside its mould, pallet, and handling equipment as one integrated system. The configuration is set against your actual mix design and target block format, not a catalogue default. Mould design covers the formats your market sells, including custom drawings for non-standard shapes. Automation level is selectable, allowing a buyer to start at a semi-automatic station and add automatic stacking later. Installation support includes on-site commissioning and operator training so the team running the line understands the parameter adjustments required for different formats.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for the quoted cycle time
- Machine specification sheet confirming pallet size, overall power, and vibration form against your site conditions
- Mould drawing and format list verifying which block types are included and which require custom tooling
- Voltage and control language confirmation to avoid commissioning delays after arrival
- Factory test record on your specified raw material mix before dispatch
Installation, Commissioning & Support
- Foundation must support the 12000 kg total mass with level tolerance across the 9350 mm length
- Dedicated circuit required for the 52 kW overall power draw with voltage confirmed before production
- Machine ships in component form for container loading, with reassembly supervised on site
- First-run commissioning includes parameter tuning for your local aggregate and target block format
- Operator training covers PLC cabinet interface, mould change procedure, and daily maintenance checkpoints
- Wear parts list and hydraulic spares provided for the first replacement cycle
What to Include in Your Inquiry
Provide your target block formats, daily output requirement, and the specific raw materials available locally including aggregate type and grading. Confirm your site voltage and frequency, the language needed for the PLC display, and the dimensions of your existing curing area. This allows the automatic concrete block making machine manufacturer configuration to be built around your actual conditions rather than a default setup.
Frequently Asked Questions
Q: Where does the QT12-15 sit compared to semi-automatic and mobile machines?
A: The QT12-15 is positioned at the high-capacity end of the stationary range, requiring a fixed plant with dedicated foundation and power supply. Semi-automatic models suit lower investment and smaller daily volumes, while mobile machines produce blocks on-site without a fixed plant. Each tier has a different footprint, automation degree, and output ceiling that should be matched to your project scale.
Q: How is daily output calculated, and which block format is assumed?
A: Daily output is derived from the moulding cycle time, the number of blocks per pallet, and the operating hours per shift. The 15–25 second cycle range requires confirmation of which block format, material mix, and thickness are assumed. A capacity calculation should always state the specific block format so you can compare quoted output against your actual product mix.
Q: Can I start semi-automatic and upgrade the line later?
A: Yes, the automation level is selectable and the line architecture supports staged upgrades. A buyer can begin with manual pallet handling and add automatic stacking or cubing as production volume grows. The PLC cabinet and hydraulic station are configured to accommodate additional automation modules without replacing the core press.
Q: What plant footprint and investment level should I plan for?
A: The QT12-15 line with PL1200 batching machine, mixer, and conveyor requires a covered production hall plus open curing area sized for the 1300 x 900 mm pallet format. Investment scales with automation level and supporting equipment included. A line layout should be confirmed before committing to building dimensions so all stations and material flow paths are accounted for.
Q: Which pallet size and material are specified, and how do they match my site?
A: The QT12-15 uses a 1300 x 900 mm pallet, which must align with your curing rack spacing and forklift capacity. Pallet material is selected based on the vibration force and expected service life. Confirming your existing handling equipment dimensions before ordering prevents a mismatch that would require separate pallet procurement or curing area modification.

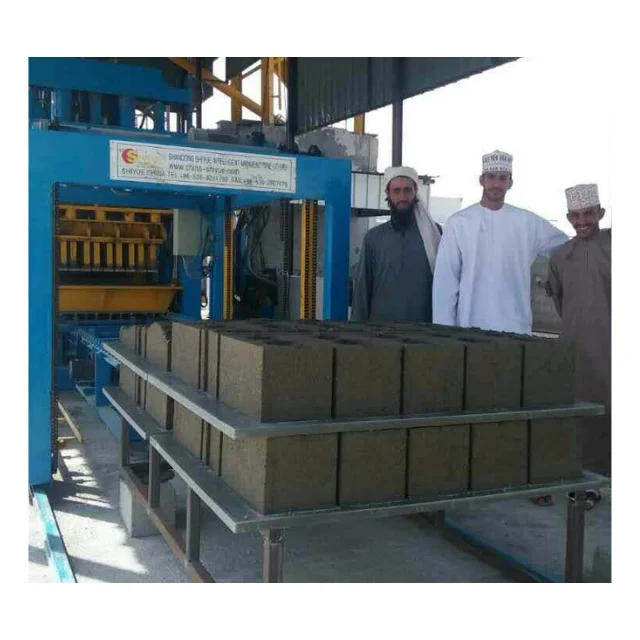
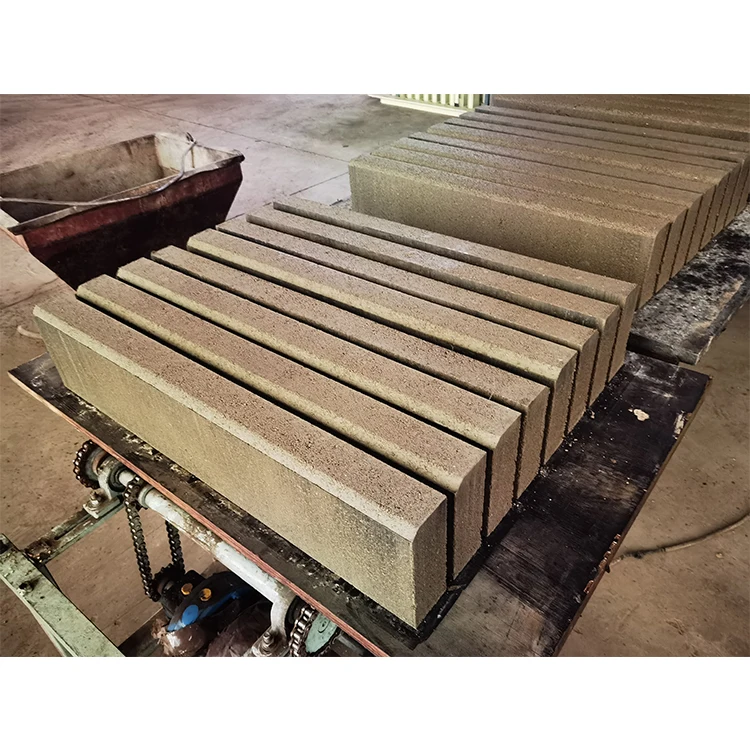 Stationary block machine