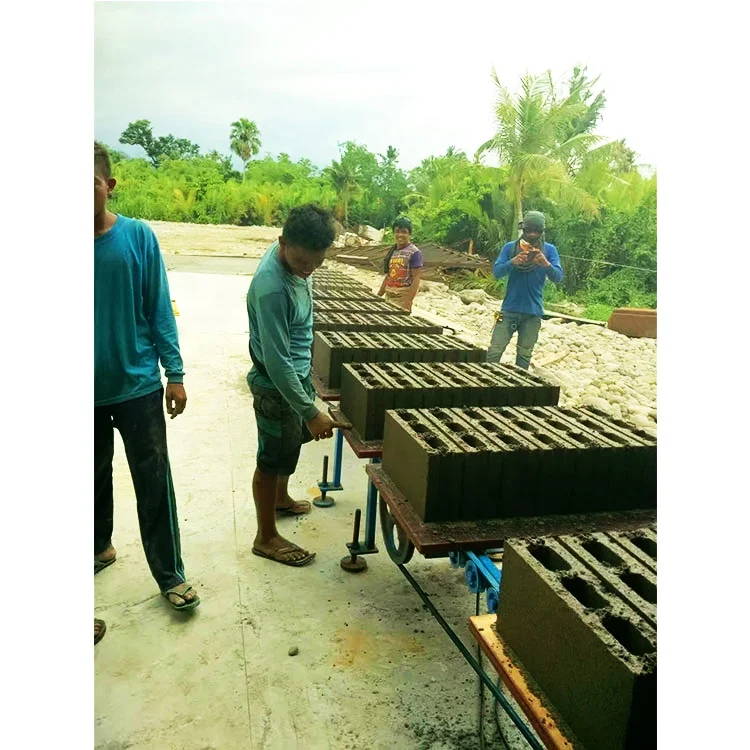
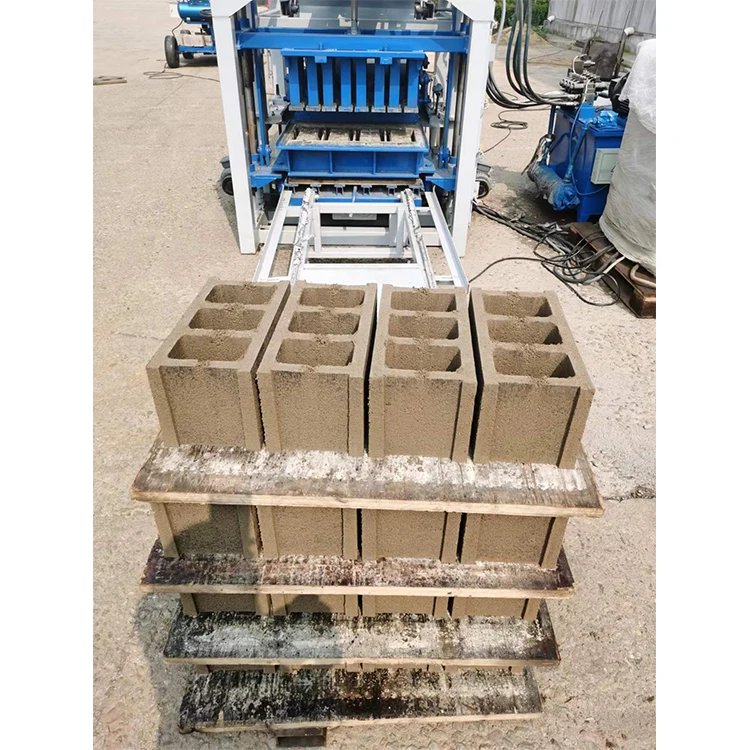
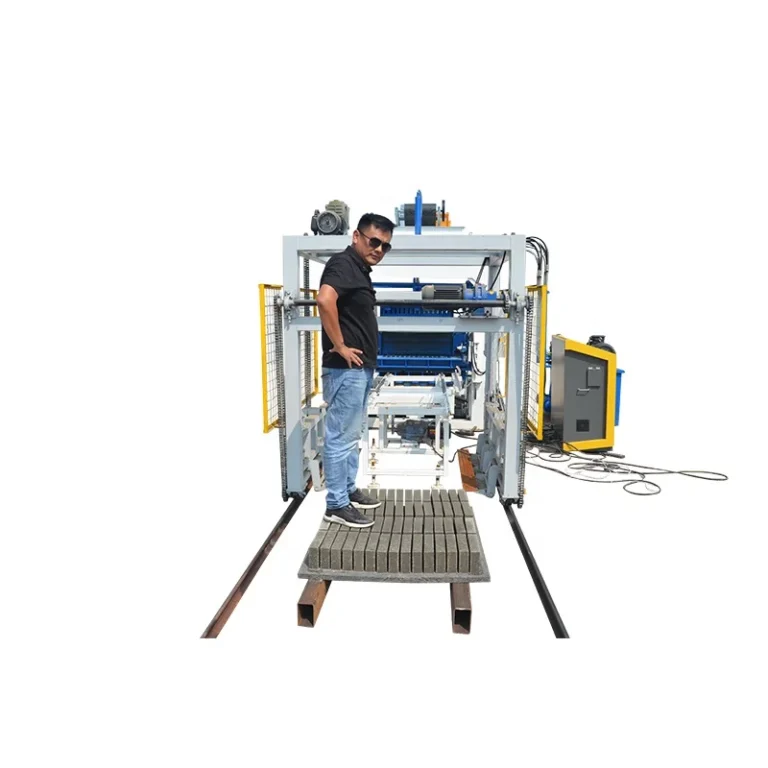
Matched System Integration — the LY1-10 is specified with compatible pallets, vibration settings, and mould options as a coordinated production unit rather than a standalone press.
Technical Specifications
| Parameter |
Value |
| Model |
LY1-10 |
| Product Type |
Semi-Automatic Clay Brick Making Machine |
| Rated Power |
1.5 kW |
| Molding Cycle |
45 seconds |
| Theoretical Productivity |
360 pcs/hour, 2880 pcs/day (based on 300×150×100mm block, 1 pc/mould) |
| Raw Materials |
Concrete, sand, cement, fly ash, lime, gypsum |
| Net Weight |
400 kg |
| Overall Dimensions (L×W×H) |
1300×1800×2400 mm |
| Vibration System |
Bed mould vertical vibration + upper mould compression vibration |
| Automation Level |
Semi-automatic |
| Voltage |
Configurable to local supply (frequency and phase to be confirmed before ordering) |
| Output Capacity |
1200–2400 pcs per 8-hour shift (basis not stated in source — confirm block format, material, and thickness) |
Application Suitability
| Application |
Material or Output |
| Workshop-level solid block production |
Concrete, sand, and cement mixes |
| On-site clay brick manufacturing for housing projects |
Local clay blended with lime or gypsum |
| Small-scale paver and masonry unit production |
Fly ash, cement, and aggregate combinations |
| Contractor-run block yards supplying local builders |
Crushed stone and cement with standard curing |
Why the Stated Capacity Rarely Matches Your First Month of Production
Output figures only mean something when the block format behind them is spelled out in writing.
The LY1-10 theoretical productivity is listed at 2,880 pieces per day, but that number assumes a specific 300×150×100mm block running at one piece per mould with a 45-second cycle. Switch to a larger hollow format or a thinner paver and the daily count shifts considerably. Many semi-automatic block machine manufacturer quotations quote a peak cycle rate without naming the format, which is why buyers arrive at commissioning expecting one number and producing another. [NEED_CITE: block format assumptions in capacity quotations across the industry]
When I visit plants in Latin America, the most common complaint is not that the machine failed — it is that the output never matched what the buyer thought they were purchasing. A 45-second cycle with a single-cavity mould producing a standard solid block is a very different proposition from the same cycle producing an interlocking paver with four cavities.

Where the LY1-10 Sits in the Full Machine Range
The LY1-10 occupies the entry semi-automatic tier. For first-time plant owners or contractors who need brick production on a project site without committing to a fully automatic line, this model offers a contained footprint at 1,300×1,800 mm and a net weight of 400 kg that fits inside a standard workshop bay. A semi-automatic block machine manufacturer typically positions this tier as the bridge between mobile egg-laying machines and high-capacity hydraulic presses.
Deciding Between Semi-Automatic and the Next Tier Up
The step up from the LY1-10 involves adding automatic pallet feeding, stacking, and PLC-controlled batching — systems that reduce labour but increase both capital outlay and floor space. If your daily target stays within the range of a single-operator workshop and your curing area is managed manually, the semi-automatic configuration keeps the investment proportional to your output. Buyers planning to scale within the first two years often start here and add automation modules later. [NEED_CITE: automation upgrade paths in block production lines]
How Vibration and Mould Design Shape Block Density
The dual vibration arrangement on this model — vertical vibration at the bed mould combined with compression vibration at the upper mould — addresses a problem common to single-source vibration: uneven compaction through the block height. With a 1.5 kW rated power driving the system, the vibration force must be matched to the buyer’s actual mix design. A fly-ash-heavy mix responds differently to vibration than a crushed-stone aggregate, and the 45-second moulding cycle only produces consistent density if the material flows and settles within that window. Pallet size, which must be confirmed before ordering, determines how many blocks cure per rack and whether your existing forklift can handle the loaded pallets. The semi-automatic block machine manufacturer should supply a mould drawing and format list so you can verify that the cavities match the dimensions your local market actually purchases.
The Hidden Cost of Skipping Configuration Details
Confirming voltage, frequency, and phase after the machine arrives is a recurring problem across export markets. A motor wound for 380V/50Hz connected to a 220V/60Hz supply will not simply underperform — it will overheat and fail, sometimes within the first shift. [NEED_CITE: electrical mismatch failures in imported industrial machinery] Pallet handling, stacking, and curing rack systems are often excluded from the base quotation, leaving buyers to manage output manually and wonder why the quoted daily capacity is unreachable. Mould change time is another variable that erases format flexibility if it consumes most of a shift.
What Sets This Procurement Path Apart
Block machinery is the sole focus, so the LY1-10 is not bundled from separate press, pallet, and handling suppliers — every component is specified as part of one system. Configuration starts from the buyer’s local aggregate and target block format, not from a catalogue default. Mould design covers the formats your market sells, including custom drawings when standard cavities do not match. The automation level is selectable, meaning you can commission semi-automatic now and plan an upgrade path without replacing the press. Installation support includes operator training so the team running the line understands cycle timing, mix adjustments, and mould change procedure from day one. A semi-automatic block machine manufacturer with this single-product focus eliminates the coordination gaps that appear when press, pallets, and moulds come from different sources.
Documentation & Verification
- Line layout drawing showing LY1-10 placement within your workshop dimensions
- Capacity calculation sheet stating the exact block format assumed for each output figure
- Machine specification sheet confirming vibration force, 1.5 kW rating, and pallet size
- Mould drawing and format list for your target block dimensions
- Voltage, frequency, and control language confirmation document signed before production
Installation, Commissioning & Support
- Foundation must support 400 kg static load across the 1,300×1,800 mm footprint
- Dedicated electrical circuit required matching confirmed voltage, frequency, and phase
- Machine ships partially assembled; on-site positioning and alignment included in commissioning
- First-run parameter setting covers 45-second cycle tuning to your specific mix design
- Operator training addresses mould change procedure, vibration adjustment, and daily maintenance
- Wear parts list identifies components requiring first replacement and recommended spare quantities
Before You Request a Quotation
To size the LY1-10 correctly, share the block formats your market demands along with target daily output and the raw materials available locally. Confirm your workshop dimensions, existing pallet inventory, and electrical supply specifications including voltage and frequency. If you already operate upstream mixing or downstream curing equipment, note those so the line layout accounts for the full workflow.
Frequently Asked Questions
Q: How is the capacity figure calculated and which block format does it assume?
A: The theoretical productivity of 2,880 pieces per day is based on a 300×150×100mm block at one piece per mould with a 45-second cycle. Different block formats, cavity counts, and material mixes will change the actual daily output. We provide a written capacity calculation stating the assumed format before you commit.
Q: What voltage, frequency, and phase options are available for my market?
A: Voltage is configurable to your local supply standard. Frequency and phase must be confirmed in writing before production begins, because a motor wound for the wrong specification will fail during commissioning. We document the agreed electrical configuration on the specification sheet.
Q: Where does the LY1-10 sit in the full machine range and when should I step up?
A: This model is the entry semi-automatic tier, suited for workshop-scale production with a single operator. If your daily target exceeds what a 45-second single-cavity cycle can deliver, or if you need automatic pallet stacking and PLC batching, the next tier in the range adds those capabilities with a larger footprint and higher investment.
Q: What mould formats are available and how long does a mould change take?
A: Mould formats depend on your local market requirements, and custom drawings are available. Mould change time varies with the specific format and operator familiarity. We provide a format list and change procedure so you can plan production schedules around realistic changeover windows.
Q: What is included in the quotation — does it cover pallets and handling?
A: The base quotation covers the LY1-10 press and specified moulds. Pallet size, material, handling equipment, and stacking systems are quoted separately based on your curing area layout and existing forklift capacity. Confirming these items early prevents surprises at commissioning.

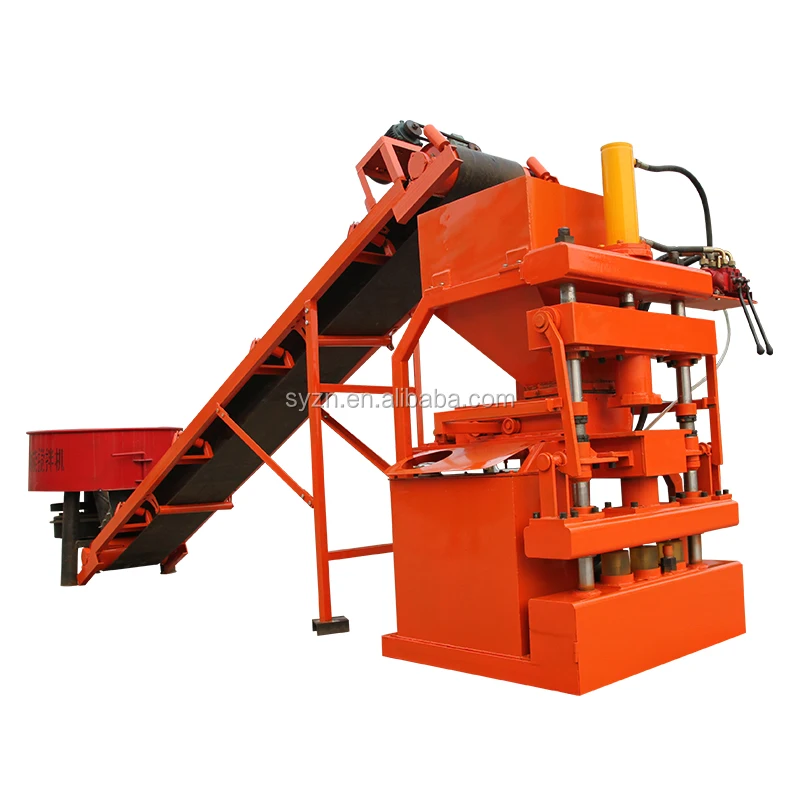
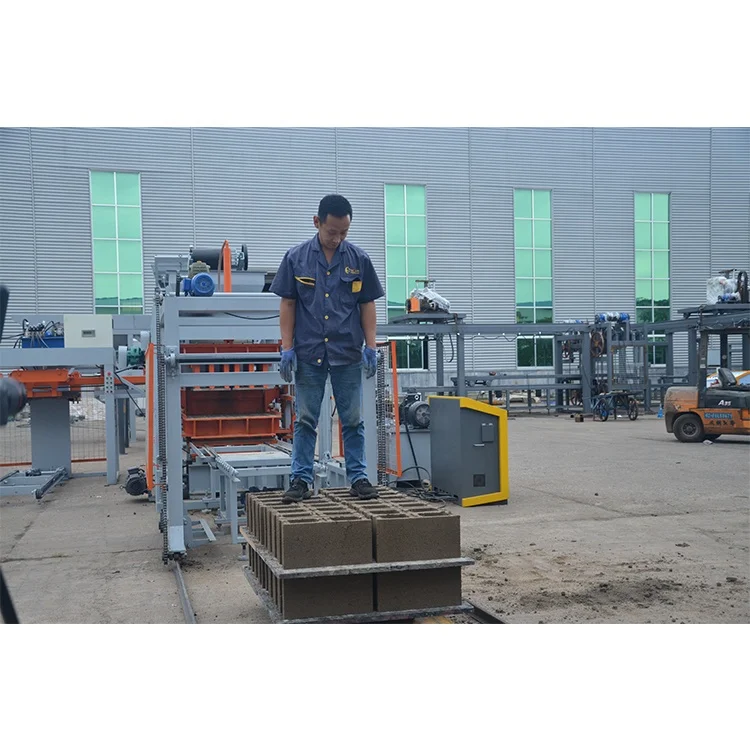 High quality block machine