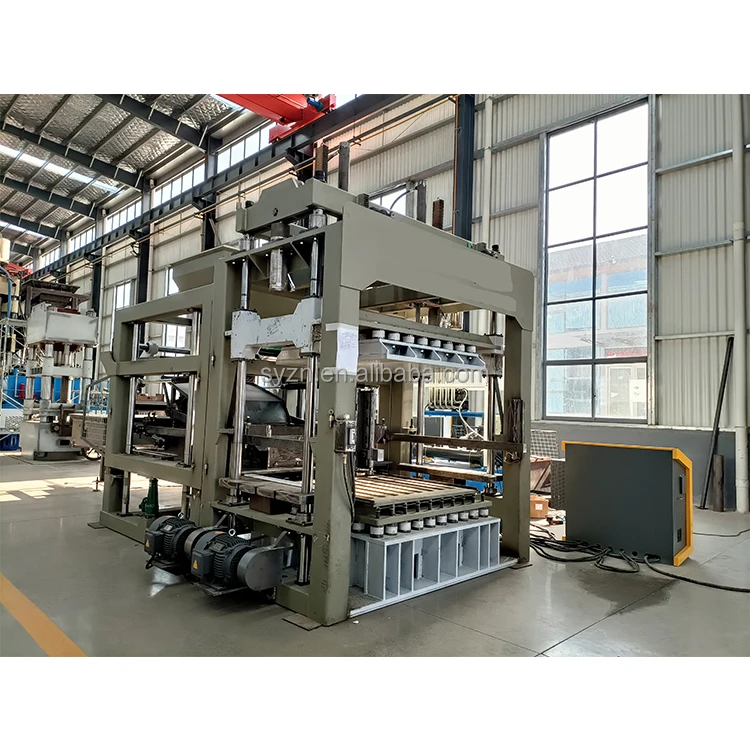
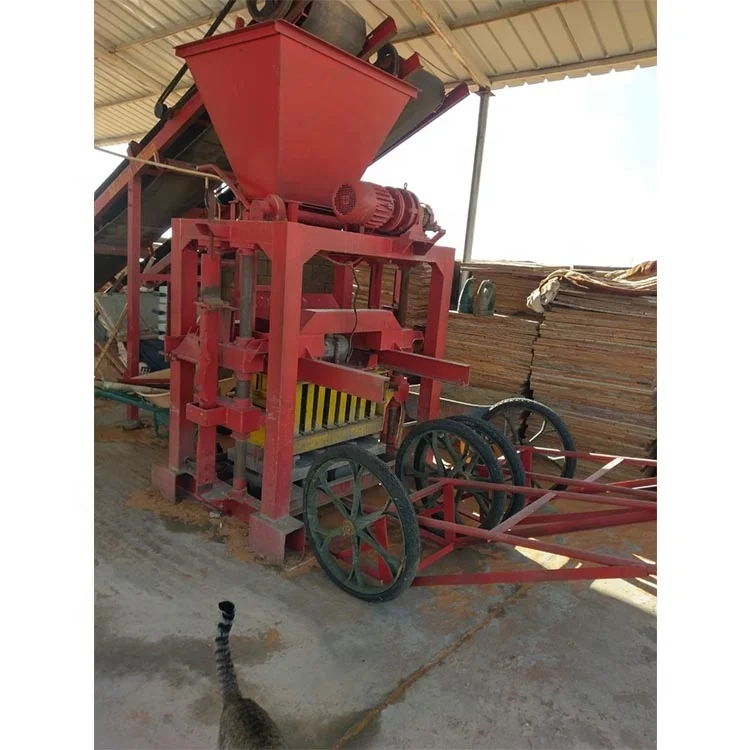
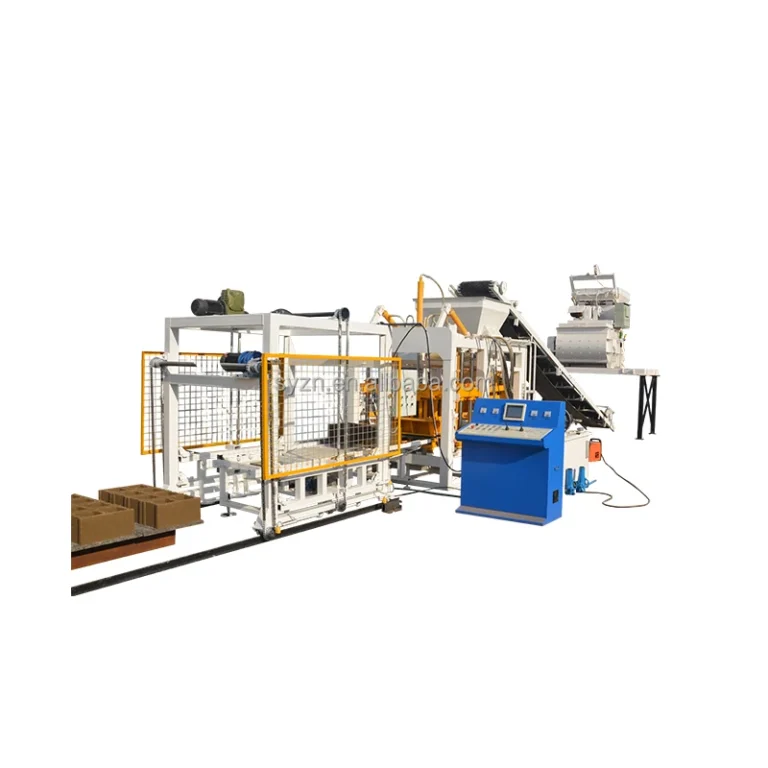
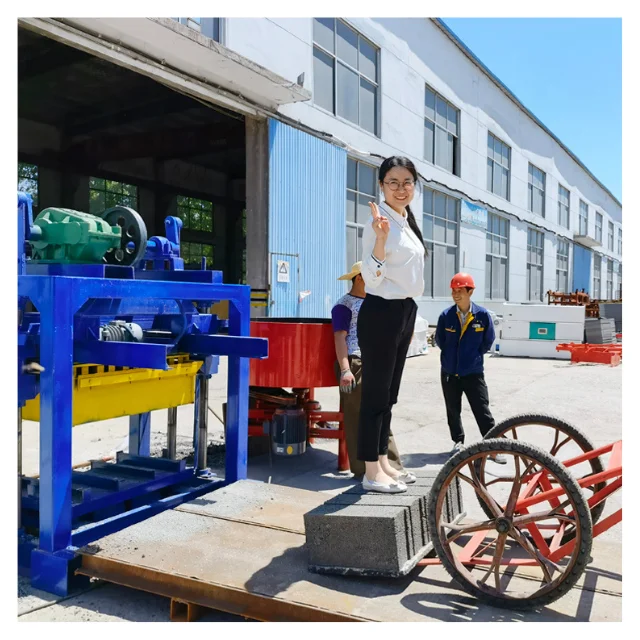
Single-focus block machinery engineering — machine, mould, pallet and handling specified as one matched system rather than assembled from separate suppliers, so the QTJ4-35 arrives as a complete working unit, not a press waiting for compatible peripherals.
Technical Specifications
| Parameter |
Value |
| Model |
QTJ4-35 |
| Product Type |
Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
1350×1460×1800 mm |
| Molding Cycle |
35 s |
| Vibration Frequency |
2800 r/min |
| Exciting Power (Vibration Force) |
30 kN |
| Total Power |
11.15 kW |
| Mixer Model |
JQ350 |
| Pallet Size |
850×450×20 mm |
| Net Weight |
1500 kg |
| Frame Construction |
Four-lead guide, channel steel frame |
| Mould Compression |
Upper and lower mould compression |
| Applied Products |
Hollow blocks (8 inch, 6 inch), solid bricks |
| Raw Materials |
Crushed stones, sand, cement, dust, fly ash |
| Output — Hollow Block 400×200×200 mm |
408 pcs/h, 3264 pcs/8 hr (based on 4 pcs/mould, 35 s cycle) |
| Output — Hollow Block 400×150×200 mm |
510 pcs/h, 4080 pcs/8 hr (based on 5 pcs/mould, 35 s cycle) |
| Output — Solid Brick 240×115×53 mm |
2100 pcs/h, 17000 pcs/8 hr (based on 18 pcs/mould, 35 s cycle) |
| Automation Level |
Semi-automatic / manual pallet handling |
| Voltage & Frequency |
Configurable to target market (basis to be confirmed before production) |
| Control System |
Available with PLC or manual control (basis to be confirmed) |
Application Suitability
| Application |
Material or Output |
| Small-scale hollow block plant |
8 inch and 6 inch concrete hollow blocks from crushed stone, sand and cement |
| On-site production for housing projects |
Solid bricks and hollow blocks using locally available aggregate |
| Fly ash brick manufacturing |
Fly ash blended with cement and sand for masonry units |
| First block plant for entrepreneurs |
Entry-level output tier with manual pallet handling and JQ350 mixer |
| Secondary line for existing distributors |
Compact footprint supplementary machine for solid brick and hollow block formats |
Why Voltage Confirmation Must Happen Before the Container Door Closes
A QTJ4-35 block machine manufacturer that skips the voltage conversation is leaving your commissioning schedule to chance.
I have seen QTJ-class machines arrive at sites running 440V with 380V motors bolted in. The machine sat idle for weeks while a transformer was sourced locally. That delay is not a shipping problem — it is a specification problem that should have been resolved before production started. When buyers ask about the QTJ4-35 block machine manufacturer, the first real question should be whether the supplier confirms your site voltage, frequency and PLC display language in writing before steel is cut [NEED_CITE: voltage and frequency standards by export market].
Placing the QTJ4-35 Within the Full Machine Range
The QTJ4-35 occupies the entry-level tier of our block machine range, positioned for buyers who need proven output without the capital commitment of a fully automatic line. This machine uses a vibration-based forming system with upper and lower mould compression, producing hollow blocks and solid bricks at a pace suited to first-time plant operators or contractors fulfilling a specific project. Understanding where it sits helps buyers decide whether this tier meets their daily volume or whether stepping up to a higher-capacity automatic model is justified.
How Output Tiers Compare Across the Range
Each tier in our range — from the QTJ4-35 through semi-automatic mid-range models to fully automatic high-capacity lines — is defined by what it removes from the operator and what it adds in consistency. At this level, pallet handling and stacking are manual tasks. Higher tiers introduce automatic pallet feeding, stacking and cubing, reducing labour while raising throughput. The gap between tiers is not just speed; it is the difference between a machine that needs an operator at every station and a line that runs from batching to stacking with minimal intervention [NEED_CITE: typical automation upgrade paths in block production]. Buyers comparing the QTJ4-35 block machine manufacturer against suppliers offering only one model should ask for a written range comparison showing where each tier fits.
Reading the Specifications That Actually Matter on Site
The 30 kN vibration force at 2800 r/min, paired with upper and lower mould compression, determines how densely the concrete mix is compacted into each cavity. Insufficient vibration against a stiff mix produces blocks that crumble at the edges; excessive force on a wet mix causes slumping before the block leaves the mould. The 850×450×20 mm pallet size is not a trivial detail — it dictates how many pallets your curing area can hold, whether your existing forklift can handle them, and how many blocks cure per square metre of yard space. The four-lead guide and channel steel frame keep the mould assembly aligned through thousands of vibration cycles, preventing uneven block height that buyers often mistake for a mix problem. The 35-second moulding cycle, combined with manual pallet handling, means realistic output depends heavily on how quickly your crew can swap pallets — a factor no catalogue figure captures.

What Happens When the Line Around the Press Is Ignored
A machine quoted in isolation — press only, no mixer, no pallet supply plan, no stacking method — leaves gaps that surface on day one of production. Pallets that do not match the curing rack spacing force double-handling. A mixer undersized for the press cycle means the mould waits for material, cutting real output well below the quoted figure. These are not defects in the QTJ4-35 itself; they are consequences of specifying the press without the line [NEED_CITE: block production line bottleneck causes].
What This Purchase Includes Beyond the Press
Block machinery as a single focus means the machine, mould, pallet and handling equipment are specified together, not sourced from separate vendors and bolted together at your site. Configuration is set against your actual mix design and local aggregate, not a default catalogue setting. Moulds are designed for the formats your market sells, with custom drawings available when standard formats do not match. The automation level is selectable — a buyer can start with the QTJ4-35’s semi-automatic setup and plan an upgrade path to higher automation without replacing the entire line. Installation support includes operator training so your crew understands mould changeover, daily maintenance and mix adjustment from the first shift.
Documentation & Verification
- Line layout drawing showing QTJ4-35 placement with mixer, pallet storage and curing area dimensions
- Capacity calculation sheet stating the exact block format and mould cavity count assumed for each output figure
- Voltage, frequency and PLC display language confirmation document signed before production begins
- Mould drawing and format list provided with quotation so block dimensions match your local market standard
- Factory test record with photographs issued before the machine leaves the workshop
Installation, Commissioning & Support
- Foundation requirements based on the 1500 kg net weight and 30 kN vibration force to prevent resonance transfer
- Dedicated electrical circuit sized for 11.15 kW total power draw with confirmed voltage and frequency matching your site supply
- Machine arrives as a single-unit frame; JQ350 mixer and pallet stock require separate staging space on arrival
- First-run commissioning includes mould alignment check, vibration frequency verification and test blocks from your local mix
- Operator training covers manual pallet handling rhythm, 35-second cycle pacing and upper-lower mould compression adjustment
- Wear parts list and mould maintenance schedule provided so replacements are ordered before the first changeover is due
Before You Send an Inquiry
Tell us the block formats your market actually sells — hollow block dimensions, solid brick sizes, and any paver or kerbstone requirements. Share your site voltage and frequency, the raw materials you can source locally, and the daily output you need per format. If you already have curing racks, forklifts or a mixer on site, let us know their specifications so the QTJ4-35 block machine manufacturer proposal fits your existing setup rather than replacing it.
Frequently Asked Questions
Q: How is the QTJ4-35 output calculated, and which block format does each figure assume?
A: Every output figure is tied to a specific block size, mould cavity count and 35-second cycle. For example, 400×200×200 mm hollow blocks are calculated at 4 pieces per mould, yielding 3264 pieces per 8-hour shift. We provide a capacity sheet stating the exact format assumed for each number so there is no ambiguity between quoted and achievable output.
Q: Where does this machine sit in the range — when should I step up to an automatic line?
A: The QTJ4-35 is our entry-level tier with manual pallet handling and semi-automatic operation. Buyers whose daily volume consistently exceeds what a manual crew can sustain, or who need multiple block formats with fast changeovers, typically move to mid-range or fully automatic tiers where pallet feeding, stacking and cubing are mechanised.
Q: What voltage options are available, and how is this confirmed before production?
A: Voltage and frequency are configured to your site supply — this is not a default setting. We confirm your exact voltage, frequency and control language in writing before production starts, so the machine arrives ready to connect without transformer swaps or rewiring delays.
Q: What is the plant footprint including the mixer and pallet handling area?
A: The press itself measures 1350×1460×1800 mm, but the working footprint must include the JQ350 mixer, pallet storage, curing yard and block stacking area. We provide a line layout drawing showing recommended spacing so you can verify your site accommodates the full setup before ordering.
Q: Can the QTJ4-35 be upgraded later to higher automation?
A: The machine is part of a range designed with an upgrade path. Buyers can start with semi-automatic operation and later add automatic pallet feeding, stacking or cubing stations. The specific upgrade options depend on your production growth and the formats you add over time.

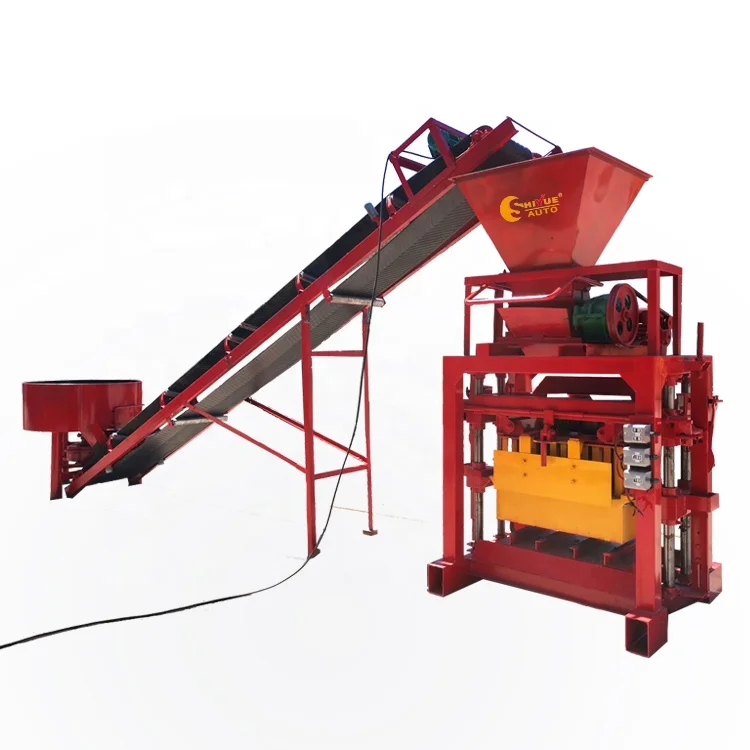
 High quality block machine