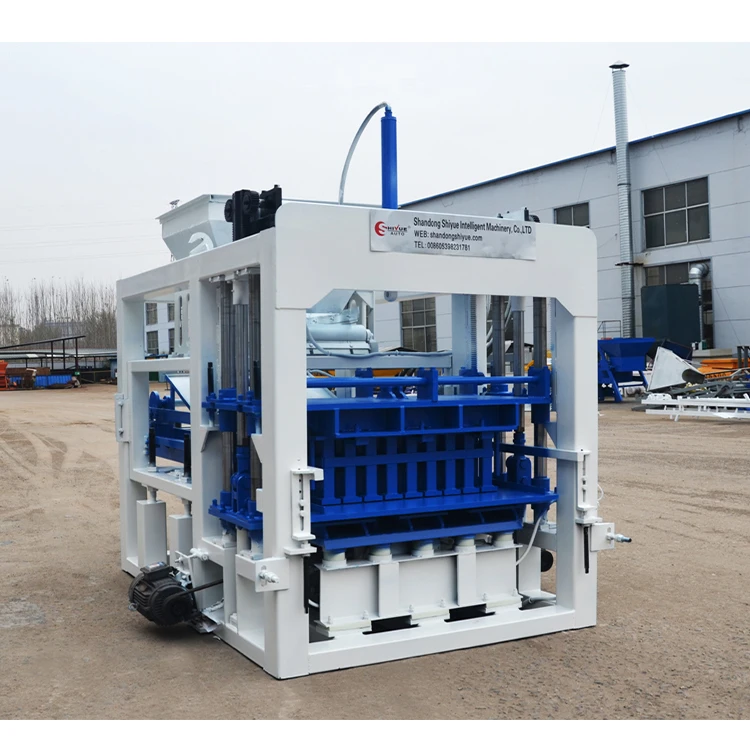
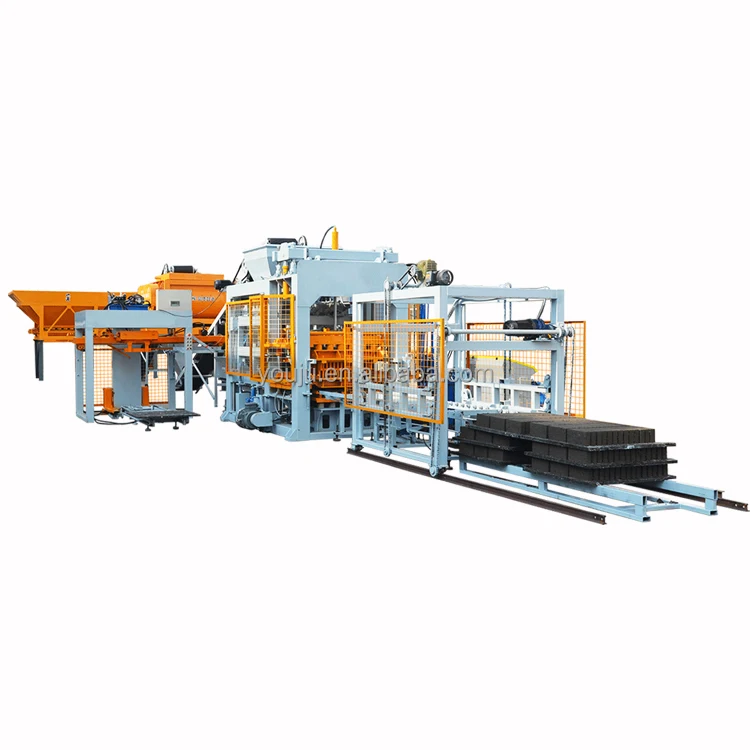
System-matched configuration — The QT10-15 is specified as a complete line where press, pallet, mould and handling are sized to one another, so the buyer receives a coordinated plant rather than a collection of unrelated stations.
Technical Specifications
| Parameter |
Value |
| Model |
QT10-15 |
| Product Type |
Fully Automatic Concrete Block Making Machine |
| Overall Dimension |
9350 × 2320 × 2950 mm |
| Total Mass |
10 T |
| Rated Pressure |
21 MPa |
| Vibration Force |
60 KN |
| Main Vibration Form |
Platform Vibration |
| Vibration Frequency |
2800 ~ 4500 r/min |
| Pallet Size |
1100 × 900 mm |
| Molding Cycle |
15–25 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power |
44 kW |
| Demolding Method |
Hydraulic |
| General Water Consumption |
8 T / Day |
| Factory Area |
500 m² |
| Control System |
PLC with person-machine conversation interface |
| Automation Level |
Fully automatic production line |
| Applied Products |
Hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material |
Crushed stone, sand, cement, dust, fly ash, gravel, slag |
Application Suitability
| Application |
Material or Output |
| Hollow block production for building envelopes |
Crushed stone, sand, cement, fly ash |
| Solid load-bearing block manufacturing |
Gravel, slag, cement blends |
| Interlocking paver and colored paver runs |
Fine aggregates with pigment additives |
| Curbstone and riverside brick forming |
Coarse aggregate and cement mixes |
| Grassed and revetment brick for landscaping |
Sand, cement, and lightweight aggregates |
What "15–25 Seconds per Cycle" Actually Means for Your Daily Output
Cycle time only becomes meaningful once the block format, mix design, and curing method are fixed.
Catalogue sheets often quote a single molding cycle without naming the format it applies to, and buyers plan their plant revenue around a number that disappears the moment a different mould is installed. On the QT10-15 automatic concrete block making machine, the 15–25 s window shifts depending on whether you are pressing thin pavers or tall hollow blocks, and on how much compaction the local aggregate demands [NEED_CITE: block format assumptions behind published cycle times]. I have watched lines stall because the quoted cycle assumed a standard 400 × 200 × 200 mm hollow block while the buyer’s market actually moved 150 mm solid partitions. Clarifying the format before signing the proforma prevents that gap.

Placing the QT10-15 Within the Full Machine Range
The QT10-15 occupies the high-capacity tier of a lineup that also includes semi-automatic and mobile egg-laying models, so a buyer evaluating this automatic concrete block making machine can see exactly where it sits relative to lower-investment alternatives. Pallet dimensions of 1100 × 900 mm define the upper footprint of block formats the press can handle in a single stroke, and that same pallet size must match the curing racks and forklifts already on site.
How Automation Level Shapes the Rest of the Line
A fully automatic configuration pairs the press with pallet feeding, stacking, and cubing stations so that output leaves the line already grouped for curing. Buyers who begin with a semi-automatic version of this platform can plan a later transition without replacing the press itself, keeping the capital already invested in the mould set and pallet inventory [NEED_CITE: upgrade paths between automation tiers]. The decision therefore is not just about today’s labour cost but about the footprint and handling equipment you want to grow into.
Reading the Specs That Decide Block Quality
Rated pressure at 21 MPa and vibration force at 60 KN work together: pressure squeezes the mix into the mould cavity while platform vibration at 2800–4500 r/min settles fine particles around the coarse aggregate. If the local sand carries high clay content, the vibration frequency may need to stay at the upper end to break air pockets, and the hydraulic dwell time extends accordingly. The 44 kW overall power budget must cover both the hydraulic pump and the vibration motors simultaneously, so undersized supply cables cause the press to stall mid-cycle. A 500 m² factory area is quoted for the complete line; the actual floor plan depends on how much curing rack space your daily volume demands.
The Cost of Overlooking Pallet and Handling Alignment
When pallet size is chosen without checking the curing yard, forklifts cannot stack racks two high and half the yard sits empty. Mould changes that take most of a shift erase the format flexibility the buyer paid for, and a PLC display in a language the operator cannot read turns a fully automatic line back into a manual one [NEED_CITE: commissioning delays caused by unconfirmed control language]. These consequences are not machine defects; they are specification gaps that surface only after the container arrives.
Why Buyers Source This Tier From Shiyue
Block machinery is the single focus here, so the QT10-15 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate vendors. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default, which is why I insist on sample material trials before locking the vibration parameters. Mould design covers the formats the buyer’s market actually sells, including custom drawings when a standard cavity does not fit. Automation level is selectable, meaning a plant can open semi-automatic and add stacking and cubing later without swapping the press. Installation support includes operator training so the crew can run independent shifts before the commissioning engineer leaves site.
Documentation & Verification
- Line layout and capacity calculation naming the exact block format behind each output figure
- Machine specification sheet confirming pallet size 1100 × 900 mm, vibration force, and hydraulic ratings
- Mould drawing and format list showing cavity dimensions and the mould change procedure
- Voltage, frequency, and PLC display language confirmation signed before production begins
- Factory test record run on the buyer’s target block format before the line is crated
- Wear parts and mould list identifying items to reorder during the first year of operation
Installation, Commissioning & Support
- Foundation drawing matched to the QT10-15 overall mass of 10 T and vibration load
- Power supply verification for 44 kW total draw, including dedicated circuit for vibration motors
- Machine dismantled for container loading and reassembled on site with alignment checks
- First-run parameter tuning against the buyer’s local aggregate and mix moisture content
- Operator training on PLC interface, mould change sequence, and daily lubrication points
- Spare mould and hydraulic wear parts list handed over before commissioning sign-off
What to Share Before Requesting a Quotation
Provide the target block formats with dimensions, the daily volume you plan to sell, and the raw materials available within hauling distance of your site. State your local voltage and frequency, the language your operators need on the PLC screen, and the curing area you can allocate. With those details, the line layout can be drawn to your actual conditions instead of a generic template.
Frequently Asked Questions
Q: How is the QT10-15’s capacity calculated, and which block format is assumed?
A: The 15–25 s molding cycle is a range that shifts with block thickness, mix stiffness, and target density. A formal capacity calculation names the exact format — for instance, 400 × 200 × 200 mm hollow block — and multiplies by the number of cavities per pallet and available production hours. Without that format anchor, the quoted pieces-per-hour figure is not comparable across suppliers.
Q: Where does the QT10-15 sit compared to semi-automatic and mobile machines?
A: It occupies the high-output fully automatic tier, paired with pallet feeders and stackers. Semi-automatic models use the same mould range but rely on manual pallet handling, while mobile egg-laying machines produce blocks directly on the ground without pallets. Choosing between them depends on daily volume targets, labour availability, and whether a fixed curing yard exists.
Q: What pallet size does the QT10-15 use, and does it match standard curing racks?
A: The QT10-15 runs on 1100 × 900 mm pallets. Before ordering, confirm that your curing racks and forklift fork spacing accept that dimension; otherwise, racks must be custom-built or the pallet size adjusted at the configuration stage to align with your existing handling fleet.
Q: Can the automation level be upgraded later if I start semi-automatic?
A: Yes. The press platform is common across automation tiers, so stacking and cubing stations can be added once production volume justifies the investment. The original mould set and pallet inventory remain in use, and the PLC programme is extended rather than replaced.
Q: What plant footprint does a complete QT10-15 automatic line require?
A: A factory area of around 500 m² is quoted for the press, mixer, pallet return, and stacking stations. The curing yard is additional and scales with daily output and ambient curing time. Ceiling height must clear the 2950 mm machine height plus lifting space for mould changes and maintenance access.
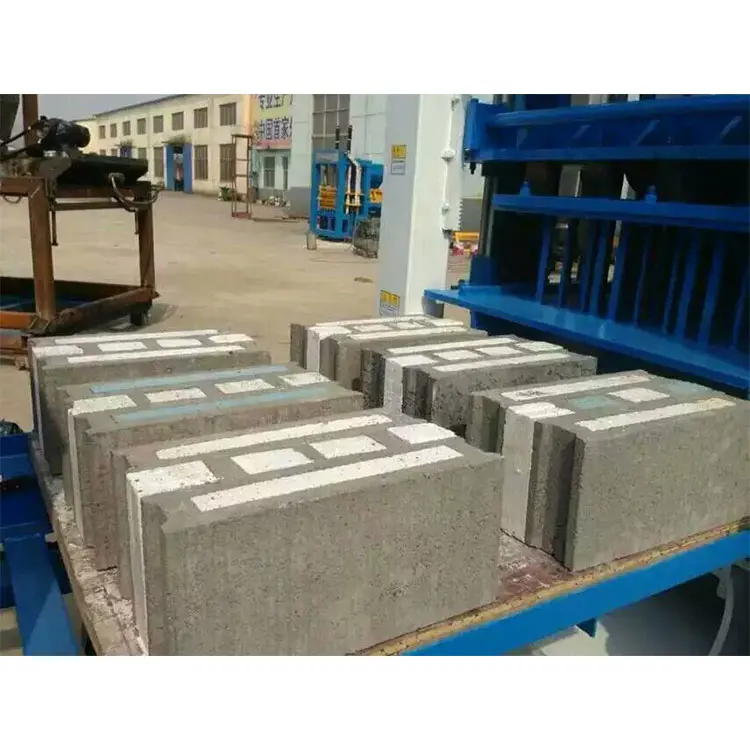 Automatic block machine