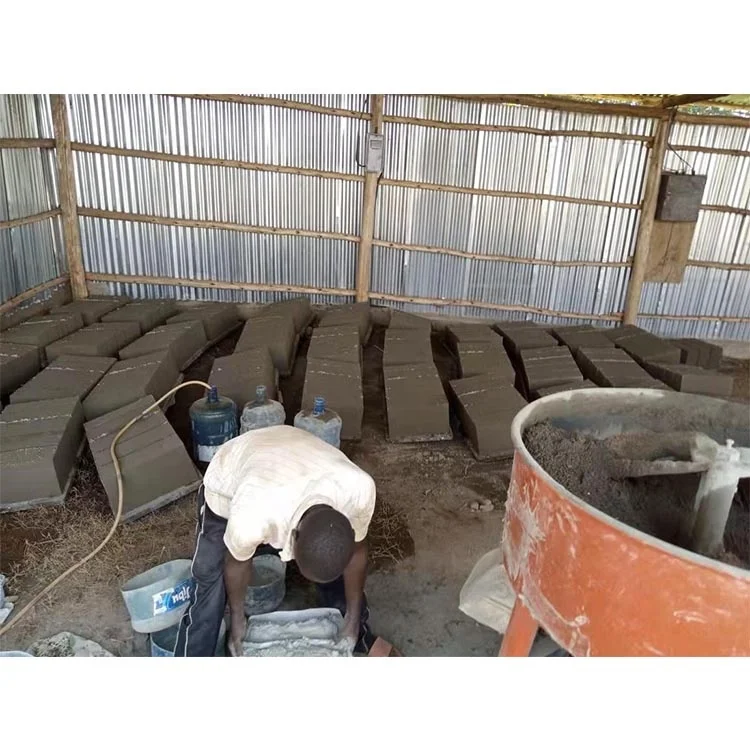
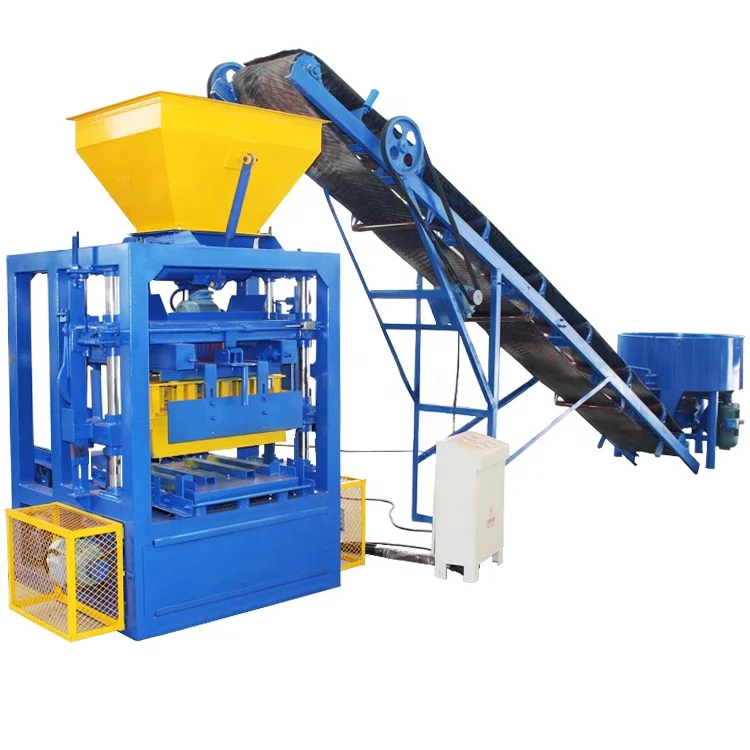
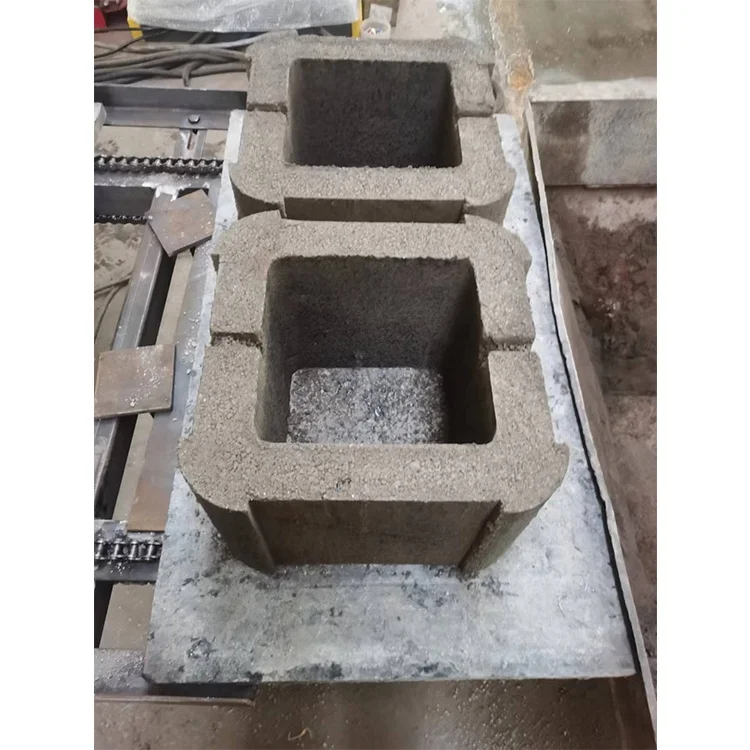
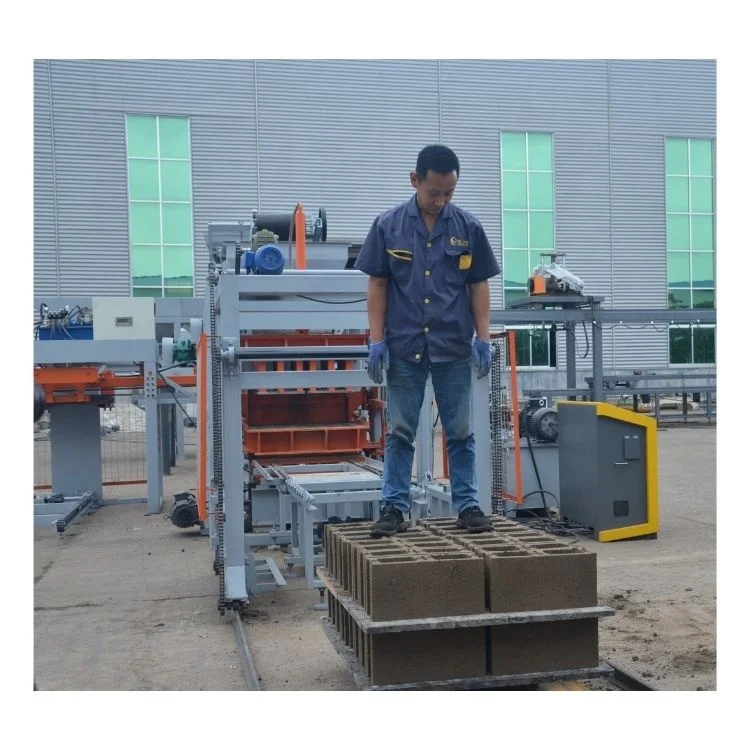
Matched System Design — the QTJ4-40 is specified as a complete unit of machine, mould, pallet, and handling, not a standalone press patched together with mismatched components from different suppliers.
Technical Specifications
| Parameter |
Value |
| Model |
QTJ4-40 |
| Product Type |
Semi-Automatic Concrete Block Making Machine |
| Machine Power |
9.5 kW |
| Molding Cycle |
40 s |
| Theoretical Productivity (400×200×200 mm hollow block, 4 pcs/mould) |
360 pcs/h, 2800 pcs/day (basis to be confirmed) |
| Theoretical Productivity (400×150×200 mm hollow block, 5 pcs/mould) |
450 pcs/h, 3600 pcs/day (basis to be confirmed) |
| Theoretical Productivity (225×112.5×60 mm solid brick, 9 pcs/mould) |
800 pcs/h, 6400 pcs/day (basis to be confirmed) |
| Raw Materials |
Concrete, sand, cement, fly ash, lime, gypsum |
| Vibration System |
Bed mould vertical vibration + upper mould compression vibration |
| Mould Actuation |
Top die push and pull with automatic scraper |
| Pallet Size |
850 × 450 mm |
| Overall Dimensions (L×W×H) |
1350 × 1460 × 1800 mm |
| Machine Weight |
1 T |
| Automation Level |
Semi-automatic |
| Stacking Method |
Manual |
| Voltage |
Configurable to buyer’s local supply (to be confirmed) |
Application Suitability
| Application |
Material or Output |
| First block plant for entrepreneurs |
Hollow blocks and solid bricks from locally sourced sand, cement, and fly ash |
| On-site contractor production |
Construction blocks manufactured directly at the building site without fixed infrastructure |
| Small workshop block line |
Pavers and solid bricks added to an existing building materials operation |
| Rural and peri-urban housing projects |
Load-bearing hollow blocks using crushed stone and cement mixes |
What "2000 Pieces per Day" Actually Means for Your Site
Every capacity figure for this semi-automatic block machine manufacturer is tied to a named block format, mould cavity count, and cycle time — never a single headline number.
Catalogue sheets often quote one peak output without stating whether the figure assumes hollow blocks, solid bricks, or interlocking pavers. A buyer who reads "2500 pcs/day" and expects that rate across every format will see real daily production fall well short once the first mould change happens. In my years commissioning block lines, I have watched plants arrive on site only to discover the quoted capacity assumed a standard sand mix while the local aggregate was volcanic ash or crushed coral, forcing a complete recalibration of vibration force and pressing time [NEED_CITE: local aggregate variation and block strength outcomes]. That mismatch costs weeks of lost production and eroded buyer confidence before the line ever reaches steady output.

Where the QTJ4-40 Sits in the Full Range
This model occupies the entry point of the semi-automatic tier, aimed at buyers who need dependable small-scale output before committing to a fully automatic line. The 9.5 kW power rating and 1 T machine weight keep foundation and electrical requirements modest, making it a practical fit for workshops where a high-capacity press would be oversized. As a semi-automatic block machine manufacturer, Shiyue positions this unit so that a buyer can start here and move to higher tiers in the range as market demand grows.
Semi-Automatic Operation Without Compromise on Density
The QTJ4-40 combines bed mould vertical vibration with upper mould compression vibration, a dual system that compacts the mix from both directions during the 40-second cycle. The top die push-pull mechanism with automatic scraper handles mould filling and release without requiring the operator to intervene at the press itself. This keeps block-to-block density consistent across a shift, which matters far more to end-user acceptance than peak hourly output [NEED_CITE: block density consistency standards for load-bearing masonry].
Reading the Spec Sheet Against Your Actual Product Mix
The 850 × 450 mm pallet size defines the maximum mould footprint and therefore the range of block formats this machine can produce. Before ordering, a buyer needs to confirm which formats the local market actually purchases — hollow blocks for wall construction, solid bricks for paving, or a mix of both — because each format changes the pieces-per-mould count and the realistic daily throughput. The vibration system must also be tuned to the buyer’s specific aggregate and cement ratio; a mix high in fly ash behaves differently under vibration than one based on sharp sand, and the wrong setting leads to surface cracking or low compressive strength. Voltage and frequency must be locked in before production begins, since arriving on site with a 380 V motor in a 220 V region delays commissioning by weeks [NEED_CITE: voltage and frequency standards by export market].
The Cost of Skipping the Configuration Step
When a buyer selects a machine purely on price and headline capacity, the hidden costs surface after arrival. Pallet size may not match the curing racks already built on site, forcing a rebuild of the entire drying area. Voltage mismatches mean rewinding motors or sourcing transformers locally. If the mould set does not cover the block formats the buyer’s customers actually order, the machine sits idle while new moulds are shipped internationally, each delay compounding lost revenue and strained contractor relationships [NEED_CITE: CE machinery directive requirements for industrial equipment].
Why Source This Semi-Automatic Block Machine Manufacturer
Block machinery is the single focus here, so the QTJ4-40 is never quoted as a bare press — pallet, mould, and handling are specified as one matched system from the first conversation. Configuration is set against the buyer’s actual mix design and target block format, not pulled from a default catalogue page. Mould design covers the formats the buyer’s market sells, including custom drawings when a local format falls outside standard sizes. The automation level is selectable: a buyer can start with the QTJ4-40’s semi-automatic setup and move to higher tiers within the same range as production grows. Installation support includes on-site commissioning and operator training so the line reaches stable output before the service team leaves.
Documentation & Verification
- Line layout with capacity calculation stating the exact block format and cycle time assumed for each output figure
- Machine specification sheet confirming voltage, frequency, and control language before production starts
- Mould drawing and format list covering every block type the buyer’s market requires
- Factory test record with photographs taken on the buyer’s specified mix before dispatch
- Packing photographs and customs documentation support provided before the container seals
Installation, Commissioning & Support
- Foundation plan sized to the QTJ4-40’s 1350 × 1460 mm footprint and 1 T operating weight
- Dedicated electrical circuit rated for the 9.5 kW motor at the buyer’s confirmed local voltage and frequency
- Machine shipped in a configuration that allows offloading and positioning with standard workshop equipment
- First-run commissioning on the buyer’s actual aggregate and cement ratio with vibration parameters adjusted on site
- Operator training covering mould change procedure, daily maintenance checkpoints, and pallet handling workflow
- Wear parts list and mould interchange guide supplied so replacements can be ordered before stock runs low
Before You Request a Quote
To size the QTJ4-40 correctly for your operation, start with the block formats your market buys most and the daily volume each format requires. Share your local aggregate type and any existing mix design data so the vibration and compression settings can be matched before the machine is built. Confirm your site’s voltage, frequency, and the language you need on the control display. If you already have curing racks or a forklift in place, send the pallet dimensions and rack spacing so the handling layout aligns from day one.
Frequently Asked Questions
Q: How is the QTJ4-40 capacity calculated, and which block format does each figure assume?
A: Every capacity figure is tied to a specific block dimension, mould cavity count, and the 40-second cycle. For example, the hollow block figure assumes a 400×200×200 mm format with four cavities per mould. When the format changes, pieces per mould change, and so does daily output. We provide a format-by-format breakdown so buyers see realistic numbers for the blocks they actually sell.
Q: Where does the QTJ4-40 fit in the full machine range?
A: It sits at the entry of the semi-automatic tier, suited for first plants and small workshops. Buyers who outgrow its output can move to higher tiers within the same range, keeping mould and pallet compatibility where possible. We help a buyer identify the crossover point based on actual daily demand, not catalogue assumptions.
Q: What voltage and control options are confirmed before the machine ships?
A: Voltage and frequency are confirmed during the quotation stage based on the buyer’s local supply. The motor is wound to match, and control display language is set before assembly. This prevents costly rewinding or transformer sourcing after the machine arrives on site.
Q: How is the pallet size matched to existing curing infrastructure?
A: The 850 × 450 mm pallet is specified alongside the buyer’s curing rack dimensions and forklift capacity. If existing racks use a different spacing, we adjust the pallet or recommend rack modifications before the machine enters production, avoiding costly rebuilding after delivery.

 High quality block machine