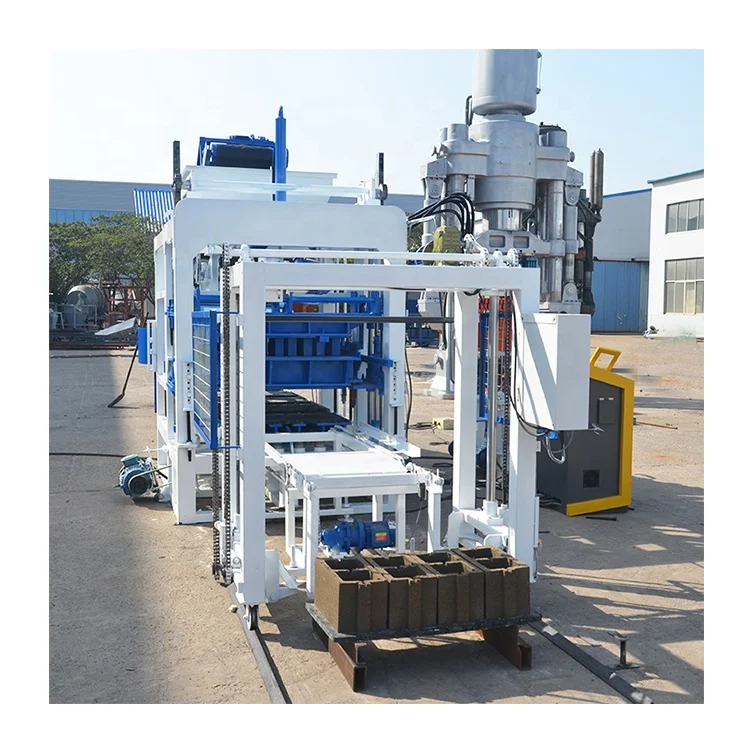
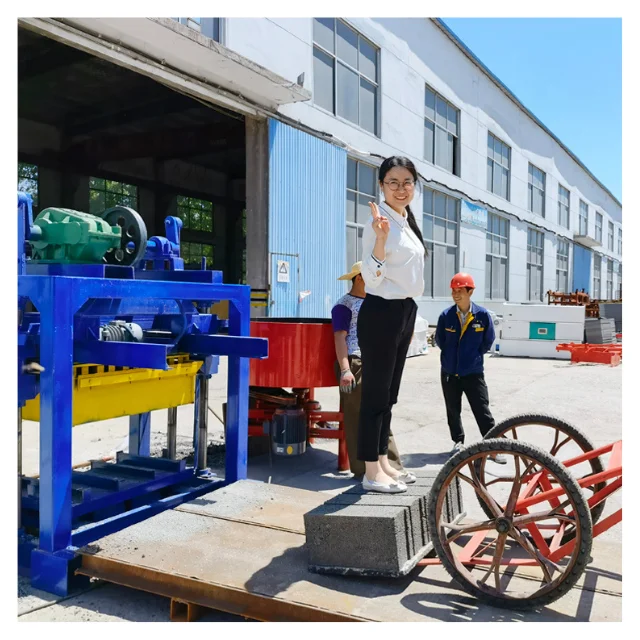
Single-tier focus, matched configuration — Every QTJ4-40 shipped leaves our floor with its electrical panel, vibration force, and pallet spec confirmed against your site conditions, not pulled from a catalogue default.
Technical Specifications
| Parameter |
Value |
| Model |
QTJ4-40 |
| Product Type |
Semi-Automatic Concrete Block Making Machine |
| Rated Power |
10.4 kW |
| Molding Cycle |
40 s |
| Output Capacity |
2,800 pcs/day (basis: 400×200×200 mm hollow block, 4 pcs/mould) |
| Theoretical Hourly Output |
360 pcs/h (basis: 400×200×200 mm hollow block) |
| Raw Materials |
Concrete, sand, cement, fly ash, lime, gypsum |
| Net Weight |
1 T |
| Overall Dimensions (L×W×H) |
1350 × 1460 × 1800 mm |
| Pallet Size |
850 × 450 mm |
| Voltage |
According to buyer’s local voltage (basis to be confirmed) |
| Vibration System |
Bed mould vertical vibration + upper mould compression vibration |
| Mould Actuation |
Top die push-and-pull with automatic scraper |
| Automation Level |
Semi-automatic |
Application Suitability
| Application |
Material or Output |
| Small to medium block production plants |
Hollow and solid blocks from locally sourced sand, cement, fly ash, and aggregate |
| On-site block production for contractors |
Standard hollow blocks and solid bricks produced directly at the construction project |
| Supplementary format production |
Secondary block sizes handled on a dedicated machine while the main line runs primary formats |
| Start-up block plants |
Entry-level semi-automatic production with limited initial investment before scaling to a full automatic line |
Why the Voltage Question Must Come Before the Price
A machine wired for the wrong frequency will not start a single production shift, no matter how competitive the quotation was.
I spent years on the buyer side before moving to equipment supply, and I watched a QTJ4-40 sit idle on a Middle East job site because the motors were wound for 50 Hz while the local grid ran at 60 Hz. The contactors burned out on the first test run, and the site manager waited nearly three weeks for replacement components to arrive by air freight. Voltage and frequency confirmation is the very first checkpoint in our order process now, because no amount of on-site troubleshooting fixes a fundamental electrical mismatch [NEED_CITE: voltage and frequency standards by export market].

Where the QTJ4-40 Sits in the Shiyue Machine Range
The Shiyue block machine lineup spans mobile egg-laying units at one end and high-capacity fully automatic lines at the other. The QTJ4-40 occupies the semi-automatic tier, meaning the press cycle is automated but pallet handling between the press, curing area, and return conveyor still relies on manual labor or basic mechanical assist. Buyers evaluating this semi-automatic concrete block making machine for sale are typically weighing whether their daily volume justifies the step up to a fully automatic pallet return system, or whether the lower capital outlay of semi-automatic operation better fits a first plant.
Deciding Between Semi-Automatic and the Next Tier Up
Choosing the right automation level depends on your shift pattern, local labor cost, and target daily volume. A semi-automatic configuration keeps the machine investment contained and still delivers consistent block density through the dual vibration system, but it requires at least one operator dedicated to pallet transfer during every shift. When daily demand grows beyond what a single QTJ4-40 can produce within a standard shift, the logical step is adding a second unit or moving to an automatic stacking and cubing line. We help buyers model this decision against their actual block format and local curing space before committing to a configuration [NEED_CITE: typical block plant staffing requirements by automation level].
How Vibration Force and Mould Design Shape Block Density
The QTJ4-40 uses a dual vibration approach: vertical vibration from the bed mould compacts the concrete mix upward, while compression vibration from the upper mould drives density from the top surface downward. This combination matters most when producing hollow blocks with thin shell walls, where uniform density prevents cracking during demoulding and early curing. The 850 × 450 mm pallet size determines the maximum mould footprint, so every block format — from 400×200×200 mm hollow blocks to 225×112.5×60 mm solid bricks — must be designed within that envelope. The 40-second molding cycle gives the vibration system enough dwell time to consolidate mixes with higher fly ash or lime content, which tend to be stiffer and slower to compact than pure sand-cement blends.
The Hidden Cost of Skipping Pallet and Curing Area Planning
A buyer who selects a pallet size without checking their existing curing racks and forklift dimensions will face daily handling bottlenecks that no machine specification can solve. Pallets that do not match the forklift tine spacing require custom adapters or, worse, manual repositioning of every wet block stack. Curing areas designed for a different pallet size waste floor space and force operators to restack blocks before they have reached handling strength, increasing breakage rates noticeably [NEED_CITE: concrete block curing practices and pallet handling standards].
Why Buyers Source This Machine Range Through Shiyue
Block machinery is our single focus, so the QTJ4-40 press, its moulds, pallets, and handling accessories are specified as one matched system rather than assembled from separate vendors. We configure every machine against the buyer’s actual mix design and local aggregate, not a generic catalogue setting. Custom mould design is available to buyer drawings, so the formats your market actually sells are the formats the machine produces from day one. Every unit undergoes a factory test run with the specified mould installed before crating. Installation guidance, operator training, and ongoing mould and wear parts support are included as standard practice, not as optional extras.
Documentation & Verification
- Line layout drawing showing QTJ4-40 footprint and pallet flow path
- Capacity calculation sheet stating block format assumed for each output figure
- Mould drawing and format list matching the quotation
- Electrical schematic with confirmed voltage and frequency
- Pallet specification sheet matched to curing area plan
- Factory test record with the buyer’s selected mould installed
Installation, Commissioning & Support
- Foundation pad must support the 1 T net weight and dynamic vibration loads of the 10.4 kW drive system
- Dedicated electrical circuit required, rated for the confirmed local voltage and frequency
- Machine arrives assembled; only the upper mould frame and hopper require on-site mounting
- First-run commissioning includes vibration timing adjustment matched to the buyer’s mix design
- Operator training covers the 40-second cycle sequence, mould change procedure, and daily inspection points
- Wear parts list and recommended spare mould inventory provided at handover
What to Include in Your Inquiry
To size a QTJ4-40 correctly for your project, we need your target block format and dimensions, your planned daily output volume, and the raw materials available locally including aggregate type and gradation. Your site’s voltage and frequency must be confirmed so the motor and control panel are wound correctly before production begins. If you have an existing curing area or forklift fleet, sharing the pallet dimensions and rack spacing you already use helps us match the pallet specification to your current handling infrastructure.
Frequently Asked Questions
Q: How is the output capacity of the QTJ4-40 calculated per block format?
A: Output is tied to specific mould configurations. With a 400×200×200 mm hollow block mould producing 4 pieces per cycle at a 40-second molding cycle, the theoretical daily capacity is 2,800 pieces based on continuous operation. Switching to a 225×112.5×60 mm solid brick mould at 9 pieces per cycle raises the theoretical figure to 6,400 pieces per day. Actual output depends on operator pace, pallet handling speed, and raw material feed continuity.
Q: Where does the QTJ4-40 fit compared to mobile or fully automatic Shiyue machines?
A: The QTJ4-40 occupies the semi-automatic tier. It offers higher and more consistent output than a mobile egg-laying machine because blocks are formed on pallets in a fixed station, but it requires manual pallet transfer unlike a fully automatic line with integrated stacking and cubing. Buyers choosing this tier typically value lower initial investment while still achieving uniform block density through the dual vibration system.
Q: What voltage and frequency options are available, and how is this confirmed?
A: The motor and control panel are configured to match the buyer’s local grid supply, whether that is 220V, 380V, 415V, or 440V at either 50 Hz or 60 Hz. Voltage and frequency must be confirmed in writing before production starts. We verify these parameters during the inquiry stage and print them on the electrical schematic included with the machine documentation.
Q: What pallet size does the QTJ4-40 use, and how should the curing area be planned?
A: The machine uses 850 × 450 mm pallets. Your curing area rack spacing, forklift tine width, and pallet return path should all be planned around this dimension before the machine arrives. Sharing your existing handling equipment specifications during the inquiry stage allows us to confirm pallet material and thickness recommendations that match your site conditions.
Q: What minimum investment and plant footprint does a QTJ4-40 line require?
A: The machine itself measures 1350 × 1460 × 1800 mm, but the total line footprint must include raw material storage, a mixing station, pallet return space, and a curing area sized for your daily output. Semi-automatic operation keeps the equipment investment lower than a full automatic line, though buyers should budget for pallet inventory, a concrete mixer, and basic material handling equipment alongside the press.

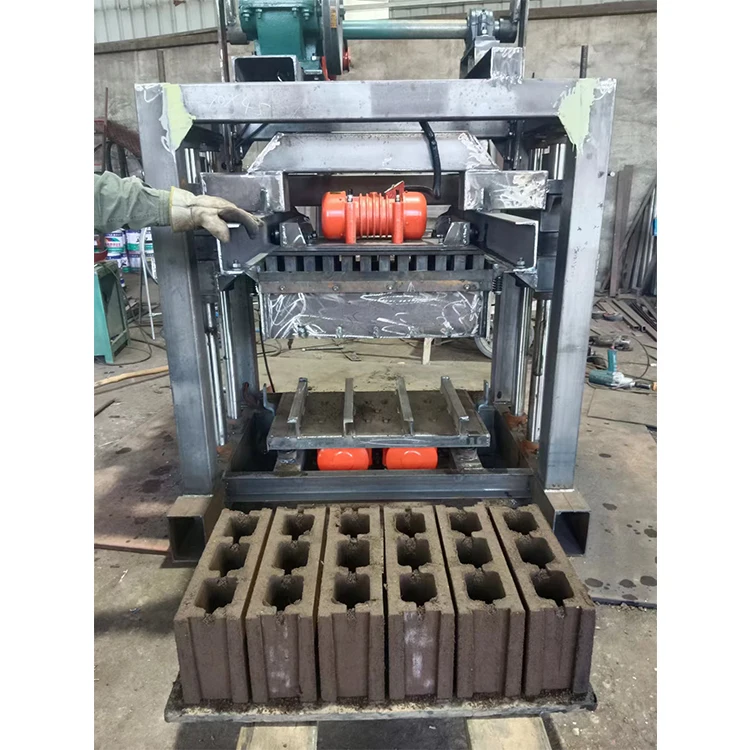
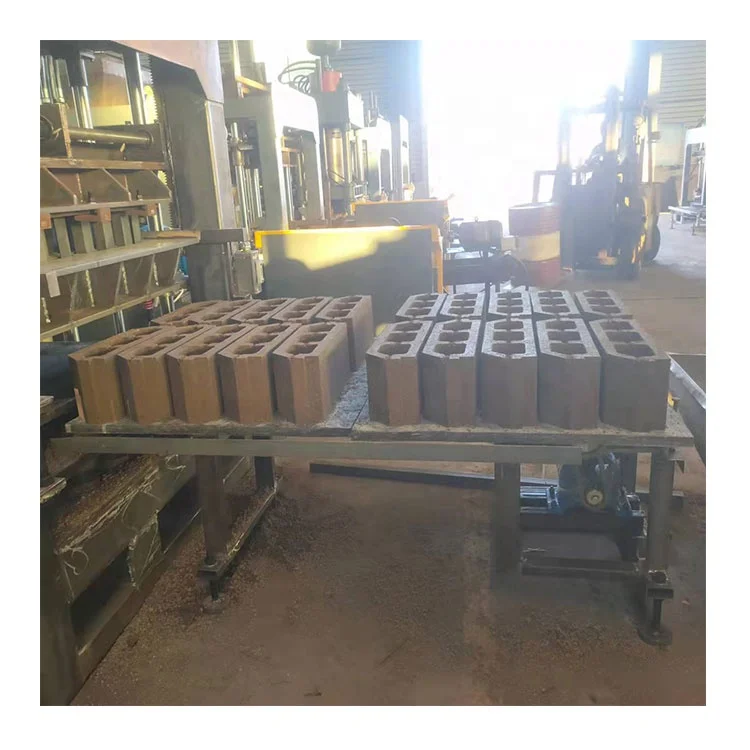 High quality block machine