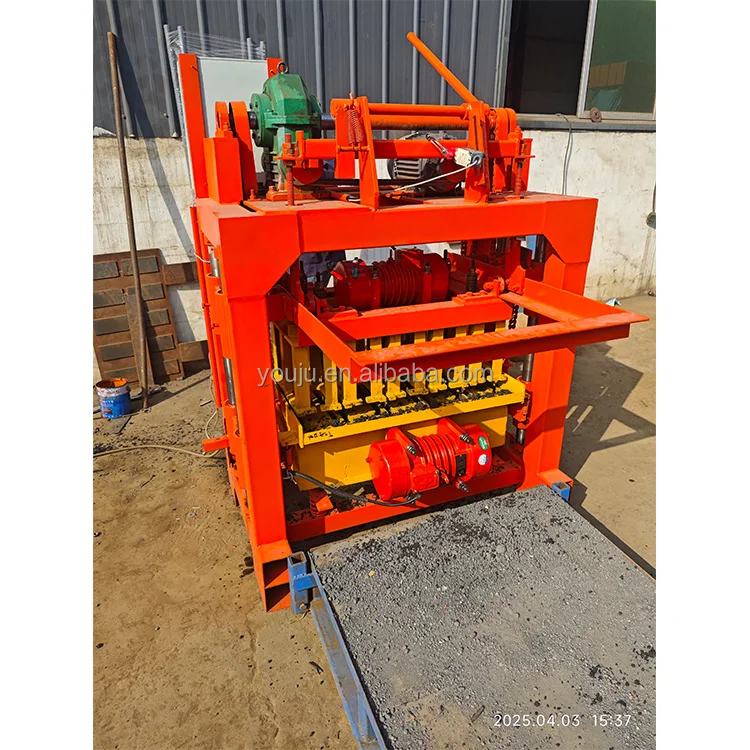
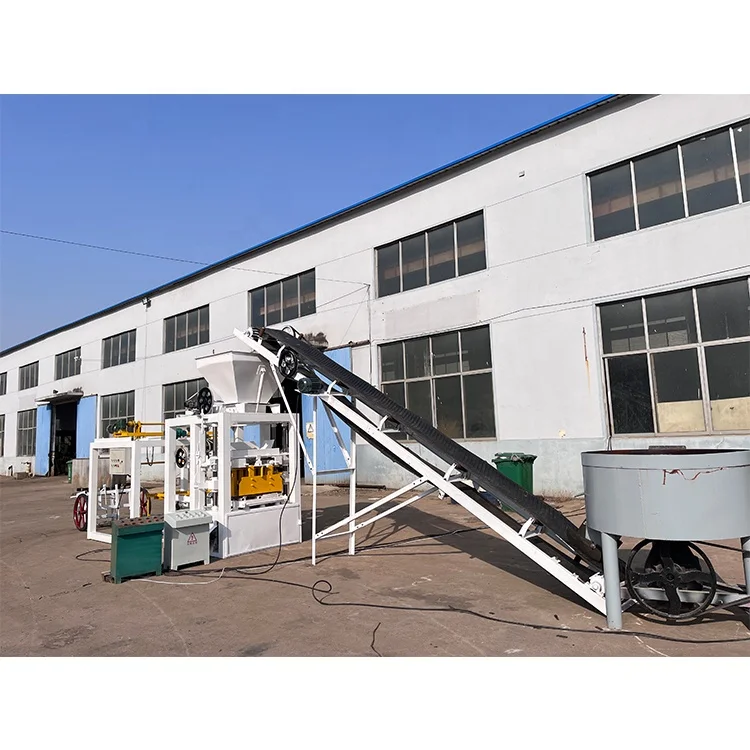
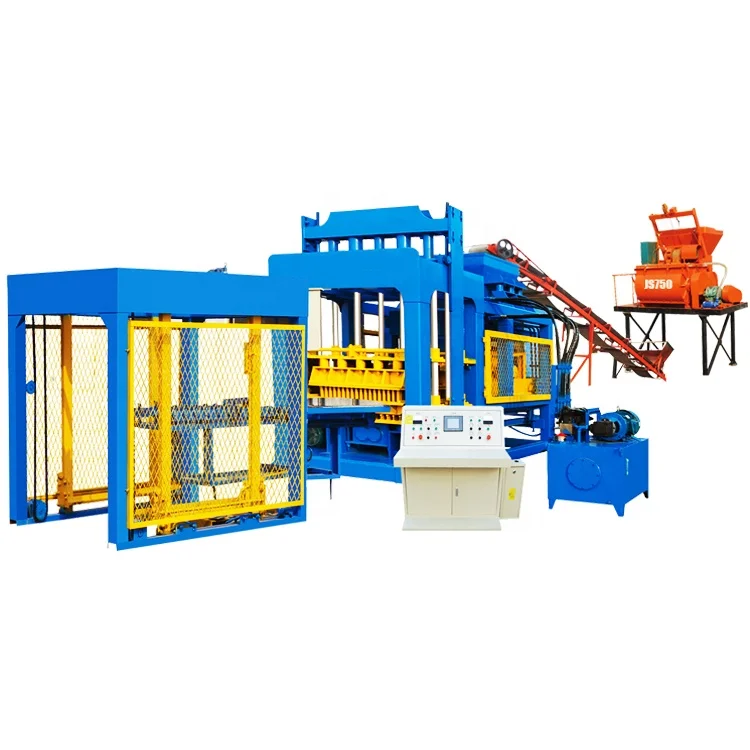
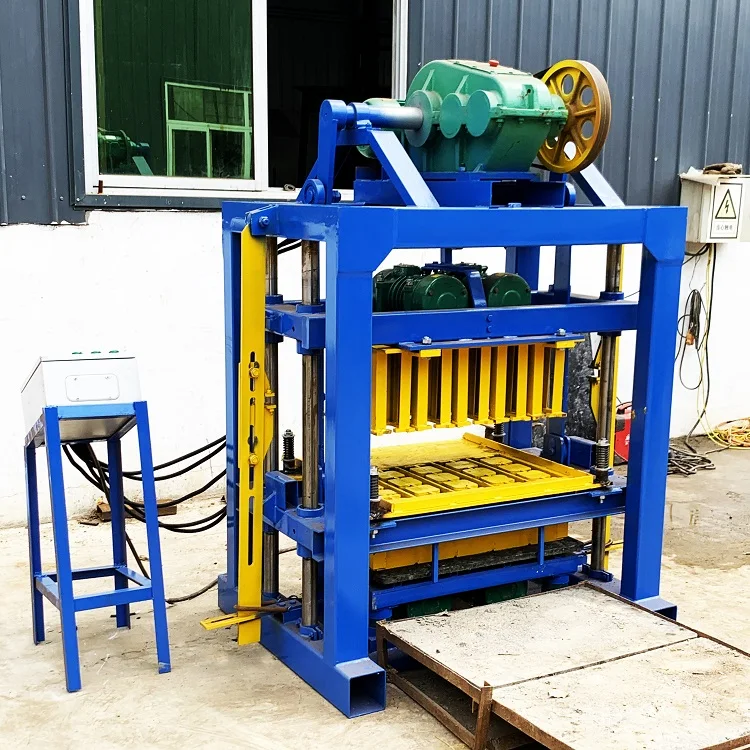
Complete Machine Range Focus — the QT7-15 bridges Shiyue’s semi-automatic workshop tier and high-capacity automatic lines, letting buyers place themselves accurately on the output spectrum before committing to a plant footprint.
Technical Specifications
| Parameter |
Value |
| Model |
QT7-15 |
| Product Type |
Stationary Concrete Block Making Machine |
| Pallet Size |
1150 × 700 mm |
| Molding Cycle |
15–20 s |
| Overall Power |
45 kW |
| Vibration Force |
100 kN |
| Vibration Frequency |
0–60 Hz (adjustable) |
| Vibration Form |
Platform Vibration |
| Demolding Method |
Hydraulic |
| Total Mass |
8 T |
| Control System |
PLC with touch screen interface |
| Output – Hollow Block 400×200×200 mm |
1260–1680 pcs/h; 10080–13440 pcs/8 hr |
| Output – Hollow Block 400×150×200 mm |
1440–1920 pcs/h; 11520–15360 pcs/8 hr |
| Output – Rectangular Paver 200×100×60 mm |
3888–4860 pcs/h (basis: 20–25 s cycle, 27 pcs/mould — source value, verify against manufacturer catalog) |
| Mould Format Compatibility |
Hollow block, rectangular paver / interlocking brick (mould changeable) |
| Automation Level |
Automatic (PLC controlled, pallet feed, hydraulic demolding) |
| Components Included |
Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
| Voltage & Frequency |
Configurable to buyer’s site supply (to be confirmed before production) |
| Certification |
CE (where applicable — verify for specific order) |
Application Suitability
| Application |
Material or Output |
| Hollow concrete block production |
Crushed stone, sand, cement, fly ash aggregates — 400×200×200 mm and 400×150×200 mm formats |
| Rectangular paving brick and interlocking paver production |
Fine aggregate and cement mixes — 200×100×60 mm format via mould change |
| Stationary block plant with multi-format requirement |
One press running hollow blocks on main shift, pavers on secondary shift |
| Contractor on-site block production |
Local aggregate and cement, formats matched to regional building codes |
What "Pieces per Hour" Leaves Out About the QT7-15 Stationary Block Making Machine Full Range
Capacity numbers mean nothing unless the block format, mould cavity count, and cycle time are stated together.
I have watched buyers sign contracts based on a single headline figure, only to discover the machine was rated on a small solid brick while they needed 200 mm hollow blocks. The QT7-15 stationary block making machine full range documentation on this page lists output per specific format and mould so you can compare against your actual product plan. When a supplier quotes cycles per hour without naming the block size, the real daily tonnage often disappoints [NEED_CITE: common mismatch between quoted and realized block plant output].

Where the QT7-15 Sits in the Shiyue Output Tier Ladder
The QT7-15 occupies the mid-to-high automatic tier in the Shiyue stationary block machine lineup. Below it, semi-automatic models such as the QT4-series serve smaller workshops that accept manual pallet handling. Above it, the QT10-series and larger automatic lines push pallet size and vibration force higher for plants targeting continuous high-volume output. Understanding this tier position helps buyers decide whether to invest in the QT7-15 or step up to the next capacity bracket before signing.
Automation Level and Future Upgrade Path
This model ships with PLC-controlled automatic pallet feeding and hydraulic demolding as standard. Buyers who want to keep initial investment lower can configure the line with manual stacking at the discharge end, then add automatic stacker and cubing modules later. The touch screen interface records fault codes, so remote troubleshooting is possible once the plant is networked. Planning the upgrade path at quotation stage prevents costly PLC cabinet swaps down the road [NEED_CITE: PLC upgrade compatibility in stationary block lines].
Reading the Specs That Actually Shape Daily Output
Platform vibration at 100 kN with adjustable frequency from 0 to 60 Hz is the core forming force of the QT7-15 stationary block making machine full range offering. Higher frequency suits fine sand mixes for pavers, while lower frequency with longer dwell works better for coarse aggregate hollow blocks. The 1150 × 700 mm pallet size dictates how many blocks fit per cycle and determines the curing rack dimensions you must build; mismatch the pallet to your existing forklift and you will double handling labor. Mould change is a hydraulic clamp design, allowing a format swap within a single shift — a practical advantage for plants alternating between hollow blocks and interlocking pavers. Total installed power of 45 kW means a dedicated circuit with appropriate breaker rating; confirm voltage and frequency before the machine leaves the factory, because rewiring a PLC cabinet on site is neither cheap nor fast.
The Hidden Cost of Skipping Configuration Checks
Ordering a QT7-15 without confirming the buyer’s actual aggregate gradation leads to weak blocks or extended cycle times. I have seen a Middle East project stall for weeks because the local stone dust contained high clay, and the default vibration settings could not compact it properly. Voltage surprises are equally painful: a 60 Hz motor on a 50 Hz supply runs slower and hotter, shortening bearing life. Skipping a written mould drawing review means the first container arrives with a paver mould that does not match the local kerbstone standard, forcing an air-freight replacement [NEED_CITE: impact of aggregate clay content on block cycle time].
Why Buyers Source This Tier From Shiyue
Block machinery is our single focus, so the QT7-15 press, mould, pallet, and handling stations are specified as one matched set rather than assembled from separate suppliers. We configure vibration force and frequency against the buyer’s trial block results, not a catalogue default. Moulds are designed for the formats that actually sell in the buyer’s market, including custom drawings when standard cavities do not fit. Documentation covers line layout, capacity calculation per format, and a factory test record on the buyer’s own mix. Operator training is included during commissioning so the crew can run independent shifts from day one.
Documentation & Verification
- Line layout drawing stating pallet flow and curing rack spacing for the QT7-15 footprint
- Capacity calculation sheet listing output per hollow block and paver format
- Mould drawing and format list with cavity count and dimensional tolerances
- Factory test record on buyer’s aggregate sample before dispatch
- Voltage, frequency, and PLC language confirmation sheet signed before production
- CE declaration documentation where applicable to the destination market
Installation, Commissioning & Support
- Foundation plan matched to the 8 T mass and vibration isolation pads of the QT7-15
- Dedicated 45 kW circuit with breaker rating confirmed to local voltage and frequency
- Machine shipped in dismantled modules for container loading, reassembled on site
- First-run parameter tuning of vibration frequency and hydraulic pressure using buyer’s mix
- Operator training on PLC touch screen fault diagnosis and mould change procedure
- Wear parts and mould cavity list with reorder part numbers provided at handover
Next Steps Before Requesting a Quotation
Send us your target block formats with dimensions, the daily output you need per format, and a sample of your local aggregate. Include the voltage and frequency at your site, the language you prefer on the PLC touch screen, and the curing area dimensions you have available. If you already own a mixer or conveyor, share those specs so the QT7-15 stationary block making machine full range proposal aligns the whole line.
Frequently Asked Questions
Q: How does QT7-15 capacity compare to adjacent models in the Shiyue stationary range?
A: The QT7-15 sits between smaller semi-automatic workshop machines and higher-capacity QT10-series automatic lines. Output is rated per block format — for example, 1260–1680 hollow blocks 400×200×200 mm per hour. Buyers needing noticeably larger daily tonnage step up to the next tier where pallet size and vibration force increase accordingly.
Q: What block formats can the QT7-15 produce and what is the realistic cycle time?
A: Hollow blocks in 400×200×200 mm and 400×150×200 mm, plus rectangular pavers and interlocking bricks at 200×100×60 mm are standard. Molding cycle ranges from 15 to 20 seconds for hollow blocks and 20 to 25 seconds for pavers. Actual cycle depends on mix design and target block density.
Q: What plant footprint and auxiliary equipment does the QT7-15 require?
A: The press, pallet feed, storage hopper, and conveyor need a covered bay with headroom for the hydraulic unit. A separate curing area sized around the 1150 × 700 mm pallet is essential. Mixer capacity should match the 45 kW press output to avoid the press waiting between cycles.
Q: Can I start with manual stacking and upgrade the QT7-15 later?
A: Yes. The PLC architecture allows adding automatic stacker and cubing modules after initial installation. Confirm the upgrade path at quotation stage so the control cabinet reserves the necessary I/O channels and the hydraulic circuit includes spare valve stations for future actuators.
Q: What investment difference exists between the QT7-15 and the next tier up?
A: The step up involves a larger pallet, higher vibration force, and greater installed power, which increases both machine cost and plant footprint. Buyers whose daily target exceeds the QT7-15 format-specific output find the higher tier justified; those below that threshold recover investment faster on the QT7-15.

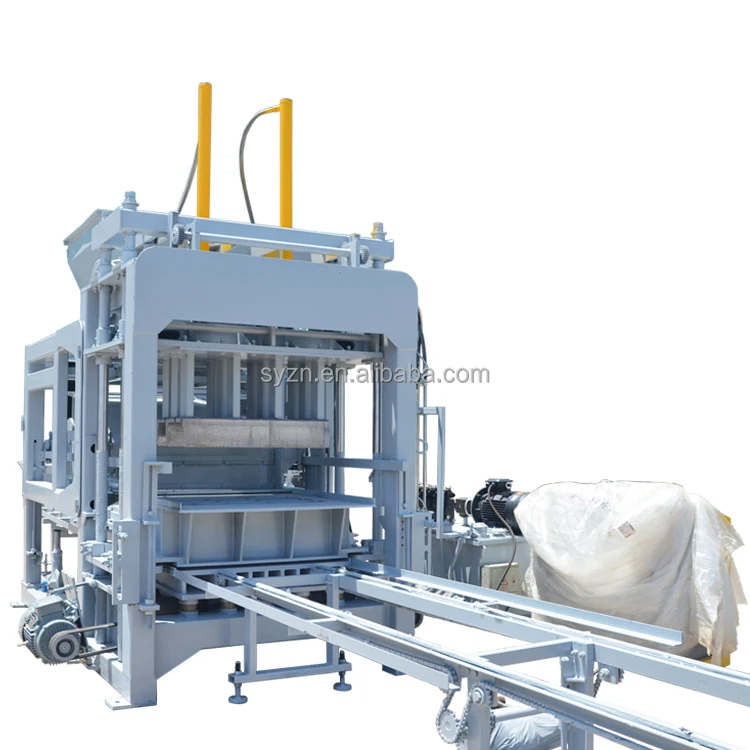
 Stationary block machine