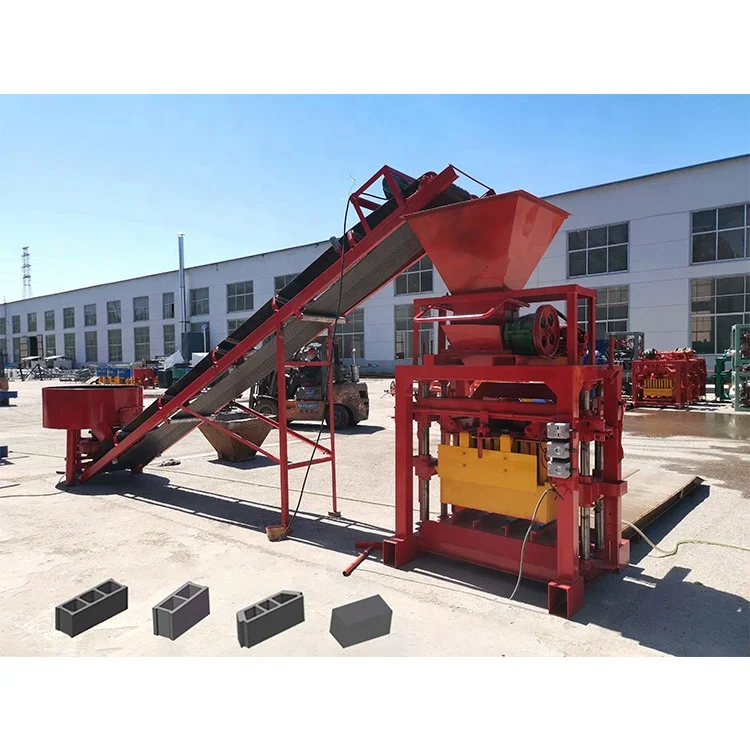
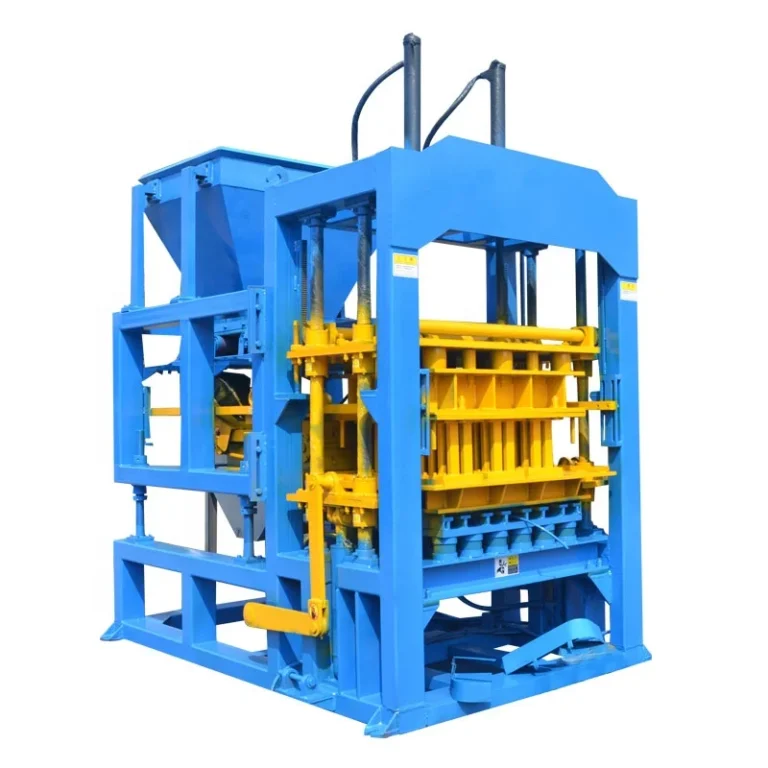
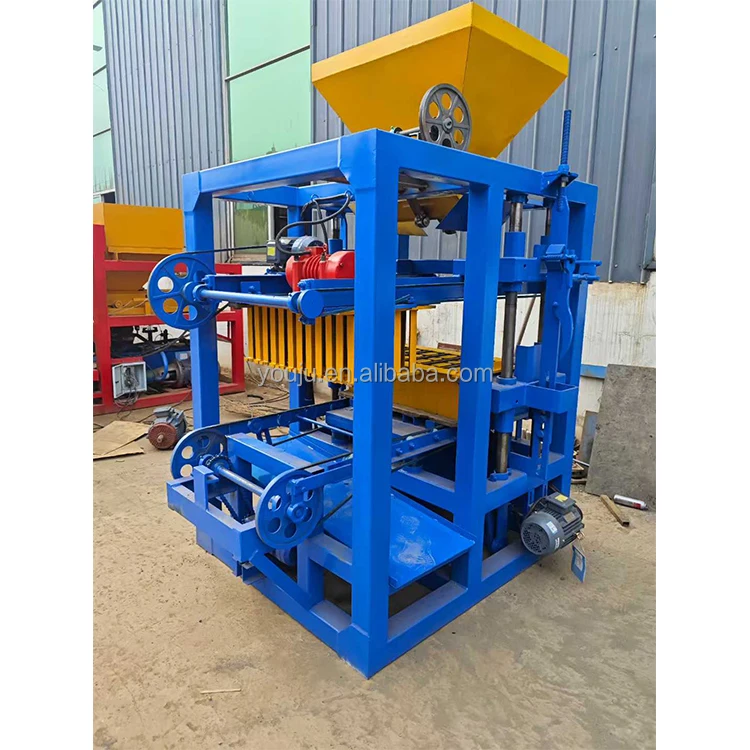
Integrated System Specification — The QT8-15 is positioned and quoted as a complete press, pallet, mould, and handling package rather than a standalone unit, ensuring every downstream station matches the cycle rhythm the buyer actually needs.
Technical Specifications
| Parameter |
Value |
| Model |
QT8-15 |
| Product Type |
Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
8300 × 1860 × 3000 mm |
| Rated Pressure |
21 MPa |
| Main Vibration Form |
Platform Vibration |
| Vibration Frequency |
2800 ~ 4500 r/min |
| Vibration Force |
60 kN |
| Pallet Size |
950 × 900 mm |
| Molding Cycle |
15–25 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power |
55.5 kW |
| Total Mass |
9 T |
| Demolding Method |
Hydraulic |
| General Water Consumption |
12 T/Day |
| Factory Area |
600 m² |
| Control System |
PLC with human-machine interface (HMI) |
| Automation Level |
Fully automatic |
| Voltage & Frequency |
Configurable to destination site (to be confirmed before production) |
| Applied Products |
Hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material |
Crushed stone, sand, cement, fly ash, gravel, slag, dust |
Application Suitability
| Application |
Material or Output |
| Hollow block production for residential and commercial walls |
Crushed stone, sand, cement, and fly ash blends |
| Solid block manufacturing for load-bearing structures |
Gravel, sand, and cement mixes with slag additions |
| Interlocking paver and colored paver runs for landscaping |
Fine aggregates with pigment dosing on 950×900 mm pallets |
| Kerbstone and curb production for road infrastructure |
High-strength concrete mixes compacted under 21 MPa hydraulic pressure |
| Porous and permeable block runs for drainage systems |
Open-graded aggregate blends requiring adjusted vibration profiles |
What "15–25 Second Cycle" Actually Means for Your Output
A cycle time is only meaningful when the block format, mix design, and pallet size behind it are named.
Catalogue sheets often quote a single molding cycle for the QT8-15 automatic concrete block making machine without saying which block format was assumed. A 15-second cycle on a thin paver is a different story from a 25-second cycle on a 200 mm hollow block, and the daily output gap between the two can be enormous. I once spent a week re-tuning vibration parameters for a buyer whose local sand carried high clay content — the cycle time on paper stayed the same, but real throughput dropped until the mix and frequency were corrected [NEED_CITE: effect of aggregate clay content on concrete block compaction]. Always ask for a per-format capacity table before committing to a purchase order.

Where the QT8-15 Sits in a Stationary Block Plant Lineup
The QT8-15 occupies the mid-to-upper tier of stationary block machines, bridging the gap between workshop-scale semi-automatic presses and high-capacity fully automatic lines. Its 950×900 mm pallet platform and 55.5 kW total power draw place it in a range that suits medium-volume plants looking to produce multiple block formats on a single machine. Buyers stepping up from a smaller press will find the footprint familiar, while those comparing upward will see it as a cost-effective alternative to larger pallet formats that demand bigger curing yards.
How Automation Tier Shapes Your Crew and Floor Plan
A fully automatic configuration means the QT8-15 handles pallet feeding, vibration compaction, hydraulic demolding, and block ejection through its PLC-controlled sequence. The operator’s role shifts from manual pallet swapping to monitoring the HMI dialogue screen and intervening only when the system flags a deviation. This reduces the crew needed at the press itself, but it also means the curing rack handling and stacking stations downstream must be matched to the same automation level — otherwise, blocks pile up faster than they can be moved.
Reading the Specs That Matter Beyond the Brochure
The platform vibration system runs between 2800 and 4500 r/min, delivering 60 kN of vibration force. In practice, the operator adjusts frequency based on the aggregate grading and block thickness — coarser mixes with larger crushed stone typically need lower frequency and longer vibration to settle fully, while fine-sand paver mixes respond better at higher frequencies. The 21 MPa rated hydraulic pressure works together with vibration to compact the mix; if pressure is set too high relative to vibration, the block surface can crack during demolding. The 950×900 mm pallet size dictates the maximum block array per cycle and must align with the curing area rack spacing and the forklift tine width already on site [NEED_CITE: matching pallet dimensions to curing rack and forklift specifications].
The Cost of Skipping Configuration Checks Before Shipment
Buyers who confirm only the press model and leave voltage, frequency, and PLC language to chance often face a stalled commissioning. A QT8-15 automatic concrete block making machine wired for a voltage that does not match the local grid sits idle while transformers are sourced, and a control panel displaying in an unreadable language slows operator training to a crawl. Mould formats are another frequent gap — a buyer may pay for format flexibility but receive moulds for block types their local market does not buy, turning a quick changeover into an expensive shelf display.
Why Sourcing This Machine Here Reduces Line-Mismatch Risk
Block machinery is the single focus of this operation, so the QT8-15 is specified alongside its moulds, pallets, and handling equipment as one matched system rather than assembled from separate vendors. Machine configuration is set against the buyer’s actual mix design and local aggregate, not a default catalogue setting. Mould design covers the formats the buyer’s market sells, including custom drawings when standard options fall short. The automation level is selectable, allowing a buyer to start with semi-automatic pallet handling and move upward as production scales. Factory testing is performed with the buyer’s target block format on the pallet before dispatch, so the capacity figures shipped with the machine reflect a real production run, not a theoretical maximum [NEED_CITE: factory pre-delivery testing protocols for block making machinery].
Documentation & Verification
- Line layout drawing with per-format capacity calculation for your target block types
- Machine specification sheet confirming voltage, frequency, and PLC display language
- Mould drawing and format list showing all compatible moulds on the 950×900 mm pallet
- Hydraulic and electrical schematic for local maintenance team reference
- Factory test record on your specified mix and block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement schedule
Installation, Commissioning & Support
- Foundation plan sized to the 8300×1860 mm footprint with vibration isolation requirements noted
- Power supply circuit rated for the 55.5 kW total draw with dedicated breaker and correct voltage confirmed
- Machine shipped partially dismantled for container loading, with reassembly sequence documented
- First-run commissioning includes vibration frequency tuning to match your local aggregate grading
- Operator training covers HMI navigation, mould changeover procedure, and daily maintenance checkpoints
- Wear parts list with hydraulic seal and vibration motor brush replacement intervals specified
Getting an Accurate Configuration Proposal
To move from a general inquiry to a firm quotation, share the block formats your market actually sells, the daily volume you plan to run, and the raw materials available locally — including a sample of your aggregate if possible. Confirm your site voltage and frequency, the language your operators read, and the dimensions of your existing curing area so pallet and rack sizing can be verified. If you already have a mixer or batching plant upstream, provide its output rate so the feed system can be matched without bottlenecks.
Frequently Asked Questions
Q: How is the QT8-15’s output capacity calculated for each block format?
A: Output is derived from the molding cycle, pallet size, and number of cavities per mould. Because cycle time varies with block thickness and mix composition, we provide a per-format capacity table that names the specific block assumed — for example, a 400×200×200 mm hollow block at a given cycle — so you can compare figures honestly against your production target.
Q: What automation options exist within the QT8-15 range?
A: The QT8-15 automatic concrete block making machine is supplied as fully automatic with PLC-controlled pallet feeding and hydraulic demolding. Buyers can choose to add or defer automatic stacking and cubing stations, allowing a phased investment that starts with core press automation and expands as output volume grows.
Q: Can the voltage, frequency, and PLC language be set for my country?
A: Yes. Voltage and frequency are configured during production to match your local grid, and the PLC display language is confirmed before the control panel is assembled. This is documented in the specification sheet and verified during the factory test so there are no surprises at commissioning.
Q: What plant footprint does a QT8-15 line require?
A: The press itself occupies an 8300×1860 mm footprint, and the recommended factory area is approximately 600 m² to accommodate raw material storage, mixing, pallet return, and curing racks. Actual layout depends on your site dimensions, ceiling height, and whether stacking and cubing stations are included in the line.
Q: Which mould formats work on the 950×900 mm pallet, and can custom moulds be made?
A: The pallet supports hollow blocks, solid blocks, pavers, interlocking bricks, and kerbstones within the dimensional envelope. Custom moulds can be designed to buyer drawings when standard formats do not match local market demand, and mould change time is specified in the configuration proposal so you can plan format switches within a shift.

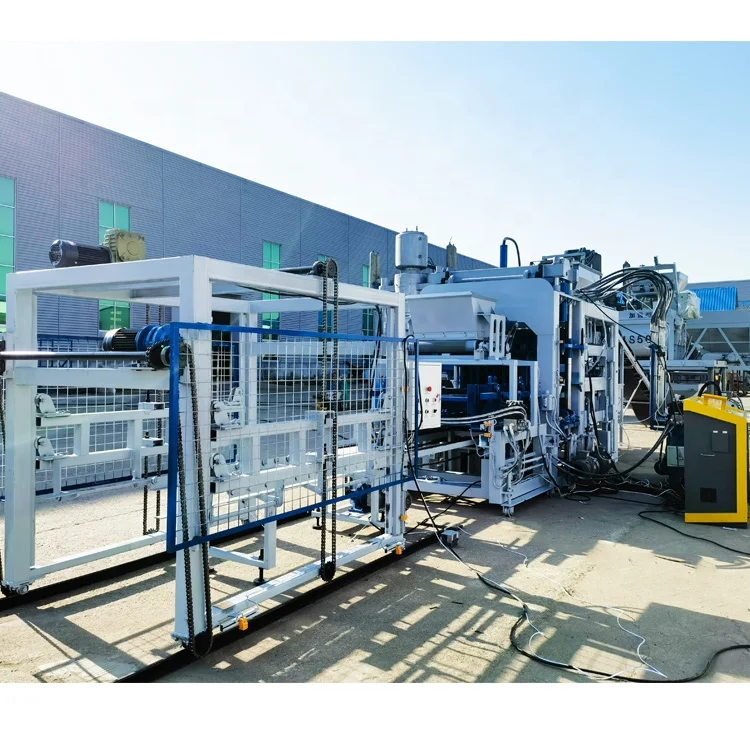
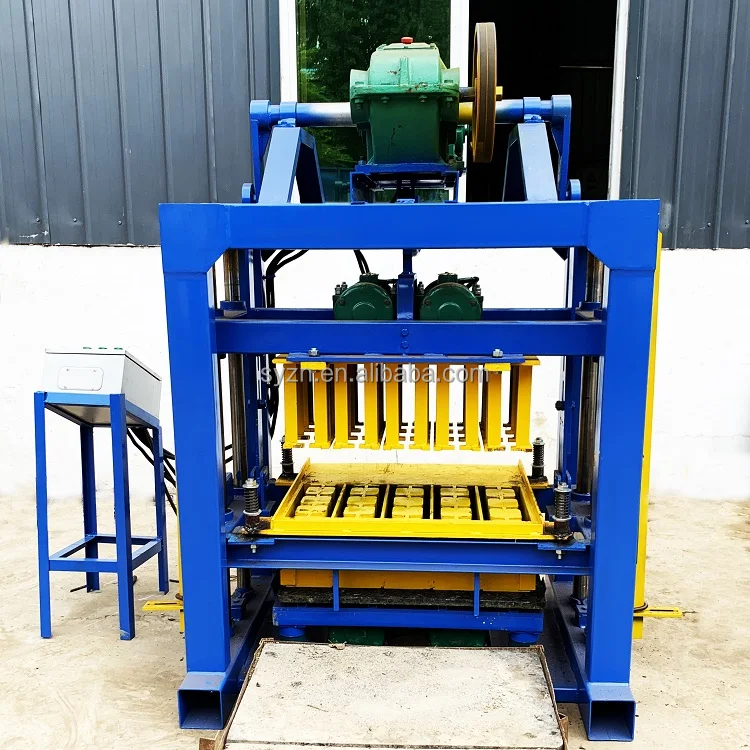 Stationary block machine