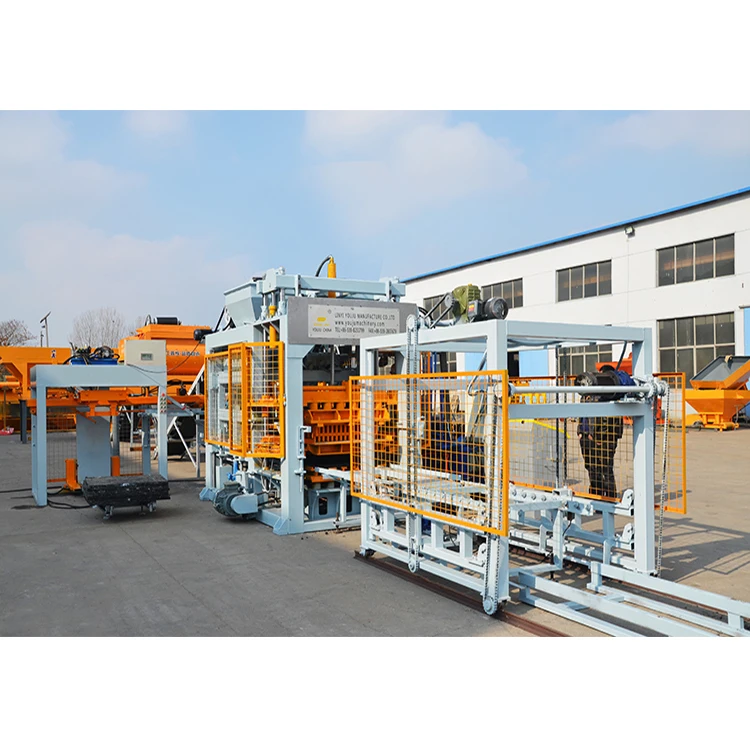
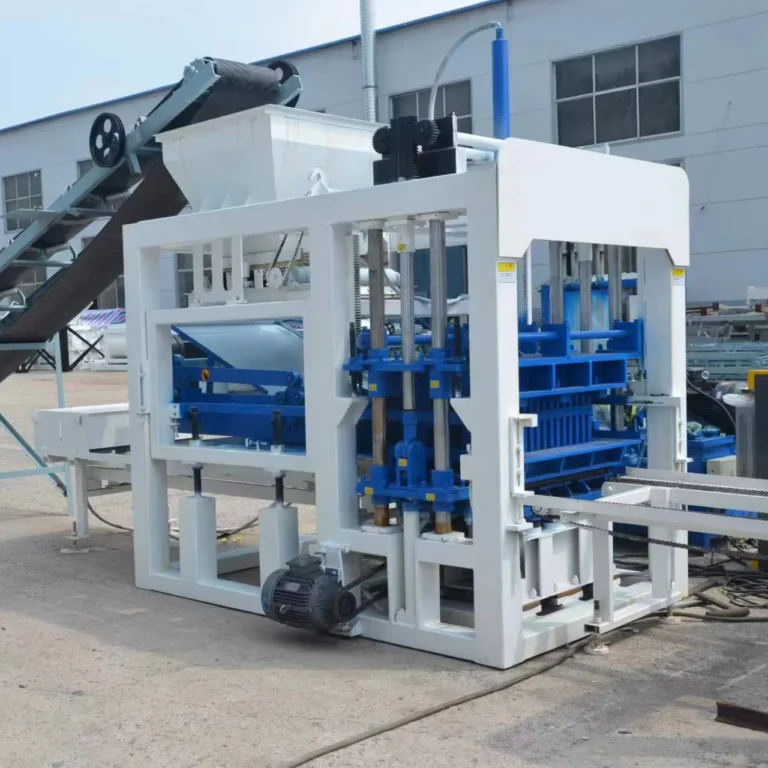
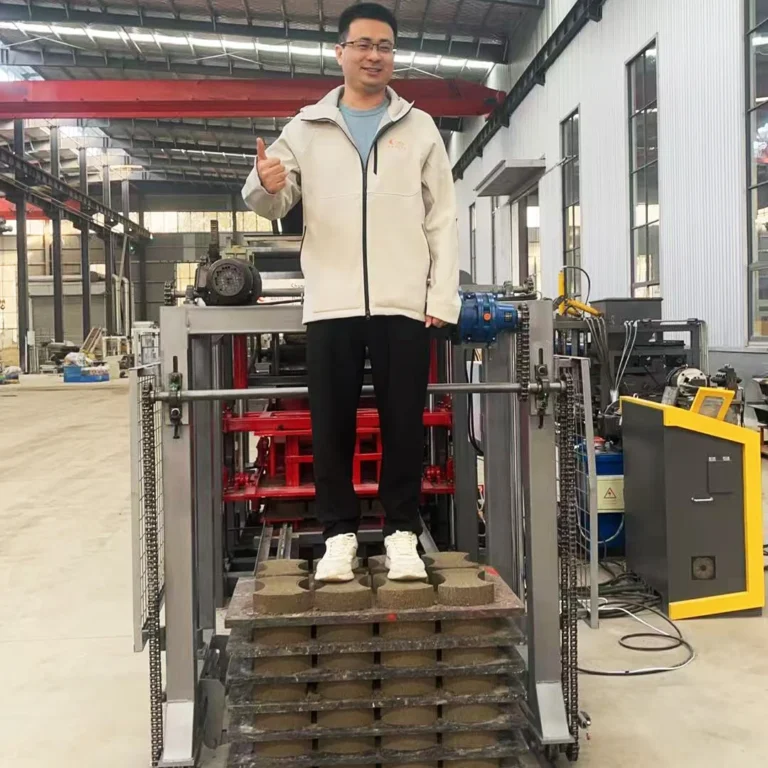
System-Matched Configuration — the QT4-18 is specified against your actual mix design, local aggregate and target block format rather than shipped as a catalogue default.
Technical Specifications
| Parameter |
Value |
| Model |
QT4-18 |
| Product Type |
Automatic Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
3900×1600×2300 mm |
| Molding Cycle |
15-25 s (basis not stated in source — confirm block format / material / thickness) |
| Vibration Force |
40-50 kN |
| Total Power |
24 kW |
| Mixer Model |
JQ350 |
| Pallet Size |
850×550×25 mm |
| Net Weight |
3 T |
| Control System |
PLC |
| Hydraulic Station |
Included |
| Output Capacity (Hollow block 400×200×200 mm) |
1200-1680 pcs/hr (based on 15-20 s cycle) |
| Output Capacity (Hollow block 400×150×200 mm) |
1800-2400 pcs/hr (based on 15-20 s cycle) |
| Output Capacity (Solid brick 240×115×53 mm) |
3240 pcs/hr (based on 15-20 s cycle) |
| Applied Products |
Paver, solid block, hollow block, curbstone |
| Raw Materials |
Crushed stones, sand, cement, dust, fly ash |
Application Suitability
| Application |
Material or Output |
| Hollow block production for load-bearing walls |
Crushed stone, sand, cement and fly ash blends |
| Solid brick manufacturing for partition walls |
Fine aggregate and cement mix designs |
| Paving block production for walkways and yards |
High-density aggregate with cement binder |
| Kerbstone forming for road and driveway edges |
Coarse aggregate with reinforced cement matrix |
What "1200 Pieces per Hour" Leaves Out When Sizing an Automatic Concrete Block Making Machine Manufacturer
Capacity figures are meaningless unless tied to a specific block format, cycle time and local material condition.
Many buyers discover after delivery that the quoted hourly output assumed a small solid brick on a short cycle, while their actual product is a large hollow block requiring longer vibration and curing. An automatic concrete block making machine manufacturer should always state which format drives the headline number. Without that link, daily planning and pallet inventory calculations fall apart on the first production run [NEED_CITE: capacity calculation assumptions in block machine quotations].

Where the QT4-18 Sits on the Output Tier Map
The QT4-18 occupies the mid-range position in the SHIYUE lineup, bridging entry-level semi-automatic machines and the high-capacity fully automatic lines. For a first-time plant owner, this tier delivers PLC-controlled consistency without the footprint and utility demands of a continuous-cure operation. Buyers replacing an older press often land here when their market volume has grown beyond manual pallet handling but does not yet justify a stacking and cubing system running around the clock.
Reading the Range Before Committing to a Tier
Choosing the right tier depends on daily output targets, available curing area and the labour model at your site. A smaller workshop with limited yard space may find the QT4-18’s pallet size and cycle rate well matched, while a high-volume paver contract could push you toward the upper tiers. Understanding this placement helps avoid over-investing in automation you cannot feed or under-investing in capacity you will outgrow within a season [NEED_CITE: block plant capacity planning and tier selection].
Vibration Force, Pallet Size and Cycle Time in Practice
The 40-50 kN vibration force, combined with hydraulic pressure, determines how densely the mix is compacted into the mould cavity. Higher density means the block can be stripped earlier without corner damage, shortening the molding cycle. The 850×550×25 mm pallet must match your existing curing racks and forklift tine spacing; a mismatch forces a second pallet purchase before the first block is made. Cycle time of 15-25 s varies with block height and mix stiffness, so the stated capacity ranges assume a confirmed format and material profile.
The Cost of Skipping the Format Conversation
When a machine arrives configured for a mix the buyer cannot source locally, the production line stalls while alternative aggregates are tested and approved. Pallet handling, stacking and curing left out of the quotation means blocks pile up at the press exit and must be moved by hand, erasing any automation advantage. Voltage, frequency and PLC display language unconfirmed before production lead to days of idle time and electrician call-outs after the container is opened [NEED_CITE: commissioning delays from unconfirmed electrical specifications].
Why Buyers Source This Tier Through SHIYUE
Block machinery is the single focus here, so the press, mould, pallet and handling equipment are specified as one matched system rather than assembled from separate suppliers. The configuration is set against the buyer’s actual mix design and target block format, not pulled from a catalogue default. Mould design covers the formats the buyer’s market actually sells, with custom drawings available. Automation level is selectable, allowing a start on semi-automatic operation with a defined upgrade path. Installation support includes operator training on the specific PLC interface shipped with the machine.
Documentation & Verification
- Line layout and capacity calculation stating which block format each output figure assumes
- Machine specification sheet confirming vibration force, power rating and pallet dimensions
- Mould drawing and format list for every block type included in the order
- Voltage, frequency and PLC display language confirmation signed before production begins
- Factory test record showing cycle times on your specified block format
Installation, Commissioning & Support
- Foundation pad sized to the 3900×1600 mm footprint with anchor bolt template provided before shipment
- Dedicated circuit rated for the 24 kW total power draw with voltage confirmed per destination country
- PLC display language and control labels set to operator preference before the crate is sealed
- Mould change procedure demonstrated on-site with the specific formats included in the order
- Wear parts list and hydraulic seal kit shipped with the machine for the first replacement cycle
- Operator training covers mix consistency checks tied to the 40-50 kN vibration force setting
What to Share With Your Inquiry
To size the QT4-18 correctly within the range, provide your target block formats, desired daily output and the raw materials available at your site. Include your local voltage and frequency, the PLC language your operators need, and the pallet size your curing area already uses. If you have an existing mixer or conveyor, note its model so the line can be configured around it.
Frequently Asked Questions
Q: How is output capacity calculated for each block format on this machine?
A: Output is derived from the molding cycle and the number of cavities in the mould for that format. The 1200-1680 pcs/hr figure assumes a 400×200×200 mm hollow block on a 15-20 second cycle. Different formats have different cavity counts and cycle lengths, so each product requires its own calculation.
Q: Where does this model sit compared to semi-automatic and high-capacity options?
A: The QT4-18 sits in the mid-tier, offering PLC-controlled automatic operation with hydraulic station and pallet feeder, positioned above manual and egg-laying machines but below the fully automatic stacking and cubing lines. It suits buyers who have outgrown manual handling but do not yet need round-the-clock capacity.
Q: Can I change the PLC language and voltage after the machine is built?
A: Voltage and frequency must be confirmed before production, as the motor, transformer and PLC power supply are sourced to match. The PLC display language is set during programming and can be adjusted, but confirming it before the control cabinet is sealed avoids rework after arrival.
Q: How long does a mould change take on this press?
A: Mould change time depends on the operator’s familiarity with the clamping system and whether the new mould is pre-positioned. The QT4-18 supports multiple formats on one frame, but realistic changeover should be planned into the shift schedule so format flexibility is not lost to downtime.

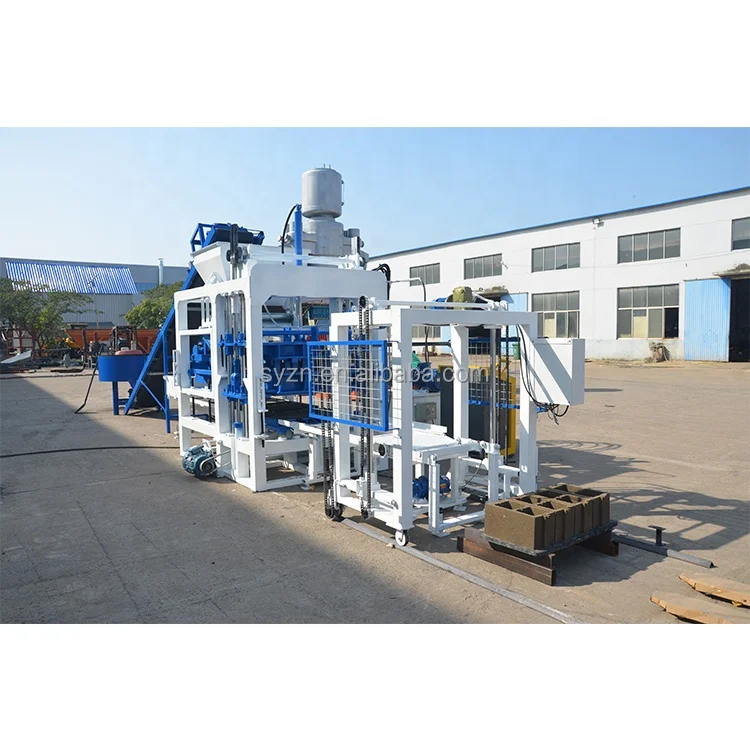
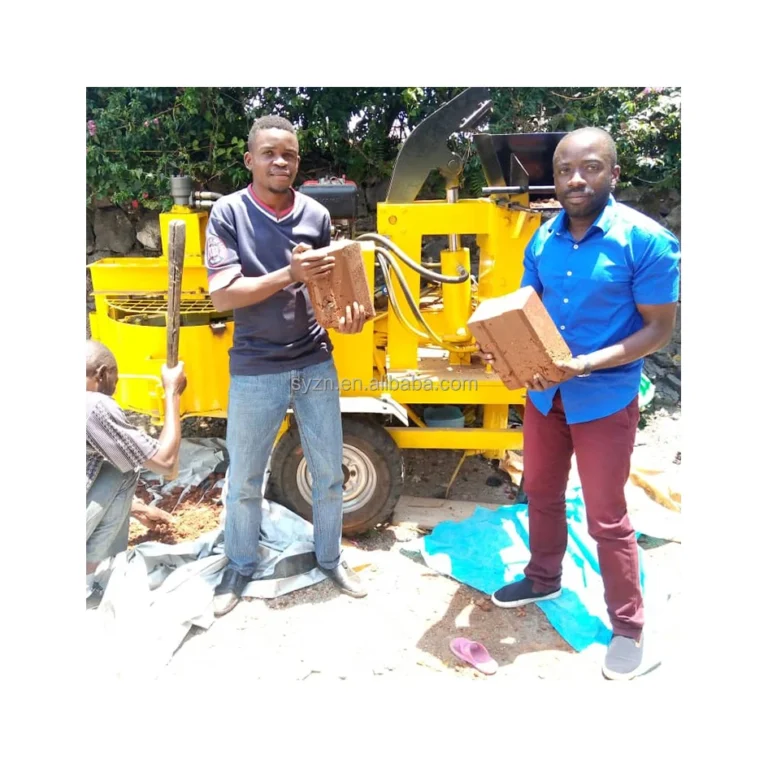 High quality block machine