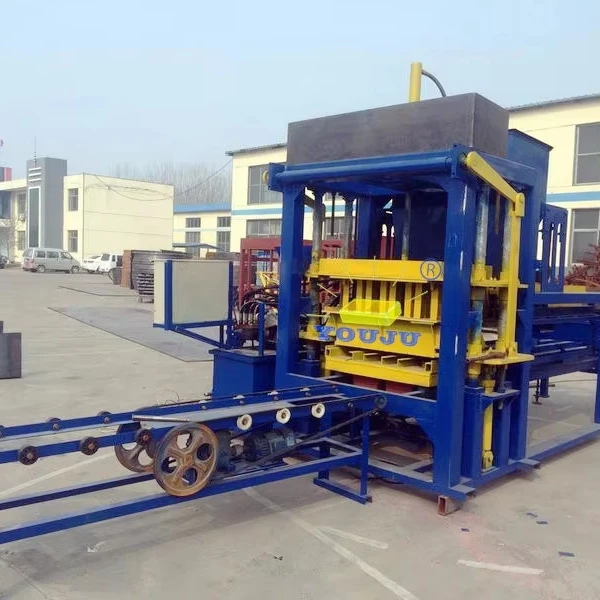
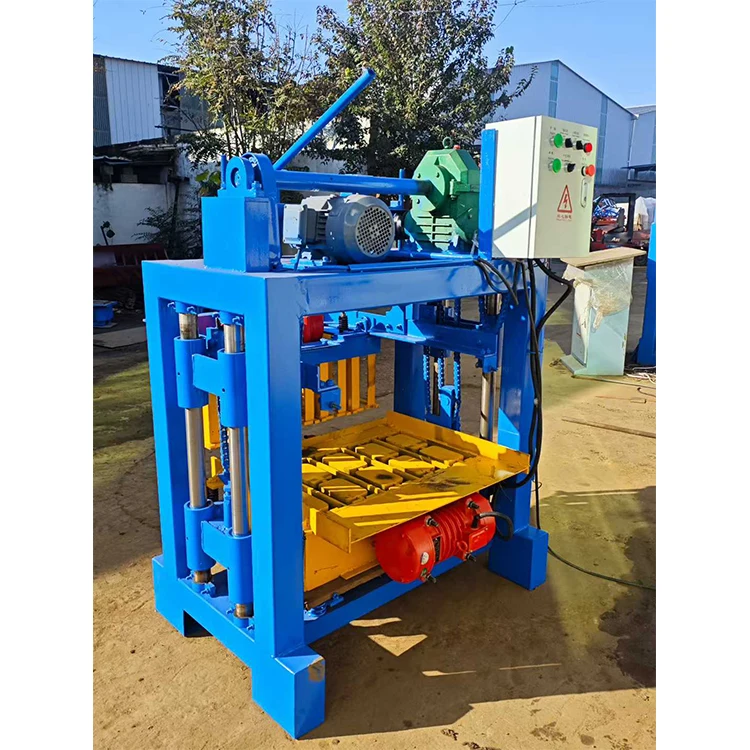
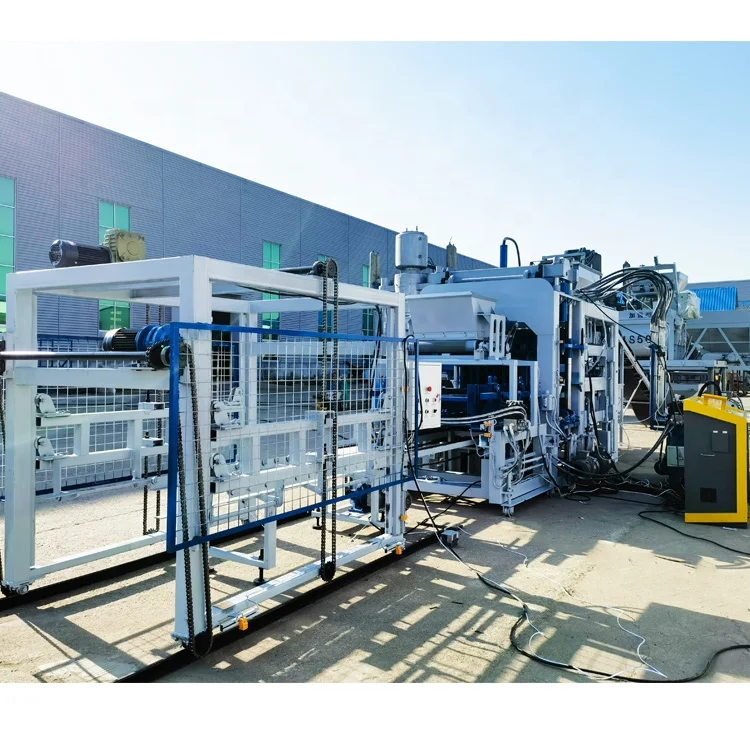
Matched System Sizing — QT12-15 press, mould, pallet and handling specified together against your actual block format, so the capacity figure you see is the capacity you run.
Technical Specifications
| Parameter |
Value |
| Model |
QT12-15 |
| Product Type |
Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
7500×2500×3020 mm |
| Total Mass |
12 T |
| Vibration Frequency |
0–60 Hz |
| Main Vibration Form |
Platform Vibration |
| Vibration Force |
100 kN |
| Overall Power |
53 kW (basis to be confirmed against manufacturer catalog) |
| Moulding Mode |
Automatic loading, vibration moulding |
| Pallet Size |
1220×900 mm |
| Molding Cycle |
15–20 s (basis not stated in source — confirm block format / material / thickness) |
| Demolding Method |
Hydraulic |
| General Water Consumption |
12 T/day |
| Factory Area Required |
1200 m² |
| Output — Hollow Bricks (400×200×200 mm) |
12 pcs/mould, 20–25 s cycle, 1728–2160 pcs/h |
| Output — Porous Bricks (240×115×90 mm) |
27 pcs/mould, 15–20 s cycle, 4860–6480 pcs/h |
| Output — Standard Bricks (240×115×53 mm) |
62 pcs/mould, 15–17 s cycle, 12700–14400 pcs/h |
| Control System |
PLC with human-machine interface dialogue system |
| Feeding System |
Semi-closed screen reticular rotational forced feeding unit |
| Stacking Method |
Automatic stacking |
Application Suitability
| Application |
Material or Output |
| High-volume hollow block production |
Crushed stone, sand, cement, fly ash aggregates for 400×200×200 mm cavity blocks |
| Standard solid brick runs |
Cement and fine aggregate blends for 240×115×53 mm bricks |
| Porous brick manufacturing |
Lightweight aggregate mixes for 240×115×90 mm perforated units |
| Paving and interlocking product lines |
Colored concrete and slag-based mixes for pavers and interlocking bricks |
| Kerbstone and curb units |
Dense aggregate concrete for heavy-duty street and road edging |
What "2160 Hollow Blocks per Hour" Actually Means on the QT12-15 Automatic Concrete Block Making Machine
The capacity number only holds if your mould, mix design, and cycle time align with the exact format tested at the factory.
Every quotation I have prepared starts with the same question: which block format are you actually selling? The QT12-15 automatic concrete block making machine delivers 1728–2160 hollow blocks per hour rated at 400×200×200 mm with a 20–25 second cycle, and 12700–14400 standard bricks per hour rated at 240×115×53 mm with a 15–17 second cycle. Switch the mould and the cycle changes, the feed behaviour changes, and the hourly output shifts with it. I once saw a buyer quote a tender based on standard brick capacity, then spend three years running mostly hollow blocks — the daily tonnage never matched the spreadsheet. [NEED_CITE: block format assumptions in capacity quotations]

Where the QT12-15 Sits in a Fixed-Plant Lineup
The QT12-15 occupies the high-output end of a stationary block machine range, designed for plants that run continuous shifts across multiple block formats. Buyers evaluating their first fixed plant or replacing an older press use this tier when daily volume requirements rule out semi-automatic or mobile options. The 1220×900 mm pallet size places it in a category that demands a curing yard and forklift fleet sized accordingly.
Matching Press, Pallet, and Handling as One System
A common mistake at this capacity level is treating the press as an isolated purchase. The 12-tonne machine mass and 53 kW overall power draw require a dedicated electrical circuit and a reinforced concrete foundation slab within the stated 1200 m² factory area. Automatic stacking and pallet feeding must keep pace with the 15–20 second molding cycle, otherwise the press sits idle waiting for the next pallet. When the entire line — raw material feeding, mixing, pallet circulation, stacking, and curing rack handling — is specified together, cycle time mismatches surface on paper instead of on the shop floor. [NEED_CITE: block production line integration and cycle time balancing]
Reading the Specs That Determine Your Daily Output
The 100 kN vibration force combined with hydraulic demolding determines how densely the concrete pack fills the mould cavity — too little force on a high-fines aggregate and blocks emerge with weak edges, too much on a lean mix and the surface cracks before curing even begins. The 0–60 Hz variable vibration frequency lets operators tune the platform vibration to different mould depths, which matters when switching between a 53 mm standard brick and a 200 mm hollow block on the same shift. The semi-closed screen reticular rotational forced feeding unit pushes material into deep cavity moulds more evenly than gravity-fed hoppers, reducing the weight variation between blocks in the same batch. Pallet size at 1220×900 mm dictates how many blocks travel per cycle and what racking system the curing area needs — ordering pallets that do not fit your existing forklift tines or curing racks creates a bottleneck no press upgrade can fix.
The Cost of Skipping the Format Conversation
When a buyer confirms the order before confirming the block format, the consequences surface during commissioning. A mould configured for a mix the local quarry cannot supply forces either a material sourcing change or a complete mould redesign, both adding weeks before the first saleable block leaves the yard. Pallets specified without checking the curing area dimensions mean blocks stack by hand until new racking arrives. Voltage and PLC display language left unconfirmed delay the entire start-up sequence while electricians rewire control panels and operators struggle with an interface in an unfamiliar language. [NEED_CITE: commissioning delays from unconfirmed electrical and control specifications]
Why Source This Machine Through a Single-System Supplier
Block machinery is the only product line here, which means the QT12-15 is not assembled from unrelated suppliers and then made to work on site. Configuration starts from the buyer’s actual mix design and local aggregate report, not a catalogue default, so vibration force and hydraulic pressure are matched to real material behaviour. Mould design covers the formats the buyer’s market actually purchases, including custom drawings when standard moulds do not fit. Automation level is selectable — a plant can start with semi-automatic pallet handling and move to full automatic stacking later without replacing the press. Installation includes operator training on the specific PLC interface and mould change procedures installed on that machine.
Documentation & Verification
- Line layout with capacity calculation stating the exact block format assumed for each output figure
- Machine specification sheet confirming voltage, frequency, and PLC display language before production starts
- Mould drawing and format list detailing changeover procedure for each product type
- Pallet specification matched to the buyer’s curing area dimensions and forklift capacity
- Factory test record run on the buyer’s target block format before dispatch
- Hydraulic and electrical schematic for on-site maintenance reference
Installation, Commissioning & Support
- Reinforced concrete foundation sized for the 12-tonne machine mass and 7500×2500 mm footprint
- Dedicated electrical circuit matching confirmed voltage and frequency for the 53 kW power draw
- Machine dismantled for container loading and reassembled on site with alignment verification
- First-run commissioning includes PLC parameter tuning for the buyer’s specific mix and block format
- Operator training covers mould changeover, feeding system adjustment, and fault diagnosis on the HMI
- Wear parts and mould inventory list provided with recommended reorder intervals
Preparing Your Inquiry
To size the QT12-15 correctly for your plant, share the block formats you intend to produce along with target daily output for each format. Include a local aggregate and cement supply report so vibration and feed settings can be calculated against real material properties. Confirm your site voltage, frequency, preferred PLC display language, and the curing yard area available for the 1220×900 mm pallet circulation system.
Frequently Asked Questions
Q: How is QT12-15 capacity calculated per block format, and what cycle time does each figure assume?
A: Each output figure is tied to a specific mould and cycle. Hollow blocks at 400×200×200 mm run 12 pieces per mould with a 20–25 second cycle yielding 1728–2160 pieces per hour. Standard bricks at 240×115×53 mm run 62 pieces per mould with a 15–17 second cycle. Switching formats changes both mould count and cycle length, so always confirm capacity against your primary product.
Q: Where does the QT12-15 sit in the full machine range compared to semi-automatic and mobile tiers?
A: The QT12-15 is positioned at the high-capacity end of the stationary range, intended for fixed plants running continuous production. Semi-automatic models serve smaller plants with lower investment, while mobile and egg-laying machines handle on-site production without a fixed facility. Buyers use this tier when daily volume requirements exceed what smaller presses can sustain.
Q: What plant footprint and pallet size do I need to plan for?
A: The stated factory area requirement is 1200 m², which covers the press, material handling, and pallet circulation but not the full curing yard. Pallet size is 1220×900 mm, so your curing racks, forklift tines, and stacking area must accommodate that dimension. Confirm these against your site plan before ordering.
Q: Which block formats can the QT12-15 produce, and how does mould change work?
A: The machine produces hollow blocks, solid blocks, porous bricks, paving blocks, interlocking bricks, and kerbstones through mould changes. The PLC-controlled system manages the molding cycle for each format, and mould drawings are provided so changeover procedures are documented. Mould change time depends on the system fitted and should be confirmed during configuration.
Q: What voltage, frequency, and PLC language options are confirmed before dispatch?
A: Voltage and frequency are confirmed against the buyer’s site electrical supply before production begins, not assumed from a default setting. The PLC human-machine interface dialogue system language is also confirmed at that stage so operators can read alarms and adjust parameters in a familiar language on arrival.

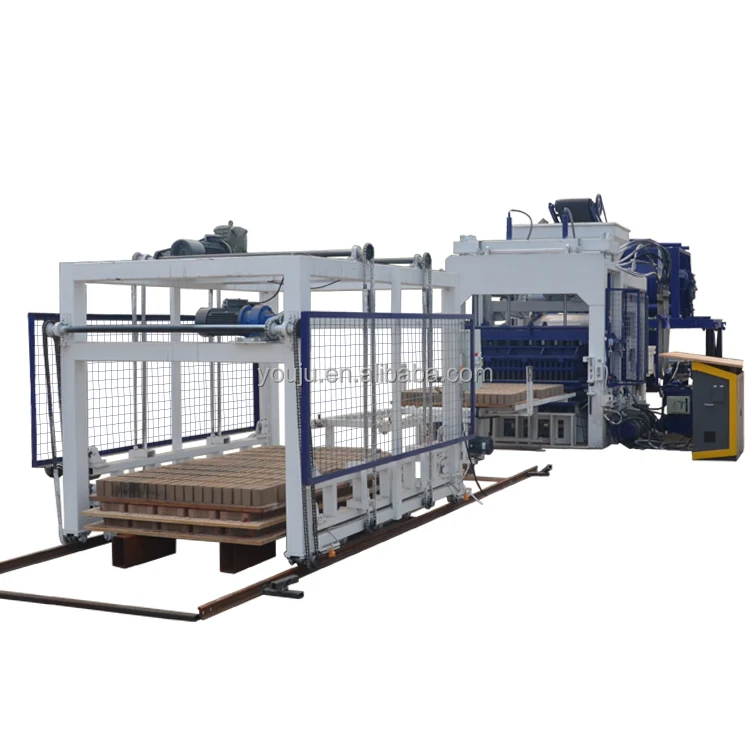
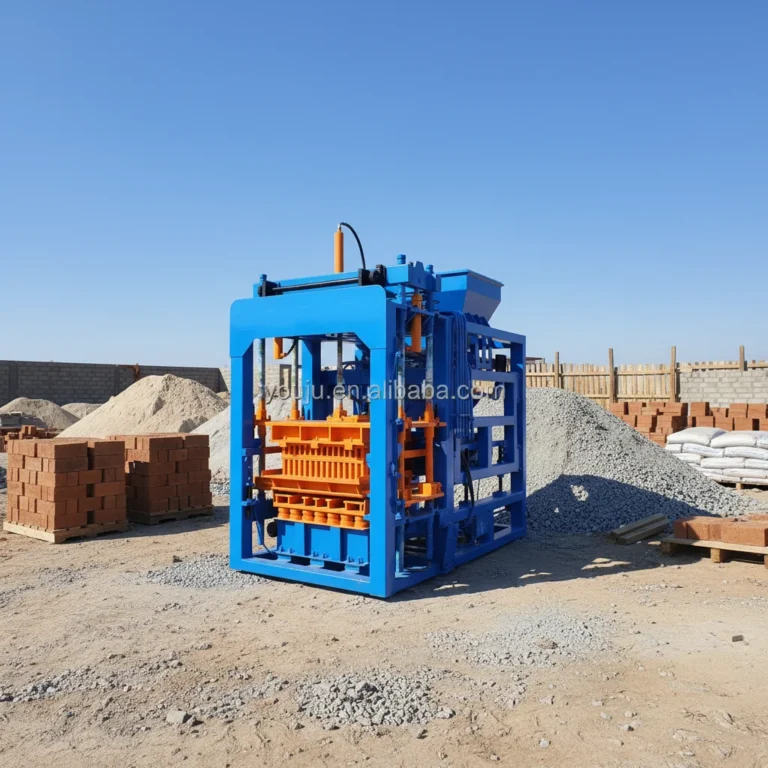 Stationary block machine