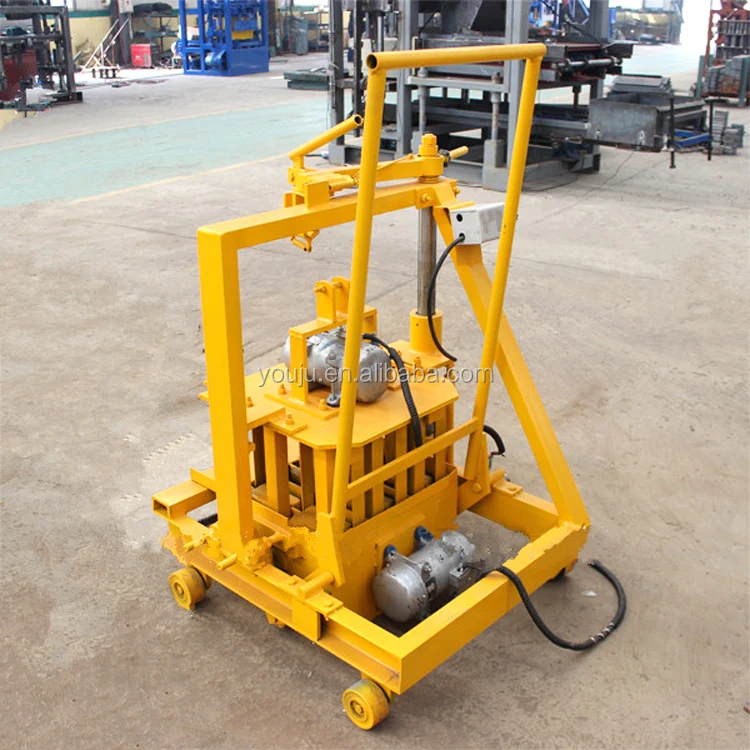
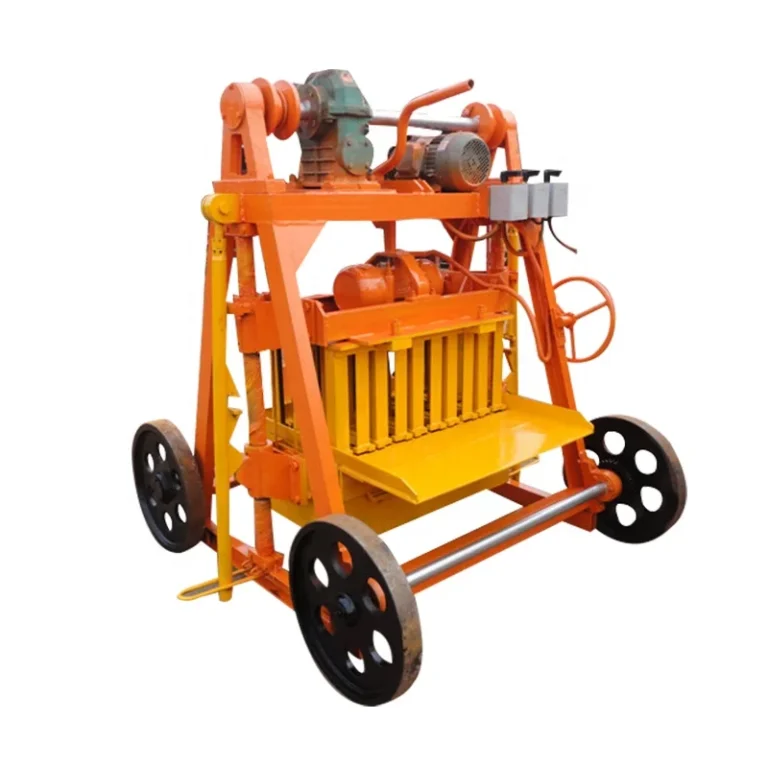
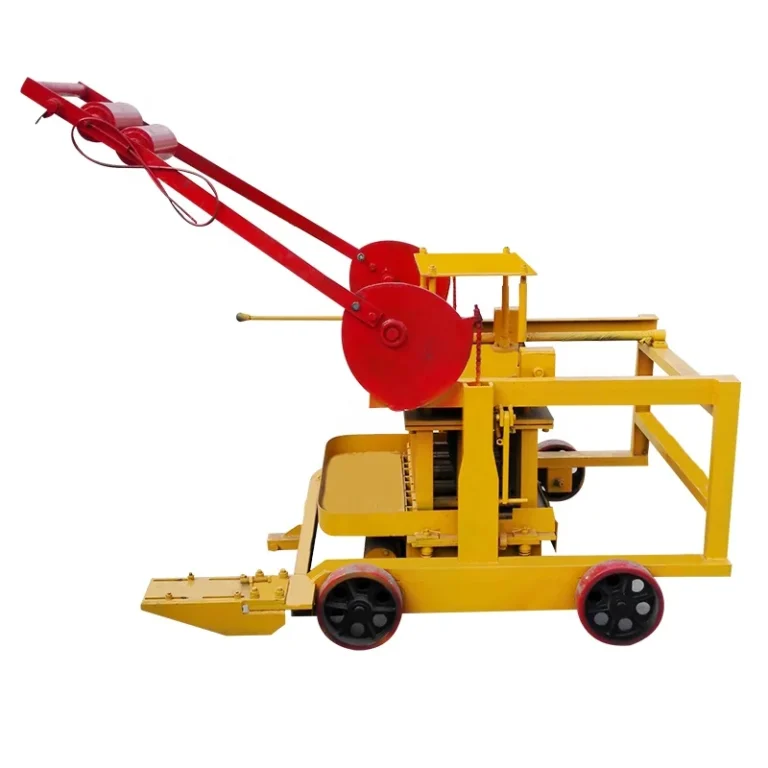
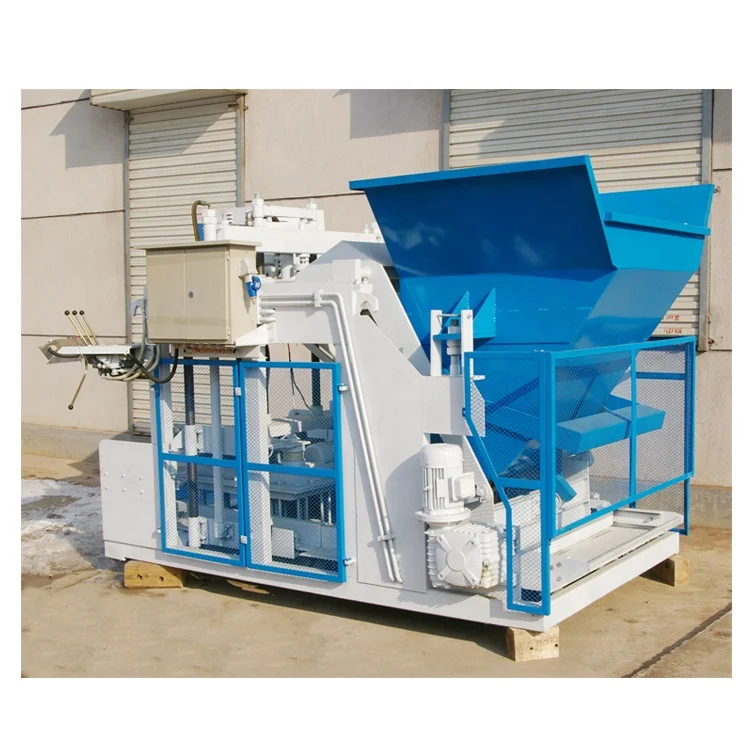
Matched System Design — the QMY12-15 mobile block machine is specified alongside its mould, engine, and gear drive as a single verified production unit, not assembled from separate suppliers, so on-site hollow block output reflects real conditions rather than factory defaults.
Technical Specifications
| Parameter |
Value |
| Model |
QMY12-15 |
| Product Type |
Automatic Mobile Cement Hollow Block Making Machine |
| Block Format Range |
4-inch, 6-inch, and 9-inch hollow blocks |
| Drive System |
Diesel engine and gear transmission |
| Automation Level |
Automatic cycle control |
| Machine Type |
Mobile / egg-laying |
| Pallet Requirement |
Not applicable (egg-laying on concrete floor) |
| Mould Format |
Hollow block, interchangeable for 4–9 inch sizes |
| Control System |
Automatic panel-controlled cycle (basis to be confirmed) |
| Voltage & Frequency |
Engine-driven, no external electrical grid required |
| Hydraulic Pressure |
Source value to be confirmed against manufacturer catalog |
| Vibration Force |
Source value to be confirmed against manufacturer catalog |
| Rated Power |
Source value to be confirmed against manufacturer catalog |
| Overall Dimensions |
Source value to be confirmed against manufacturer catalog |
| Net Weight |
Source value to be confirmed against manufacturer catalog |
| Mould Change Time |
Source value to be confirmed against manufacturer catalog |
Application Suitability
| Application |
Material or Output |
| On-site hollow block production for building contractors |
Cement, sand, crushed stone or local aggregate blended on-site |
| Housing and infrastructure projects in remote locations |
4-inch partition blocks through 9-inch load-bearing hollow blocks |
| First-stage block plant for entrepreneurs entering the market |
Egg-laying production directly onto a prepared concrete slab |
| Temporary production yards for development contractors |
Mobile operation without fixed curing racks or pallet handling |
Why Quoted Output Figures Often Fail on Real Construction Sites
Cycle rates mean nothing unless the block format, local aggregate, and ground conditions are locked into the calculation.
A QMY12-15 mobile block machine manufacturer will typically quote production in cycles per hour, but that figure assumes a specific block size and an ideal mix design. When the machine arrives on a project site and the available sand is crushed coral or a high-silt river sand rather than the standard quartz sand used during factory testing, the vibration and pressure settings no longer produce the same block density or cycle speed. Blocks crack, output drops, and the daily target becomes unreachable. I have watched this exact scenario unfold with mobile egg-laying machines in Southeast Asian project yards, where the site engineer was left re-tuning parameters for days while the construction schedule slipped [NEED_CITE: on-site aggregate variability and its effect on block press cycle time]. The honest starting point is a capacity calculation that states the assumed block format and mix, then verifies both against your actual material before the configuration is locked.

Positioning the QMY12-15 Within the Mobile Block Machine Range
The QMY12-15 mobile block machine sits in the entry-to-mid output tier for buyers who need hollow block production without investing in a fixed plant with pallets, batching silos, and curing racks. Compared to smaller mobile egg-laying models, it offers automatic cycle control and a wider mould range covering 4-inch through 9-inch hollow blocks, making it suitable for contractors who need to produce multiple wall thicknesses on a single project. Buyers evaluating their first block machine investment often compare this tier against semi-automatic stationary lines; the QMY12-15 removes the need for pallets and a dedicated curing area, trading some peak output for lower capital cost and faster site mobilization.
Ground Conditions That Determine Whether the Machine Actually Works
An egg-laying block machine produces directly onto the floor, so the quality and flatness of that concrete slab becomes part of the production system. If the slab is uneven, freshly laid blocks shift before the cement sets, causing dimensional inconsistency and waste. The QMY12-15 mobile block machine requires a smooth, level concrete surface with sufficient strength to bear the machine weight and vibration load without cracking. In tropical climates where site yards are often compacted earth with a thin concrete skim, ground preparation frequently becomes the hidden bottleneck [NEED_CITE: concrete slab flatness tolerance for egg-laying block machines]. Budgeting for proper floor preparation before the machine arrives avoids costly rework and production delays.
How Drive, Vibration, and Mould Design Interact During Production
The diesel engine and gear drive system means the QMY12-15 operates independently of the local electrical grid, a practical advantage on remote project sites where power supply is unreliable or unavailable. The engine drives both the hydraulic pump and the vibration mechanism, so consistent RPM is essential for stable block density across every cycle. The vibration force and hydraulic pressure must be matched to the specific mix design and aggregate particle size; a coarser crushed stone demands higher vibration amplitude to consolidate fully, while a fine coral sand requires lower vibration to avoid over-compaction and surface tearing. The interchangeable mould system covers the hollow block sizes most commonly specified in emerging construction markets, but mould change involves swapping the full mould box, so planning production runs by format minimizes changeover interruptions and keeps daily output on schedule.
What Happens When the Mix Design Is Assumed Instead of Verified
Shipping a mobile block machine configured for a standard river sand mix to a site that only has access to crushed limestone or volcanic aggregate almost guarantees production problems from the first day. Block walls will be too weak, faces will crumble during handling, and the vibration parameters will need complete re-tuning before the machine can produce sellable output. The cost is not just wasted cement and labor — it is the construction schedule slipping while the engineering team figures out why the factory test results are not replicating on-site [NEED_CITE: importance of pre-shipment mix design verification for block making equipment]. Every parameter set should be validated against the buyer’s actual aggregate sample before the machine leaves the factory.
Why This Machine Source Reduces Configuration Risk
The machine, mould, engine, and gear drive are specified as one matched system rather than assembled from separate suppliers, so compatibility issues that delay commissioning are resolved before shipment. Configuration is set against the buyer’s actual mix design and local aggregate, not a generic catalog default, which means the vibration and pressure parameters are realistic for the site. Mould design covers the 4-9 inch hollow block formats that the buyer’s market actually demands, with custom drawings available if local building codes require non-standard sizes. Automation level is selectable within the mobile range, so a buyer can start with the standard automatic cycle and add features as production grows. Installation support includes operator training on-site, so the crew understands ground preparation, mix proportions, and daily maintenance before the first production shift begins.
Documentation & Verification
- Line layout and capacity calculation stating the specific hollow block format assumed for each output figure
- Machine specification sheet confirming hydraulic pressure, vibration force, and cycle time per block size
- Mould drawing and format list showing exactly which 4-9 inch formats are included and which are optional extras
- Engine and gear drive specification with maintenance intervals and spare part part numbers
- Factory test record produced using buyer-confirmed aggregate and mix design before dispatch
Installation, Commissioning & Support
- Concrete slab flatness and thickness requirement verified before the QMY12-15 is placed on the production yard
- Engine oil, coolant, and gear drive lubrication checked and topped up during on-site assembly
- First production run supervised with mix design adjusted to the actual local aggregate available on-site
- Operator training covering mould change procedure, daily vibration mechanism inspection, and engine maintenance schedule
- Wear parts list with part numbers for mould liners, vibration springs, and gear drive components supplied at handover
- Follow-up support available for parameter re-tuning if the aggregate source changes during the project life
Preparing Your Inquiry for Accurate Configuration
To receive a realistic capacity proposal for the QMY12-15 mobile block machine, specify the hollow block sizes your market requires, your available aggregate type and source, and the daily output target stated per block format. Include the production yard dimensions, ground condition description, and whether a concrete slab is already in place or needs to be poured. If you are comparing mobile versus stationary options, note your project timeline and whether production will move between sites during the contract period.
Frequently Asked Questions
Q: What is the realistic daily output of the QMY12-15, and which block format is that figure based on?
A: Output capacity depends entirely on the block size, mix design, and aggregate used. A capacity figure quoted without stating the assumed block format and material is not actionable. We provide a per-format calculation based on your confirmed mix so you can plan production shifts against your actual project schedule.
Q: How does the QMY12-15 compare to semi-automatic stationary machines in terms of investment and output?
A: The QMY12-15 mobile block machine occupies the entry-to-mid tier with lower capital cost because it eliminates pallets, fixed curing racks, and a batching plant. Output is moderate compared to a full stationary line, but the investment and site preparation requirements are significantly reduced, making it practical for project-based production.
Q: What block formats and mould options are available within this machine tier?
A: The standard mould range covers 4-inch, 6-inch, and 9-inch hollow blocks, which account for the majority of wall construction specifications in emerging markets. Custom mould sizes can be manufactured to buyer drawings if local building codes require non-standard dimensions or special void patterns.
Q: What ground conditions does a mobile egg-laying block machine require?
A: The machine produces blocks directly onto the floor, so a smooth, level concrete slab of adequate thickness and strength is mandatory. Uneven or soft ground causes block shifting and dimensional inconsistency. Proper slab preparation before machine arrival is essential for consistent output.
Q: Where does this model sit in the full range, and what is the upgrade path if production needs grow?
A: The QMY12-15 sits in the mobile tier below semi-automatic and fully automatic stationary lines. If production volume eventually justifies a fixed plant, the buyer can move to a pallet-based stationary system with higher output and automated stacking, while the QMY12-15 remains useful for satellite or project-site production.

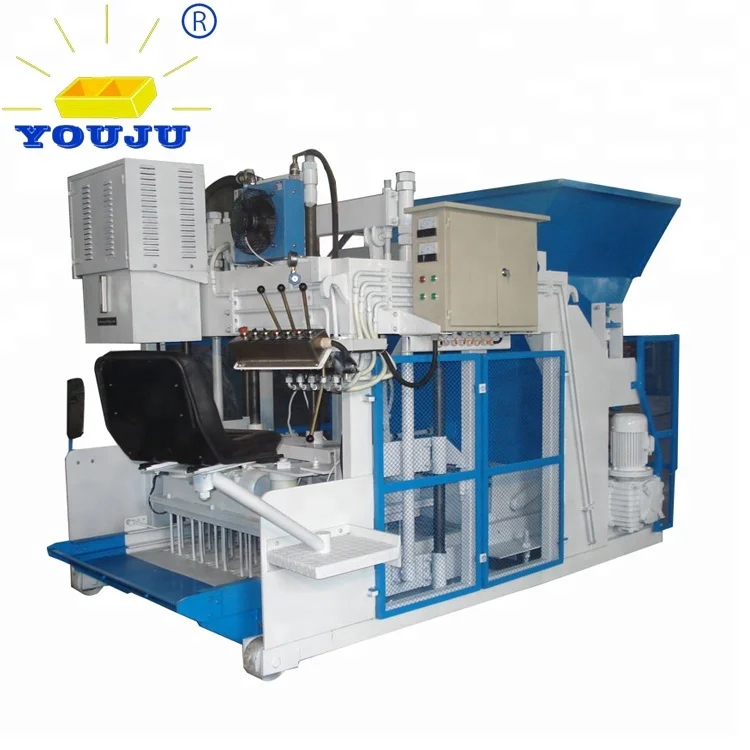
 Mobile block machine