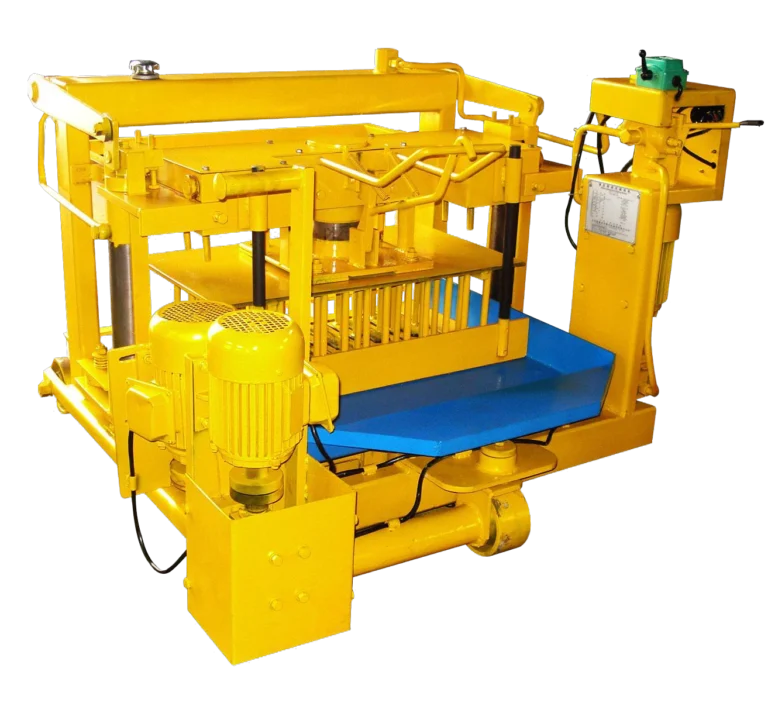
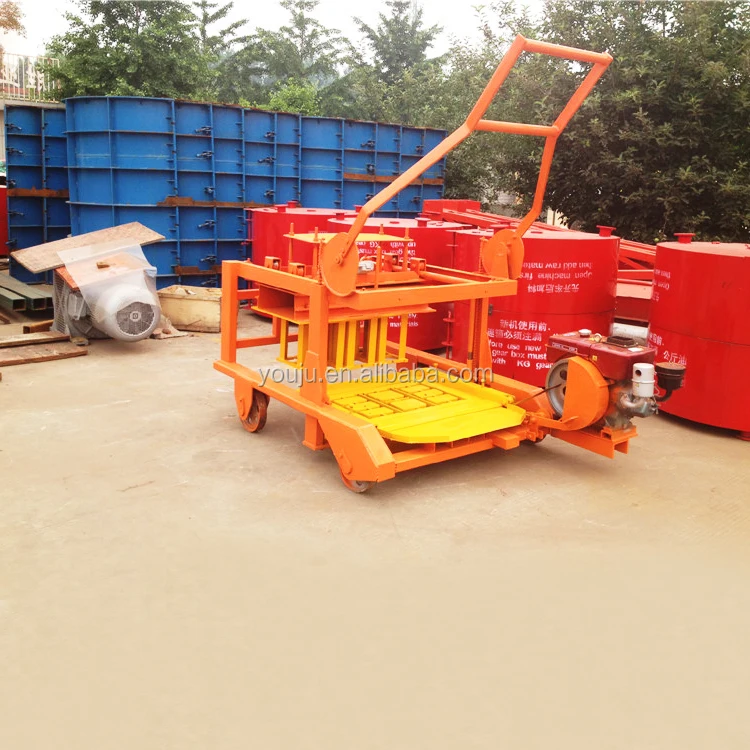
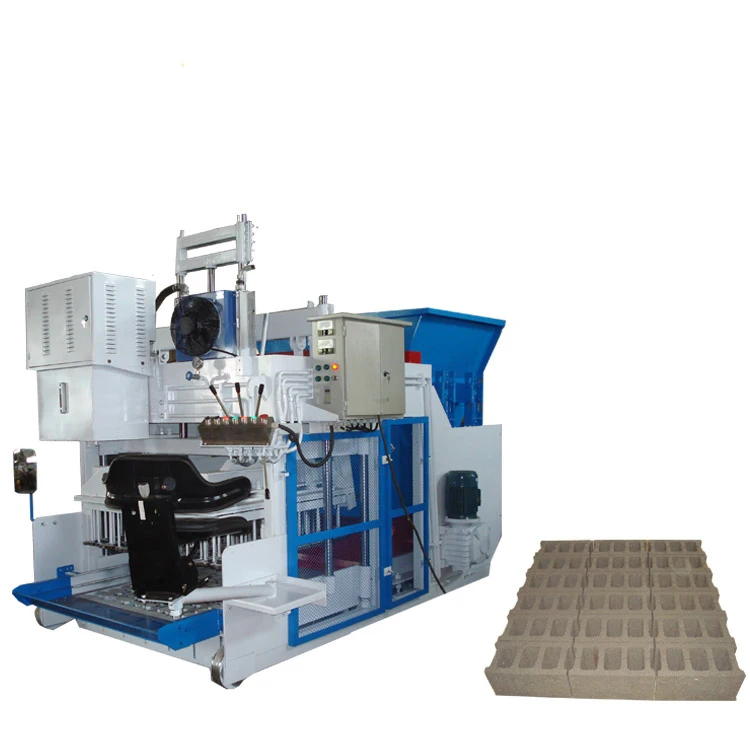
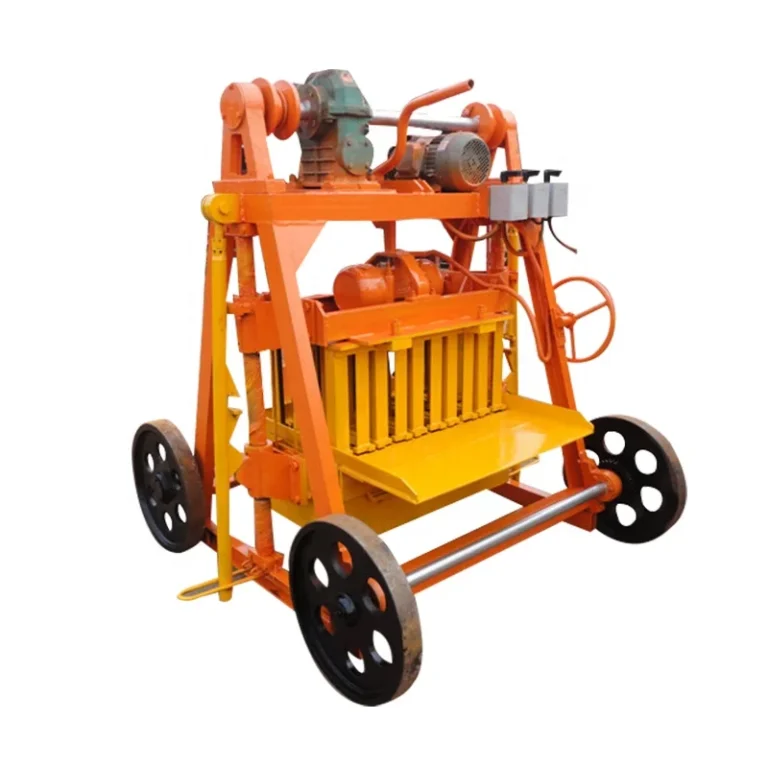
Pallet-free egg-laying design — the QMJ2-45 mobile block making machine manufacturer lineup starts here, producing hollow bricks directly on cured ground without pallets or rack systems.
Technical Specifications
| Parameter |
Value |
| Model |
QMJ2-45 |
| Product Type |
Mobile Block Making Machine |
| Operation Mode |
Manual mobile egg-laying |
| Mould Format |
Hollow brick (interchangeable sizes) |
| Cycle Time |
25–30 seconds per mould |
| Output Capacity |
160 pcs/h based on 400×200×200mm hollow brick, 2 pcs/mould |
| Output Capacity |
240 pcs/h based on 400×150×200mm hollow brick, 3 pcs/mould |
| Output Capacity |
320 pcs/h based on 400×100×200mm hollow brick, 4 pcs/mould |
| Daily Output |
1,280 pcs/8hr based on 400×200×200mm hollow brick |
| Daily Output |
4,800 pcs/8hr based on 400×150×200mm hollow brick |
| Daily Output |
2,560 pcs/8hr based on 400×100×200mm hollow brick |
| Pallet Requirement |
No pallets required (egg-laying type) |
| Labor Requirement |
1 to 3 workers |
| Mobility |
Free movement on flat ground |
| Automation Level |
Manual |
Application Suitability
| Application |
Material or Output |
| On-site housing project production |
Hollow bricks from local crushed stone, sand, and cement |
| Remote infrastructure job sites |
Block manufacturing without a fixed plant footprint |
| Entrepreneurial first block plant |
Low-investment hollow brick manufacturing |
| Small workshop add-on production |
Supplemental output alongside existing stationary equipment |
| Space-constrained construction yards |
Compact mobile block making in limited working areas |
What "Pieces per Hour" Actually Means for Your Project
Every capacity figure on this page names the exact block format behind it, because a cycle-time number alone tells you nothing about what your shift will deliver.
In my time commissioning mobile machines across Southeast Asia, I have watched contractors invest in equipment based on a headline output number, only to find that the figure assumed a block size their market does not buy. The QMJ2-45 is rated at 160 pieces per hour only when pressing 400×200×200mm hollow blocks at two per mould. Switch to the 100mm partition wall format at four per mould and the same cycle delivers 320 pieces per hour — but those are fundamentally different products with different material consumption and curing behaviour [NEED_CITE: block format standards and dimensional tolerances by market]. A mobile block making machine manufacturer that quotes one number without naming the format is asking you to guess.

Where the QMJ2-45 Sits in the Mobile Range
This model occupies the entry tier of the full mobile block machine lineup. It serves buyers who need hollow brick production on-site with no fixed plant, no pallet inventory, and a crew of one to three workers. The egg-laying principle means the machine lays each block directly onto a prepared ground surface and moves forward to the next position, eliminating the entire pallet feeding, curing rack, and de-stacking subsystem that stationary lines require. For contractors working a single housing development or entrepreneurs testing market demand before committing to a semi-automatic plant, this is the starting point.
How Egg-Laying Changes Your Site Layout
A stationary block line demands a flat concrete floor, pallet return conveyors, and curing racks occupying significant yard space. The QMJ2-45 inverts that requirement: you prepare a level strip of ground — compacted earth or a simple concrete apron — and the machine walks along it, depositing blocks in continuous rows. Curing happens in place under wet burlap or plastic sheeting [NEED_CITE: on-site concrete block curing practices]. The footprint is essentially the length of your production run, which means the machine adapts to whatever linear space the job site offers rather than dictating a fixed plant layout. This is why mobile block making machine configurations are specified around site access and ground conditions, not factory floor plans.
Reading the Specs That Matter on a Mobile Machine
Three parameters dominate real-world output on an egg-laying machine: cycle time, mould cavity count, and crew coordination. The 25–30 second cycle time assumes the operator has mixed material ready and the machine is positioned on level ground; any delay in feed preparation extends the cycle. Mould cavity count varies by format — two cavities for the 200mm wall block, three for 150mm, four for 100mm — which is why hourly output shifts across formats even though the press mechanism is identical. The manual automation level means the crew controls material feeding, machine advance, and mould release directly, so labour discipline and mix consistency set the ceiling on what the spec sheet promises.
The Hidden Cost of Skipping the Material Sample
I once shipped a mobile unit configured for standard river sand to a project where the local aggregate ran high in clay content. The vibration parameters that produced clean, dense hollow bricks in our factory test produced crumbly, undersized blocks on arrival. We spent days on-site re-matching the water-to-cement ratio and adjusting compaction technique before the line ran acceptably. When the material arriving at your hopper differs from what the machine was set up to press, every output and strength assumption collapses [NEED_CITE: aggregate grading and clay content limits for concrete block production]. This is why a mobile block making machine manufacturer should request your local sand and stone samples before finalising the mould and vibration setup, not after the container is loaded.
Why Sourcing from a Single-Focus Line Matters
Block machinery is our single product category, which means the QMJ2-45 is specified as part of a matched system rather than assembled from separate catalogue items. The mould formats we quote are the ones your local construction market actually specifies, verified against your drawings before production. Mould interchangeability on this model lets you shift between hollow brick wall thicknesses without buying a second machine, but the changeover procedure and tooling are documented specifically for your format list. We confirm voltage, frequency, and any control labelling language before the machine enters production — not at the packing stage — because an egg-laying machine arriving with the wrong motor winding or unreadable labels sits idle while you source local electrical components.
Documentation & Verification
- Line layout showing egg-laying run length and ground preparation requirements
- Capacity calculation sheet stating block format assumed for each output figure
- Mould drawing and format list matching your specified hollow brick dimensions
- Voltage and frequency confirmation record signed before production begins
- Factory test record run on material gradation matching your local aggregate sample
- Operation and maintenance manual with wear parts list for first replacement cycle
Installation, Commissioning & Support
- Ground preparation guide specifying compaction level and minimum linear run length for egg-laying
- Power supply requirements confirmed against your site voltage and frequency before dispatch
- Machine arrives fully assembled with mould installed; no major on-site reassembly required
- First-day commissioning covers mix adjustment, cycle timing verification, and block dimension checks
- Operator training addresses material feeding rhythm, machine advance technique, and mould release timing
- Wear parts list identifies first-order spares based on your chosen aggregate abrasiveness
What We Need to Configure Your QMJ2-45
To move from inquiry to a meaningful quotation, share the hollow brick dimensions your local market specifies and the daily volume you plan to run. Tell us what sand and stone are available locally — a sample or a gradation report lets us match vibration and compaction settings before build. Confirm your site power supply voltage and frequency so the motor is wound correctly. If you already have ground preparation or curing practices in place on-site, describe them so we can align the machine setup with your existing workflow rather than asking you to adapt to ours.
Frequently Asked Questions
Q: How is the output capacity of the QMJ2-45 verified, and which block format does each number assume?
A: Every capacity figure we publish names the block dimensions and mould cavity count behind it. The 160 pieces per hour rating assumes 400×200×200mm hollow bricks at two per mould; the 320 pieces per hour figure assumes 400×100×200mm at four per mould. We provide a capacity calculation sheet with your quotation that breaks down hourly and daily output for the specific format your market requires.
Q: Which block formats can the QMJ2-45 produce, and how long does a mould change take?
A: The QMJ2-45 accepts interchangeable moulds within the hollow brick family. Standard formats include 200mm, 150mm, and 100mm wall thicknesses at 400mm length. Mould changeover is a manual procedure involving bolt release and re-alignment; exact time depends on operator familiarity and is covered during commissioning training. We supply a format list with your order so you confirm which sizes are included before production.
Q: What voltage and frequency options are available for the QMJ2-45?
A: The motor is wound to your specified voltage and frequency before the machine enters production. We confirm these values during the quotation stage and record them on a signed specification sheet. This prevents the common problem of a machine arriving with a motor that does not match the local power grid, which otherwise delays commissioning while a replacement is sourced.
Q: Where does the QMJ2-45 sit in the full Shiyue range, and what is the upgrade path?
A: The QMJ2-45 is the entry tier of our mobile block machine lineup, designed for pallet-free egg-laying production with minimal investment. Buyers who outgrow its manual output level typically move to a semi-automatic stationary line with pallet handling, then to a fully automatic system with stacking and cubing. Each step adds automation while retaining the block format knowledge and mould tooling from the previous stage.
Q: What site conditions are needed to run the QMJ2-45 on a construction site?
A: You need a prepared linear strip of level ground — compacted earth or a concrete apron — long enough for your planned daily run. The machine deposits blocks in place and advances forward, so curing happens on the ground under cover. One to three workers handle material mixing, machine operation, and block protection. Site power must match the confirmed motor specification, and local aggregate should be sampled before machine configuration.

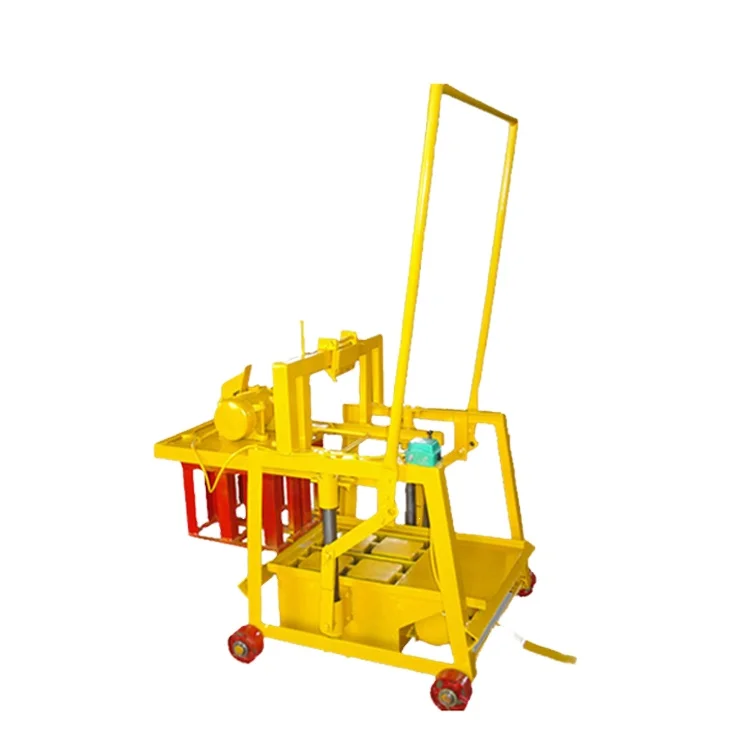
 Mobile block machine