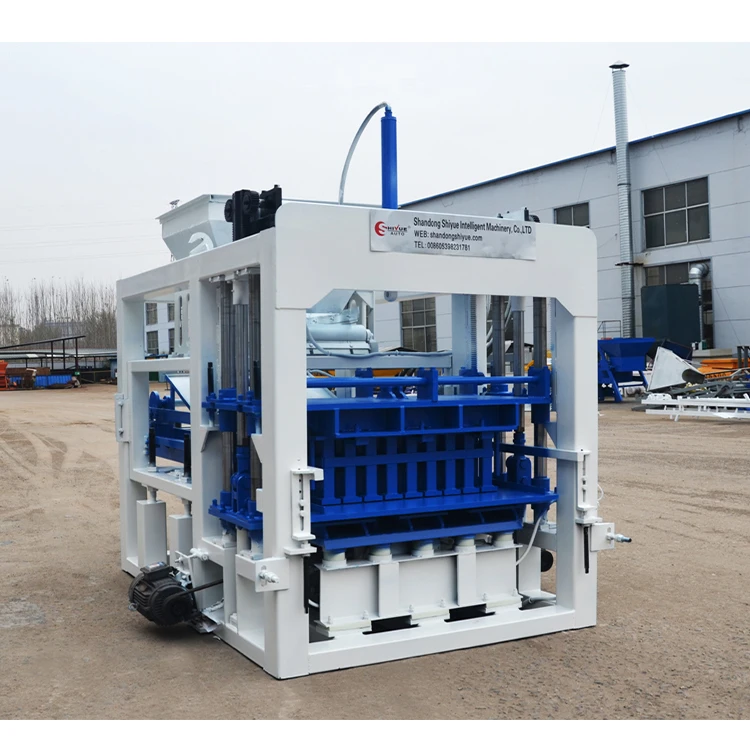
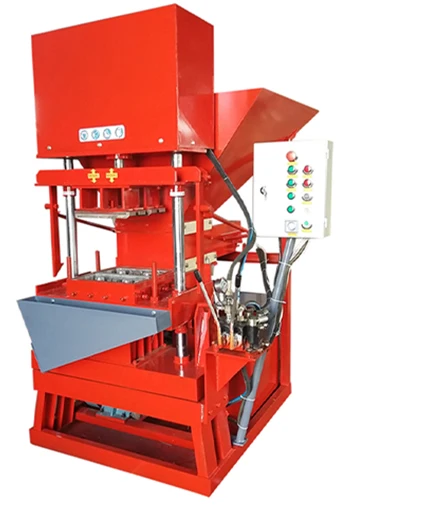
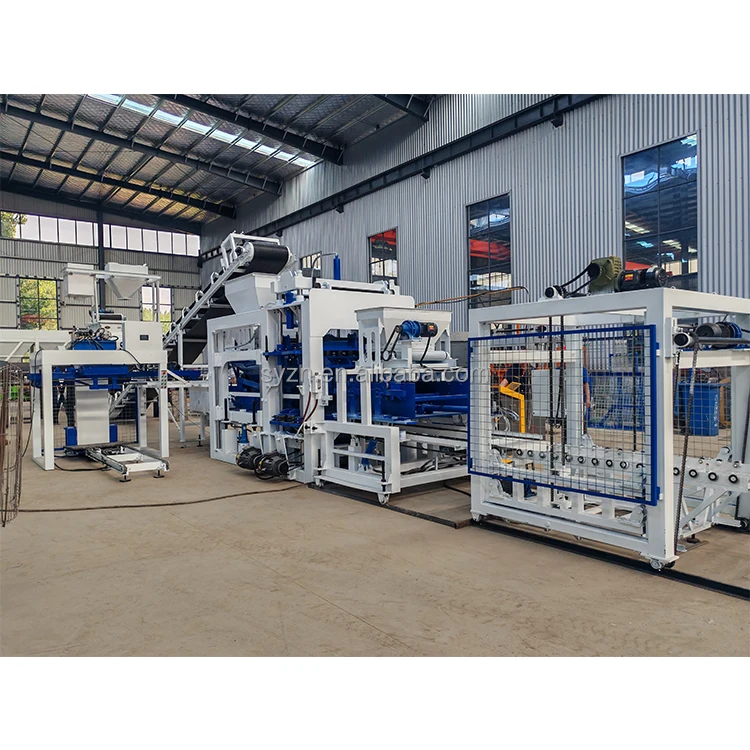
Single-Focus Machinery Configuration — the QTJ4-25D is specified as one matched system covering press, pallet handling and stacking, not assembled from separate suppliers.
Technical Specifications
| Parameter |
Value |
| Model |
QTJ4-25D |
| Product Type |
Automatic Concrete Block Making Machine |
| Control System |
PLC controlled fully automatic |
| Machine Power |
16.58 kW |
| Molding Cycle |
25 seconds |
| Output Capacity |
4600 pcs / 8 hours (basis not stated in source — confirm block format, material, thickness) |
| Machine Weight |
5000 kg |
| Overall Size |
6400 × 1500 × 2700 mm |
| Pallet Size |
850 × 480 mm |
| Vibration System |
Vibration motor with large vibration box |
| Motor Brand |
Siemens motor |
| Frame Construction |
Thickened steel |
| Voltage |
Configured to buyer’s local supply |
| Automation Features |
Automatic pallet feeding, automatic material feeding and scraping, automatic block stacker |
| Raw Materials |
Concrete, sand, cement, fly ash, crushed stone, lime, water |
| Warranty |
One year |
Application Suitability
| Application |
Material or Output |
| Medium-sized hollow block production |
Crushed stone, sand, cement blends |
| Solid concrete block manufacturing |
Fly ash, cement, aggregate mixes |
| Paver stone brick output |
Cement-bound sand and fine aggregate |
| First-plant entrepreneurs evaluating automatic tier |
Standard concrete mixes with locally available sand |
| Building material distributors stocking multiple formats |
Interchangeable moulds on one press platform |
What "4600 Pieces Per Shift" Leaves Out When Format Is Unstated
A capacity figure without a block format attached is a number without meaning.
Many buyers receive quotations quoting thousands of pieces per shift, then discover on the production floor that the figure assumed a small solid paver while they needed large hollow blocks. I have watched this mismatch unfold when a buyer in the Middle East expected a certain daily volume of hollow blocks, only to find the cycle time and mould cavity count for that format cut real output noticeably. The QTJ4-25D as an automatic block machine manufacturer offering is rated at 4600 pieces per 8-hour shift, yet the block format behind that figure must be confirmed before the number can be trusted for plant planning. Real daily output depends on whether the mould produces hollow blocks, solid blocks or pavers, and on the local aggregate in the mix [NEED_CITE: block format and cycle time relationship in concrete block production].

Where the QTJ4-25D Sits on the Full Machine Range
The block machine range spans mobile egg-laying units for on-site work, semi-automatic presses for smaller plants, and fully automatic lines like the QTJ4-25D for medium-volume factories. This model brings PLC-controlled operation together with automatic pallet feeding and block stacking, removing manual pallet handling from the operator’s workflow. For a buyer moving up from a semi-automatic press, the step means continuous production cycles without waiting for an operator to place or remove pallets by hand.
Matching Automation Level to Plant Size and Investment
A first-time plant owner may not need the highest output tier; the QTJ4-25D occupies the middle ground where automatic operation justifies the investment without the footprint of a high-capacity hydraulic line. The automation package includes automatic material feeding with scraping and an automatic stacker, which reduces labour on the line while keeping the plant floor area manageable. Buyers who plan to add formats later benefit from a platform that already handles mould changes and pallet logistics, leaving room to grow without replacing the press [NEED_CITE: automation tier selection criteria for concrete block plants].
Reading the Specs That Shape Daily Production
The 16.58 kW machine power drives both the vibration motor and the material feed system simultaneously, which matters when the press runs dense aggregate mixes that demand sustained vibration force throughout each 25-second cycle. The 850 × 480 mm pallet size determines how many block cavities fit per mould and must align with the curing racks and forklifts already in the buyer’s yard. A pallet dimension chosen without checking existing handling equipment leads to double-handling on the curing floor. The Siemens motor specification supports serviceability in export markets where local technicians recognise the brand and can source replacement parts. The thickened steel frame absorbs repeated vibration loads over continuous shifts, reducing the fatigue cracking that lighter frames develop after extended production runs.
The Cost of Skipping Voltage and Language Confirmation
When voltage, frequency and PLC display language are not locked down before production, the machine arrives on site and sits idle while transformers are sourced or control panels are reprogrammed. I have seen commissioning delayed by weeks because the PLC screen defaulted to a language the local operators could not read, and the buyer’s electrician had no schematic matching the installed voltage. Every QTJ4-25D leaves the factory only after these three items are confirmed in writing against the buyer’s local grid standard [NEED_CITE: voltage and frequency standards by export market].
Why Source This Automatic Block Machine Manufacturer Range Here
Block machinery is the single production focus, so the press, mould, pallet and stacking system are specified together rather than pulled from unrelated suppliers. The configuration process starts with the buyer’s actual mix design and local aggregate, not a catalogue default, which prevents the mismatch between machine settings and available raw materials. Mould design covers the formats the buyer’s market demands, with custom drawings accepted to buyer specifications. Automation level is selectable within the range, allowing a buyer to begin at this tier and move higher as production grows. Installation support includes on-site commissioning with operator training so the team running the press understands mould changes, pallet handling and daily maintenance from day one.
Documentation & Verification
- Machine specification sheet with confirmed voltage, frequency and PLC display language
- Line layout and capacity calculation stating the block format assumed for the 4600-piece figure
- Mould drawing and format list showing every cavity option available for the 850 × 480 mm pallet
- Factory test record with photographs taken on the buyer’s selected block format before dispatch
- Operation and maintenance manual covering mould change procedure and vibration box servicing
Installation, Commissioning & Support
- Foundation plan sized to the 6400 × 1500 mm footprint and 5000 kg operating weight
- Dedicated power circuit matching the 16.58 kW load at the buyer’s confirmed voltage and frequency
- PLC display language set and verified before the control cabinet leaves the factory
- On-site mould change training so operators can switch between hollow, solid and paver formats
- Vibration box and motor inspection schedule aligned with continuous shift operation
- One-year warranty covering frame, hydraulic wear parts and electrical components
What We Need to Size Your Line Correctly
Send the block format or formats you plan to produce, including dimensions and target wall thickness for hollow blocks. Share the local aggregate type and any sample mix proportions you have already tested, so the vibration force and cycle time can be matched before the machine is built. Confirm your site voltage, frequency and the language your operators need on the PLC screen, along with the curing area dimensions and forklift capacity, so the 850 × 480 mm pallet specification fits your existing handling setup.
Frequently Asked Questions
Q: What block format does the 4600 pieces per 8 hours figure assume?
A: The source does not state which block format, wall thickness or mix density was used for that capacity figure. We provide a detailed capacity calculation per format — hollow, solid or paver — once your target product and mould cavity count are confirmed, so you can plan shifts around real output rather than a catalogue number.
Q: Where does the QTJ4-25D sit between semi-automatic and high-capacity hydraulic lines?
A: It occupies the automatic tier with PLC control, automatic pallet feeding and stacking, suited to medium-sized factories stepping up from manual operation. Buyers needing higher volumes or heavier compaction may move to a hydraulic press tier, while smaller plants or first-time buyers might start with semi-automatic models on this range.
Q: How are voltage and PLC language confirmed before shipment?
A: We request your local voltage, frequency and preferred PLC display language during the inquiry stage and lock them into the machine specification sheet before production begins. This prevents commissioning delays caused by incompatible power supply or unreadable control screens when the automatic block machine manufacturer delivers the equipment to your site.
Q: What plant footprint does the QTJ4-25D line require including pallet handling?
A: The press itself measures 6400 × 1500 × 2700 mm, but the working line must account for pallet feeding on one side and the automatic stacker output on the other, plus space for curing rack access. We provide a line layout drawing showing total floor area needed before you commit to the order.
Q: Are moulds and wear parts available when the first replacement is due?
A: Mould and hydraulic wear parts are listed in the documentation pack shipped with the machine, and replacements are supplied against the one-year warranty and beyond. We keep mould drawings on file for every format produced, so reorder lead times remain short when your production schedule demands a quick turnaround.

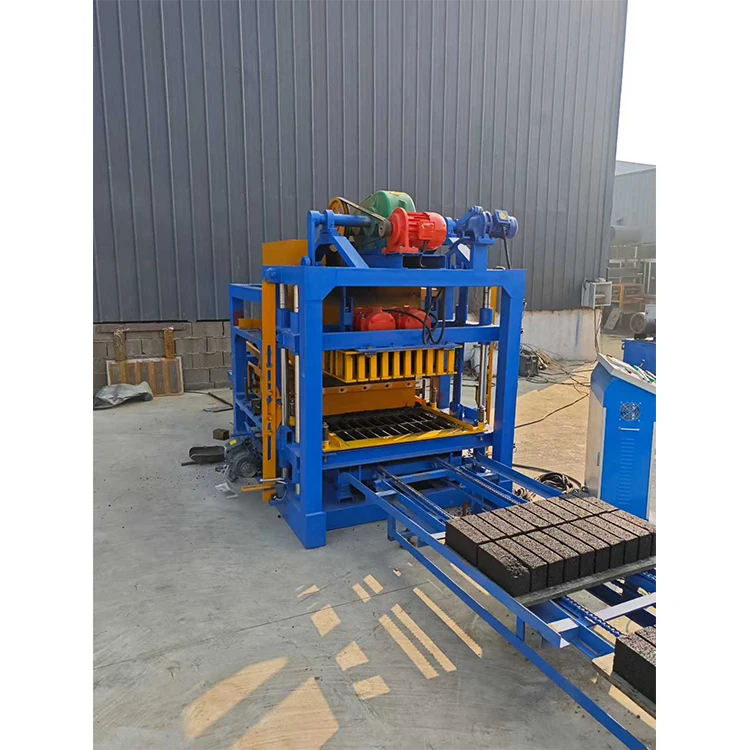
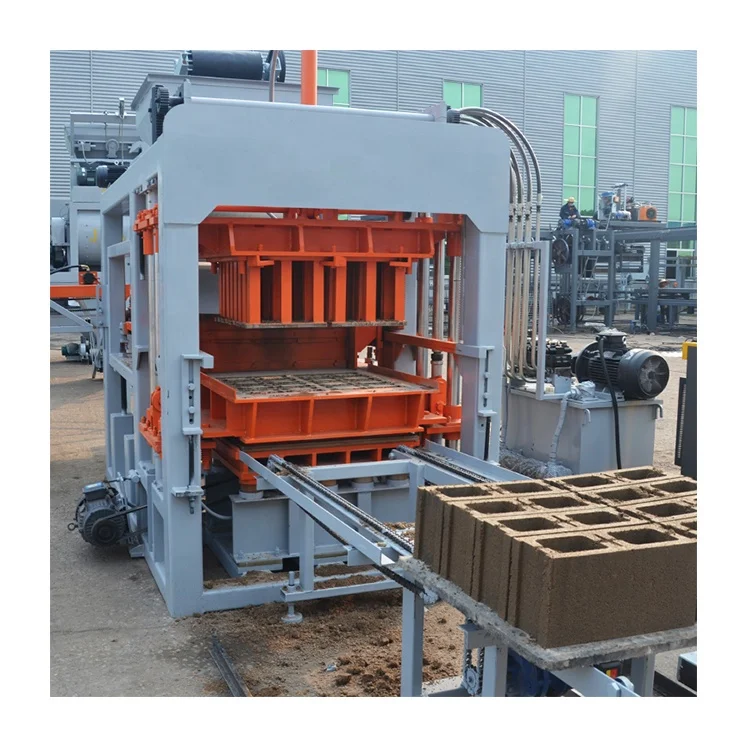 Automatic block machine