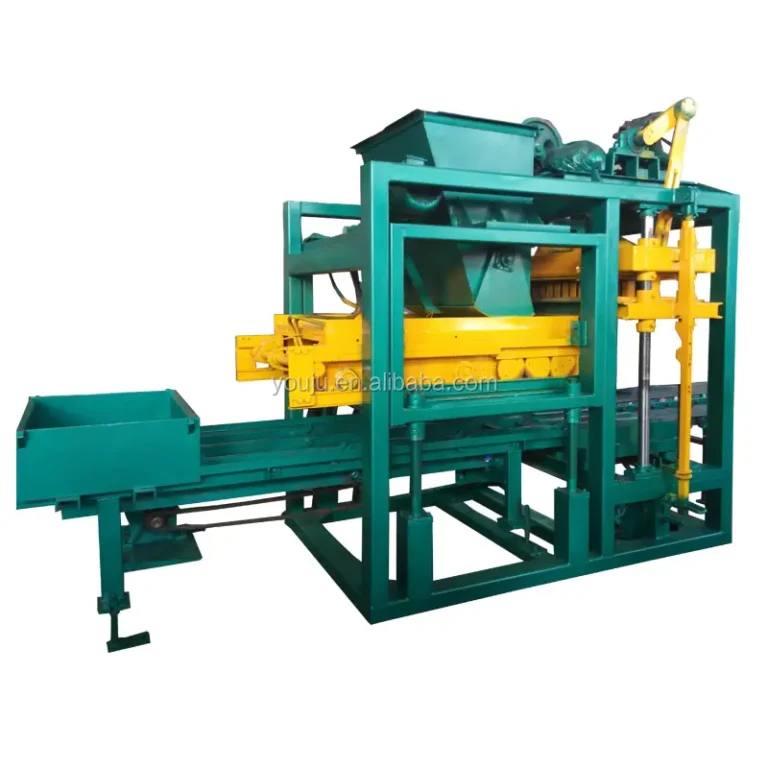
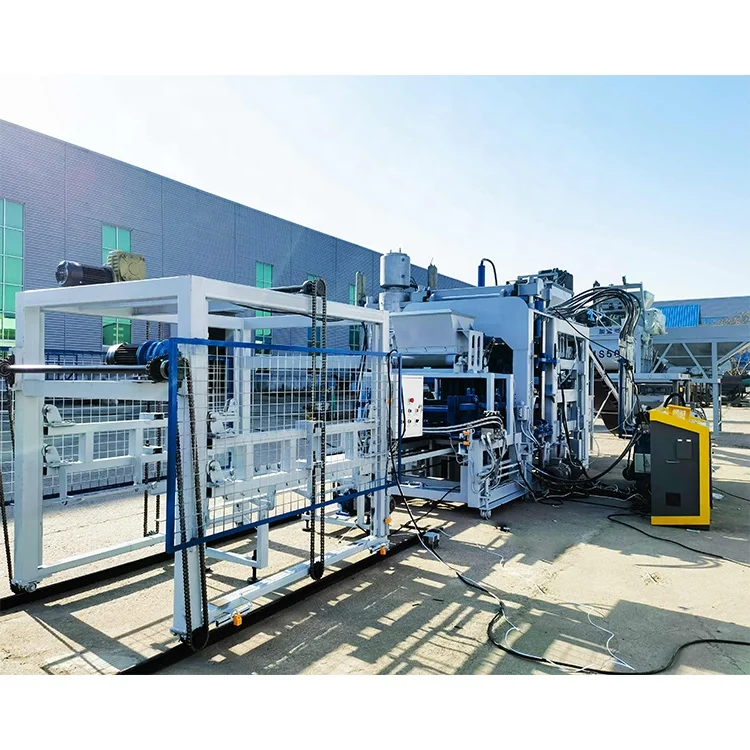
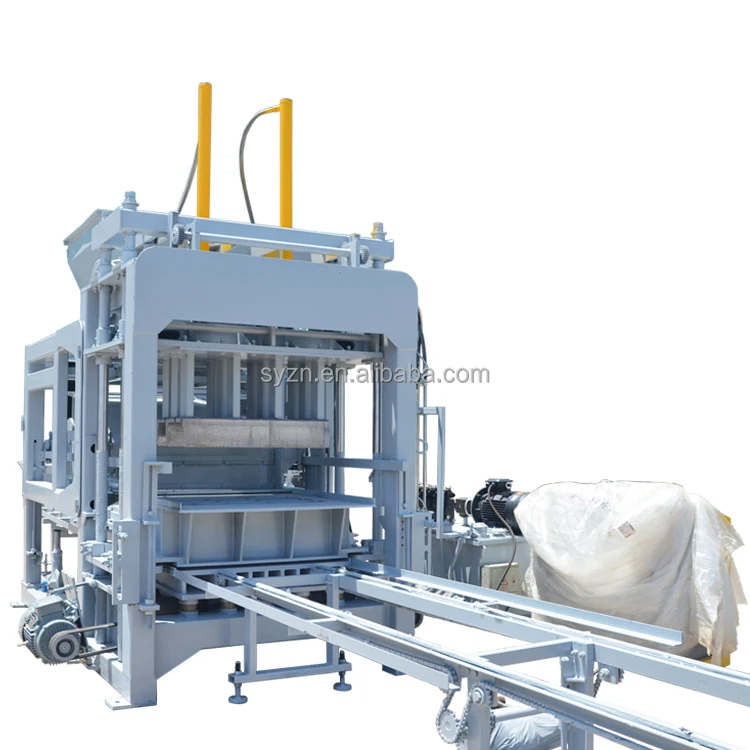
Integrated System Match — The QTF3-20 is specified against your actual block format, local aggregate, and curing layout before a capacity number is ever quoted.
Technical Specifications
| Parameter |
Value |
| Product Type |
Stationary Concrete Block Making Machine |
| Model |
QTF3-20 |
| Total Power |
17.5 kW |
| Overall Dimensions (L×W×H) |
4000 × 3500 × 2300 mm |
| Net Weight |
2870 kg |
| Vibration Form |
Platform Vibration |
| Control System |
Semi-Automatic |
| Output Capacity |
4,320 pcs/day (basis to be confirmed — dependent on block format and material) |
| Raw Material Compatibility |
Cement, sand, fly ash, coarse aggregate, slag |
| Drive System |
Hydraulic system with no-contact proximity switch monitoring |
| Material Layers |
Double layer (raw material and color surface) |
| Electrical & Hydraulic Components |
Imported from Germany or Chinese famous brand (specific brands to be confirmed) |
| System Components |
Host machine, material feeder, color material machine, pallet feeder, block conveyor, hydraulic station, electricity box |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Cement, sand, and coarse aggregate mixes for structural wall units |
| Interlocking brick production |
Fly ash or slag blends for mortarless wall systems |
| Color paver production |
Double-layer feeding with pigmented surface material over standard base |
| Porous and permeable brick |
Open-graded aggregate mixes for stormwater management installations |
| Park grass brick |
Coarse aggregate and cement for landscaped parking and pathway grids |
| Standard solid brick |
Dense sand-cement mixes for load-bearing and partition walls |
Why the 4,320 Pieces Per Day Figure Needs Context
A daily output number means nothing without the block format, cycle time, and pallet size that produced it.
Many quotations for stationary block machines list a single capacity figure and leave the buyer to discover on commissioning day that hollow blocks run at a different pace than solid pavers. I have watched contractors base their project timelines on a number that assumed a thin paver format while they actually needed 200 mm hollow blocks. The QTF3-20 is rated at 4,320 pieces per day, but that number shifts depending on whether you are pressing hollow blocks, interlocking pavers, or porous bricks, and what your local aggregate allows in terms of cycle time. [NEED_CITE: block format impact on daily output calculations]
Every stationary block machine manufacturer should tell you which format their capacity assumes. We calculate the realistic daily output against your specific block type, your mix design, and your working hours before the quotation goes out.
Where the QTF3-20 Sits in the Machine Range
The QTF3-20 occupies the entry-to-mid tier of the stationary block machine lineup. It pairs a semi-automatic hydraulic press with platform vibration, giving buyers a practical starting point for a first block plant or a supplementary line for an existing operation. The semi-automatic control keeps the electrical cabinet straightforward while still delivering consistent block density through proximity switch monitoring.
For a buyer surveying options, this model answers the question of what a semi-automatic stationary block machine can produce before committing to a fully automatic line. The double-layer material feeding system means color pavers and face-mix bricks are within reach from day one, not an afterthought requiring a separate machine.
Matching the Line Around the Press

A block press does not work in isolation. The QTF3-20 forms a simple production line when paired with a JQ350 mixer and an 8-meter conveyor belt, but the cycle times at every station must align so the press is never left waiting for material or pallets. The pallet feeder, material feeder, color material machine, and block conveyor are all specified as part of the same system.
When the mixer output, conveyor speed, and pallet return loop are mismatched to the press cycle, the stated capacity becomes theoretical. We size each station against the QTF3-20 cycle time for your chosen block format so the line runs continuously rather than in bursts. [NEED_CITE: production line synchronization in concrete block plants]
How Hydraulic Pressure and Vibration Shape Block Density
The QTF3-20 uses platform vibration combined with hydraulic press force to compact the mix into the mould. The hydraulic system controls block height while vibration determines internal density, and these two forces must be balanced against your specific aggregate. A high-clay sand requires different vibration amplitude and press dwell time compared to clean crushed stone.
The 17.5 kW total power drives both the hydraulic station and the vibration motor. Platform vibration transmits force through the mould table rather than through the mould walls, which produces more uniform compaction across the pallet area. The no-contact proximity switches monitor press position without mechanical wear, maintaining consistent block height over long production runs. The double-layer feeding system delivers a base material charge followed by a color surface charge in a single cycle, which is essential for pavers and face-mix bricks where surface finish matters.
The Cost of Skipping the Mix Design Conversation
Ordering a stationary block machine without confirming your local aggregate and target block format leads to problems that surface only after commissioning. The vibration parameters are set at the factory for a reference mix, and if your sand has a different moisture content or clay percentage, the blocks may come out under-compacted or over-pressed. I have seen machines arrive on site and produce blocks at a fraction of expected output because the mould was sized for a format the buyer never intended to sell.
Pallet size is another specification that buyers overlook until the curing area is already built. If the pallets do not match the forklift tine spacing or the curing rack dimensions you already have, every pallet becomes a manual handling problem. [NEED_CITE: common commissioning issues in exported block machinery]
Why Buyers Spec This Machine Through Us
We focus exclusively on block making machinery, which means the QTF3-20 host machine, moulds, pallets, and handling equipment are specified as one matched system rather than sourced from separate suppliers and bolted together. The configuration is set against your actual mix design and target block format, not pulled from a catalogue default.
Mould design covers the formats your market actually sells, and custom mould drawings are available when standard formats do not match local building codes. The automation level is selectable, so you can start with the semi-automatic QTF3-20 and plan a future upgrade path. Installation support includes operator training on your specific mould set and mix proportions. [NEED_CITE: matched system approach in block machinery supply]
Documentation & Verification
- Line layout drawing showing QTF3-20 footprint with mixer, conveyor, and curing area dimensions
- Capacity calculation sheet stating the block format assumed for the daily output figure
- Machine specification sheet with hydraulic and electrical schematics for the 17.5 kW system
- Mould drawing and format list covering hollow, paving, interlocking, and porous brick types
- Voltage, frequency, and control language confirmation recorded before production begins
- Factory test record on your specified block format and mix proportion before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 4000 × 3500 mm footprint with anchor bolt positions
- Electrical supply confirmation for 17.5 kW total load on a dedicated circuit at your local voltage
- Machine ships as host unit plus line components for on-site assembly and alignment
- First-run commissioning includes hydraulic pressure and vibration tuning to your aggregate
- Operator training covers mould change procedure and proximity switch calibration
- Wear parts list identifies hydraulic seals, vibration springs, and mould liner replacement intervals
What to Prepare Before Requesting a Quote
To size the QTF3-20 correctly, share the block formats you plan to produce with dimensions and target daily output for each. Provide a sample or description of your local sand and aggregate so we can set the vibration and hydraulic parameters before the machine leaves the factory. Confirm your site voltage, frequency, and preferred control panel language to avoid commissioning delays.
Frequently Asked Questions
Q: What block format is the 4,320 pcs/day capacity based on, and how does output change across formats?
A: The 4,320 pieces per day figure requires confirmation against a specific block format, as hollow blocks, pavers, and interlocking bricks each have different cycle times and mould fill volumes. We recalculate daily output once you provide your target block dimensions and local mix design, so the number in your quotation reflects the product you will actually produce.
Q: Which voltage and frequency configurations are available for the target market?
A: The QTF3-20 electrical system is configured to your site voltage and frequency before production begins. We confirm these values during the quotation stage along with the control panel display language, so the electricity box arrives matched to your local supply without requiring on-site modification or transformer installation.
Q: What is the full line footprint including mixer, conveyor, and curing area?
A: The host machine occupies 4000 × 3500 mm, and the complete line with JQ350 mixer and 8-meter conveyor belt extends beyond that. We provide a line layout drawing showing total floor space, material flow direction, pallet return path, and recommended curing rack positions based on your target output and available building dimensions.
Q: Can the automation level be upgraded from semi-automatic to fully automatic later?
A: The QTF3-20 semi-automatic control system is designed with an upgrade path in mind. Adding automatic stacking and cubing equipment later is possible when your production volume justifies the investment. We discuss the upgrade timeline during initial specification so the machine layout leaves space for future automation stations.
Q: Which mould formats are included, and how long does a mould change take?
A: The standard configuration includes moulds for the block formats you specify during the quotation stage. Mould change time depends on the mould clamping system and operator familiarity, and we cover the procedure during on-site training so your team can switch formats within a practical timeframe during a normal shift.

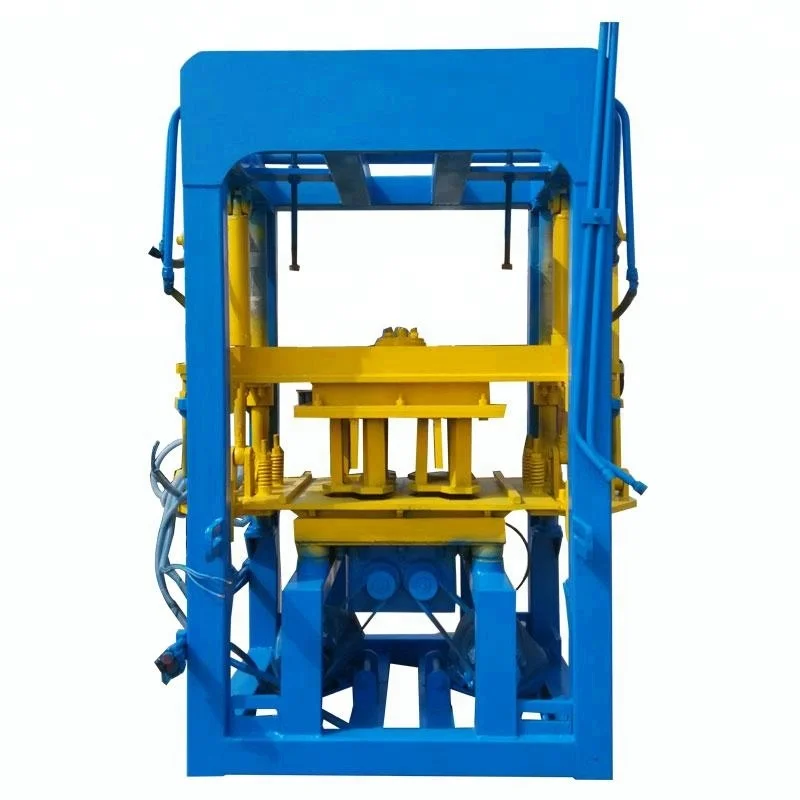
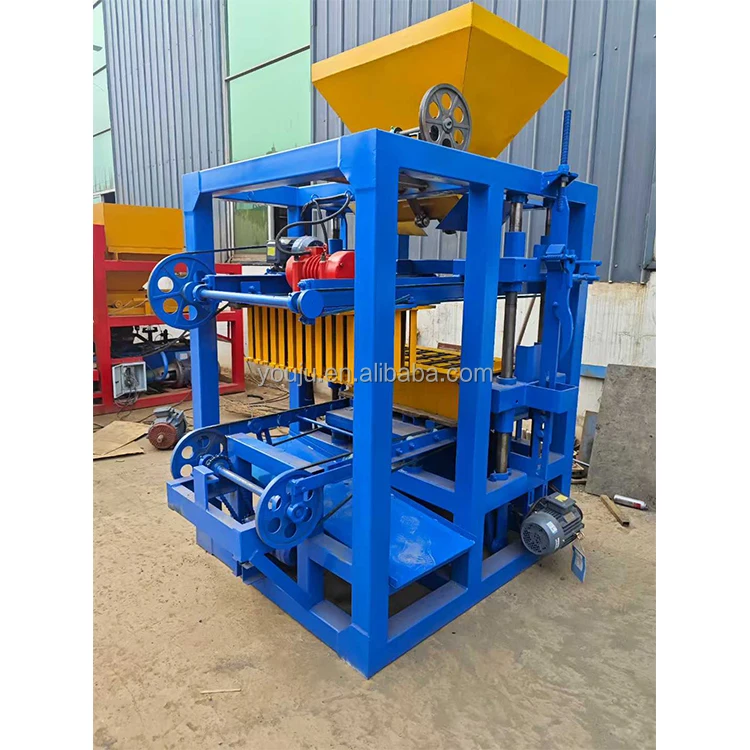 Stationary block machine