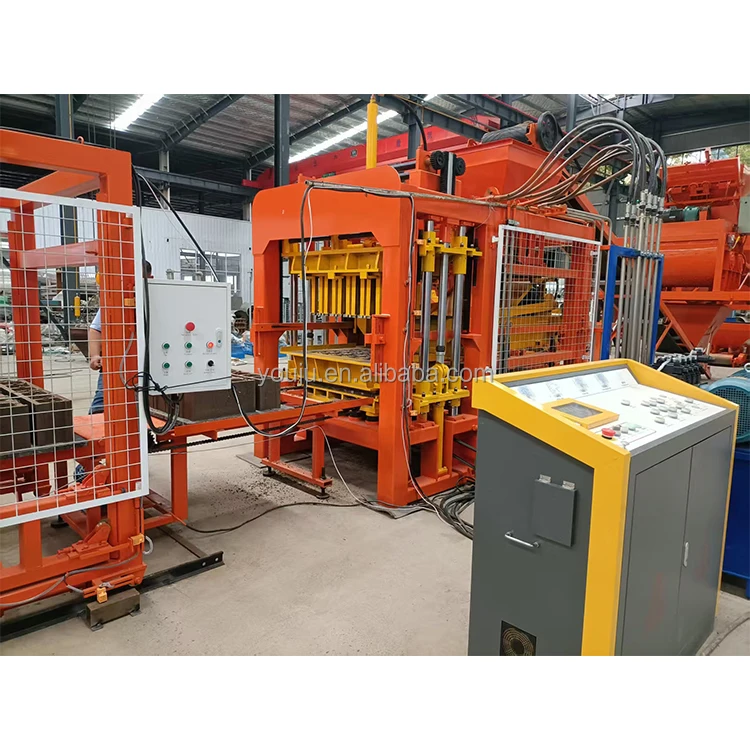
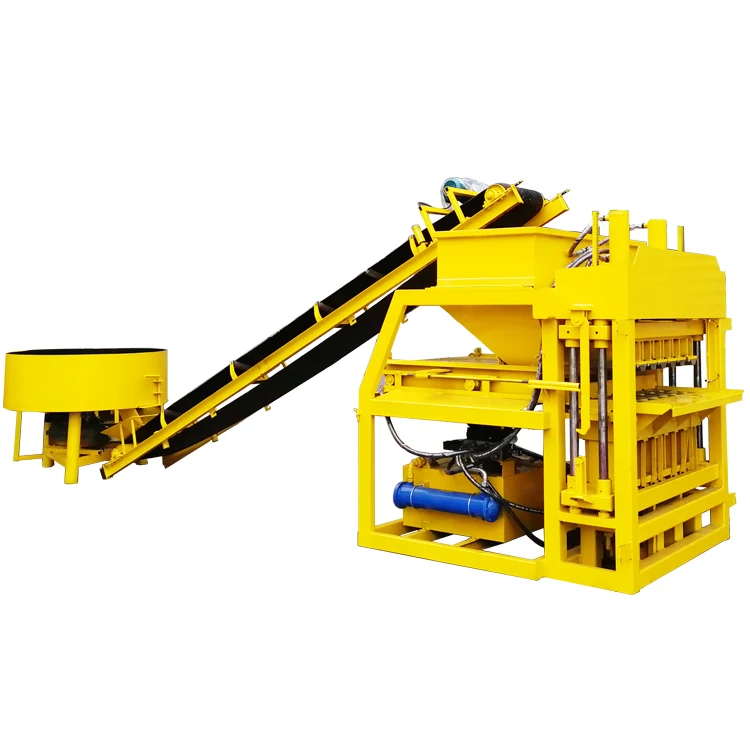
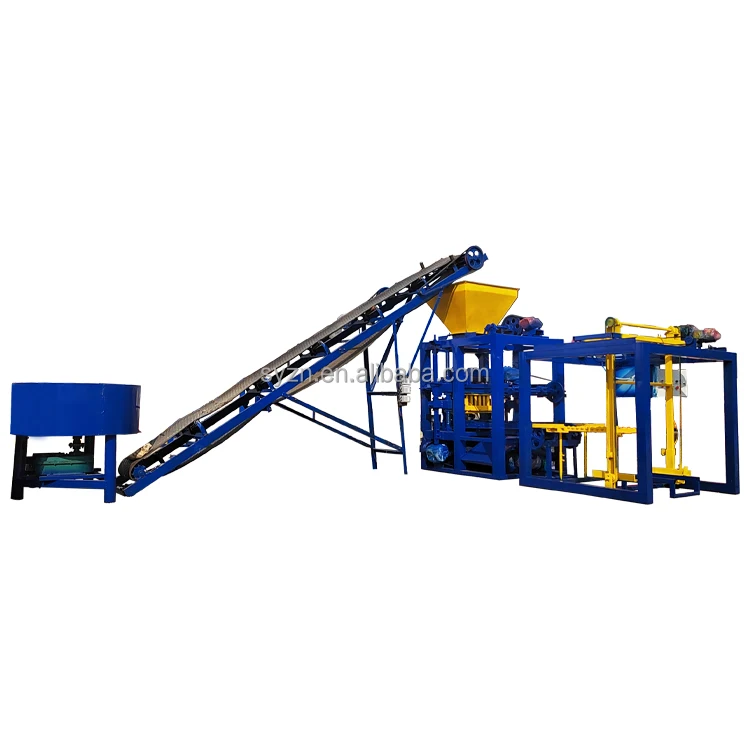
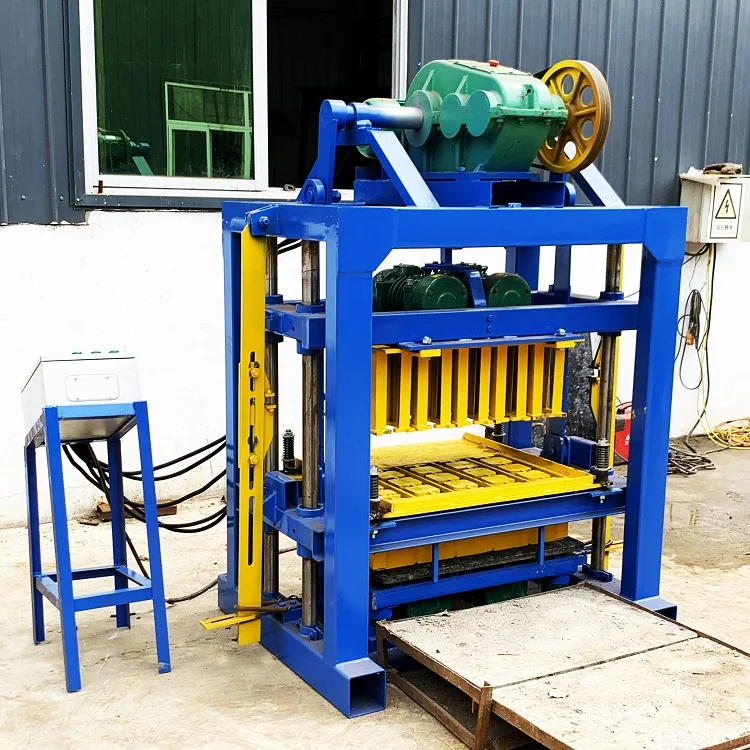
Matched System Configuration — The QTF3-20 semi-automatic stationary press is specified alongside its pallet, mould, and feeder as one integrated unit, preventing the mismatched-supplier problems that stall first-time block plants.
Technical Specifications
| Parameter |
Value |
| Model |
QTF3-20 |
| Product Type |
Stationary Block Making Machine |
| Overall Dimensions (L×W×H) |
4000 × 3500 × 2300 mm |
| Net Weight |
2870 kg |
| Total Installed Power |
17.5 kW |
| Control Style |
Semi-Automatic |
| Vibration Form |
Platform Vibration |
| Hydraulic System |
Yes (applied to drive) |
| Material Feeding |
Double layer (base and color surface feed) |
| Monitoring |
No-contact proximity switch |
| Output Capacity |
4320 pcs/day (basis to be confirmed per block format) |
| Standard Line Components |
Host press, material feeder, color feeder, pallet feeder, block conveyor, hydraulic station, electric control box |
| Mould Format Options |
Hollow block, solid standard brick, interlock brick, color paver, porous brick, park grass brick |
| Main Electrical & Hydraulic Components |
Sourced from German or established Chinese brands (verify against current build sheet) |
Application Suitability
| Application |
Material or Output Focus |
| Hollow block production for low-rise walls |
Cement, sand, and coarse aggregate blends |
| Color paver and walkway brick manufacturing |
Two-layer feed with surface pigment and base concrete |
| Interlocking landscape and retaining bricks |
Interlock moulds with fly ash or slag aggregate |
| Standard solid brick for masonry |
Cement-sand mixes with platform vibration compaction |
| Porous and grass bricks for drainage areas |
Open-void moulds with controlled aggregate grading |
| Park grass brick for permeable paving |
Cement and coarse aggregate with large-void cavity |
Why "Pieces per Day" Is the Wrong Starting Question
Capacity only matters once the block format is named.
Buyers often compare two machines on daily output numbers and assume the higher figure wins. A stationary block making machine manufacturer quoting 4320 pieces per day might be counting small solid standard bricks, while the buyer’s real product is a 400×200×200 mm hollow block that yields far fewer units per cycle. I have watched operators arrive at a new site expecting a full shift of hollow blocks, only to find the pallet slots filled with standard bricks at a pace that left the curing yard half-empty by noon. The mismatch is not a machine fault; it is a quotation that never anchored capacity to a specific format and mould [NEED_CITE: block format impact on daily output calculations]. When the QTF3-20 enters the Shiyue range conversation, the first step is always agreeing on which mould the buyer will run most days, then recalculating output from that cycle time.

Where the QTF3-20 Sits in the Full Range
The Shiyue lineup spans mobile egg-laying units at the entry end, semi-automatic stationary presses in the middle, and fully automatic lines with robotic stacking at the top. The QTF3-20 occupies the semi-automatic stationary tier, meaning it uses a fixed press with platform vibration and a dedicated pallet feeder, but still relies on manual or semi-manual pallet transfer to the curing area. This positioning suits a buyer who has outgrown a mobile machine and needs consistent multi-format output, yet is not ready to invest in the conveyors, stackers, and cubing systems that a full automatic line demands.
How This Tier Shapes Plant Layout
A stationary block making machine at this tier defines the entire floor plan. The 4000 × 3500 mm footprint of the QTF3-20 press, plus the feeder, hydraulic station, and control cabinet, sets the minimum building envelope. Buyers must also allocate space for pallet circulation and the curing racks or open yard beyond the block conveyor [NEED_CITE: typical block plant floor space allocation by automation tier]. Unlike a mobile egg-laying machine that lays blocks directly on the ground, the QTF3-20 requires pallets to carry every wet product until it gains enough green strength to stack. That requirement dictates how many pallets to purchase, what curing area to prepare, and whether a forklift or hand cart will move them.
Reading the Specs That Actually Move Production
Total installed power of 17.5 kW is modest, which means the press can run on a standard three-phase industrial supply without a dedicated transformer upgrade in most regions. Platform vibration, rather than mould-only vibration, transmits compaction force through the entire pallet surface; this produces more uniform density across wide paver formats and deep hollow blocks. The double-layer material feeding system lets the operator send a pigmented surface mix and a standard base mix in the same cycle, creating color pavers without a separate coloring line. No-contact proximity switches monitor mould and feeder positions, reducing the mechanical wear that plagues limit switches in dusty block plant environments. Hydraulic drive on the press head delivers the pressure needed for dense hollow block walls, complementing vibration to reach target compressive strength.
The Hidden Cost of Skipping Pallet and Voltage Confirmation
Buyers who focus only on the press itself often overlook two details that delay commissioning by weeks. First, pallet size must match the curing rack spacing and the forklift tine width already on site; arriving with pallets that are too wide for an existing rack forces a full rack rebuild. Second, voltage and frequency must align with the local grid before the control cabinet is wired. I once saw a semi-automatic line sit idle for three days because the control panel was configured for 50 Hz while the local supply ran at 60 Hz, and the proximity switches refused to cycle [NEED_CITE: voltage and frequency mismatch in exported machinery]. Neither issue reflects a machine defect, but both turn a smooth startup into an expensive troubleshooting trip.
Why Buyers Source This Tier Through Shiyue
Block machinery is the sole focus of the workshop, so the QTF3-20 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate vendors. Configuration starts from the buyer’s actual mix design and local aggregate, not a catalogue default that assumes materials unavailable at the destination. Mould design covers the formats the buyer’s market actually sells, including custom drawings for region-specific interlock profiles. The automation level is selectable; a buyer can begin with the QTF3-20 semi-automatic setup and add automatic stacking or pallet return later as volume grows. Installation includes on-site commissioning and operator training so the first shift runs under supervision rather than guesswork.
Documentation & Verification
- Line layout drawing showing QTF3-20 press position, pallet flow path, and curing area allocation.
- Capacity calculation sheet stating the exact block format and cycle time used for the quoted output.
- Mould drawing and format list covering every brick type the buyer intends to produce.
- Voltage, frequency, and control panel language confirmation signed off before production begins.
- Factory test record with the buyer’s specified mould installed and running.
- Hydraulic and electrical schematic for on-site troubleshooting and spare part ordering.
Installation, Commissioning & Support
- Foundation pad sized for the 4000 × 3500 mm press footprint and 2870 kg static load.
- Three-phase power supply rated for 17.5 kW total draw with a dedicated circuit breaker.
- Pallet feeder and block conveyor assembled on site to match curing yard distance.
- First-run parameter setting for vibration duration and hydraulic pressure against the buyer’s mix.
- Operator training on mould change procedure and proximity switch calibration.
- Wear parts list covering platform springs, hydraulic seals, and feeder belts for the first year.
What to Prepare Before Requesting a Quote
To size the QTF3-20 correctly within the range, share the block formats that dominate your local market, the daily volume you plan to run, and the raw materials you can source nearby. Include your site’s voltage and frequency, the language your operators need on the control display, and the pallet dimensions that fit your existing curing setup. With those details in hand, the proposal can anchor output to your actual product mix rather than a generic cycle count.
Frequently Asked Questions
Q: How does the QTF3-20 output tier compare to other models in the Shiyue range?
A: The QTF3-20 sits in the semi-automatic stationary tier, above mobile egg-laying machines but below fully automatic lines with stackers and cubing systems. It suits buyers who need multi-format production on a fixed plant without committing to the capital cost of full automation.
Q: What block format is the 4320 pieces per day figure based on?
A: That figure requires confirmation against a specific block format, material, and mould configuration. Daily output changes significantly when switching from small solid bricks to large hollow blocks, so we calculate real capacity only after the target format is agreed.
Q: What is the minimum plant footprint for a QTF3-20 setup?
A: The press itself measures 4000 × 3500 mm, but the total footprint must also accommodate the pallet feeder, block conveyor, hydraulic station, and a curing area sized for the daily pallet volume. We provide a line layout drawing to map every station.
Q: Can I start semi-automatic and move to a higher automation tier later?
A: Yes. The QTF3-20 platform supports adding automatic pallet return, stacking, or cubing equipment as production volume grows. Planning the upgrade path during the initial layout avoids costly floor plan changes later.
Q: What separates the QTF3-20 investment from the next tier up?
A: The gap is mainly in the handling equipment beyond the press. Moving to the next tier adds automatic pallet circulation, stackers, and sometimes cubing systems, which raise capital cost but reduce manual labor. The press itself remains the same proven platform.

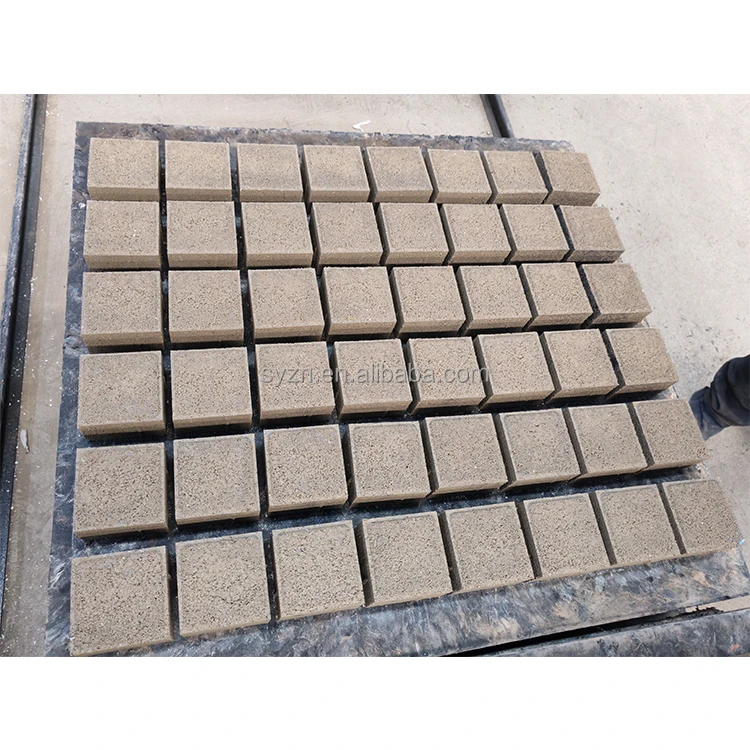
 Stationary block machine