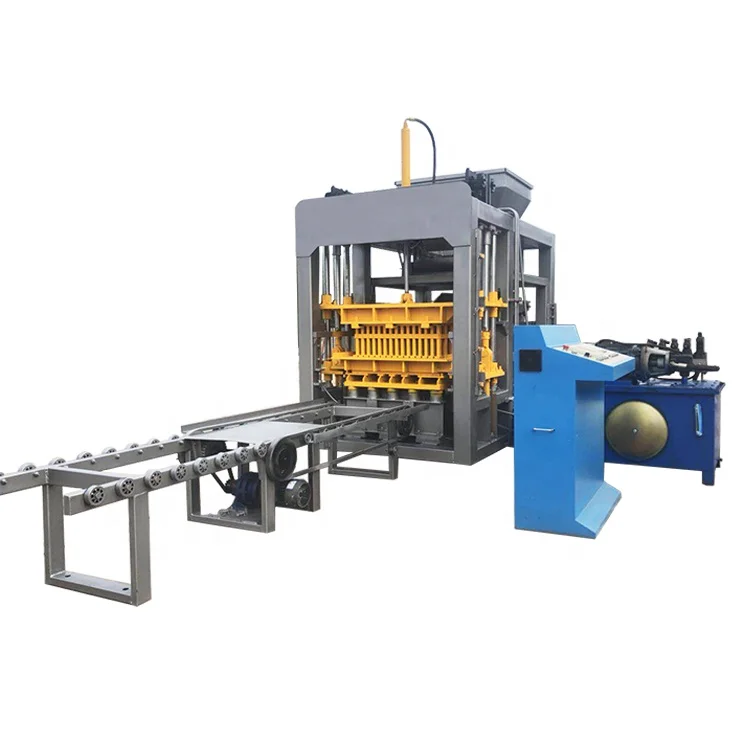
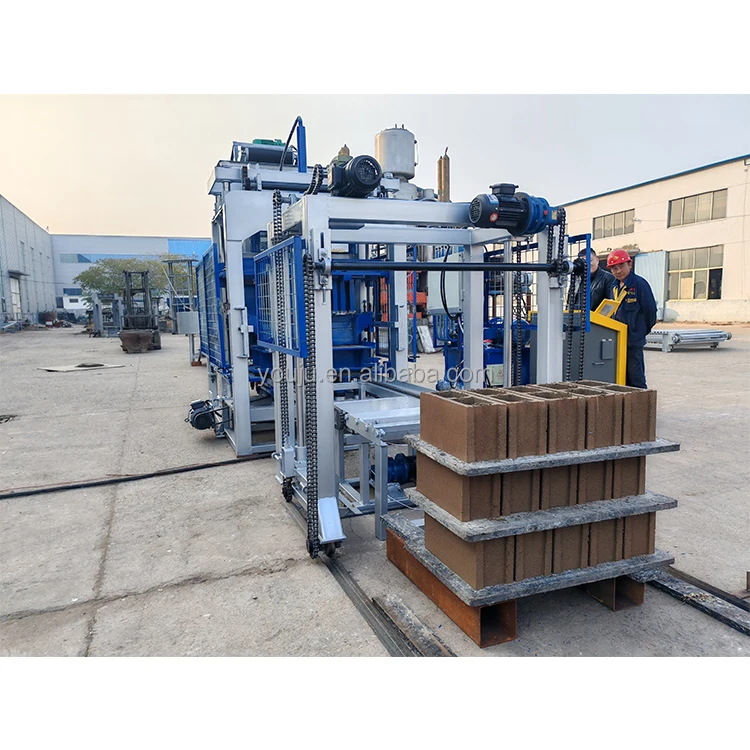
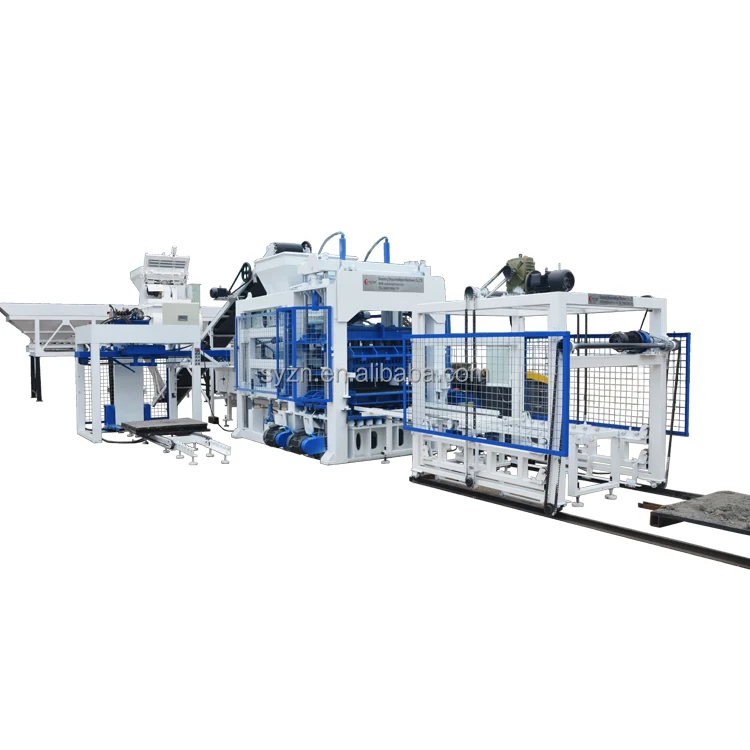
Configuration matched to your block format — the QT7-15 line is specified against the buyer’s actual mix design and target block dimensions, not a catalogue default, so capacity calculations hold up on your shop floor.
Technical Specifications
| Parameter |
Value |
| Model |
QT7-15 |
| Product Type |
Automatic Hydraulic Hollow Block Making Machine |
| Host Machine Dimensions (L×W×H) |
3200 × 2300 × 2750 mm |
| Host Machine Weight |
6 Tons |
| Molding Area |
1150 × 700 mm |
| Host Machine Power |
45 kW |
| Vibration Force |
100 kN |
| Vibration Method |
Hydraulic + Platform Vibration |
| Vibration Frequency |
2800–4500 Times/Minute |
| Pallet Size |
1150 × 700 × 25 mm |
| Molding Period (Cycle Time) |
15 Seconds (basis not stated in source) |
| Control System |
Siemens PLC with independently developed program |
| Motor Brand |
Germany SIEMENS or CE standard brand |
| Travel Switch |
France Schneider / Japan Omron |
| Voltage |
220/380/415/440V (Customized) |
| Mould Heat Treatment |
Carburizing, 54–58 HRC, lifespan >100,000 cycles |
| Batching Machine Model |
PLD1200 |
| Batching Hopper Capacity |
1200 L |
| Storage Hopper Capacity |
4 × 2.5 m³ |
| Batching Theoretical Productivity |
56 m³/h |
| Batching Precision |
±2% |
| Batching Machine Dimensions |
12000 × 2200 × 2500 mm |
| Batching Machine Weight |
4500 kg |
| Mixer Model |
JS500 |
| Mixer Charging / Discharging Volume |
800 L / 500 L |
| Mixer Production Capacity |
25 m³/h (basis not stated in source) |
| Mixer Motor Power |
18.5 kW (mixing) / 5.5 kW (windlass) / 0.75 kW (pump) |
| Maximum Aggregate Grain Size |
60 mm |
| Mixer Dimensions |
4490 × 3030 × 5280 mm |
| Mixer Weight |
2800 kg |
| Stacker Model |
SY-4 |
| Stacker Type |
Mobile pallet stack |
| Stacker Power |
3 kW |
| Automation Level |
Automatic (pallet feeder, brick receiver, hydraulic station, hydraulic trolley) |
Application Suitability
| Application |
Material or Output |
| Hollow block production for block plants |
Crushed stone, sand, cement, fly ash aggregates |
| Solid block and cement brick manufacturing |
Dense aggregate mixes with standard cement ratios |
| Paving block and kerbstone production |
High-strength concrete with fine aggregate grading |
| Color paver production (with optional color feeding) |
Pigmented face mix over standard base concrete |
| On-site housing project block supply |
Local quarry aggregate with site-adapted mix design |
Why "15-Second Cycle Time" Means Nothing Without Block Format
The cycle figure only matters once you know which block size and thickness it was measured on.
Every automatic hollow block making machine manufacturer quotes a cycle time, but that number shifts depending on whether you are pressing a thin paving block or a tall hollow block that needs longer vibration to consolidate the core. A buyer in the Middle East once received a machine rated at a fast cycle, only to find the vibration force could not fully compact the dense local aggregate his market demanded. Output dropped to less than half the quoted figure, and we spent days on-site retuning the pressure and frequency. The QT7-15 pairs 100 kN of vibration force with a 2800–4500 cycles/min frequency range specifically so the cycle can be adjusted to different block heights and mix densities rather than locked to one laboratory ideal. [NEED_CITE: vibration force requirements for different concrete block densities]

Where the QT7-15 Sits on the Stationary Range
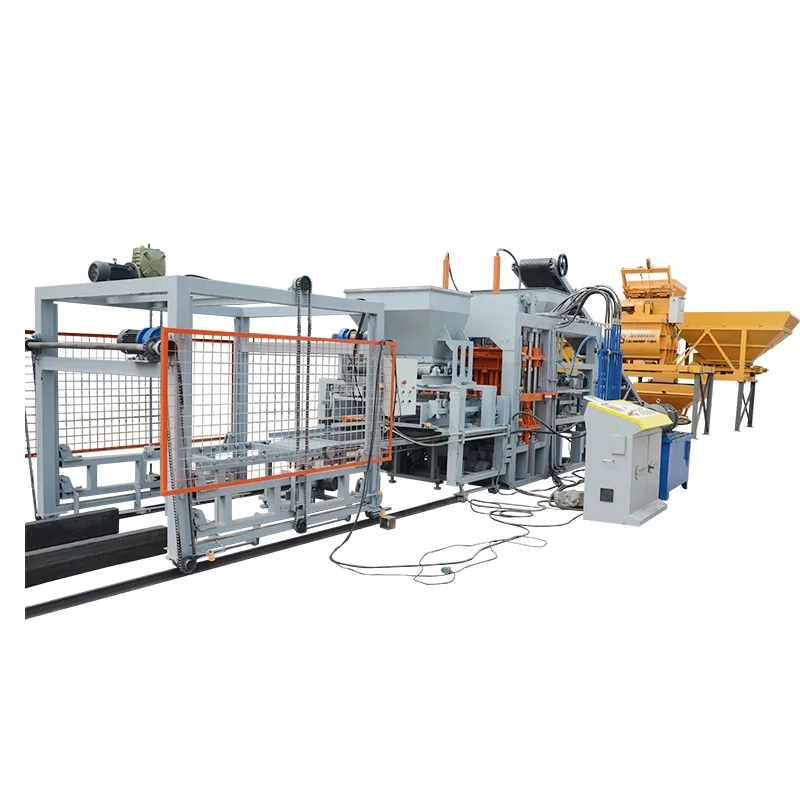
The QT7-15 occupies the upper-mid tier of our stationary block machine lineup. Below it, semi-automatic models serve smaller plants that handle pallets manually and run lower daily volumes. Above it, high-capacity lines use larger pallets and fully automated cubing systems designed for continuous three-shift operation. This model bridges the gap for buyers who have outgrown semi-automatic output but are not yet ready to commit to the footprint and capital of a top-tier plant. The 1150 × 700 mm molding area defines the ceiling: it accommodates a wide variety of hollow block, solid block, and paver formats, but it does not reach the multi-block-per-cycle counts of the largest pallet sizes in the range.
How the Full Line Connects Around the Press
An automatic hollow block making machine manufacturer must ensure every station upstream and downstream of the press keeps pace. The PLD1200 batching machine feeds three aggregate species with ±2% precision into the JS500 mixer, which discharges 500 L batches at up to 25 m³/h. If the mixer cannot recharge the press hopper fast enough, the press sits idle and cycle counts per hour drop regardless of how fast the mould closes. Downstream, the SY-4 mobile stacker lifts loaded pallets for curing, and the hydraulic trolley shuttles them to the rack area. When any one station is undersized, the bottleneck moves to the press and the buyer wonders why daily output falls short. [NEED_CITE: block plant line balancing and station cycle matching]
Reading the Specifications That Actually Shape Output
The 100 kN vibration force combined with hydraulic pressure is what determines whether a hollow block leaves the mould with uniform density or crumbles at the webs. Higher frequency alone will not consolidate a stiff, low-water mix; the hydraulic pressure must push the aggregate into the mould corners at the same time the vibration liquefies the cement paste. The 1150 × 700 mm pallet size sets the maximum mould footprint, which in turn dictates how many blocks of a given format you can press per cycle — a 400 × 200 mm hollow block fits a different count than a 200 × 100 mm paver. The Siemens PLC with a custom-developed program stores cycle recipes per format, so operators switch between block types without manually retiming every stroke. Carburized moulds at 54–58 HRC withstand the abrasion of dense aggregate over extended production runs, keeping dimensional tolerance within spec well past the initial break-in period.
The Hidden Cost of Skipping Pallet and Voltage Details
Buyers who confirm the press specs but leave pallet material and voltage open end up absorbing costs after the crate arrives. A pallet that warps under steam curing forces the stacker to jam, halting the line until an operator clears it. A 415 V machine wired into a 380 V supply runs the hydraulic pump motor at reduced torque, weakening compaction and producing blocks that fail drop tests. These problems are not defects in the automatic hollow block making machine itself — they are configuration gaps that surface only once production starts. [NEED_CITE: industrial motor performance under voltage mismatch conditions]
Why Source This Line Here
Block machinery is our single focus, which means the press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. Every configuration is set against the buyer’s actual mix design and local aggregate, not pulled from a catalogue default. Mould design covers the formats your market sells, including custom drawings when standard formats do not match. Automation is selectable: you can start with the current pallet feeder and stacker setup, then add automatic cubing later without replacing the press. Installation and commissioning include operator training so your crew can run the line independently from day one.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet covering host machine, batching, mixer, and stacker as a matched set
- Mould drawing and format list showing pieces per cycle for every block type on the 1150 × 700 mm pallet
- Voltage, frequency, and PLC display language confirmation document signed before production begins
- Factory test record with your specified mix design and block format before dispatch
Installation, Commissioning & Support
- Foundation plan sized for the 6-ton host machine and 12-meter batching conveyor footprint
- Dedicated power circuit for the 45 kW host and 18.5 kW mixer motor at your confirmed voltage
- Hydraulic station pre-filled and tested; lines disconnected for container loading and reconnected on site
- PLC program loaded with your target block recipes and display language before shipment
- Operator training covering mould change procedure, vibration frequency adjustment, and daily maintenance checkpoints
- Wear parts list identifying mould liners, hydraulic seals, and vibration motor bearings with replacement intervals
Before You Request a Quote
To size this line accurately, tell us the block formats you sell most, the daily volume your market absorbs, and the aggregate materials available within hauling distance of your plant. Confirm your site voltage, frequency, and the language your operators will read on the PLC screen. If you already have curing racks, forklifts, or a mixer in place, share those details so we can match or exclude overlapping stations.
Frequently Asked Questions
Q: How is the QT7-15 capacity calculated per block format?
A: The 15-second cycle time is a machine-level figure. Actual output depends on how many blocks fit on the 1150 × 700 mm pallet for your chosen format. We provide a capacity table listing pieces per cycle and pieces per eight-hour shift for each block type you plan to produce, so there is no guesswork about daily volume.
Q: Where does the QT7-15 sit compared to smaller and larger models?
A: It occupies the upper-mid tier of our stationary range. Semi-automatic models below it use smaller pallets and manual pallet handling. High-capacity lines above it use larger pallets and full cubing systems. The QT7-15 suits buyers scaling past semi-automatic output without needing the largest plant footprint.
Q: What workshop area does the full QT7-15 line require?
A: The host machine, batching plant, mixer, pallet feeder, stacker, and curing rack handling together require a workshop area that must be confirmed against your specific line layout. We provide a scaled floor plan showing each station, conveyor run, and operator walkway before production begins.
Q: How do I confirm voltage and PLC language before shipment?
A: During the configuration stage we send a written confirmation form listing your site voltage, frequency, motor wiring, and PLC display language. You sign off before we build, so the electrical cabinet and control screen match your local standards when the line arrives.
Q: Can I upgrade the stacking and cubing system later?
A: Yes. The QT7-15 ships with the SY-4 mobile stacker and hydraulic trolley as standard. When your volume grows, the line can accept an automatic cubing system without replacing the host machine or reprogramming the PLC from scratch.

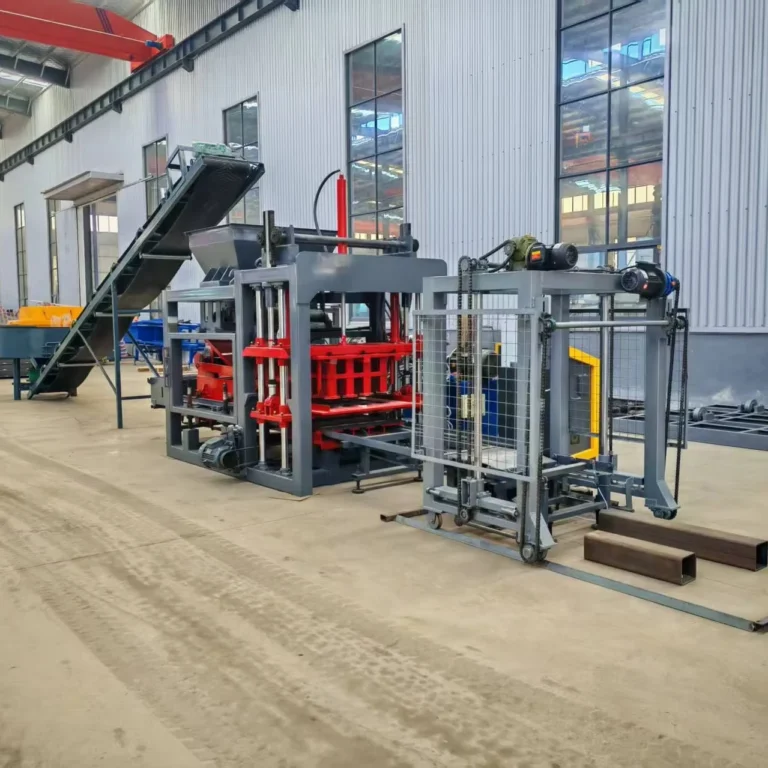 Stationary block machine