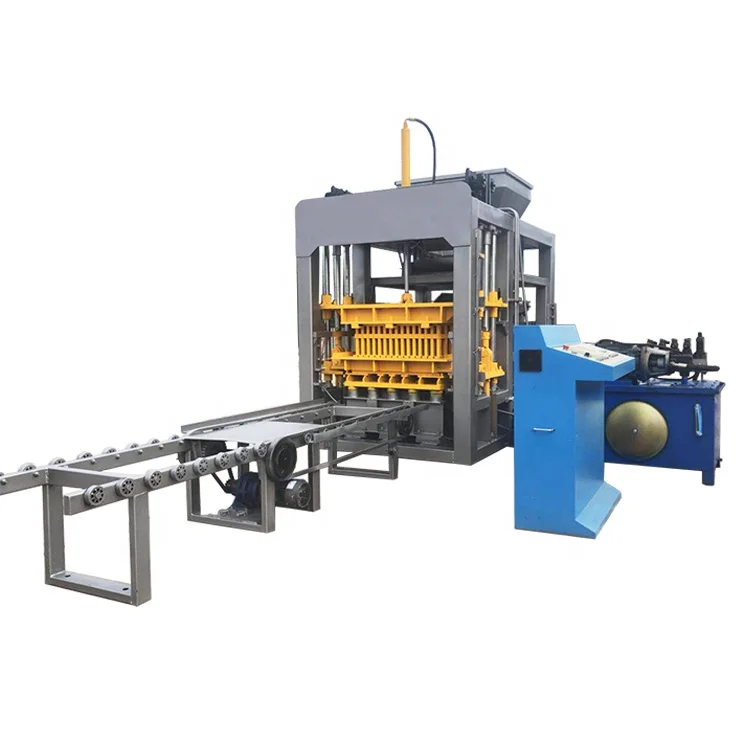
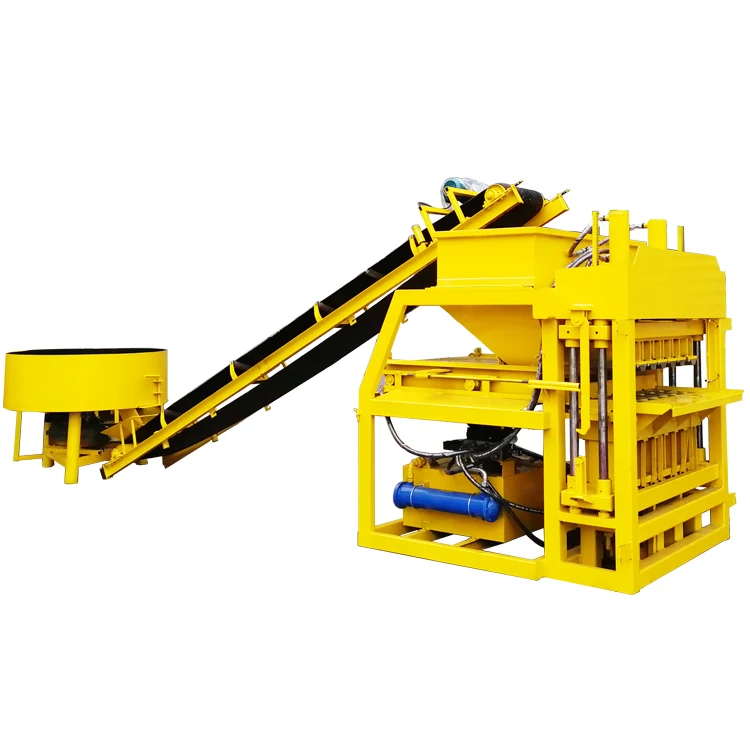
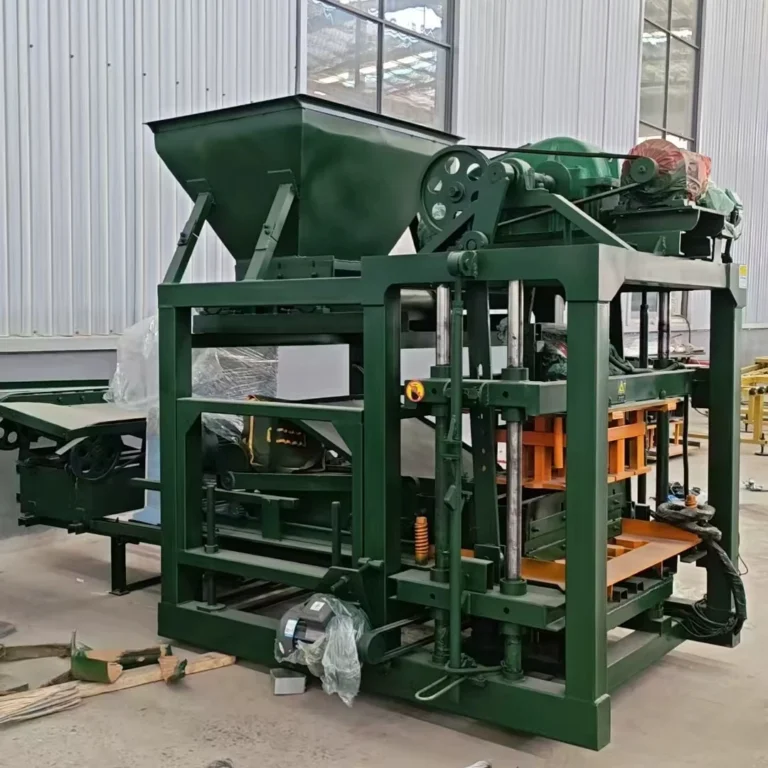
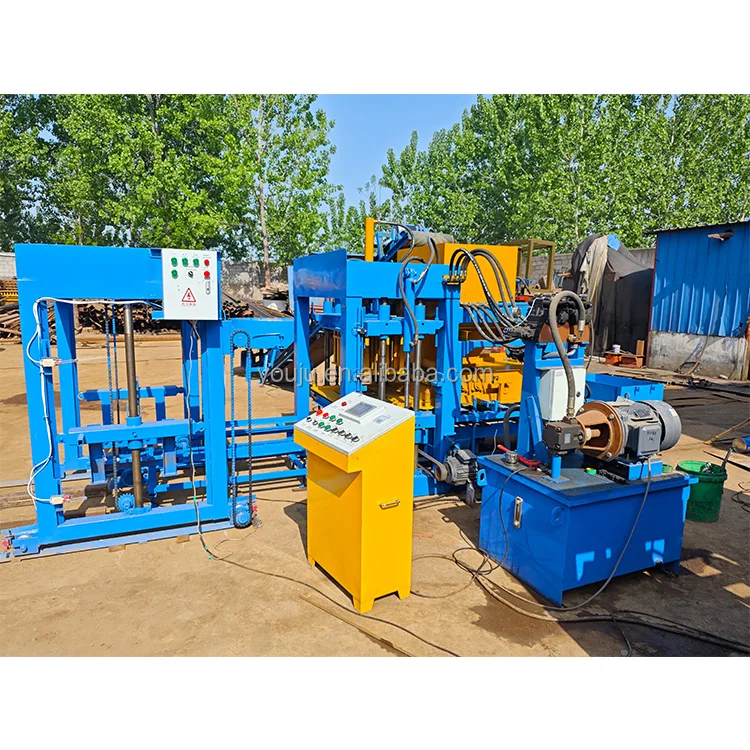
Single-focus block machinery — every station from mixer to stacking is sized against the press so the line runs without bottlenecks, not assembled from unrelated catalog pages.
Technical Specifications
| Parameter |
Value |
| Model |
QT4-15 |
| Product Type |
Stationary Block Making Machine |
| Rated Power |
27.5 kW |
| Voltage |
380V (frequency to be confirmed per target market) |
| Control System |
PLC with directional vibration logic |
| Overall Dimensions (L×W×H) |
7100 × 1600 × 2610 mm |
| Net Weight |
5 T |
| Vibration Force |
40 kN |
| Pallet Size |
1020 × 570 mm |
| Moulding Cycle |
15 s (basis not stated in source — format and material to be confirmed) |
| Mixer Model |
JS500 |
| Water Consumption |
4 T per day |
| Required Workers |
3–4 |
| Workshop Area |
150 m² |
| Automation Level |
Semi-automatic with manual pallet handling |
| Feed System |
Hopper with swing-type cutting device |
| Vibration Mode |
Table and mould synchronous; low-frequency feed, high-frequency press |
| Photoelectric Control |
Host material feed regulated by sensor |
| CE Declaration |
Available per shipment where applicable |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Crushed stone, sand, cement blends for masonry walls |
| Solid block manufacturing |
Dense aggregate mixes for load-bearing structures |
| Paving block forming |
Fine aggregate and cement for pedestrian and light-traffic surfaces |
| Small workshop output |
Standard formats at volumes matching 150 m² plant capacity |
| On-site contractor production |
Fixed-setup masonry blocks for housing and commercial builds |
Why "15-Second Cycle" Means Nothing Without the Block Format
A cycle time is only honest when the block size, wall thickness, and mix design are named beside it.
I have watched buyers in Southeast Asia sign contracts based on a single cycle number, then spend weeks realizing their local hollow block takes longer to press than the standard test piece. The vibration dwell alone shifts when you move from a 100 mm solid to a 200 mm three-hole hollow. Without the format written into the capacity table, daily output calculations fall apart before the first pallet leaves the press. [NEED_CITE: block format assumptions in capacity quotations]
The QT4-15 block machine manufacturer specification sheet we issue lists each format separately, so you see the cycle and the output it actually produces — not a best-case number from a smaller solid brick.

Mapping the QT4-15 Across the Full Stationary Range
This model occupies the entry-to-mid tier of our stationary block making lineup. Below it sits mobile and egg-laying equipment for job-site production without a fixed plant; above it are higher-output automatic lines with mechanized pallet handling and stacking. Placing the QT4-15 on this spectrum helps first-time buyers understand what semi-automatic operation looks like before committing to a fully automatic station layout. The upgrade path remains open — the same pallet size and mould interface allow a later move to automatic stacking without replacing the press itself.
Where Semi-Automatic Ends and the Line Continues
With manual pallet handling, the operator transfers wet blocks from the press to the curing rack by hand or with a simple trolley. This keeps the initial investment contained and suits workshops where labour is available and floor space is under 150 m². However, the JS500 mixer, hopper feed, and PLC-controlled vibration already operate as a coordinated sequence, so adding automatic pallet feeding and stacking later does not require rewiring the core logic. [NEED_CITE: semi-automatic to automatic upgrade considerations in block plants]
Reading the Numbers That Matter on Site
The 40 kN vibration force paired with table-and-mould synchronous shaking is the specification that most directly determines block density. Low-frequency feed distributes the mix evenly, then high-frequency vibration compacts it — the two stages must match the aggregate gradation you source locally. The 1020 × 570 mm pallet size decides how many blocks press per cycle and how the curing rack must be dimensioned. A 27.5 kW rated power draw means the plant needs a dedicated circuit sized for starting surge, not just running load. Photoelectric feed control prevents the hopper from over-filling the mould box after vibration has already settled the mix, reducing surface cracking on the finished block.
The Cost of Skipping the Configuration Conversation
Ordering a QT4-15 stationary block making machine for sale without confirming local aggregate and target format leads to vibration parameters that were set for a different mix. Blocks leave the press looking intact but crumble at the stacking rack because compaction force never matched the stone dust and cement ratio your supplier actually delivers. Pallet size mismatches show up later — your existing forklift cannot lift the rack, or the curing yard runs out of space by mid-shift. [NEED_CITE: consequences of unconfirmed block mix and pallet logistics]
Why Buyers Place Repeat Orders Here
Block machinery is our single focus, so the press, mould, pallet, and handling equipment are specified as one matched system rather than sourced from separate vendors. We set the configuration against your actual mix design and local aggregate, not a catalogue default. Mould design covers the formats your market sells, with custom drawings available. Automation level starts where your budget and labour market sit, with a documented upgrade path. Installation includes on-site commissioning and operator training so the first production shift runs with supervision, not guesswork.
Documentation & Verification
- Line layout with capacity per block format for the QT4-15
- Machine specification sheet listing confirmed voltage and frequency
- Mould drawing set covering every format in your initial order
- Pallet specification matched to your curing area dimensions
- Factory test record showing vibration force against your mix sample
- Operation and maintenance manual in your requested language
Installation, Commissioning & Support
- 150 m² workshop with level concrete slab to suit 7100 × 1600 mm footprint
- Dedicated 380V circuit rated for 27.5 kW plus JS500 mixer starting surge
- Press arrives partly assembled; hopper and PLC cabinet bolt on site
- First-run vibration tuning matched to your aggregate and block format
- Operator training covers mould change, feed adjustment, and daily checks
- Wear parts list with reorder codes for vibration springs and hopper liners
What to Prepare Before You Send an Inquiry
Share the exact block formats your market demands, the aggregate sources within hauling distance of your plant, and your daily output target per format. Include the voltage and frequency standard in your country, the PLC display language your operators read, and the curing area dimensions you already have or plan to build. This lets us return a capacity table that reflects your actual production day, not a generic estimate.
Frequently Asked Questions
Q: What block format is the 15-second cycle based on, and how does output change for other sizes?
A: The published cycle is a reference point; actual time varies with block wall thickness, aggregate size, and target density. We issue a capacity table listing each format you plan to produce — hollow, solid, and paver — with its own cycle and daily output so your production planning starts from realistic numbers, not a single best-case figure.
Q: Where does the QT4-15 sit in your full machine range, and what is the upgrade path?
A: It occupies the entry-to-mid tier of our stationary lineup, with manual pallet handling keeping initial costs contained. The press shares the same pallet interface and mould mounting as our higher-tier automatic models, so adding automatic pallet feeding and stacking later is a line extension rather than a full replacement.
Q: Can voltage, frequency, and PLC language be configured before shipment?
A: Yes. We confirm your country’s electrical standard and operator language during the quotation stage. The PLC program, motor winding specification, and control cabinet labeling are all set to match before the factory test, so commissioning on arrival focuses on block quality rather than electrical rework.
Q: Is pallet handling and curing equipment included or separate?
A: The QT4-15 as quoted is semi-automatic, meaning pallet transfer and stacking are handled manually. Pallet racks, curing carts, and any future automatic stacking station are specified separately but dimensioned to the same 1020 × 570 mm pallet so every station in the line aligns from day one.

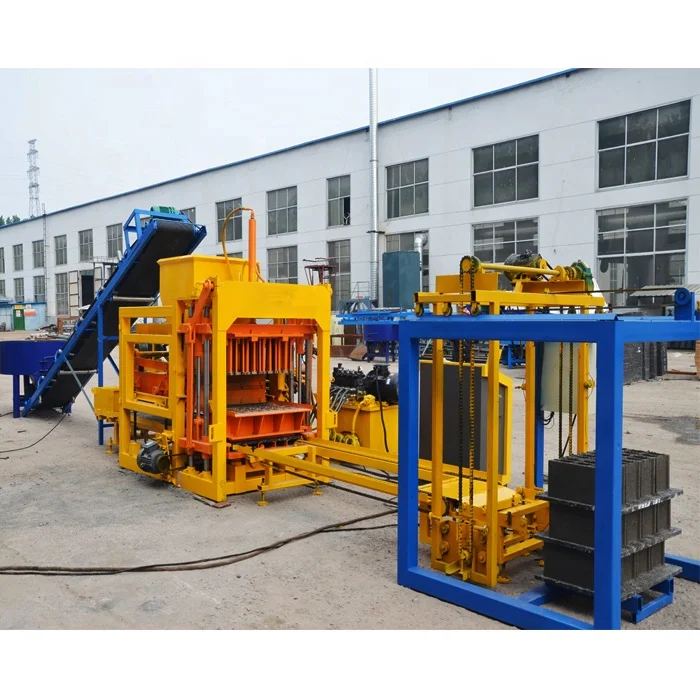
 Stationary block machine