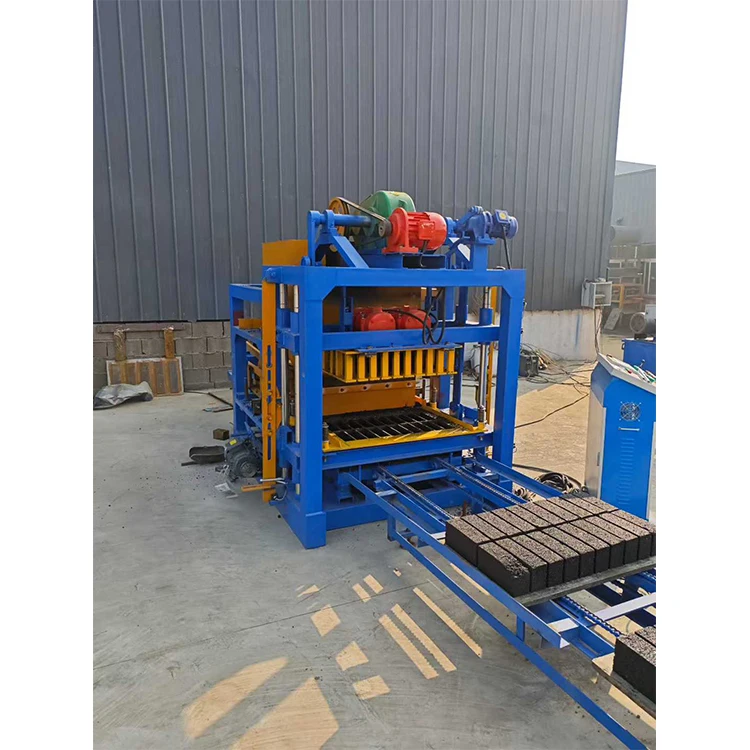
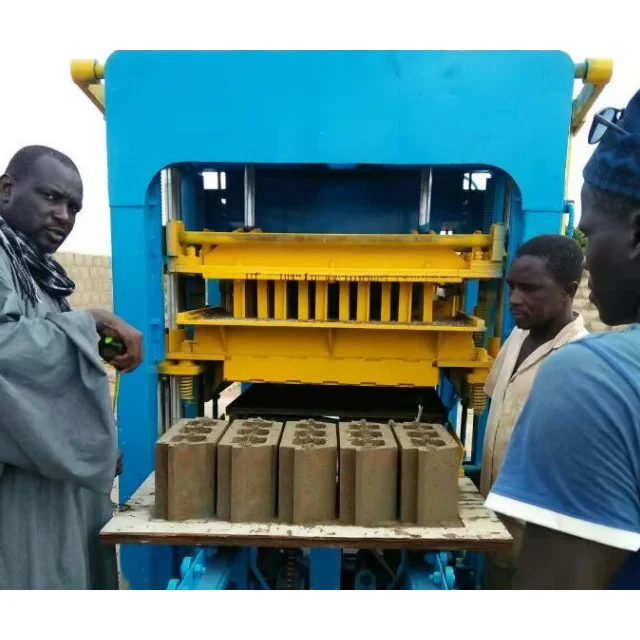
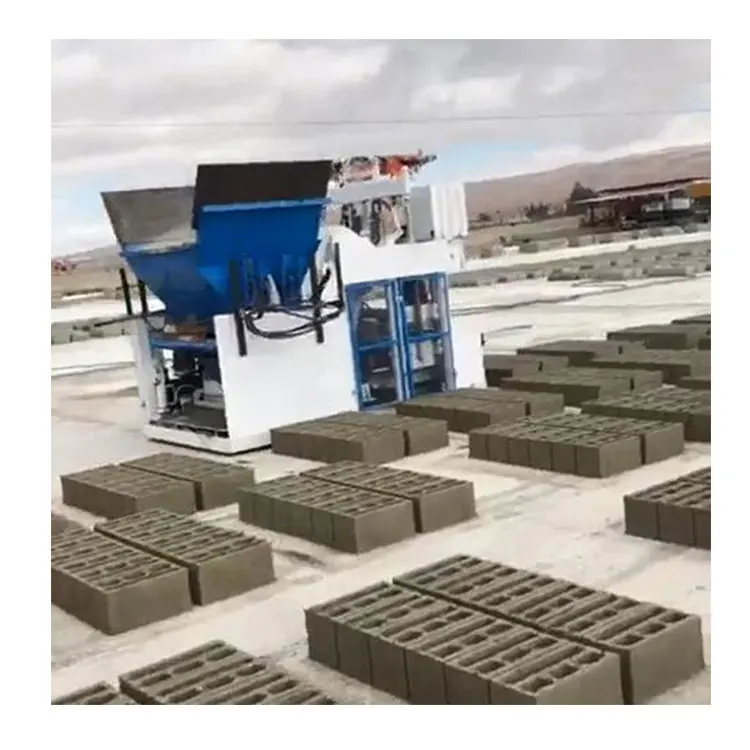
Matched System Configuration — QT10-15 block machine, mould, pallet, and handling are specified together against your actual target format and curing setup, not pulled from separate catalogue defaults.
Technical Specifications
| Parameter |
Value |
| Model |
QT10-15 |
| Product Type |
Fully Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
9350 × 2320 × 2950 mm |
| Rated Hydraulic Pressure |
21 MPa |
| Main Vibration Form |
Platform vibration |
| Vibration Frequency |
4500 – 5100 r/min |
| Pallet Size |
1100 × 900 mm |
| Molding Cycle |
15 – 25 s |
| Forming Height Range |
40 – 250 mm |
| Moulding Area |
1025 × 810 mm |
| Overall Power |
44 kW |
| Mixer Model |
JS750 |
| General Water Consumption |
12 T/day |
| Voltage |
Customized to local request |
| PLC Control Unit |
Mitsubishi (Japan) |
| Hydraulic Unit |
Jiugang (Taiwan) |
| Switches |
Omron (Japan) |
| Electrical Elements |
Schneider (France) |
| Host Machine and Mixer Motor |
Siemens (Germany) |
| Mould Treatment |
High-temperature carburizing heat treatment |
| Output – Hollow Block 400×200×200 mm |
14,400 – 19,200 pcs/8 h (basis: 10 pcs/mould) |
| Output – Hollow Block 400×150×200 mm |
17,280 – 23,040 pcs/8 h (basis: 12 pcs/mould) |
| Output – Solid Brick 240×115×90 mm |
74,880 – 99,840 pcs/8 h (basis: 52 pcs/mould) |
Application Suitability
| Application |
Material or Output |
| Hollow block production for load-bearing walls |
Crushed stone, cement, and fly ash mixes on 1100×900 mm pallets |
| Solid brick manufacturing for masonry |
Concrete and cement blends at high-pressure hydraulic compaction |
| Paver and interlocking brick runs |
Aggregate-rich mixes with tight dimensional tolerance requirements |
| Curbstone forming for road and landscape projects |
High-density concrete with extended vibration and pressure cycles |
| Fly ash brick production for cost-sensitive housing |
Fly ash, lime, and cement combinations with adjusted moisture content |
What "1800 Pieces per Hour" Leaves Out About Block Format
A cycle rate is meaningless unless it names the exact block format, mould cavity count, and pallet size behind the number.
Many buyers receive a quotation that quotes the highest possible output figure—usually based on a small solid brick with a high cavity count per mould—and then wonder why their actual daily production of hollow blocks falls far short. The QT10-15 automatic block machine specification sheet ties every output number to a specific format: 14,400–19,200 pieces per eight-hour shift for 400×200×200 mm hollow blocks, and 74,880–99,840 for 240×115×90 mm solid bricks. These two figures are not interchangeable. A plant planned around the solid brick number but actually running hollow blocks will find its curing yard and forklift logistics sized incorrectly from day one. I have seen buyers commit to a curing area based on one output figure, only to discover during commissioning that their real product mix demands a completely different yard layout [NEED_CITE: block plant capacity planning based on target format].

Mapping the QT10-15 to the Complete Machine Range
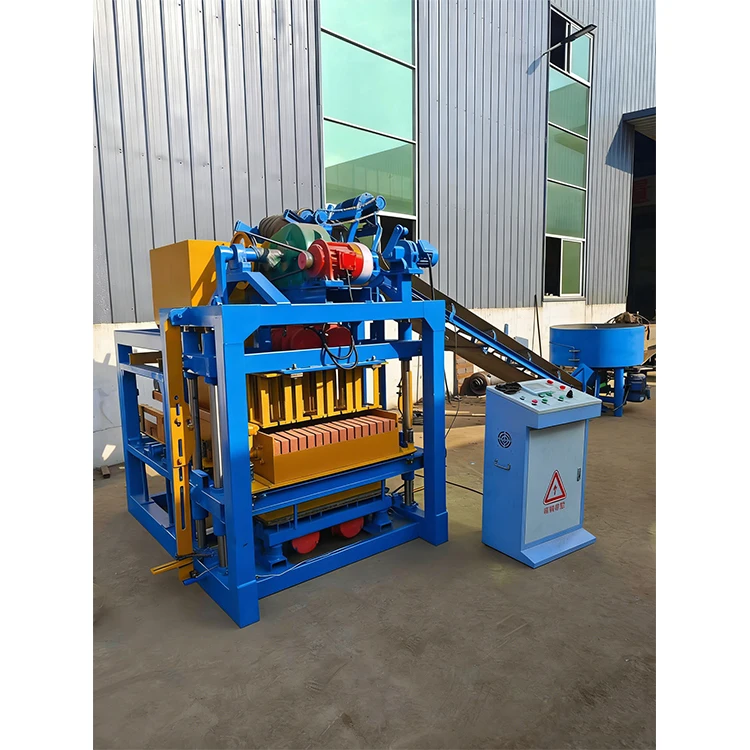
The QT10-15 sits at the high-capacity end of the fully automatic block machine lineup, designed for production plants that need continuous, high-volume output across multiple block formats. Where semi-automatic models require manual pallet feeding and hand-stacking at the press exit, this model integrates automatic pallet circulation, stacking, and cubing into a single control loop managed by the Mitsubishi PLC. The large 1025×810 mm moulding area and 1100×900 mm pallets give each cycle a higher piece count, which is why the machine suits buyers moving from workshop-scale production to a dedicated plant operation.
How Automation Level Defines Plant Footprint and Labour
Choosing between semi-automatic and fully automatic is not just a price decision—it determines how many operators stand on the line and how much floor space the stacking and curing zones consume. The QT10-15 block machine for sale as a fully automatic system requires dedicated space for the pallet return conveyor, automatic stacker, and curing rack handling equipment. A buyer starting with a smaller workforce and a compact curing area may begin with a semi-automatic configuration on the same press and upgrade the pallet and stacking stations later. This modular upgrade path means the initial investment does not lock the plant into a fixed automation ceiling.
Reading the Engineering Numbers Behind Consistent Block Density
Hydraulic pressure and vibration force must work together to achieve uniform block density—pressure alone compresses the mix from the top, while vibration settles the aggregate into voids from the platform below. The QT10-15 delivers 21 MPa of rated hydraulic pressure alongside platform vibration at 4500–5100 r/min. When these two forces are correctly matched to the buyer’s specific aggregate gradation and cement content, the resulting block has consistent compressive strength across every cycle. The 15–25 second molding cycle range reflects the adjustment window: lighter mixes with high fly ash content may need longer vibration, while coarse aggregate mixes compact faster under peak pressure. The JS750 mixer feeds a controlled volume per cycle, and the 44 kW overall power budget covers both the press and mixer motors without requiring a separate electrical sub-panel. Moulds undergo high-temperature carburizing heat treatment to resist the abrasive wear of dense concrete mixes over extended production runs [NEED_CITE: carburizing heat treatment for mould wear resistance].
The Cost of Skipping Voltage Confirmation Before Production
A three-week commissioning delay is the real-world price of a single unchecked line on the specification sheet. One fully automatic block machine was shipped to a site where the local supply was 380 V at a frequency that did not match the motor nameplate. The on-site electrician could not start the Siemens host motor, and a transformer had to be sourced locally before the line could run. Since then, every QT10-15 configuration sheet requires written confirmation of voltage, frequency, and PLC display language before the machine enters production. The Omron switches and Schneider electrical elements are sourced for the confirmed voltage spec, and the Mitsubishi PLC display is set to the buyer’s operating language so the control panel is readable from the first power-on [NEED_CITE: industrial machinery voltage and frequency confirmation prior to export].
Why Buyers Source the QT10-15 Here
Block machinery is the single manufacturing focus, which means the QT10-15 press, mould, pallet, and handling equipment are engineered as one matched system rather than assembled from unrelated suppliers. Machine configuration starts from the buyer’s target block format, local aggregate, and mix design—not from a catalogue default page. Mould design and supply cover every format the buyer’s market actually sells, including custom mould drawings when standard cavity layouts do not match the local product range. Automation level is selectable, so a buyer can commission the QT10-15 in semi-automatic mode and add automatic stacking or cubing stations as production volume grows. Installation and commissioning support includes operator training on the Mitsubishi PLC, ensuring the local crew can run the machine independently after the technician departs.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format assumed for each output tier
- Machine specification sheet covering hydraulic, vibration, and electrical parameters for your confirmed voltage
- Mould drawing and format list showing cavity count and block dimensions per pallet cycle
- Factory test record on your specific block format and mix design before dispatch
- Voltage, frequency, and PLC display language confirmation document signed before production
- Operation and maintenance manual with wear parts and mould replacement intervals
Installation, Commissioning & Support
- Foundation plan sized to the QT10-15 overall dimensions of 9350 × 2320 × 2950 mm and dynamic vibration loads
- Dedicated power circuit rated for 44 kW total load with confirmed voltage and frequency at the panel
- Pallet size and material verified against your existing curing yard layout and forklift fork dimensions
- First-run commissioning with hydraulic pressure and vibration frequency adjusted to your local aggregate and mix
- Operator training on the Mitsubishi PLC interface, including mould change procedures and fault diagnostics
- Wear parts and hydraulic seal list provided with recommended replacement intervals per production hour count
Starting the Conversation on Your Plant Configuration
Before we can size the QT10-15 to your project, we need a clear picture of the block formats your market demands, the daily output target for each format, and the aggregate materials available in your region. Share your site voltage and frequency, the PLC display language your operators read, and whether your curing yard and forklift fleet are already in place or still being planned. If you are replacing an existing machine, let us know your current pallet size so we can confirm compatibility with the 1100 × 900 mm pallets the QT10-15 uses.
Frequently Asked Questions
Q: How does the 15–25 second molding cycle translate to real daily output for my specific hollow block design?
A: The QT10-15 molding cycle varies within the 15–25 second range depending on your mix design and block format. A 400×200×200 mm hollow block with 10 cavities per mould yields 14,400–19,200 pieces per eight-hour shift, but your actual output depends on the specific cycle time your aggregate and cement ratio require. We calculate the exact cycle and daily figure during the configuration proposal.
Q: What plant footprint is required for the QT10-15 and its supporting automatic stacking equipment?
A: The press itself measures 9350 × 2320 × 2950 mm, but a fully automatic configuration adds the pallet return conveyor, automatic stacker, and curing rack handling stations. The total line footprint depends on your chosen automation level and pallet circulation layout. We provide a complete line drawing with all station positions during the proposal stage.
Q: Where does the QT10-15 sit in the investment range compared to semi-automatic or mobile options?
A: The QT10-15 is positioned at the high-capacity automatic tier of our block machine range, requiring a higher initial outlay than semi-automatic or mobile egg-laying machines but delivering substantially greater output per shift. Investment level also depends on the supporting equipment you include—pallet handling, stacking, and curing systems each add to the total line cost.
Q: Can the automation level be configured to start semi-automatic and upgrade later?
A: Yes. The QT10-15 press can be commissioned with manual pallet handling and stacking first, then upgraded with automatic pallet feeding and cubing stations as your production volume and workforce capacity grow. The Mitsubishi PLC control is pre-wired to accommodate these additions without replacing the main control unit.
Q: How are hydraulic pressure and vibration force matched to my local aggregate and mix design?
A: The 21 MPa hydraulic pressure and 4500–5100 r/min platform vibration are adjusted during commissioning based on your specific aggregate gradation, cement content, and target block strength. Coarse, dense mixes typically need higher vibration frequency and longer compaction time, while lighter fly ash blends compact effectively at lower settings within the available range.

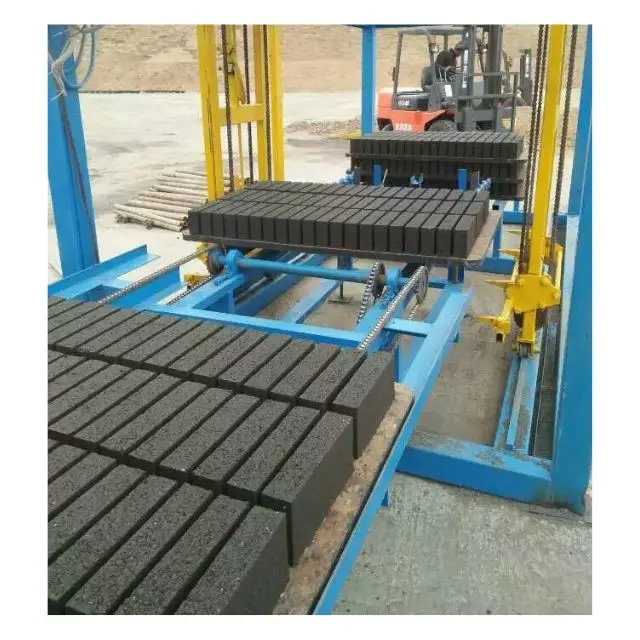
 Automatic block machine