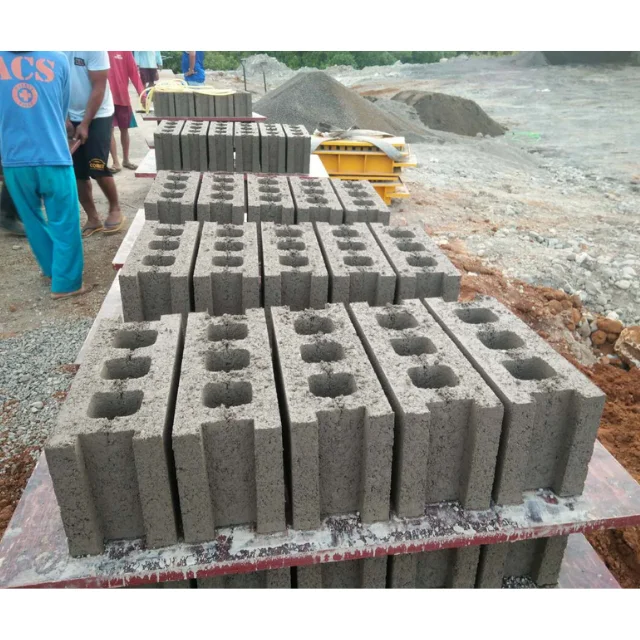
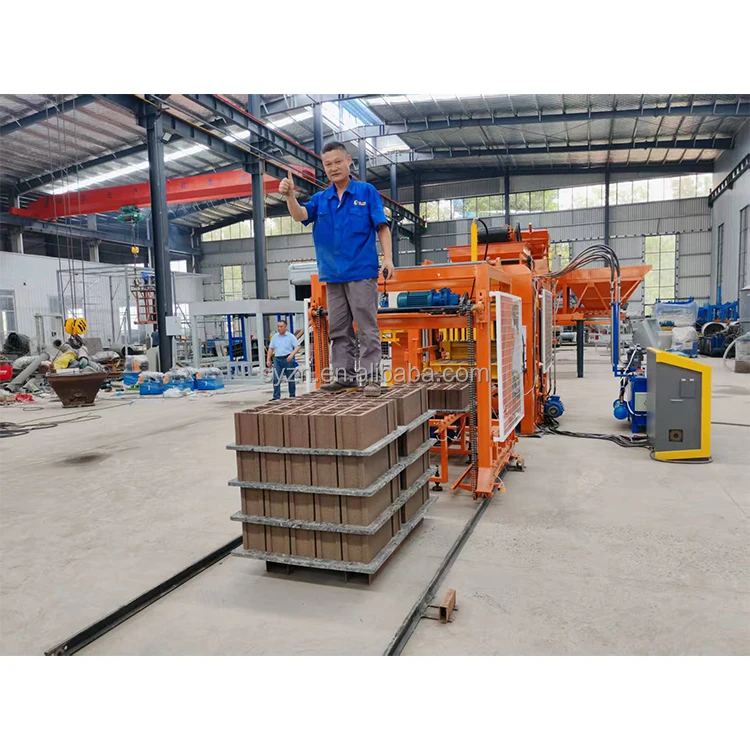
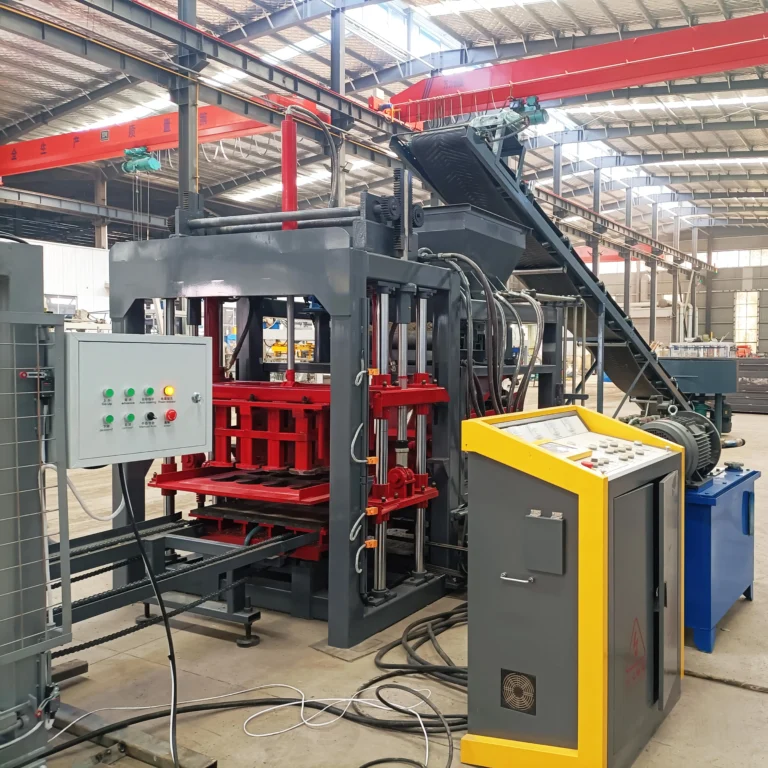
Specified as a Matched System — the QT4-18 is configured with its mould, pallet and mixer as one line, not assembled from disconnected components, so cycle times align and the press is never left waiting for upstream equipment.
Technical Specifications
| Parameter |
Value |
| Model |
QT4-18 |
| Product Type |
Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
3900 × 1600 × 2300 mm |
| Total Weight |
3 T |
| Rated Power |
24 kW |
| Exciting Force |
40–50 kN |
| Molding Cycle |
15–25 s |
| Pallet Size |
850 × 550 × 25 mm |
| Vibration Type |
Bed mould vertical vibration + upper mould compression vibration |
| Hydraulic Station |
Equipped |
| Mixer Model |
JQ350 |
| Automation Level |
Semi-automatic |
| Applicable Products |
Hollow block, solid brick, paver, curbstone |
| Raw Materials |
Crushed stone, sand, cement, dust, fly ash |
| Output Capacity |
1200–1680 pcs/hr (based on 400×200×200 mm hollow block, 4 pcs/mould) |
| Output Capacity |
1800–2400 pcs/hr (based on 400×150×200 mm hollow block) |
| Output Capacity |
3240 pcs/hr (based on 240×115×53 mm solid brick) |
| Daily Output (8 hr) |
9600–13440 pcs (400×200×200 mm hollow block) |
| Daily Output (8 hr) |
14400–19200 pcs (400×150×200 mm hollow block) |
| Daily Output (8 hr) |
16200–19440 pcs (240×115×53 mm solid brick) |
| Standards |
CE (where applicable) |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Crushed stone, sand, cement and fly ash for masonry walls |
| Solid brick production |
Dense aggregate mix for structural and infill applications |
| Paver production |
Fine aggregate and cement for walkways and driveways |
| Curbstone production |
Coarse aggregate blend for road and infrastructure edging |
| On-site block plant |
Locally sourced aggregate with portable semi-automatic line setup |
What "1200 Pieces per Hour" Actually Means for Your Block Format
Capacity figures are meaningless without the block format attached to them.
Most concrete block making machine for sale quotations lead with a single headline output number. That number is almost always based on a standard hollow block, and it drops significantly when you switch to smaller formats or denser mixes. I have watched buyers sign off on a machine expecting one throughput, only to discover during commissioning that their actual paver cycle runs considerably slower than the quoted figure. The QT4-18 output data on this page is listed per block format so you can match the machine to the product your market demands, not a catalogue default [NEED_CITE: block machine capacity claims and format dependency].

Where the QT4-18 Sits in the Full Machine Range
The SHIYUE range covers mobile egg-laying machines at the entry level, semi-automatic lines like the QT4-18 in the mid-tier, and fully automatic plants with robotic stacking at the top. This concrete block making machine for sale targets buyers who have outgrown mobile production but are not yet ready to commit the floor space and capital a fully automatic line requires. The semi-automatic configuration keeps the initial investment contained while leaving a clear path to add automatic pallet feeding and stacking later.
Planning the Line Around the Press, Not Just the Press
A block machine is only as productive as the slowest station connected to it. The JQ350 mixer, material feeding, pallet return and stacking must all be timed so the QT4-18 press completes its 15–25 second cycle without idle gaps. When the mixer batch size is too small for the press hopper, the machine pauses between cycles and the quoted throughput is never reached. Line layout work before purchase prevents this mismatch [NEED_CITE: production line cycle time synchronization principles].
Vibration, Pressure and the Density Equation
Block strength comes from two forces working together: the bed mould vertical vibration settles the aggregate into the mould cavity, while the upper mould compression vibration and hydraulic pressure compact it from above. The 40–50 kN exciting force on the QT4-18 is matched to the hydraulic station pressure so that hollow blocks achieve wall density without cracking at the webs. If vibration force is too high relative to hydraulic pressure, blocks fracture at demoulding. If pressure dominates, density is uneven from top to bottom. Both parameters must be set against your specific aggregate grading and cement ratio.
When Semi-Automatic Becomes the Bottleneck
Semi-automatic operation means pallet handling and stacking still rely on manual labour. In a small plant producing under 10,000 hollow blocks per shift, one or two operators manage the flow without issue. Push beyond that volume and the pallet return pace starts dictating press speed — the machine waits while workers carry cured pallets back to the feed end. Buyers who underestimate their second-year volume often find themselves replacing a machine they have barely paid off [NEED_CITE: block plant capacity planning and automation threshold].
Why This Range Carries the Weight of One Focus
Block machinery is the only product line here, which means the QT4-18 press, its moulds, pallets and handling equipment are specified together rather than sourced from separate vendors and forced to fit. Configuration is set against your actual mix design and local aggregate, not a generic template. Mould drawings are provided per format, including custom profiles if your market demands a non-standard block. Voltage, frequency and PLC display language are confirmed in writing before production starts — a discipline I adopted after a Spanish-speaking operator in Peru stalled for four days on an English-only interface. Installation support includes operator training so the first production run is not a learning exercise.
Documentation & Verification
- Line layout with capacity calculation stating the block format assumed for each figure
- Machine specification sheet with vibration force and hydraulic pressure ratings
- Mould drawing and format list covering hollow, solid, paver and curbstone profiles
- Pallet specification matched to your curing area dimensions and forklift capacity
- Voltage, frequency and control language confirmation document before production
- Factory test record on your target block format before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 3900 × 1600 mm footprint with vibration isolation provisions
- Dedicated power circuit rated for 24 kW continuous draw at confirmed voltage and frequency
- Machine arrives partially assembled; press frame, hydraulic station and mixer bolt on site
- First-run parameter setting for cycle time, vibration duration and hydraulic pressure per mould
- Operator training on mould change procedure, pallet loading sequence and daily maintenance checks
- Wear parts list covering hydraulic seals, vibration springs and mould liners with reorder references
Starting the Conversation with the Right Details
To size the QT4-18 line correctly, share the block formats your market actually buys, the daily volume you need per format, and the aggregate sources available within hauling distance of your site. Confirm your local voltage and frequency, the language your operators read, and whether your curing yard uses pallets you already own or needs new ones specified. With that information, a layout and per-format capacity calculation can be drafted before any commercial discussion begins.
Frequently Asked Questions
Q: How is the QT4-18 output verified per block format, and what cycle time applies?
A: Output figures are calculated from the 15–25 second molding cycle multiplied by the number of cavities per mould. For a 400×200×200 mm hollow block with 4 cavities, that yields 1200–1680 pieces per hour. Smaller formats like solid bricks have more cavities per cycle, raising the count. The capacity calculation document provided with your quotation states the exact assumption for each format.
Q: When should a buyer step up to a fully automatic model instead of the QT4-18?
A: The threshold is usually when daily hollow block volume consistently exceeds what two operators can pallet-handle manually within a standard shift. If your second-year projection shows sustained high output or you plan to run multiple formats with quick changeovers, a fully automatic line with robotic stacking removes the labour bottleneck and protects consistency across shifts.
Q: What voltage, frequency and control language options exist, and how are they confirmed?
A: The QT4-18 can be configured for common industrial voltages and frequencies across export markets. The PLC display language is set before production — not at commissioning. You receive a written confirmation document listing voltage, frequency and language, which you sign off before the machine enters assembly. This prevents the interface delays I have seen cost buyers days on site.
Q: Which pallet material and quantity are recommended for this machine?
A: Pallet size is fixed at 850 × 550 × 25 mm. Material — typically bamboo, PVC or steel — depends on your curing method and local climate. The quantity you need is calculated from your daily output, curing duration and return cycle. Using pallets from an existing inventory is possible if they match the dimension; a pallet specification sheet is provided to verify compatibility before you order.

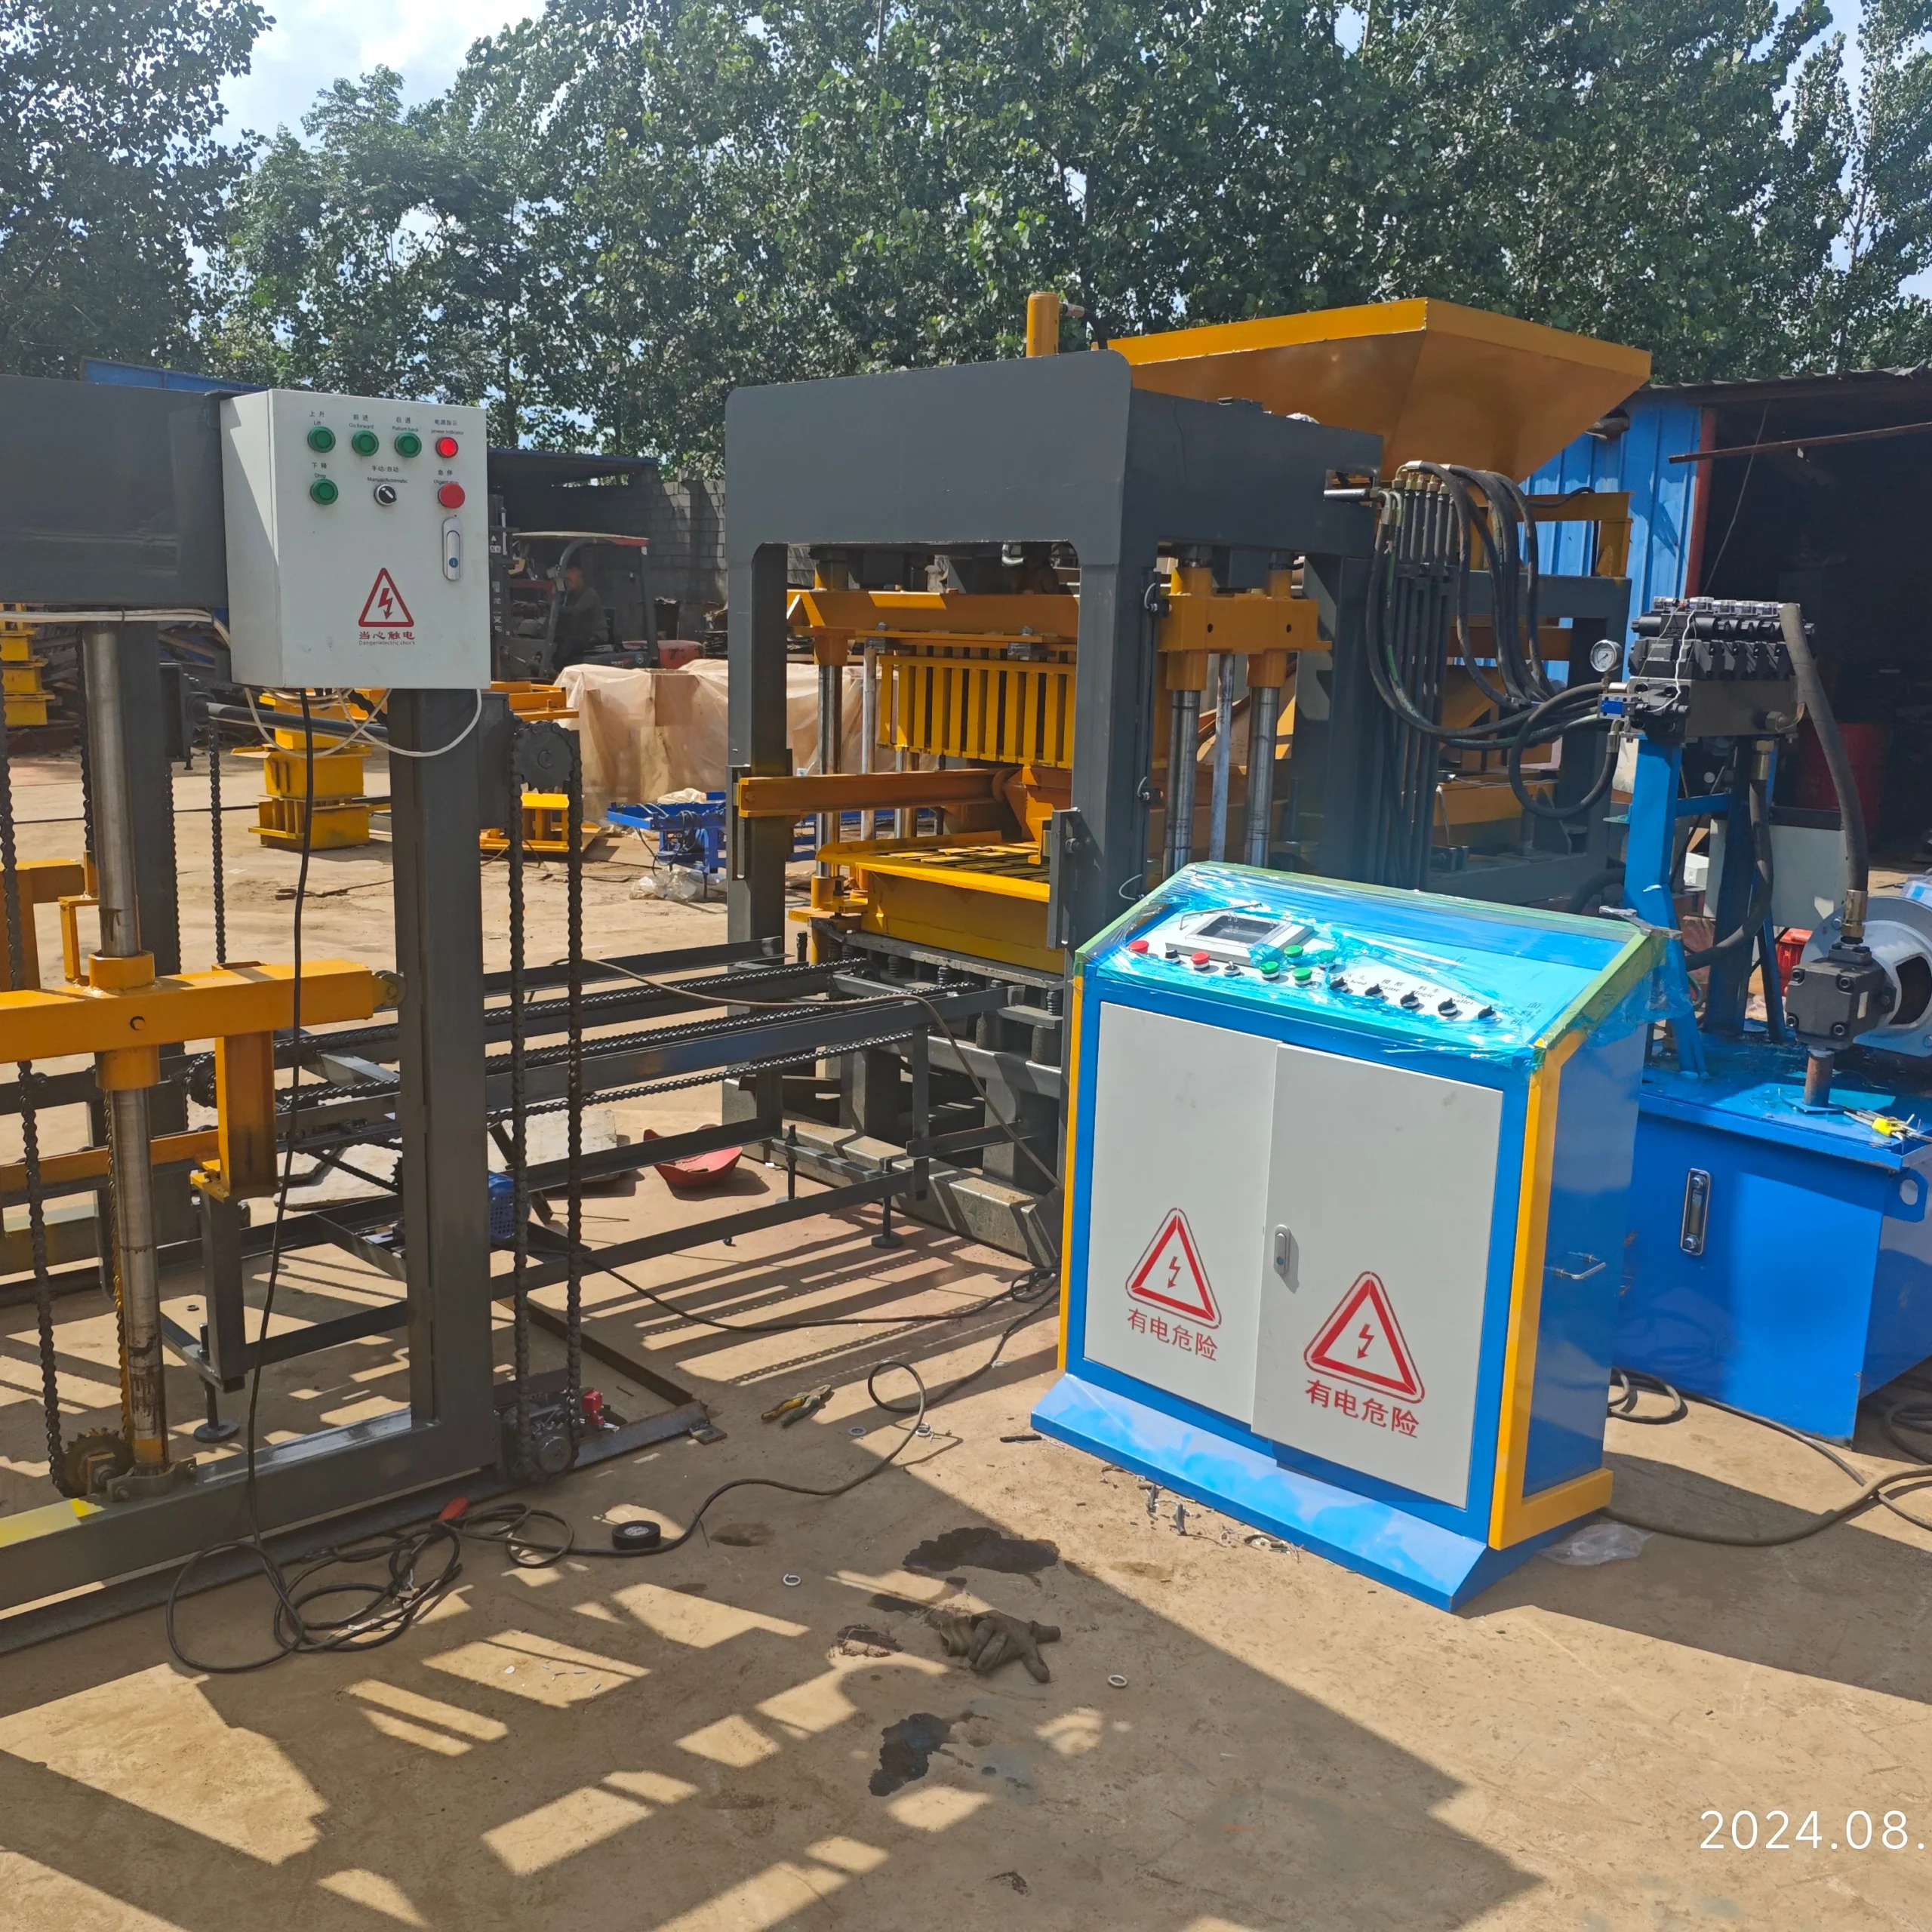
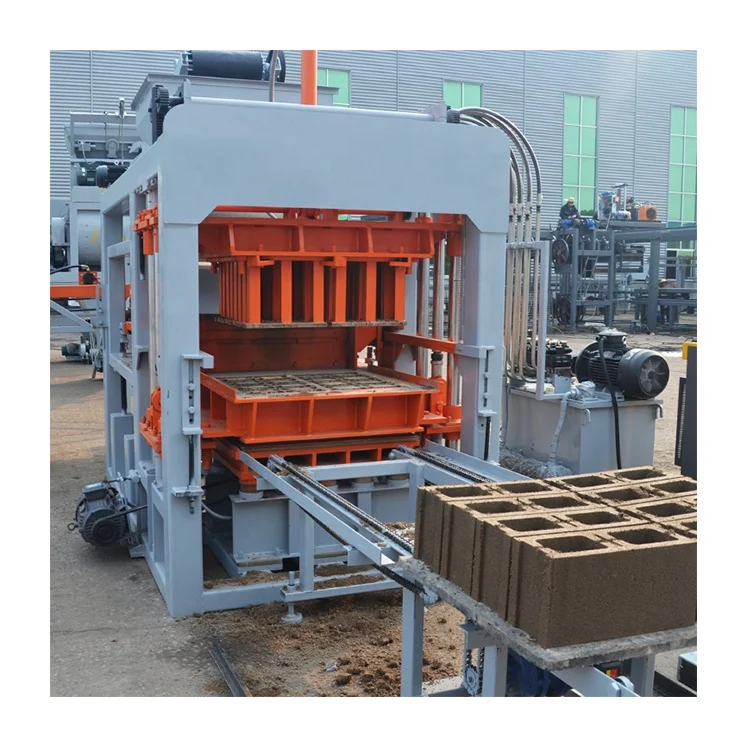 High quality block machine