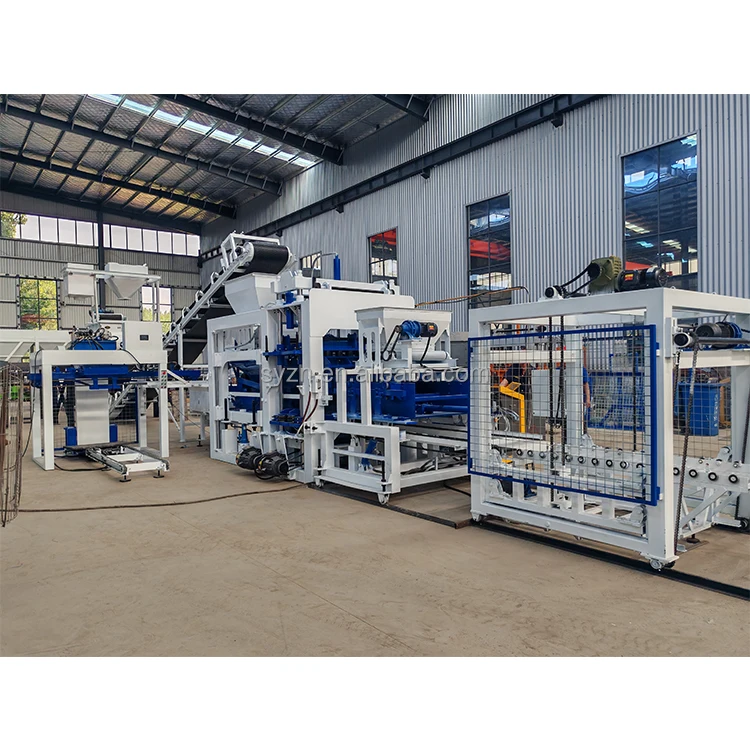
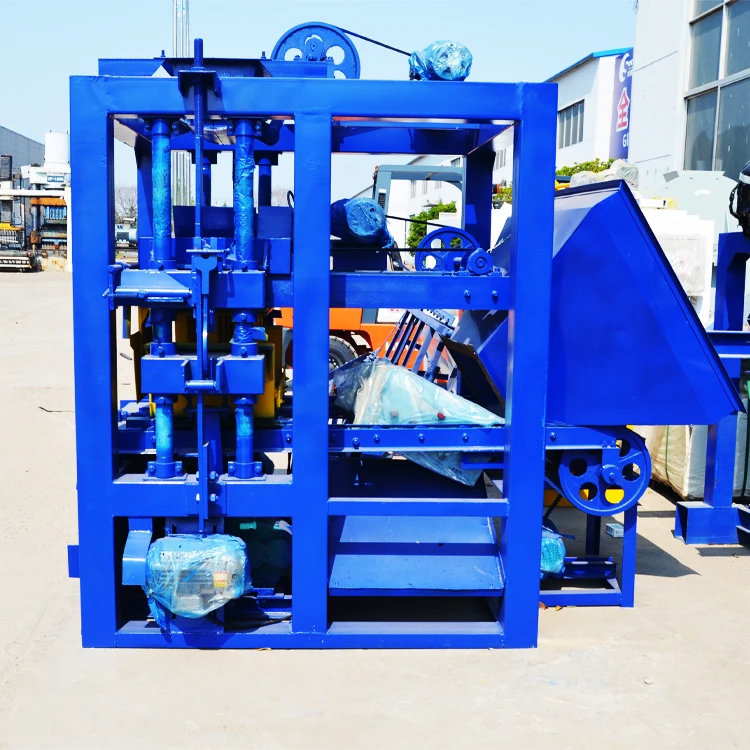
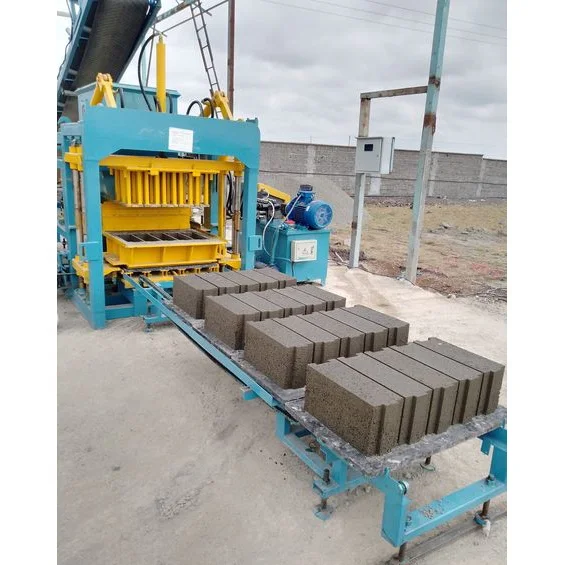
Format-Matched System — The QT4-18 is configured against your actual mix design, local aggregate and target block format rather than shipped as a catalogue default, so vibration force, hydraulic pressure and pallet size arrive aligned with what you will actually produce.
Technical Specifications
| Parameter |
Value |
| Model |
QT4-18 |
| Product Type |
Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
3900×1600×2300 mm |
| Total Weight |
3T |
| Rated Power |
24KW |
| Exciting Power (Vibration Force) |
40-50KN |
| Molding Cycle |
15-25s (basis not stated in source — confirm block format / material / thickness) |
| Mixer Model |
JQ350 |
| Pallet Size |
850×550×25 mm |
| Applied Products |
Paver, solid block, hollow block, curbstone |
| Raw Materials |
Crushed stones, sand, cement, dust, fly ash |
| Automation Level |
Semi-automatic |
| Output Capacity (400×200×200mm hollow block) |
9600-13440 Pcs/8hr at 15-20s cycle |
| Output Capacity (400×150×200mm hollow block) |
14400-19200 Pcs/8hr at 15-20s cycle |
| Output Capacity (240×115×53mm solid brick) |
16200-19440 Pcs/8hr at 15-20s cycle |
| Key Features |
CE documentation scope, pallet handling via trolley, automatic stacker option |
Application Suitability
| Application |
Material or Output |
| Small to medium block production plants |
Hollow and solid blocks from crushed stone, sand and cement |
| On-site construction block production |
Project-scale hollow blocks using locally sourced aggregates |
| Paver and curbstone manufacturing |
Interlocking and kerb formats from cement, fly ash and dust |
| Format expansion for existing producers |
Secondary machine adding hollow or paver lines alongside current output |
What "9600 Blocks per Day" Leaves Out About the QT4-18 Block Machine Manufacturer Quotation
Capacity figures mean nothing unless they name the exact block format, cycle time and mould assumed in the calculation.
I have watched buyers receive a machine rated for thousands of pieces per shift, only to discover the number was based on a thin solid brick while they needed 200mm hollow blocks. The QT4-18 block machine manufacturer output figures above each carry a specific format and cycle window — 400×200×200mm hollow blocks at 15-20 seconds yield a different daily total than 240×115×53mm solid bricks at the same cadence. When a quotation lists a single headline capacity without these qualifiers, the gap between expectation and real output becomes a costly surprise on day one [NEED_CITE: block format assumptions in capacity quotations].

Where the QT4-18 Sits on the Range
The SHIYUE range spans mobile egg-laying units at one end and high-capacity fully automatic lines at the other. The QT4-18 occupies the mid-tier semi-automatic position, aimed at buyers who need format flexibility across hollow blocks, solid bricks, pavers and kerbstones but do not yet have the floor space or capital for a fully automatic stacking and cubing system. This is the tier where a first-time plant owner typically enters, and where an existing producer parks a secondary machine to broaden their product catalogue without duplicating a full line.
Semi-Automatic Means You Choose What to Automate Later
Semi-automatic operation here covers the press cycle and vibration sequence, while pallet feeding and product stacking can start manual and move to automated handling as your curing area and workforce evolve. The 850×550×25 mm pallet size stays constant across that upgrade path, so pallets you buy on day one remain compatible when you later add an automatic stacker or pallet return conveyor [NEED_CITE: semi-automatic block line upgrade stages].
How Vibration Force and Hydraulic Pressure Shape Block Density
The 40-50 kN exciting power works in tandem with the hydraulic station to compact the concrete mix inside the mould cavity. Higher vibration amplitude fluidises the aggregate bed, while hydraulic pressure locks particle-to-particle contact before the block is stripped from the mould. If the mix contains a high proportion of fly ash or fine dust, the pressure and vibration balance must shift compared to a coarse crushed-stone mix — which is why machine settings should follow your specific raw material profile, not a factory default. The 24 kW rated power budget allocates enough headroom for both the vibration motor and the hydraulic pump to run simultaneously without voltage sag during the compaction stroke.
The Hidden Cost of Skipping Voltage Confirmation
A machine wired for a grid that does not match the destination site will sit idle until a local electrician rewires the control panel — a delay that can stretch across multiple weeks and burn through project timelines. I once saw a semi-automatic line held up because the PLC display language defaulted to a script the operators could not read, turning a simple mould-change procedure into a trial-and-error exercise [NEED_CITE: electrical commissioning delays in exported machinery]. Confirming voltage, frequency and control language before the QT4-18 enters production eliminates the most common cause of post-arrival downtime.
Why Buyers Source This Tier from a Single-Focus Manufacturer
Block machinery is the only product category here, so the host machine, mould, pallet and handling equipment are specified as one matched set rather than assembled from unrelated suppliers. Configuration starts with your target block format, local aggregate sample and daily volume, not a catalogue page. Mould drawings are supplied for each format you intend to run, including custom profiles drafted to your market dimensions. Pallet quantity and material are sized against your actual curing area and forklift capacity, so you are not left stacking product by hand on day one. The sales sequence runs from inquiry through factory test, factory test record, and dispatch with every electrical parameter confirmed before the machine leaves the assembly floor.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Mould drawing and format list covering every cavity profile in the quotation
- Pallet specification matched to your curing rack spacing and forklift fork width
- Voltage, frequency and PLC display language confirmation sheet signed before production
- Factory test record on your target block format before dispatch
Installation, Commissioning & Support
- Foundation pad must support 3T total weight across the 3900×1600 mm footprint with level tolerance for the vibration table
- Dedicated 24 kW circuit with voltage and frequency verified against the confirmed electrical schematic before first start-up
- Machine shipped partially assembled; vibration table and hydraulic station bolt together on site within the semi-automatic layout
- Commissioning includes cycle time adjustment across each mould format to match the 15-25 second window to your mix design
- Operator training covers mould changeover procedure, pallet feeding via trolley and basic hydraulic station maintenance
- Wear parts list identifies vibration springs, hydraulic seals and mould liner plates for first reorder planning
What to Include in Your First Enquiry
Tell us the exact block formats your market buys, the daily volume you need for each, and the raw materials available within hauling distance of your site. Share your local voltage and frequency, the control language your operators read, and the dimensions of the curing area you plan to use. If you already own pallets or forklifts, include those specifications so the pallet size and handling workflow can be matched before the line is laid out.
Frequently Asked Questions
Q: How is output capacity calculated per block format on the QT4-18, and what cycle time does each format assume?
A: Each capacity line ties to a specific block dimension and a 15-20 second molding cycle. For example, 9600-13440 pieces per eight-hour shift assumes 400×200×200mm hollow blocks, while 16200-19440 pieces assumes 240×115×53mm solid bricks. The cycle window accounts for vibration, press and stripping time but does not include pallet return or curing handling.
Q: What voltage, frequency and control language options are available for different target markets?
A: Voltage and frequency are confirmed during the quotation stage to match your local grid, and the PLC or control panel display language is set before production. This step is written into the sales sequence specifically to prevent commissioning delays that occur when electrical specifications are left to default factory settings.
Q: How long does a mould change take on the QT4-18, and what formats share the same pallet size?
A: Mould changeover duration depends on the format pair being swapped and should be confirmed with the factory for your specific mould set. All standard formats — hollow, solid, paver and curbstone — use the common 850×550×25 mm pallet, so pallet inventory does not multiply when you add new block types.
Q: Where does the QT4-18 sit on the SHIYUE range compared to smaller and larger models?
A: It occupies the mid-tier semi-automatic position, above entry-level workshop machines and below the fully automatic stacking and cubing lines. Buyers who need multiple formats but are not ready for a continuous automatic plant typically land here, with the option to add pallet return and automatic stacking later without replacing the host press.
Q: What supporting equipment is included in the quotation and what is optional?
A: The standard package covers the host press, JQ350 mixer, pallet trolley and the agreed pallet quantity. Automatic stackers and pallet return conveyors are quoted separately so you can match the automation level to your current workforce and curing layout, then upgrade when volume justifies the investment.

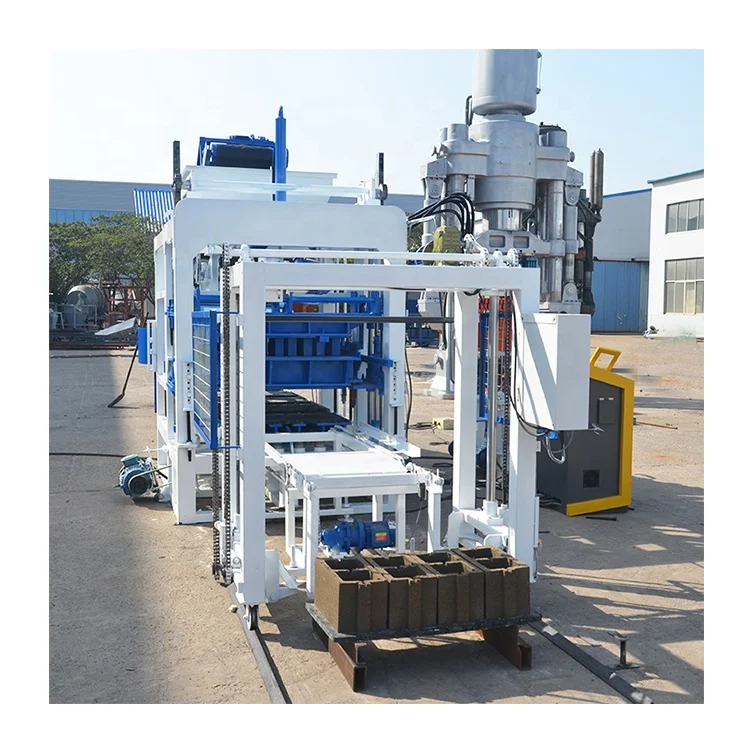
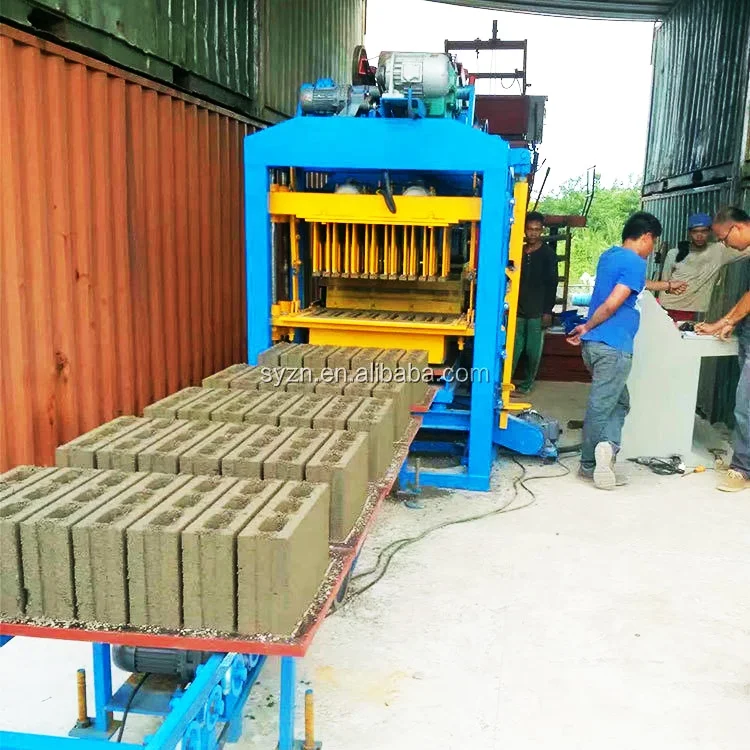 High quality block machine