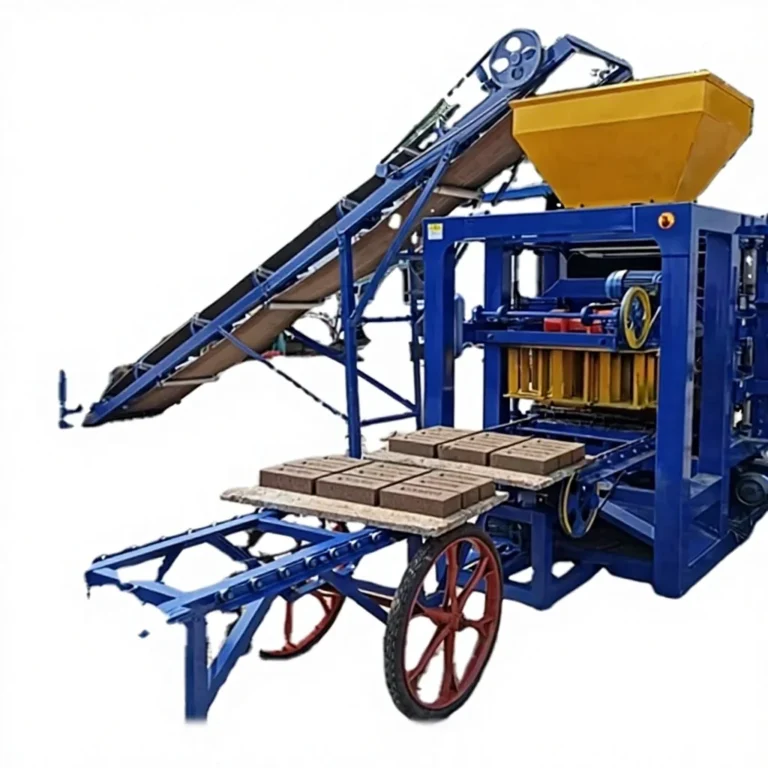
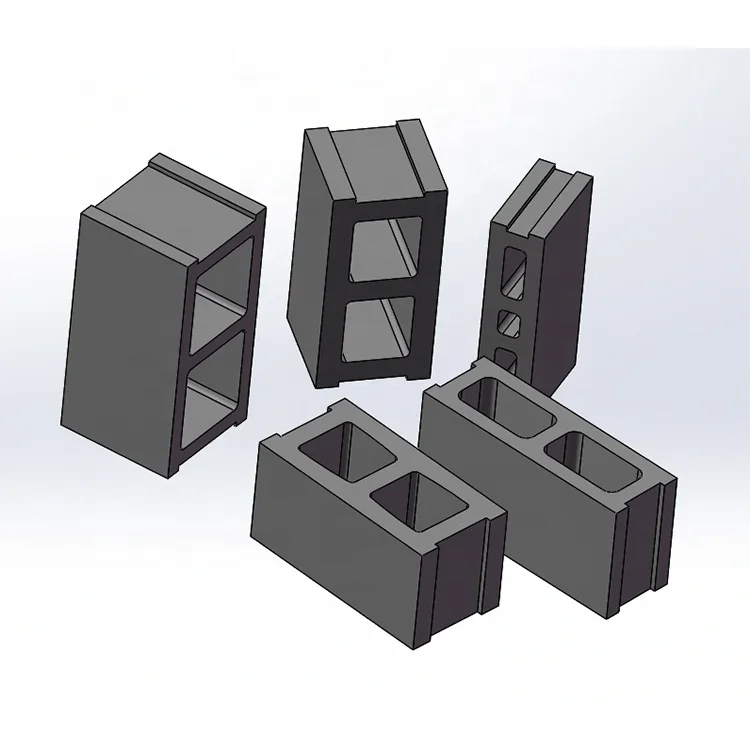
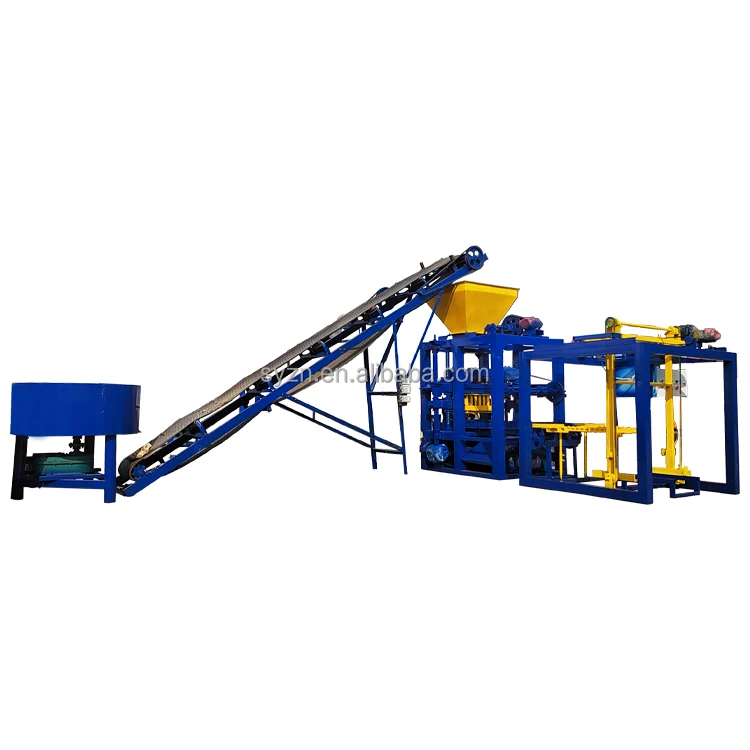
Complete Machine Range — The QT10-15 anchors the high-output automatic tier, sized and configured around the specific block formats your market actually moves.
Technical Specifications
| Parameter |
Value |
| Model |
QT10-15 |
| Product Type |
Stationary Concrete Block Making Machine |
| Vibration Technology |
Four-axis vibration with dynamic and static table |
| Vibration Acceleration |
20g |
| Control System |
Frequency conversion control |
| Automation Level |
Full automatic |
| Material Feeding System |
Press-in arch breaker with 360° rotation |
| Mould Compatibility |
Hollow, solid, pavement, interlocking, porous, slope protection bricks |
| Vibration Damping |
Flexible pressure head damping; adjustable air bag damping in mould box |
| Output Capacity |
(basis to be confirmed by block format, material, and thickness) |
| Cycle Time |
(basis to be confirmed by block format, material, and thickness) |
| Pallet Size |
(basis to be confirmed) |
| CE Marking |
European version configuration available (verify against specific dispatch) |
Application Suitability
| Application |
Material or Output Focus |
| High-volume hollow block production |
Crushed stone, cement, and local aggregate mixes for load-bearing wall construction |
| Solid block manufacturing |
Dense concrete mixes for structural applications requiring high compressive strength |
| Interlocking and pavement bricks |
Finer aggregate blends for precise surface finish and dimensional tolerance |
| Porous and slope protection bricks |
Permeable concrete formulations for drainage and erosion control infrastructure |
Where the Quoted "Cycle Time" Fails the Business Plan
The cycle time on a brochure assumes a specific block format, a specific mix, and a specific pallet — none of which are guaranteed to match your plant.
When a stationary block machine manufacturer quotes a cycle time, they are often referencing a standard hollow block under ideal lab conditions. In a real yard, producing interlocking pavers with a different mould and a finer aggregate blend will change the vibration profile, the hydraulic pressure requirement, and the feeding time. [NEED_CITE: vibration force requirements for different concrete block formats]. If the buyer’s local sand has a high clay content, the material flow through the arch breaker slows, extending the cycle and reducing the actual daily output far below the headline number. The QT10-15 stationary block machine is configured for the buyer’s actual materials, not a catalogue default.
Positioning the QT10-15 Within the Full Machine Range
The stationary block machine range is built around output tiers and automation levels. The QT10-15 sits at the high-capacity, fully automatic end, intended for plants where manual pallet handling would become a bottleneck. Smaller semi-automatic models in the range serve workshops where investment capital is limited and the daily volume requirement is lower. Mobile egg-laying machines occupy a different segment entirely, producing blocks directly on a concrete floor without pallets. Understanding where this model sits helps a buyer decide if the investment in full automation and a larger pallet circuit is justified by their market demand.
Matching the Press to the Pallet Circuit and Curing Yard
A high-output press like the QT10-15 is only as fast as the pallet handling system behind it. [NEED_CITE: concrete block curing cycle time and yard space requirements]. The frequency conversion control and 20g vibration acceleration mean the press itself can cycle quickly, but if the pallet return conveyor, the stacker, and the curing rack system cannot keep pace, the press sits idle waiting for an empty pallet. This is why the machine range is specified as a matched system. The pallet size and material, the stacking method, and the curing area footprint must all be confirmed against the buyer’s existing infrastructure or planned site layout before the line is finalized.
Reading the Vibration and Feeding Specifications
The four-axis vibration with dynamic and static table and 20g acceleration is the core forming mechanism. In stationary block machines, vibration force and hydraulic pressure must work together; vibration settles the mix, and pressure compacts it to the target density. If the vibration is too aggressive for a delicate interlocking brick mould, it damages the mould and creates surface spalling. If it is too weak for a dense solid block, the product fails strength tests. The 360° rotating press-in arch breaker addresses a common feeding problem: material bridging in the hopper, which causes inconsistent fill across the mould cavity and results in blocks of uneven height and weight. The adjustable air bag vibration damping in the mould box isolates the vibration from the machine frame, reducing noise and wear on structural components over thousands of cycles.

The Hidden Cost of Unmatched Specifications
When the pallet size is chosen without considering the buyer’s existing forklift and curing rack dimensions, the entire post-press handling workflow breaks down. Pallets that are too wide for the forklift tines require manual repositioning. Pallets that do not stack correctly on the curing racks create a safety hazard and damage the wet blocks. [NEED_CITE: pallet handling safety in concrete block plants]. Similarly, if the voltage and PLC display language are not confirmed before production, the machine arrives on site and cannot be commissioned until the correct electrical components are sourced or the software is reprogrammed, turning a planned installation into a multi-week delay.
Why Source This Tier From This Range
The machine, mould, pallet, and handling equipment are specified as one system, preventing the integration failures that occur when components are sourced from separate suppliers. The configuration is set against the buyer’s actual mix design and target block format, not a generic template. Mould design covers the specific formats the buyer’s market sells, with custom drawings available for non-standard shapes. The automation level is selectable within the range, so a buyer can install the QT10-15 press with semi-automatic pallet handling now and upgrade to full automatic stacking and cubing later as volume grows. Installation support includes operator training focused on the specific control system and mould change procedures for this machine.
Documentation & Verification
- Line layout drawing showing the QT10-15 press footprint and the connected pallet circuit stations.
- Capacity calculation sheet stating the assumed block format and cycle time for each product in the buyer’s list.
- Machine specification sheet confirming pallet size, voltage, frequency, and PLC display language before production starts.
- Mould drawing and format list detailing the cavity count and dimensional tolerances for each ordered mould.
- Factory test record demonstrating the press running with the buyer’s specified block format and cycle parameters.
Installation, Commissioning & Support
- Site preparation requires a level concrete foundation sized to the QT10-15 overall dimensions and dynamic load.
- Electrical supply must match the confirmed voltage and frequency, with a dedicated circuit for the rated power draw.
- The press arrives with the vibration table and frame assembled; the feeder and mould are mounted on site.
- Commissioning includes tuning the frequency conversion control and vibration acceleration to the buyer’s mix.
- Operator training covers the PLC interface, the mould change procedure, and the daily maintenance checklist.
- Wear parts list identifies the specific vibration springs, hydraulic seals, and mould liners required for this model.
Request a Machine Range Configuration
To determine if the QT10-15 is the correct tier for your operation, or if a different model in the stationary block machine range is a better fit, provide your target daily output per block format, your local raw material analysis, and your available site footprint. Specify your local voltage and frequency, and confirm the control language required for your operators. If you have an existing pallet size and curing yard layout, include those dimensions so the supporting equipment can be matched from the start.
Frequently Asked Questions
Q: Where does the QT10-15 sit compared to semi-automatic and mobile models in the range?
A: The QT10-15 is positioned in the high-output, fully automatic tier of the stationary block machine range. It requires a fixed plant with a pallet circuit and curing system. Semi-automatic models in the range are for lower investment and volume, often with manual pallet handling. Mobile egg-laying machines produce blocks without pallets on a concrete floor, serving a completely different production method and site setup.
Q: How is daily output calculated per block format, and what is the assumed cycle time?
A: Daily output is calculated by taking the confirmed cycle time for a specific block format, multiplying by the number of blocks per pallet and the number of effective operating hours, then applying a realistic utilization factor. The cycle time depends on the block type, the concrete mix, and the required density. A hollow block will have a different cycle than a dense paver. We provide a capacity calculation for each format you intend to produce, not a single headline number.
Q: What pallet size and automation level come with this tier, and can I upgrade later?
A: The pallet size is configured to match the mould cavity layout and your existing curing rack and forklift specifications; it is not a fixed standard. The QT10-15 tier is designed for full automation, including automatic pallet feeding and stacking, but the range allows a buyer to start with a simpler pallet handling setup and add automatic stacking and cubing modules later as production volume justifies the investment.
Q: What plant footprint and supporting equipment does the QT10-15 require?
A: The footprint includes the press itself, the raw material batching and mixing station, the pallet feeder, the stacker, and the curing rack area. The supporting equipment must be balanced so the press is not left waiting for a pallet or for the mixer to deliver a fresh batch. We provide a line layout drawing that maps each station and confirms the total area required before the order is finalized.
Q: How do I confirm voltage, frequency, and PLC display language before shipment?
A: These parameters are locked during the quotation and production confirmation stage. You provide your site’s electrical specification and the required operator language, and we confirm these on the machine specification sheet. The factory test before shipment is conducted with these exact settings active, so the machine arrives ready for connection without requiring electrical or software modifications on site.

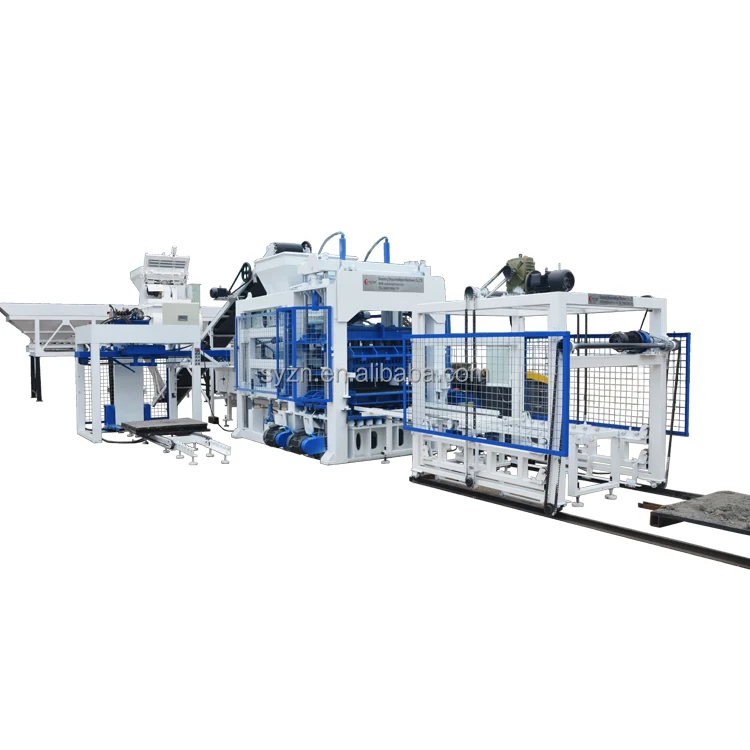
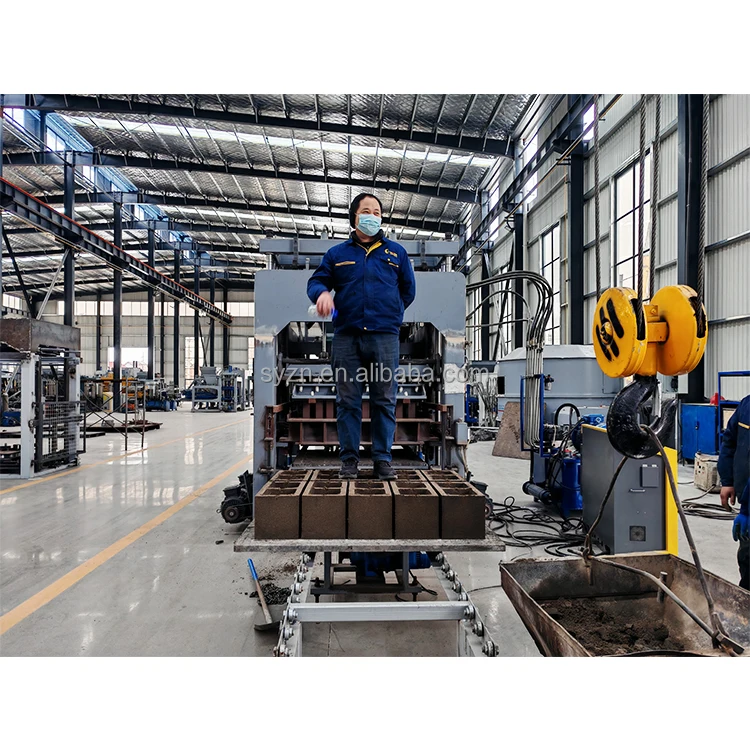 Stationary block machine