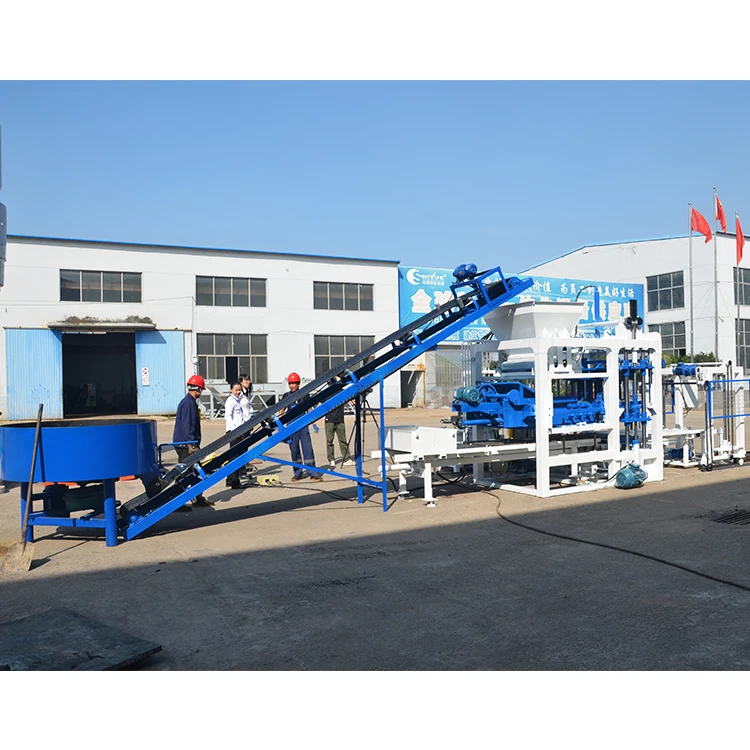
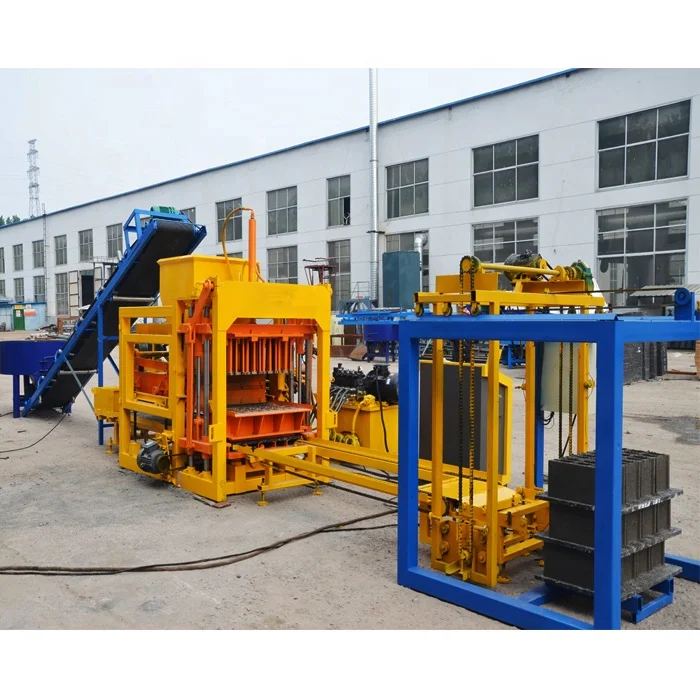
Matched System Specifying — the QT10-15 block press, moulds, pallets and handling stations are configured as one coordinated line rather than sourced from separate vendors, so cycle times balance across every station.
Technical Specifications
| Parameter |
Value |
| Model |
QT10-15 |
| Product Type |
Full Automatic Concrete Block Making Machine |
| Dimension of Host Machine |
5870×2220×2850 mm |
| Weight of Host Machine |
12 Tons |
| Molding Area |
1100×900 mm |
| Workshop Area Required |
200 m² |
| Host Machine Power |
57 kW |
| Vibration Force |
100 kN |
| Pallet Size |
1100×900×30 mm |
| Voltage |
220/380/415/440V (Configurable) |
| Molding Period |
15 Seconds |
| Vibration Method |
Hydraulic + Platform Vibration |
| Vibration Frequency |
2800–4500 Times/Minute |
| Control System |
PLC (Siemens) with Touch Screen |
| Travel Switch |
France Schneider / Japan Omron |
| Motor |
Germany Siemens or CE Standard Brand |
| Mould Heat Treatment |
Carburizing, 54-58 HRC, >100,000 cycles |
| Welding Process |
Carbon Dioxide Protection Welding |
| Grouped Equipment |
PLD1200 Batching Machine, JS750 Mixer, Conveyor, Hydraulic Station, Pallet Feeder, Brick Receiver, Hydraulic Trolley, SY-8 Stacker (3 kW, 600 kg) |
| Color Paver Option |
Color feeding system available as add-on |
| Output Capacity |
(basis not stated in source — capacity to be confirmed by block format and mix design) |
Application Suitability
| Application |
Material or Output |
| Hollow Block Production |
Crushed stone, cement, sand, and fly ash blends for load-bearing and partition walls |
| Solid Block Production |
Dense aggregate mixes for foundation and structural masonry |
| Interlocking Brick Production |
Graded sand and cement for dry-stack wall systems |
| Paving Brick / Color Paver Production |
Fine aggregate and cement with optional surface color layer |
What "15-Second Cycle Time" Actually Means for Your Output
A cycle time only translates to daily output when the block format, mix design, and pallet handling are factored in together.
Catalogue sheets often list a single molding period without specifying which block format was used to measure it. A 15-second cycle for a standard solid brick on a 1100×900 mm pallet yields a very different daily figure than the same cycle producing large hollow blocks where fewer units fit per pallet. When buyers compare machines based on cycle time alone, they frequently discover on commissioning day that real throughput falls short of what the brochure implied. I have seen this misunderstanding delay project handovers by weeks while the plant scrambles to add shifts [NEED_CITE: common causes of block plant underperformance in developing markets].

Positioning the QT10-15 Within the Shiyue Automatic Range
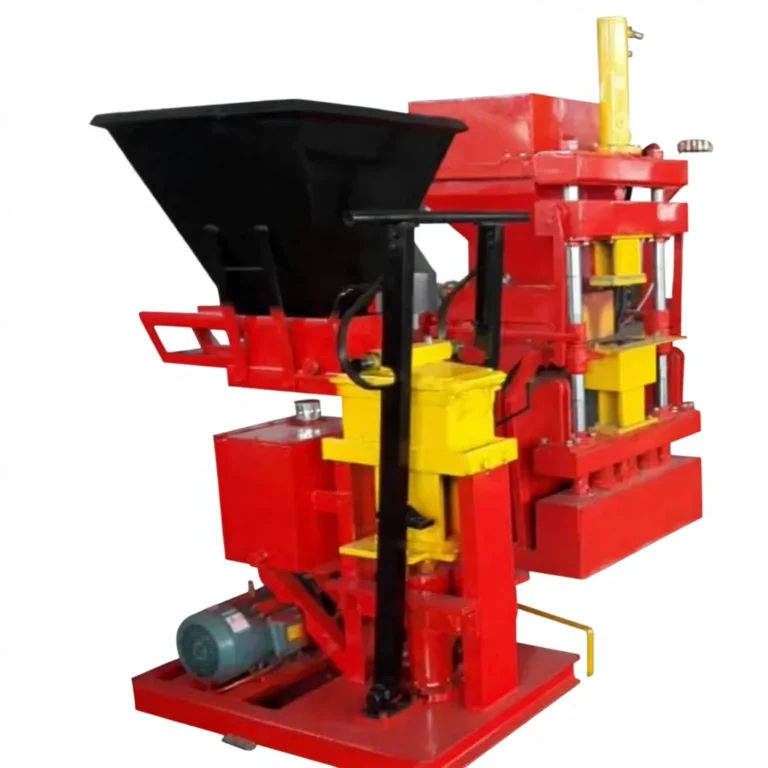
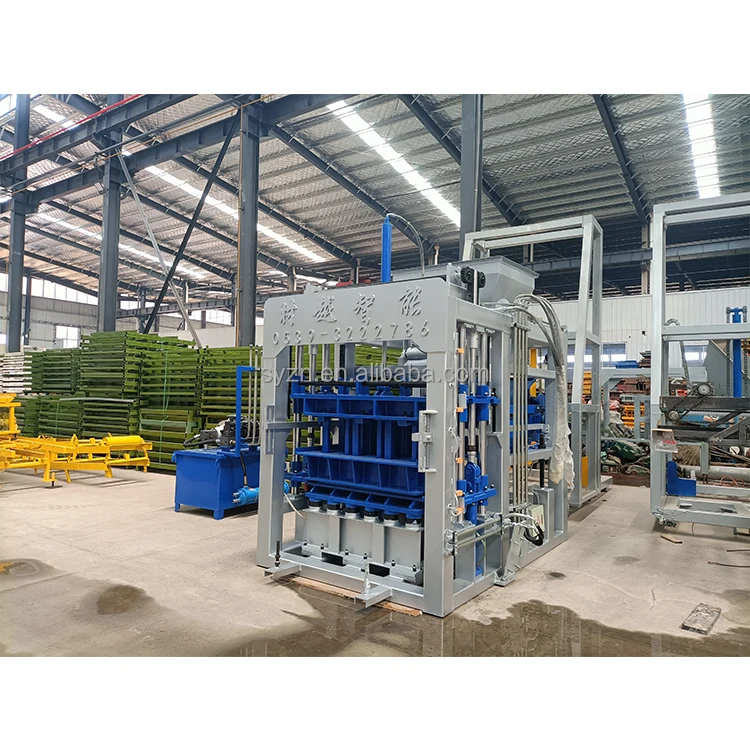
The QT10-15 sits at the high-capacity end of the Shiyue full automatic block machine lineup. Its 1100×900 mm molding area and 100 kN vibration force place it above the mid-tier presses, making it suitable for buyers planning dedicated block production plants rather than workshop-scale operations. Semi-automatic models in the range handle lower volumes with manual pallet handling, while mobile egg-laying machines serve on-site contractors who need zero fixed infrastructure. Understanding where this model lands helps a buyer surveying options decide whether the investment and footprint match their stage.
How the Grouped Line Prevents Bottlenecks Around the Press
A block press can only run as fast as its slowest upstream or downstream station. The QT10-15 grouped equipment package pairs a PLD1200 batching machine and JS750 mixer with a dedicated pallet feeder, brick receiver, hydraulic trolley, and SY-8 stacker rated at 600 kg. This configuration means the press is not left idle waiting for mixed material or empty pallets, and finished blocks are moved off the line without manual lifting. The SY-8 stacker handles the output load so that curing rack turnaround stays ahead of the press cycle [NEED_CITE: block line throughput balancing principles for stationary plants].
Reading the Specs That Decide Block Quality
The 100 kN vibration force combined with hydraulic pressure determines the compaction density of each block — too little force on a coarse aggregate mix produces weak units, while excessive force on a fine mix can cause surface cracking. The 2800–4500 vibrations per minute range allows the operator to tune frequency to the specific aggregate gradation and cement content being used. Carburized moulds hardened to 54–58 HRC maintain dimensional accuracy across production runs; softer moulds lose tolerance and produce blocks that do not stack true. The Siemens PLC with touch screen lets operators store parameter sets for different formats, so switching from hollow blocks to pavers does not require re-entering vibration and pressure profiles from scratch every time.
The Hidden Cost of Specifying Pallets Without Checking Your Curing Yard
If pallet dimensions are chosen without regard to the curing racks and forklifts already on site, the buyer ends up either rebuilding curing infrastructure or hand-stacking blocks that the stacker cannot place correctly. A 1100×900×30 mm pallet must align with rack spacing and forklift tine width. When this alignment is missed, pallets pile up on the floor awaiting manual handling, and the automatic line effectively downgrades itself to semi-automatic output. This mismatch is one of the most common reasons buyers feel they paid for automation they never received [NEED_CITE: pallet and curing area coordination in block production].
Why Buyers Source This Machine Through Shiyue
Block machinery is the single focus of the Shandong Shiyue workshop, so the QT10-15 is specified as a matched system — press, mould, pallet, batching, and stacking — rather than assembled from unrelated suppliers. Each line proposal references the buyer’s actual target block format and local aggregate, not a generic catalogue default. Moulds are designed and built for the formats the buyer’s market sells, including custom drawings when standard formats do not fit. The automation level is selectable, allowing a buyer to start with semi-automatic pallet handling and add full stacking and cubing later. Factory testing runs the complete grouped equipment set before shipment so that arrival surprises are minimized.
Documentation & Verification
- Line layout and capacity calculation specifying the block format assumed for output projections
- Machine specification sheet covering host machine, grouped equipment, and pallet dimensions
- Mould drawing and format list reviewed against your local market requirements
- Hydraulic and electrical schematic with confirmed voltage and control language
- Factory test record on your target block format before dispatch
- CE declaration documentation where applicable to your import regulations
Installation, Commissioning & Support
- Workshop area of 200 m² with level reinforced concrete foundation for the 12-ton host machine
- Dedicated 57 kW power circuit matching confirmed voltage and frequency before machine arrival
- Host machine and grouped equipment dismantled for container loading, reassembled on-site
- PLC touch screen language and Siemens control parameters set during commissioning to match operator needs
- Operator training covering mould change procedure, vibration frequency adjustment, and daily maintenance
- Wear parts list and mould inventory provided for planning first replacement orders
Before You Request a Quote, Prepare These Details
To build a configuration proposal that reflects real output rather than catalogue figures, we need to know the specific block formats your market demands and the daily volume you plan to produce. Share the type and gradation of aggregate available locally, along with your site’s existing voltage supply and frequency. If you already have curing racks or forklifts, their dimensions determine whether the standard 1100×900 mm pallet fits your yard or whether a custom pallet size is needed. Providing these inputs at the inquiry stage avoids costly reconfiguration after the machine is built.
Frequently Asked Questions
Q: How is the QT10-15 daily output calculated, and which block format is assumed?
A: Daily output depends on the block format placed on each 1100×900 mm pallet, the molding cycle, and the number of productive hours. A capacity calculation document is prepared for your specific target format, stating the assumed mix and shift pattern, so the projection reflects what your plant will actually produce rather than a generic catalogue figure.
Q: Where does the QT10-15 sit in the Shiyue range compared to semi-automatic and mobile machines?
A: It occupies the high-capacity tier of the stationary full automatic block machine range, above semi-automatic models that rely on manual pallet handling and above mobile egg-laying machines used for on-site production. Buyers choose this tier when daily volume and product consistency justify the investment in a fixed plant with automatic stacking.
Q: Can the voltage, frequency, and PLC touch-screen language be customized?
A: Yes. The QT10-15 supports 220, 380, 415, and 440V configurations, and frequency is matched to your local grid. The Siemens PLC touch-screen interface is set to your preferred language during production so that operators can navigate menus and parameter screens from day one of commissioning.
Q: What workshop area and foundation does the QT10-15 line require?
A: The host machine needs approximately 200 m² of workshop space, and the 12-ton weight requires a level reinforced concrete slab. The full grouped line including batching, mixing, and stacking stations needs additional yard area for pallet circulation and curing racks, which is confirmed during the line layout stage.
Q: Is the QT10-15 supplied as a complete line, or can I add automation later?
A: The grouped equipment package is designed as one system, but the automation level is selectable. A buyer can start with the press and manual pallet handling, then add the SY-8 stacker and full cubing station later as production volume grows, without replacing the core machine.

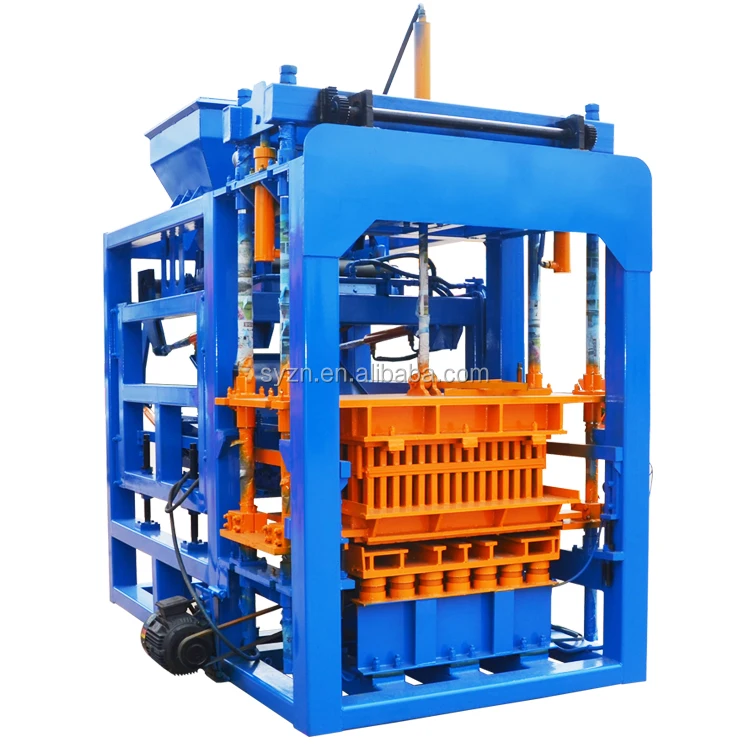 Stationary block machine