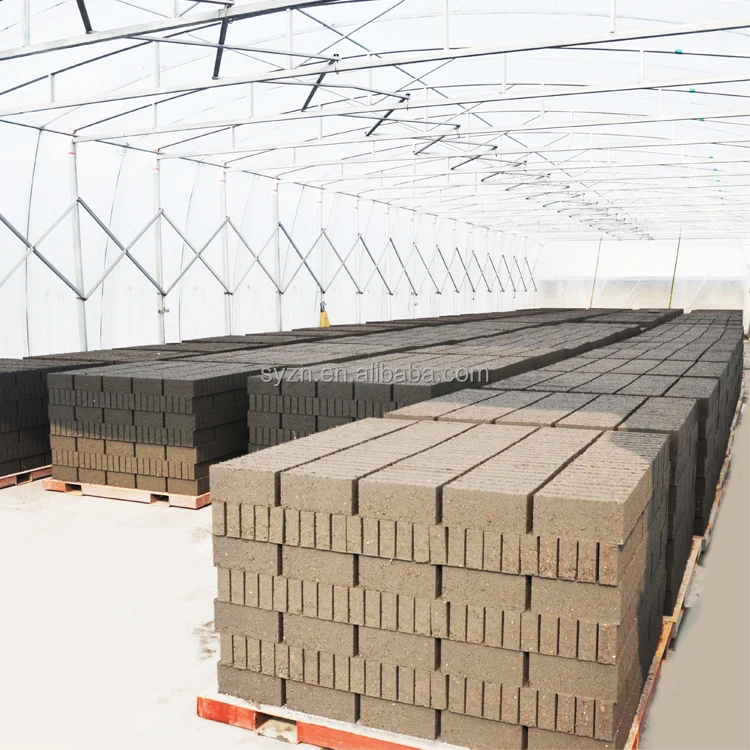
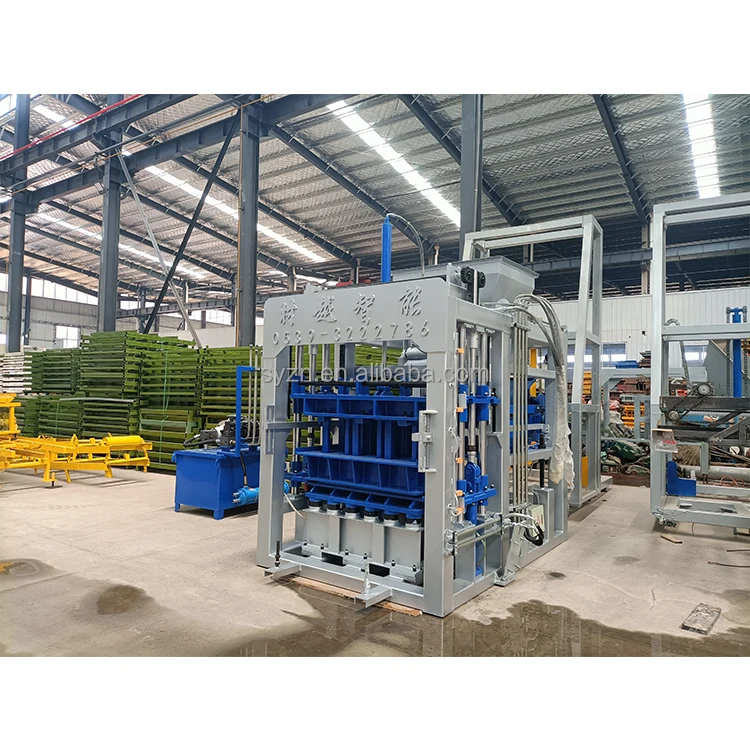
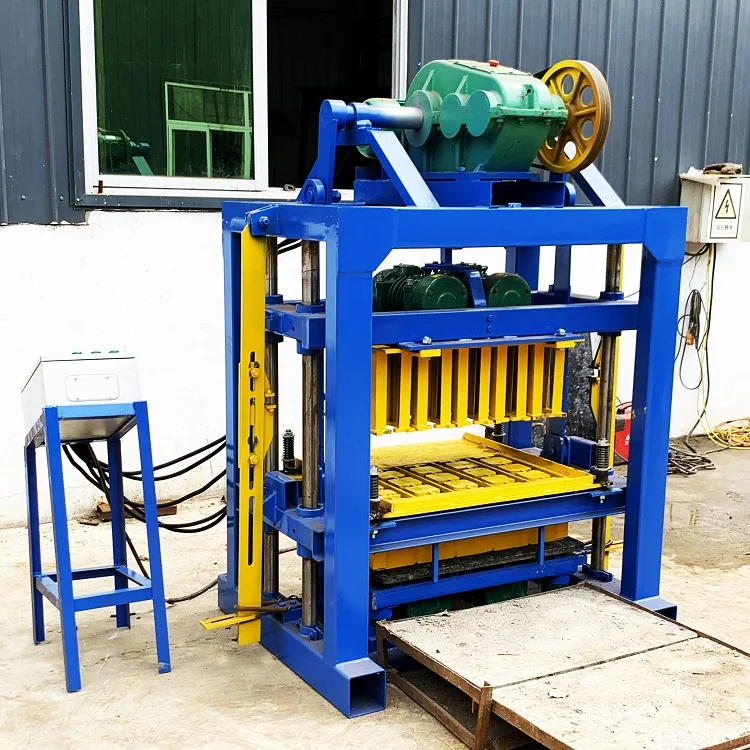
Matched System Sizing — Every QT4-16 block making machine leaves our factory with moulds, pallets, and handling gear specified as one matched set, not sourced separately and forced together on site.
Technical Specifications
| Parameter |
Value |
| Model |
QT4-16 |
| Product Type |
Stationary Concrete Block Making Machine |
| Overall Dimensions (L×W×H) |
7400 × 1950 × 2800 mm |
| Rated Pressure |
21 MPa |
| Vibration Form |
Platform Vibration |
| Vibration Frequency |
2800–4500 r/min |
| Vibration Force |
40 kN |
| Pallet Size |
900 × 550 mm |
| Molding Cycle |
15–20 s (basis not stated in source — confirm block format / material / thickness) |
| Demolding Method |
Hydraulic |
| Factory Area |
600 m² |
| Control System |
PLC intelligent control with man-machine interface, fault diagnosis, remote control function |
| Total Mass |
5 T |
| Applied Products |
Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Materials |
Crushed stone, sand, cement, fly ash, gravel, slag, dust |
| Voltage & Frequency |
Configurable per destination market (basis to be confirmed before production) |
| Rated Power |
To be confirmed per motor configuration |
| Stacking Method |
Selectable from manual pallet handling to automatic stacking |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing |
Gravel, sand, cement mixes for load-bearing walls |
| Interlocking paver runs |
Colored concrete with fine aggregate finishes |
| Curbstone and kerb production |
High-density concrete with coarse aggregate |
| On-site housing project blocks |
Local aggregate and cement available at project location |
Why "Cycles per Hour" Can Mislead Even Experienced Buyers
Cycle time only means something when the block format behind it is named.
I have watched buyers receive a QT4-16 block making machine manufacturer quotation showing impressive cycles per hour, only to discover the figure assumed a small solid block while their actual product was a 200 mm hollow block. The daily output gap between those two formats is substantial, and no amount of optimism closes it after installation. [NEED_CITE: typical output variance across block formats on stationary presses]
A mid-tier stationary press like the QT4-16 operates across a range of formats, each with its own mould cavity count, fill depth, and vibration requirement. The 15–20 second molding cycle listed in general specifications is a starting point for discussion, not a guarantee. Without knowing whether your target product is a 400×200×200 mm hollow block or a 200×100×60 mm paving unit, that number floats free of reality.
Where the QT4-16 Sits Within the Stationary Range
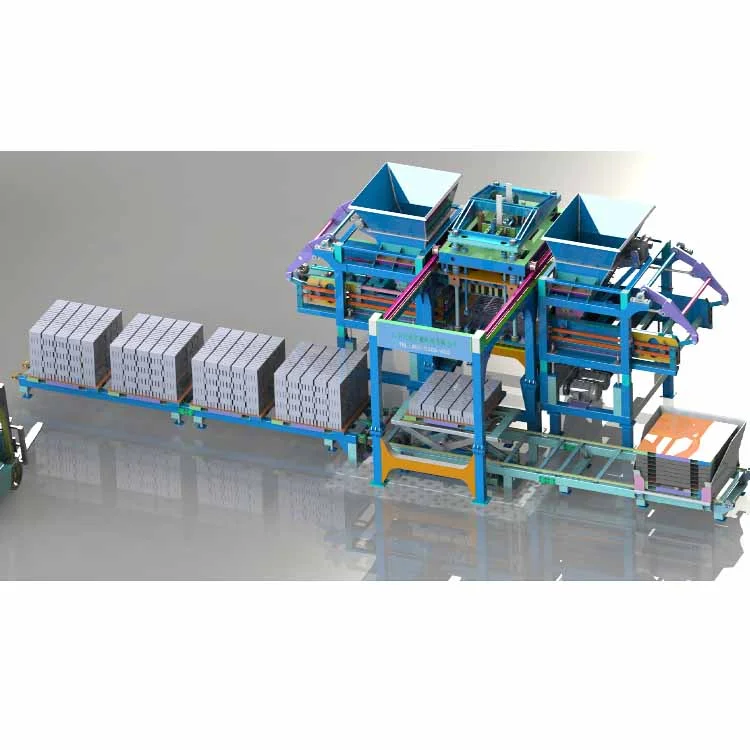
The QT4-16 block making machine occupies the middle ground in our stationary lineup. It delivers more output than entry-level workshop presses while demanding less factory space and lower utility infrastructure than high-capacity automatic lines. For buyers who have outgrown mobile or egg-laying machines but are not ready to commit to a fully automatic plant, this model offers a realistic stepping stone. The PLC-controlled platform gives operators a consistent starting point, and the automation level around the press can be selected based on available labour and budget.
Automation Tiers and How They Connect
Every stationary block line involves stations beyond the press itself: raw material feeding, mixing, pallet circulation, stacking, and curing rack handling. The QT4-16 block making machine manufacturer range allows each of these stations to be configured independently. [NEED_CITE: automation tier impact on daily labour requirements in block plants] A buyer in a market where labour costs are manageable may choose semi-automatic pallet handling and manual stacking, then upgrade to automatic cubing later. A buyer facing tight labour availability or strict production deadlines may prefer full automatic stacking from day one. The press cycle must be matched to whichever peripheral speed is chosen, so the press is never left waiting for a pallet or a cleared curing rack.
Reading the Specifications That Actually Matter
The 21 MPa rated pressure and 40 kN vibration force work together to determine block density and compressive strength. Hydraulic pressure compresses the mix while platform vibration at 2800–4500 r/min settles aggregate into voids. If either figure is mismatched to the buyer’s local aggregate gradation or cement content, blocks emerge with inconsistent strength. The 900 × 550 mm pallet size dictates how many cavities each mould can carry and must align with the buyer’s existing curing yard dimensions and forklift capacity. The PLC system with built-in fault diagnosis and remote control capability reduces troubleshooting time, but the display language must be confirmed before production so operators can read alerts immediately upon commissioning.

The Cost of Getting Configuration Wrong
When pallet size is chosen without considering the curing area, blocks sit in poorly ventilated stacks and strength development slows unpredictably. When voltage and frequency are assumed rather than confirmed, transformers must be sourced locally, and commissioning stalls for weeks. [NEED_CITE: common commissioning delays caused by unconfirmed electrical specifications] A mould change system that takes most of a shift defeats the purpose of owning a multi-format press. These are not theoretical failures — they show up repeatedly in plants where the machine was selected from a catalogue rather than configured against the buyer’s actual conditions.
Why Buyers Source This Line From Shiyue
The QT4-16 is specified as a complete system: press, mould, pallet, and handling equipment are sized together so cycle times align across every station. Mould design covers the formats the buyer’s local market actually sells, with custom drawings available when standard options do not match. Automation level is selectable, meaning a first-time entrepreneur can start with semi-automatic handling and add stacking automation as volume grows. Voltage, frequency, and PLC display language are confirmed before the machine enters production, eliminating the most common on-site delays. Factory testing replicates the buyer’s target block format and mix design, providing a documented baseline before the machine is crated for shipment.
Documentation & Verification
- Line layout drawing showing block format assumed in capacity calculation
- Machine specification sheet with confirmed voltage, frequency, and motor ratings
- Mould drawing and format list matched to your local product demand
- Pallet specification aligned with your curing area and forklift capacity
- Factory test record on your target block format before dispatch
- Packing photographs and customs documentation support
Installation, Commissioning & Support
- Foundation plan based on the 7400 × 1950 mm footprint and 5 T operating mass
- Electrical hookup guide specifying confirmed voltage, frequency, and dedicated circuit requirements
- Assembly from dismantled shipping configuration with alignment checks on the platform vibration system
- First-run parameter setting for hydraulic pressure and vibration frequency against your mix design
- Operator training covering PLC fault diagnosis screens and mould change procedure
- Wear parts list for hydraulic seals, vibration springs, and mould liners with reorder references
What We Need to Configure Your Line
To move from a general inquiry to a firm configuration, share your target block formats and the daily output you need for each. Let us know the raw materials available locally — aggregate type, maximum particle size, and cement brand. Confirm your site voltage and frequency, preferred PLC display language, and the dimensions of your curing area so we can match pallet handling accordingly.
Frequently Asked Questions
Q: How is QT4-16 daily output calculated and which block format is assumed?
A: Daily output depends on the block format, mould cavity count, and actual cycle time for that specific product. A 15–20 second cycle is a general range, but the realistic figure for a 200 mm hollow block differs from a 60 mm paver. We provide a per-format capacity calculation before you commit, so the quoted output matches your actual production plan.
Q: Where does the QT4-16 sit compared to smaller and higher-tier models?
A: It occupies the mid-range of our stationary lineup, offering more output than workshop-scale presses without the infrastructure demands of high-capacity automatic lines. Buyers who have outgrown mobile machines but are not ready for full plant automation typically find this tier appropriate. Automation around the press remains selectable.
Q: What voltage, frequency, and PLC language options are available?
A: Voltage and frequency are confirmed per destination market before production begins. The PLC display language is set to match your operator team’s requirements. This confirmation step is mandatory in our sales process to prevent commissioning delays on site.
Q: Can I start semi-automatic and upgrade to full automatic stacking later?
A: Yes. The QT4-16 supports manual pallet handling, semi-automatic feeding, or full automatic stacking and cubing. The press and control system are designed so peripheral automation can be added later without replacing the core machine, protecting your initial investment.
Q: What factory area does the QT4-16 line require?
A: The press itself operates within approximately 600 m², but total area must include raw material storage, mixing station, curing racks, and finished block stacking. We provide a line layout drawing that accounts for each zone based on your chosen automation level and pallet circulation method.

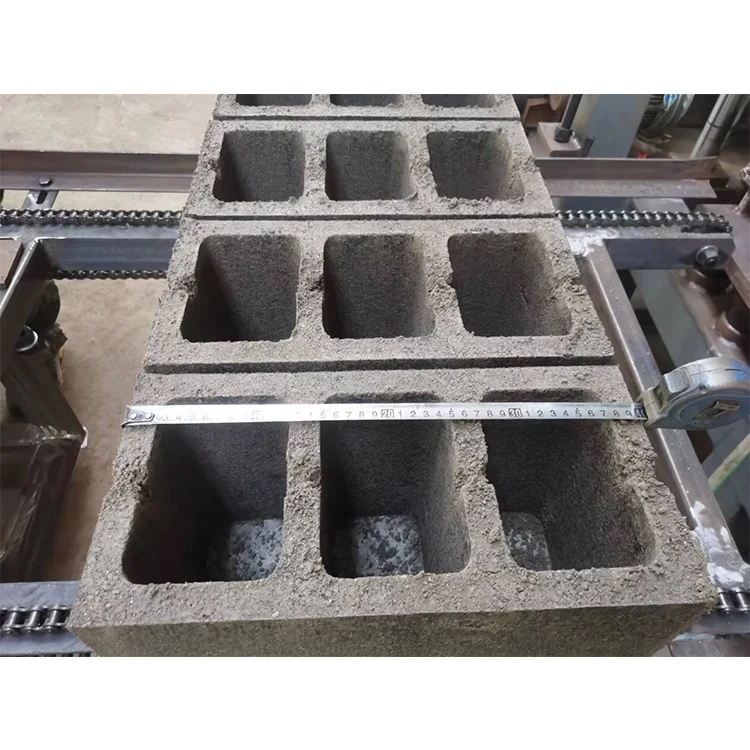
 Stationary block machine