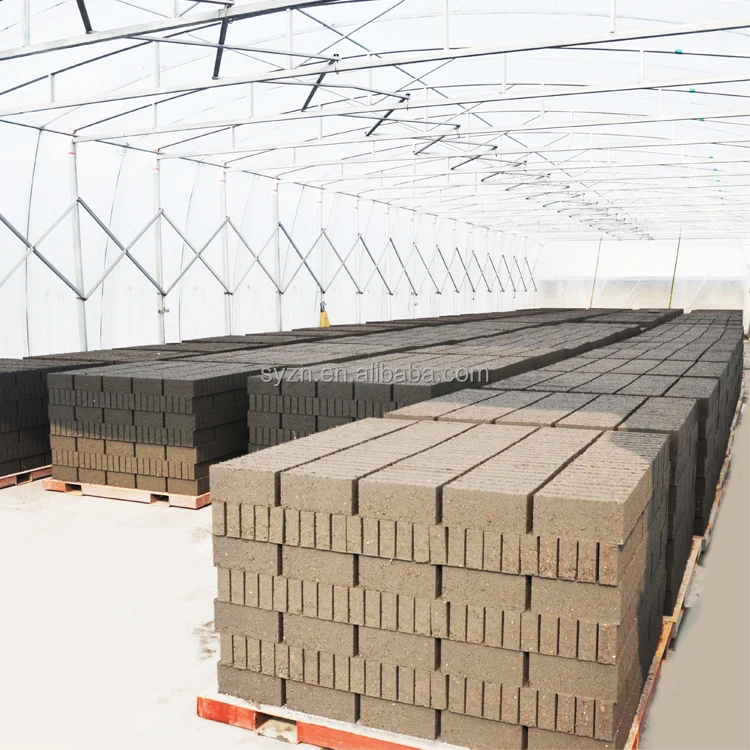
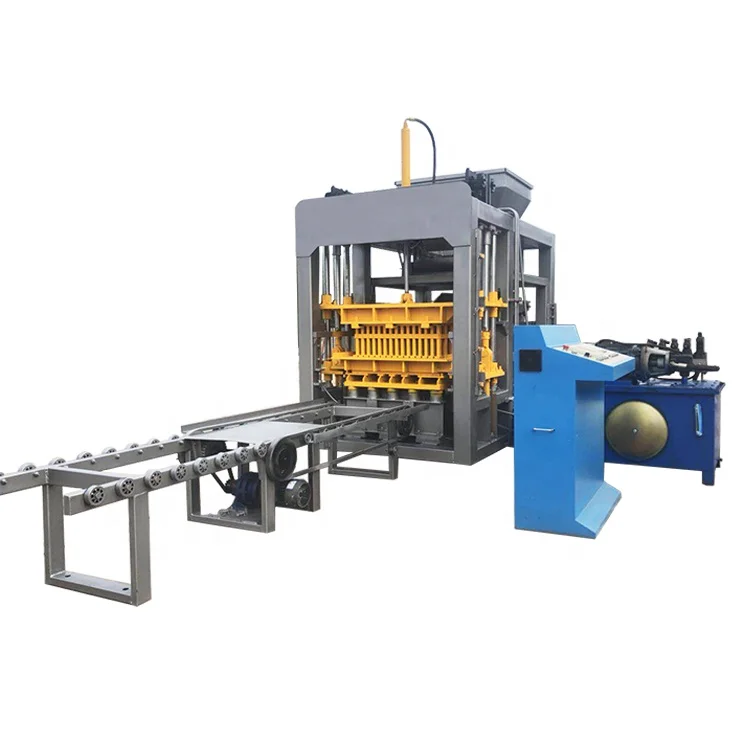
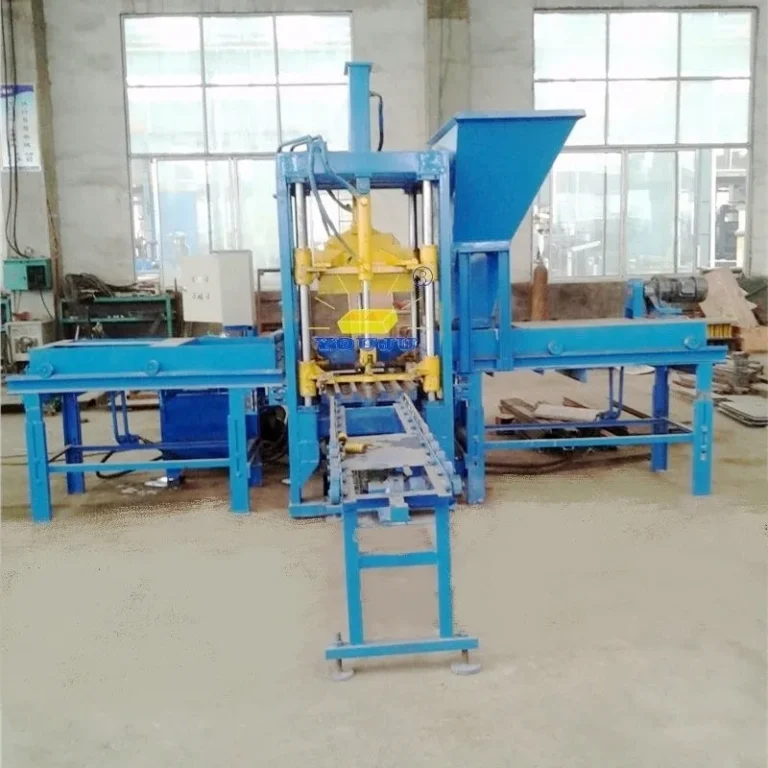
Single Focus, Complete System — The QT18-25 pallet-free line integrates press, stacking, and handling as one matched system rather than assembled from separate suppliers, so cycle times and formats align from day one.
Technical Specifications
| Parameter |
Value |
| Model |
QT18-25 |
| Product Type |
Fully Automatic Pallet-free Hollow Block Making Machine |
| Brick Height Range |
50–300 mm |
| Stacking Height |
0–1200 mm |
| Main Vibration Form |
Platform Vibration |
| Vibration Frequency |
2800–4500 r/min |
| Vibration Power |
60 kW |
| Hydraulic System Power |
59 kW |
| Driving Method |
Hydraulic |
| Demolding Method |
Vibration and Hydraulic |
| Molding Cycle |
15–25 s (basis to be confirmed per block format) |
| General Water Consumption |
~8 T/Day |
| Recommended Factory Area |
~2000 m² |
| Control System |
PLC with person-machine conversation interface |
| Automation Level |
Fully automatic, pallet-free stacking |
| Pallet Requirement |
None (pallet-free design) |
| Applied Products |
Hollow/solid blocks, pavers, interlocking blocks, curbstones, colored pavers |
| Raw Materials |
Crushed stone, sand, cement, fly ash, gravel, slag, dust |
| Standards |
CE (declaration availability to be confirmed) |
Application Suitability
| Application |
Material or Output |
| High-volume hollow block production |
Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing for load-bearing walls |
Gravel, cement, slag aggregates |
| Paver and interlocking block runs |
Colored concrete mixes, fine aggregates |
| Curbstone and kerb production |
Coarse aggregate, high-strength cement mixes |
| On-site contractor production for housing projects |
Locally sourced sand, stone dust, cement |
What "15-25 Seconds" Actually Means for Your Daily Output
A molding cycle quoted without the block format it assumes is not a capacity figure — it is a starting point.
Buyers regularly receive quotations stating a cycle time of 15–25 seconds and mentally convert that into a daily output number. The problem is that a 15-second cycle for a small solid paver and a 25-second cycle for a large hollow block produce vastly different piece counts, and neither number accounts for mould change delays, raw material feed interruptions, or the stacking rhythm downstream. [NEED_CITE: realistic block plant output calculation methods] When the actual block format is never stated in the capacity calculation, the real daily output falls noticeably short of expectation, and the buyer is left wondering where the missing volume went. A fully automatic block machine manufacturer must anchor every cycle time to a specific block dimension and mix design.

Where the QT18-25 Sits in the Full Machine Range
The QT18-25 occupies the high-capacity, fully automatic tier of the block machine lineup. Below it sit semi-automatic models for smaller plants where pallet handling is done manually, and mobile egg-laying machines for on-site production without a fixed plant footprint. This fully automatic block machine manufacturer positions the QT18-25 for buyers who need continuous production with pallet-free stacking up to 1200 mm, eliminating the pallet circulation system that standard automatic lines require.
Understanding the Pallet-free Distinction and Plant Footprint
Standard automatic block lines rely on pallets to carry wet blocks from the press to the curing area, which means pallet return conveyors, pallet cleaners, and a forklift fleet dedicated to pallet movement. The QT18-25 removes that entire layer — blocks are stacked directly after moulding, which changes the plant layout fundamentally. The curing rack arrangement, the stacking station footprint, and the floor space needed for raw material feed all shift when pallets leave the equation. [NEED_CITE: pallet-free versus pallet-based block plant layout differences] Buyers evaluating this fully automatic block machine manufacturer range should compare not just the press cost but the total auxiliary equipment each tier demands.
Reading the Vibration and Hydraulic Numbers Correctly
The platform vibration system delivers 60 kW at 2800–4500 r/min, while the hydraulic system provides 59 kW of pressing force. In block making, vibration frequency and hydraulic pressure must work together — vibration fluidizes the mix so it fills the mould cavity, and hydraulic pressure then compacts it to target density. If the local aggregate has high clay content or unusual moisture, the vibration frequency that works in the factory test may not work on the buyer’s site, which is why configuration must be set against the actual mix design. The 50–300 mm brick height range covers hollow blocks, solid blocks, pavers, and curbstones, but each format demands a different balance of vibration time and pressing force within the 15–25 second cycle window. The PLC person-machine interface allows operators to store parameter sets for each format, so switching production does not mean starting from scratch every time.
The Hidden Cost of Configuring Against the Wrong Mix
A buyer who receives a machine configured for a clean silica sand mix but only has access to high-silt river sand will face inconsistent block strength from the first production run. The vibration frequency and hydraulic pressure that produce excellent results with one aggregate may leave blocks friable or cracked with another. Mould wear accelerates, cycle times stretch as operators compensate, and the daily output that justified the investment quietly erodes. [NEED_CITE: impact of local aggregate variation on block compressive strength] This is not a defect in the machine — it is a gap in the specification process that surfaces only after the equipment is bolted to the factory floor.
Why Buyers Source This Fully Automatic Block Machine Manufacturer
Block machinery is the single focus here, so the QT18-25 press, mould, stacking system, and handling equipment are specified as one matched set rather than assembled from separate vendors. Machine configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default that assumes ideal materials. Mould design covers the formats the buyer’s market actually sells, with custom drawings available for non-standard dimensions. The automation level is selectable — a buyer can begin with semi-automatic operation and add automatic stacking and cubing as volume grows. Installation support includes on-site commissioning and operator training so the crew understands parameter adjustment from the first week.
Documentation & Verification
- Line layout drawing showing QT18-25 stacking station and curing area placement
- Capacity calculation stating block format and cycle time assumption per product
- Machine specification sheet confirming voltage, frequency, and PLC display language
- Hydraulic and electrical schematic for on-site maintenance reference
- Factory test record with actual cycle times across buyer’s target block formats
- Wear parts and mould list with recommended replacement intervals
Installation, Commissioning & Support
- Foundation plan sized for QT18-25 vibration load and 2000 m² plant area
- Power supply verification for 60 kW vibration and 59 kW hydraulic circuits
- Machine dismantling state documented for container loading and reassembly sequence
- On-site commissioning over approximately one week with parameter tuning per block format
- Operator training covering PLC interface navigation and mould change procedure
- First-year spare parts supply excluding quick-wear items with ongoing support available
Preparing Your Inquiry with the Right Technical Details
To receive a configuration proposal that reflects actual production conditions, share the target block formats with dimensions, the daily output volume required, and the local aggregate types available including sand source and moisture characteristics. Provide the site voltage and frequency, preferred PLC display language, and the dimensions of any existing curing area or forklift equipment that the stacking height must accommodate.
Frequently Asked Questions
Q: What output tiers does the full range cover, and where does the QT18-25 sit?
A: The range spans mobile egg-laying machines for small on-site work, semi-automatic models for lower-investment workshops, and fully automatic lines for high-capacity plants. The QT18-25 sits at the upper end as a pallet-free automatic machine with stacking up to 1200 mm, suited for buyers who want continuous production without pallet circulation infrastructure.
Q: How does plant footprint differ between pallet-free and pallet-based machines?
A: Pallet-free systems like the QT18-25 eliminate pallet return conveyors, pallet cleaners, and pallet storage zones, which reduces the overall line length. However, the stacking station and curing rack arrangement require their own dedicated space. The recommended area of approximately 2000 m² accounts for press, stacking, curing, and raw material zones combined.
Q: How do I verify realistic daily output for my specific block format?
A: Request a capacity calculation that states the exact block dimensions and cycle time assumed, not a generic cycles-per-hour figure. The QT18-25 molding cycle of 15–25 seconds varies by format, and a 300 mm hollow block will produce fewer pieces per shift than a 50 mm paver. Ask for factory test records run on your target format.
Q: Can I start semi-automatic and upgrade to fully automatic later?
A: Yes. The automation level across the machine range is selectable, so a buyer can begin with manual pallet handling or semi-automatic operation and add automatic stacking and cubing modules as production volume grows. The PLC control system supports upgrade integration without replacing the core press.
Q: What is the investment difference between mobile, semi-automatic, and fully automatic tiers?
A: Mobile machines carry the lowest equipment cost but produce on bare ground with limited format range. Semi-automatic lines add a fixed press and mixer but require manual pallet handling. Fully automatic pallet-free machines like the QT18-25 represent the highest equipment investment but remove pallet purchase and circulation costs, shifting the cost structure toward automation rather than consumables.

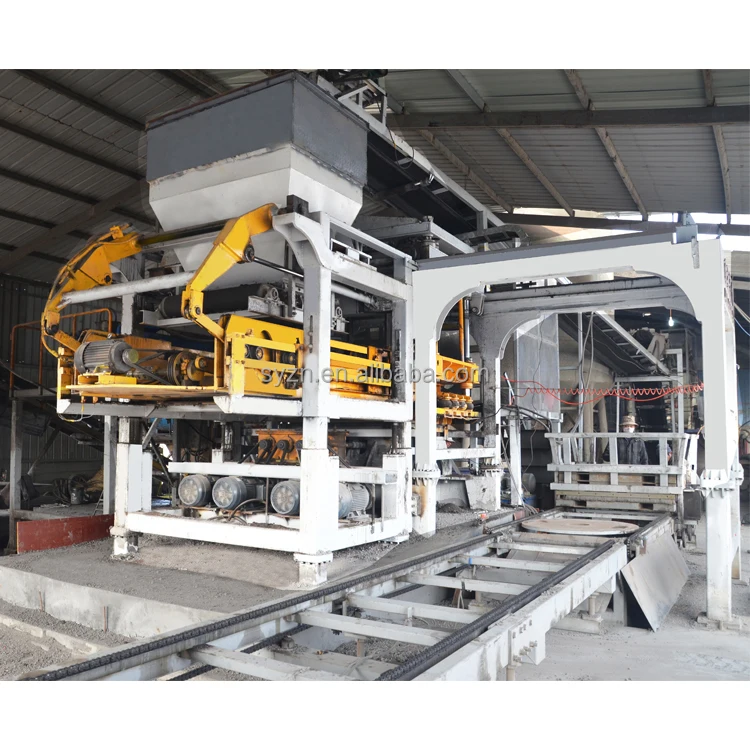
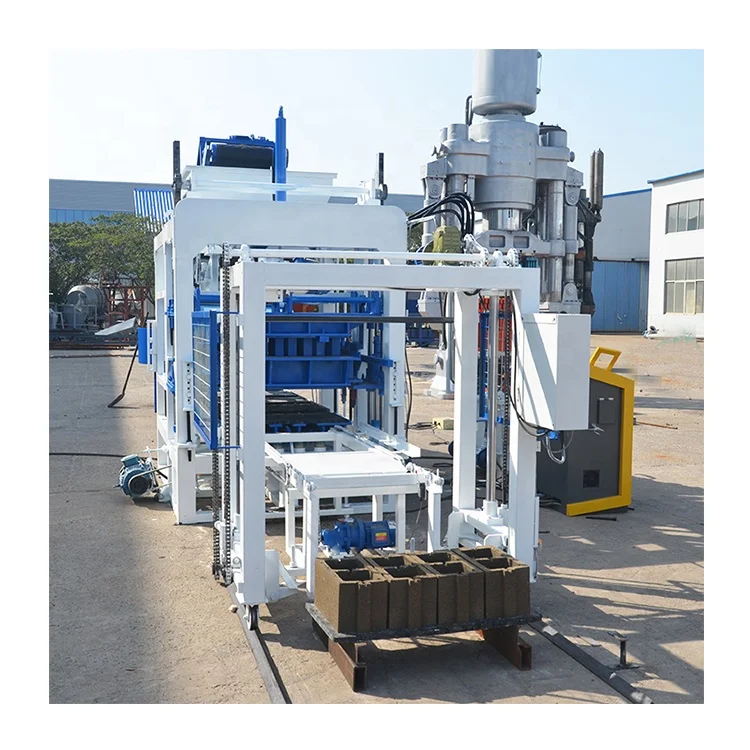 Stationary block machine