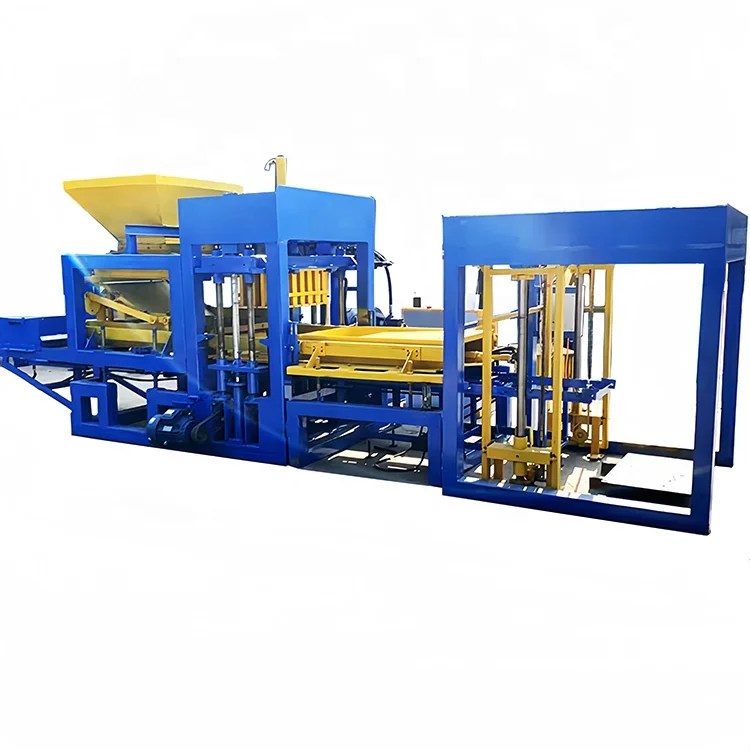
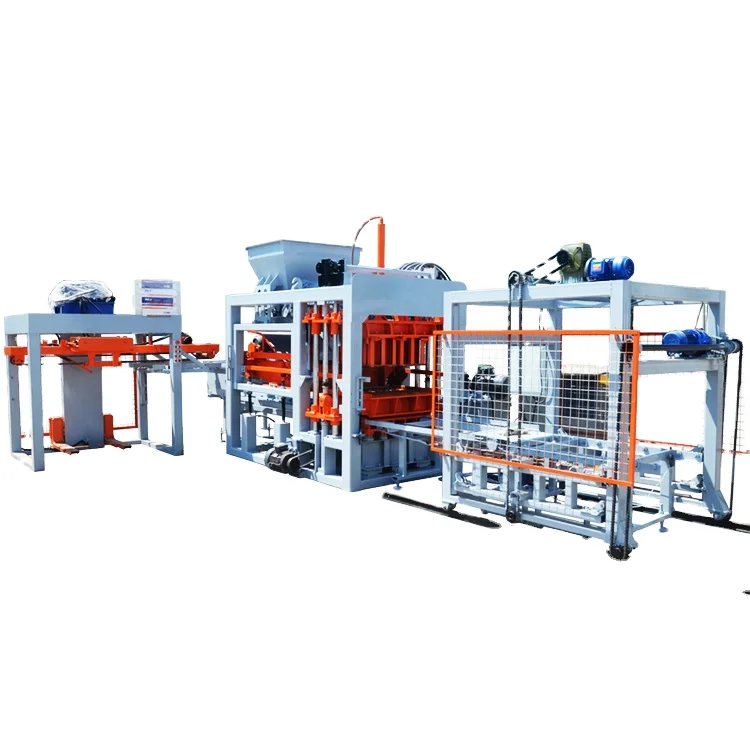
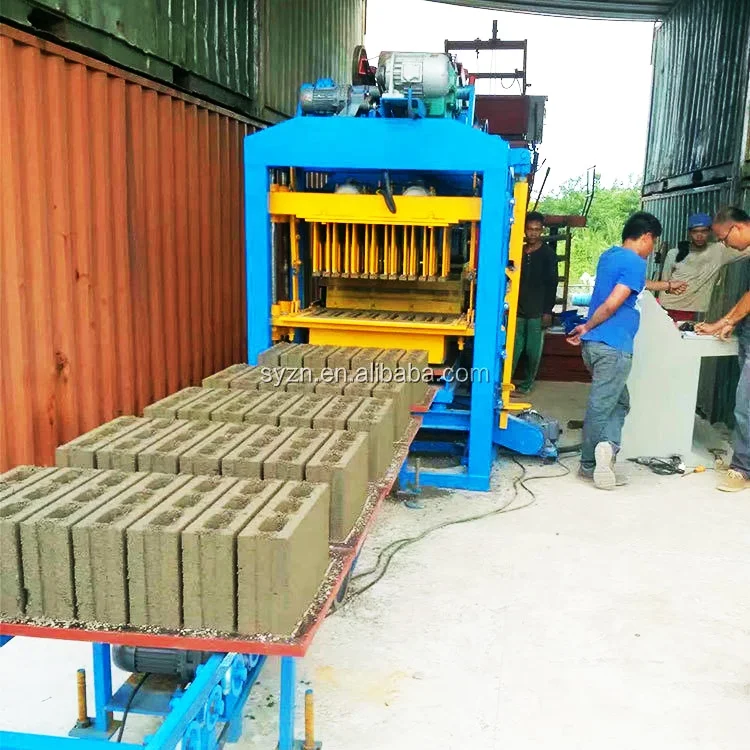
Matched System Configuration — the QT10-15 interlocking brick machine and its supporting line are specified together against your actual block format, local aggregate and target output, not assembled from catalogue defaults.
Technical Specifications
| Parameter |
Value |
| Model |
QT10-15 |
| Product Type |
Interlocking Brick Making Machine |
| Control System |
PLC control cabinet |
| Hydraulic System |
Independent integrated hydraulic station |
| Vibration Mode |
Vertical station mode resonance, automatic FM-AM |
| Component List |
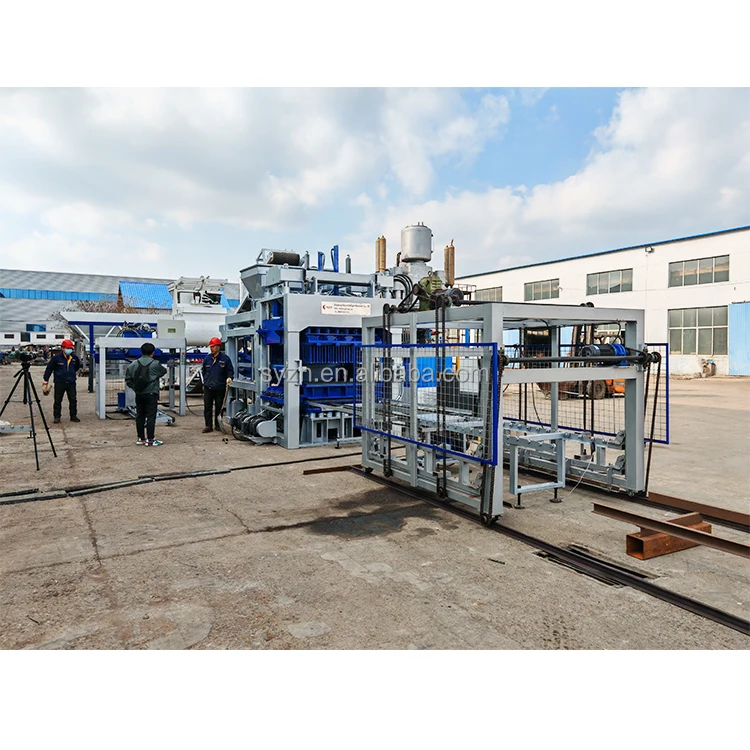
Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
| Cycle Time (400×200×200mm hollow block) |
15–20s |
| Output Capacity (400×200×200mm, 10 pcs/mould) |
1800–2400 pcs/hour, 14400–19200 pcs/8hr |
| Cycle Time (400×150×200mm hollow block) |
15–20s |
| Output Capacity (400×150×200mm, 12 pcs/mould) |
2160–2880 pcs/hour, 17280–23040 pcs/8hr |
| Cycle Time (240×115×53mm solid brick) |
15–20s |
| Output Capacity (240×115×53mm, 62 pcs/mould) |
8928–11160 pcs/hour, 71424–89280 pcs/8hr |
| Cycle Time (200×100×60mm paver) |
20–25s |
| Output Capacity (200×100×60mm, 27 pcs/mould) |
5184–6480 pcs/hour, 41472–51840 pcs/8hr |
| Cycle Time (225×112.5×60mm interlocking brick) |
20–25s |
| Output Capacity (225×112.5×60mm, 24 pcs/mould) |
4032–5040 pcs/hour, 32256–40320 pcs/8hr |
| Mould Change |
Simple replacement for multi-format production |
| Automation Level |
Automatic (full line scope to be confirmed) |
| Rated Power |
Basis to be confirmed |
| Voltage & Frequency |
Basis to be confirmed |
| Overall Dimensions |
Basis to be confirmed |
| Net Weight |
Basis to be confirmed |
| Hydraulic Pressure |
Basis to be confirmed |
| Vibration Force |
Basis to be confirmed |
| Pallet Size |
Basis to be confirmed |
| Mould Change Time |
Basis to be confirmed |
| PLC Language Options |
Basis to be confirmed |
| Warranty |
1 year for whole machine (excluding spare parts) |
| Certification |
CE (verify applicability to this model) |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Crushed stone, sand, cement, fly ash blends |
| Solid brick production |
Fine aggregate and cement mixes for standard masonry units |
| Paving brick production |
Dense aggregate blends for vehicular and pedestrian surfaces |
| Interlocking brick production |
Graded aggregate with cement for mortarless wall systems |
| Multicellular brick production |
Lightweight or standard aggregate for partition and infill blocks |
What "Pieces per Hour" Means When No Block Format Is Named
A capacity number without a block format attached is not a capacity number. The QT10-15 interlocking brick machine manufacturer literature across this industry frequently quotes a single headline output. That figure almost always assumes the smallest, fastest-cycling product the machine can press. Once the buyer switches to a larger hollow block or a dense paver, the real throughput drops because the cycle must lengthen and the mould holds fewer cavities. I have watched project schedules slip in Southeast Asia because the plant was sized on a headline figure that assumed solid brick, while the actual product mix was dominated by 400mm hollow blocks running at a slower cadence. The numbers in the specification table above are tied to specific block dimensions, cavity counts and cycle ranges so the daily plan can be built on them [NEED_CITE: block machine capacity calculation standards per format].

Where the QT10-15 Sits in the Range
The QT10-15 occupies the high-output tier within Shiyue’s automatic block machine catalogue. It is positioned for plants that run multiple block formats across a single shift and need the press to keep pace without becoming the bottleneck. Buyers comparing tiers should look at pallet size, vibration force rating and the automation scope around the press rather than motor power alone.
Multi-Format Production on One Press
The value of this QT10-15 interlocking brick machine lies in its mould-change flexibility. A plant can run hollow blocks in the morning, switch to pavers after lunch, and press interlocking bricks for a housing contract the next day — all on the same pallet circuit. The real question buyers should ask is how long that changeover takes with a trained crew and whether the hydraulic and vibration settings need manual adjustment or follow a stored recipe [NEED_CITE: mould change procedures for hydraulic block presses].
How Vibration and Pressure Shape Block Density
Vertical station mode resonance with automatic FM-AM tuning adjusts the vibration profile as the mould fills, which matters when the aggregate gradation shifts between batches. The independent integrated hydraulic station sits apart from the main vibration zone, reducing seal wear from constant shaking. Together these systems determine whether a 225×112.5×60mm interlocking brick meets the compressive strength the local building code demands, or whether the block crumbles at the corners during pallet handling.
Reading the Specs That Matter Most
Cycle time and cavity count multiply directly into hourly output, which is why the table lists both side by side for every format. The 15–20 second range for hollow blocks assumes a well-graded mix that flows freely into the mould; a sticky volcanic ash aggregate can push that toward the upper end or beyond. The PLC control cabinet coordinates pallet feed, material dosing and vibration timing, but the language on the HMI and the voltage feeding the cabinet must match the buyer’s site before the machine ships. Pallet size governs how many cavities fit in one press stroke, and it also determines whether the cured blocks can be moved by the forklift already in the yard [NEED_CITE: pallet sizing standards for concrete block curing].
The Cost of Ignoring Mix Design Before Purchase
When a buyer orders a machine configured for river sand and then feeds it crusher dust with high fines content, the material does not compact the same way. Blocks come off the press with soft edges, the reject pile grows, and operators slow the cycle to compensate. I saw a plant in the Philippines lose an entire month of production chasing a mix problem that should have been resolved at the quotation stage. The hydraulic pressure and vibration force need to be matched to the aggregate report, not to a generic catalogue setting [NEED_CITE: aggregate grading effects on block compaction].
Why Source the QT10-15 Here
Block machinery is the single focus of this operation, so the QT10-15 press, its moulds, pallets and handling equipment are specified as one matched system. The configuration is set against the buyer’s actual mix design and target block format rather than a default line from a brochure. Mould design covers the formats the buyer’s market sells, including custom drawings when a local standard falls outside the catalogue. Automation level can be selected at semi-automatic for a lower entry investment and upgraded later as volumes grow. Installation support includes on-site commissioning and operator training so the crew can run the machine independently from the first week.
Documentation & Verification
- Line layout with capacity calculation tied to your chosen block format
- Machine specification sheet confirming voltage, frequency and PLC language
- Mould drawing and format list covering every product you plan to run
- Hydraulic and electrical schematic for local maintenance teams
- Factory test record on your aggregate blend before dispatch
- CE declaration provided where applicable to the destination market
Installation, Commissioning & Support
- Foundation plan based on the QT10-15 vibration load and hydraulic station weight
- Dedicated power circuit sized to the confirmed rated power and voltage
- Machine dismantled for container loading and reassembled on-site at arrival
- First-run parameter tuning against your local aggregate and mix design
- Operator training covering PLC navigation, mould change and daily checks
- Wear parts and mould list supplied for planned maintenance scheduling
Before You Request a Quote
Send the block formats your market buys most, the daily volume you need for each, and an aggregate report or lab analysis of your local raw material. Confirm the voltage and frequency at your site along with the preferred PLC display language. If you already own pallets or curing racks, share their dimensions so the line can be configured around them rather than replacing them.
Frequently Asked Questions
Q: How is the QT10-15 output capacity calculated per block format?
A: Each capacity figure in the table is tied to a specific block size, mould cavity count and cycle time range. For example, the 400×200×200mm hollow block runs ten cavities per mould at 15–20 seconds, giving 1800–2400 pieces per hour. Different formats have different cavity counts and cycle ranges, which is why a single headline number does not represent the full picture.
Q: What voltage and PLC language options are available?
A: Voltage and frequency are confirmed during the quotation stage to match the buyer’s local supply. The PLC display language is agreed before production so operators can read alarms and recipes in their working language. Both items are listed on the specification sheet that ships with the machine.
Q: Which block formats can the QT10-15 produce?
A: The machine can press hollow blocks, solid bricks, pavers, interlocking bricks and multicellular bricks by changing the mould. The specification table lists five standard formats with their cycle times and outputs. Custom moulds can be designed for formats outside that list based on buyer drawings.
Q: Does the standard line include pallet handling and stacking?
A: The base component list covers pallet feed, the press, storage hopper, conveyor, hydraulic unit and PLC cabinet. Automatic stacking and curing rack handling are available as line extensions. Buyers should confirm the full automation scope during configuration so manual pallet handling is not assumed by default.
Q: What on-site support is provided after delivery?
A: The manufacturer sends technicians for installation, commissioning and operator training at the buyer’s plant. The team sets press parameters against the local mix design, runs test cycles and hands over the operation and maintenance manual. Mould and wear parts support continues after the crew is running independently.

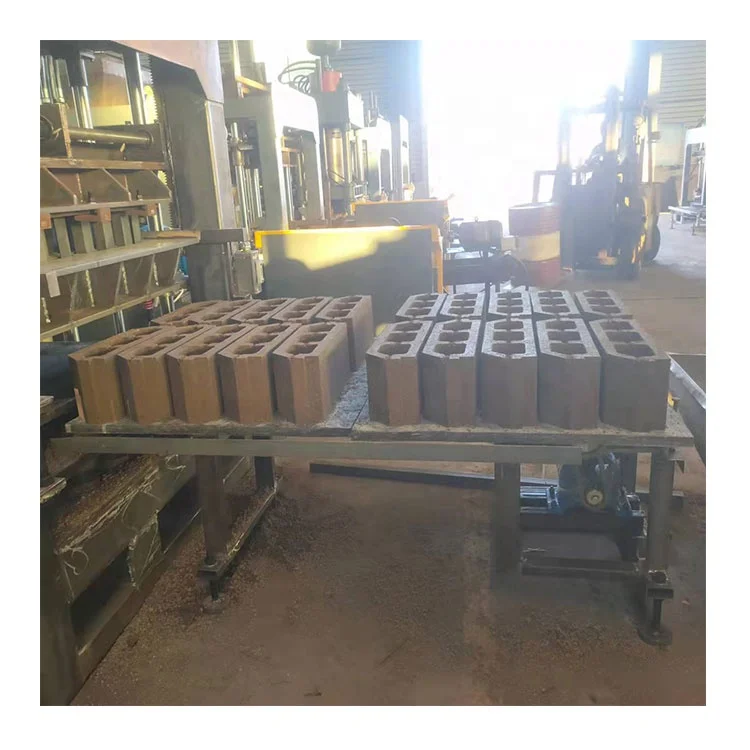
 High quality block machine