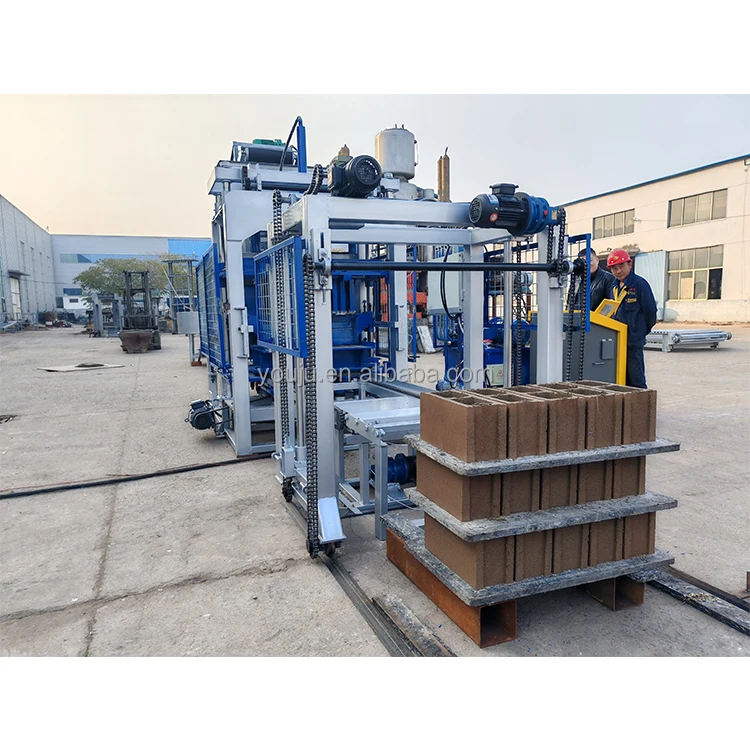
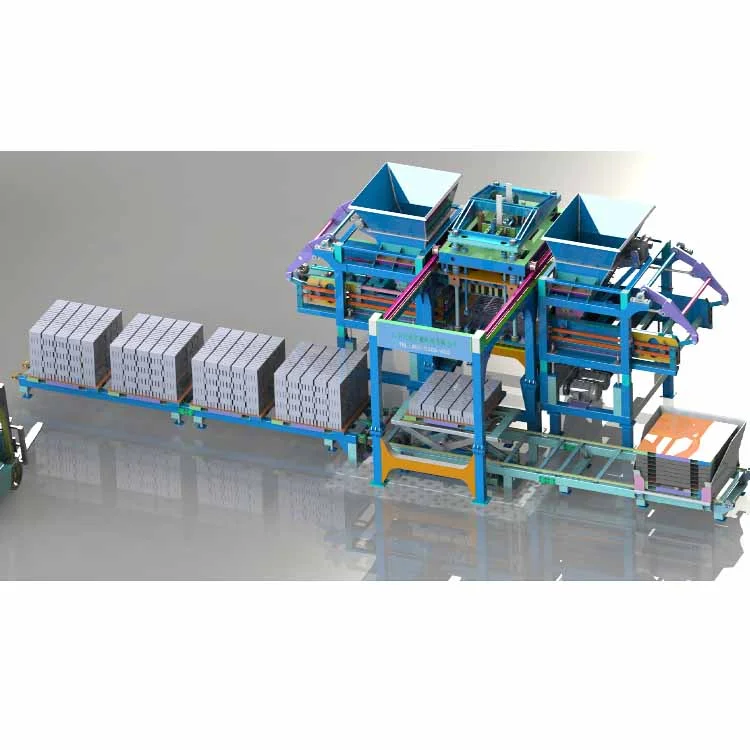
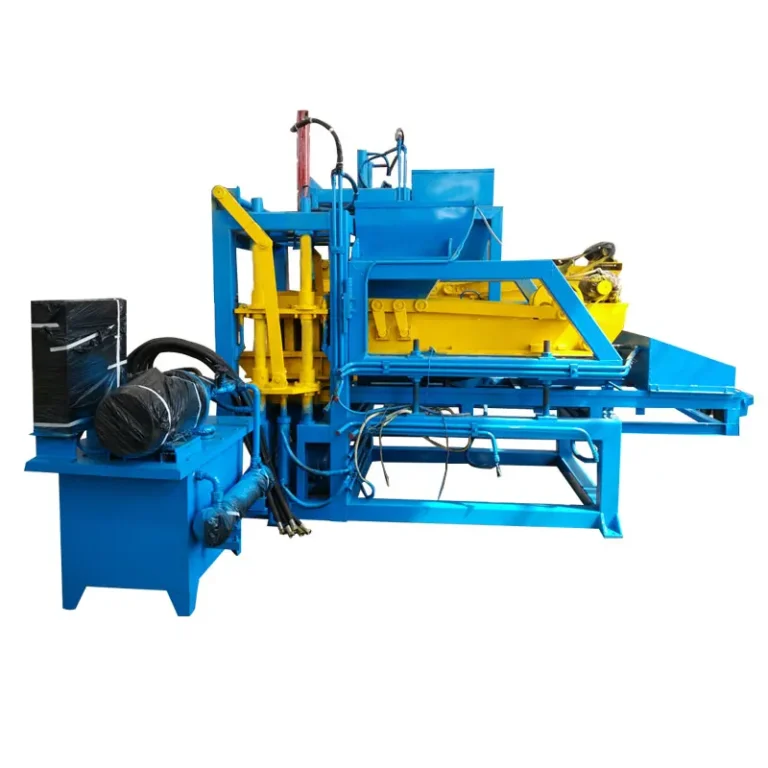
Matched System Supply — the QTJ4-25 host, JQ350 mixer, mould and pallet are specified together so cycle times align from feed to curing, avoiding the mismatch buyers face when sourcing the press and line equipment from separate suppliers.
Technical Specifications
| Parameter |
Value |
| Model |
QTJ4-25 |
| Product Type |
Semi-Automatic Concrete Block Making Machine |
| Rated Power |
17.9 kW |
| Vibration Force |
60 kN |
| Vibration Frequency |
2800 r/min |
| Molding Cycle |
25 s |
| Output Capacity |
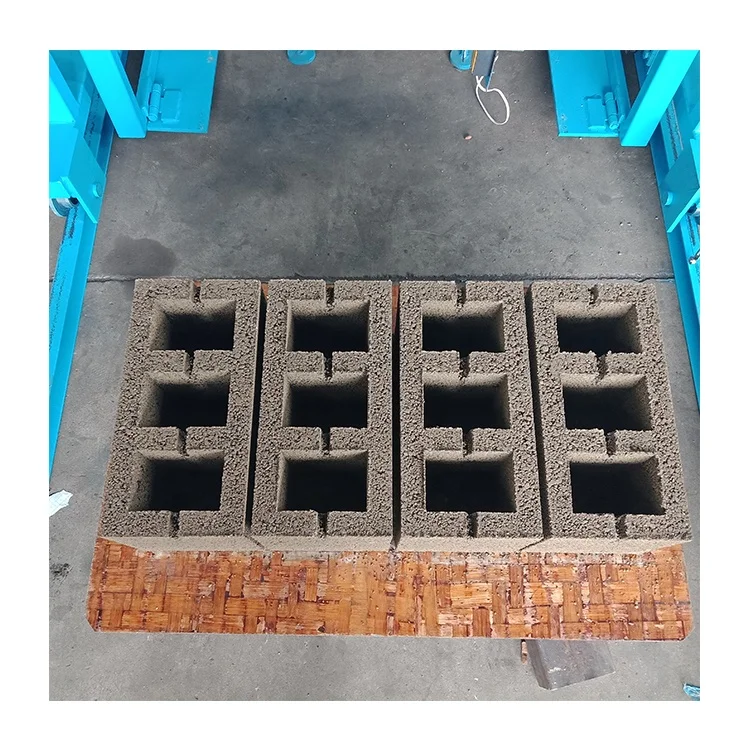
960 pcs/h, 7680 pcs/day (based on 400×200×200 mm hollow block, 4 pcs/mould) |
| Pallet Size |
850×550×20 mm |
| Overall Dimensions |
6400×1500×2700 mm |
| Total Mass |
2500 kg |
| Control System |
Motor-operated, semi-automatic |
| Hydraulic Station |
Included |
| Configuration Included |
Host machine 1 set, block mould 1 set, JQ350 mixer |
| Mould Compatibility |
Hollow, solid, paver, curbstone via mould change |
| Voltage & Frequency |
Configurable to buyer’s local standard (basis to be confirmed before order) |
Application Suitability
| Application |
Material or Output |
| Hollow block production |
Crushed stone, sand, cement, and fly ash mixes |
| Solid block production |
Dense aggregate blends for load-bearing walls |
| Paving block production |
Fine aggregate and cement for pedestrian and light-traffic surfaces |
| Curbstone production |
Coarse aggregate with higher cement content for road edge profiles |
Why the Voltage Question Must Come Before the Quotation
A machine that cannot start on arrival wastes weeks, not hours.
Quoted lead times and cycle speeds mean nothing when the local grid frequency does not match what the hydraulic pump motor expects. I once saw a semi-automatic concrete block making machine manufacturer ship a unit to West Africa without confirming the 50 Hz versus 60 Hz split, and the site spent three weeks waiting for a transformer retrofit before the PLC would even power on. [NEED_CITE: voltage and frequency standards by export market] The QTJ4-25 draws 17.9 kW across its vibration and hydraulic circuits, a load that demands a dedicated supply line at the correct voltage. Buyers who treat electrical confirmation as a post-order formality are the ones who end up paying for idle installation crews and missed delivery commitments to their own customers.

Where the QTJ4-25 Sits in the Output Tier Ladder
The QTJ4-25 occupies the entry-to-mid tier of the stationary block machine range. For a first-time plant or a contractor producing on site, this tier offers a semi-automatic concrete block making machine manufacturer configuration that keeps initial capital controlled while leaving a clear path to higher automation later. The 25-second molding cycle and four-block-per-mould layout suit workshops where pallet handling is still done manually but consistent pressing pressure is non-negotiable.
How the Range Scales Around This Model
Stepping up from this tier means moving to larger pallet sizes, faster cycles, and fully automatic stacking and cubing. Stepping down means mobile or egg-laying machines with no fixed pallet circuit. The QTJ4-25 sits at the pivot point where buyers decide whether their volume justifies a fixed plant layout or whether a smaller mobile unit still covers their needs. [NEED_CITE: block plant capacity planning for developing markets] Understanding this position helps buyers avoid over-investing in automation they cannot yet staff or under-investing in a machine they will outgrow within a year.
Reading the Specs That Actually Shape Daily Output
The 60 kN vibration force working together with the included hydraulic station determines how densely the mix is compacted into the mould cavity. Higher compaction means blocks that reach handling strength faster in the curing yard, which directly affects how quickly pallets cycle back to the press. The 850×550×20 mm pallet size defines both the mould footprint and the curing rack dimensions a buyer must prepare. If the existing forklift and curing area were set up for a different pallet standard, the mismatch creates a bottleneck no amount of press speed can fix. The 2800 r/min vibration frequency is tuned for standard aggregate blends; buyers running unusually fine or coarse local material should confirm the frequency suits their mix before committing.
What Happens When the Line Around the Press Is an Afterthought
Quotations that cover the host machine alone leave buyers discovering pallet, mixer, and stacking costs after the deposit is paid. A press sitting idle while a mismatched mixer catches up on batching is a common scene in plants that sourced equipment piecemeal. The QTJ4-25 ships with the JQ350 mixer as part of the base configuration, sized to keep pace with the 25-second cycle so the press is not starved of material. [NEED_CITE: block line bottleneck analysis for semi-automatic plants] Skipping the line-level view at the inquiry stage is the single most frequent reason buyers report output falling short of the number on the quotation.
Why Buyers Source This Tier from Shiyue
Block machinery is the single production focus, so the press, mould, pallet, and mixer are matched as one system rather than assembled from unrelated suppliers. Configuration is set against the buyer’s actual mix design and target block format, not pulled from a catalogue default. Mould design covers the formats the buyer’s market sells, including custom profiles drawn to buyer specifications. The automation level is selectable, so a plant can start with semi-automatic operation and add automatic stacking as volume grows. Installation support includes operator training and a wear parts list so first replacements do not become an emergency.
Documentation & Verification
- Line layout showing the QTJ4-25 footprint with pallet flow and curing area
- Capacity calculation stating the 400×200×200 mm hollow block basis
- Mould drawing and format list for hollow, solid, paver, and curbstone
- Voltage and control language confirmation signed before production
- Factory test record with cycle time and block density readings
- Hydraulic and electrical schematic for local maintenance teams
Installation, Commissioning & Support
- Foundation pad sized to the 6400×1500 mm footprint with anchor bolt plan
- Dedicated 17.9 kW supply circuit at confirmed voltage and frequency
- Machine arrives as a single host unit with bolt-on vibration motor and hydraulic station
- First-run commissioning includes cycle timing and mould alignment checks
- Operator training covers mould change procedure across all four block formats
- Wear parts list with reorder codes for vibration springs and hydraulic seals
- Pallet inspection and replacement schedule based on the 850×550 mm board standard
What to Prepare Before Sending an Inquiry
Share the specific block formats your market demands, the daily volume you need to sustain, and the aggregate materials available locally. Confirm your site voltage, frequency, and preferred control panel language so electrical specifications are locked before production begins. [NEED_CITE: CE machinery directive requirements for industrial equipment] Include your existing curing area dimensions and forklift capacity so the pallet specification aligns with equipment already on site.
Frequently Asked Questions
Q: How is the 960 pcs/h capacity calculated, and what output should I expect for my block format?
A: That figure is based on a 400×200×200 mm hollow block at four pieces per mould with a 25-second molding cycle. Smaller solid blocks or pavers use different mould layouts and cycle times, so actual hourly output changes. A format-specific capacity calculation is provided with each quotation so buyers can plan against their real product mix.
Q: Where does the QTJ4-25 fit in the full machine range, and when should I step up?
A: This model sits in the entry-to-mid tier for stationary plants, suited to first-time setups or contractor sites. When daily volume consistently exceeds what a single semi-automatic press can sustain and the curing yard can absorb, stepping to a higher tier with automatic stacking becomes justified.
Q: What automation level does this model offer, and can I upgrade later?
A: The QTJ4-25 runs semi-automatic with motor-operated controls. Pallet feeding and block removal are handled manually at this tier. The plant layout can be designed so that automatic pallet feeders and stackers are added later without replacing the host press.
Q: How do I confirm voltage and frequency match my country before the machine ships?
A: Voltage, frequency, and control language are confirmed in writing before production starts. This avoids the situation where a machine arrives on site and the local grid cannot run the hydraulic pump or vibration motor without costly transformer work.
Q: What pallet size does the QTJ4-25 use, and will it fit my curing setup?
A: The machine uses an 850×550×20 mm pallet. Buyers should compare this against their curing rack spacing and forklift fork width before ordering. If the existing yard was built for a different pallet standard, the pallet and rack dimensions need to be reconciled at the layout stage.

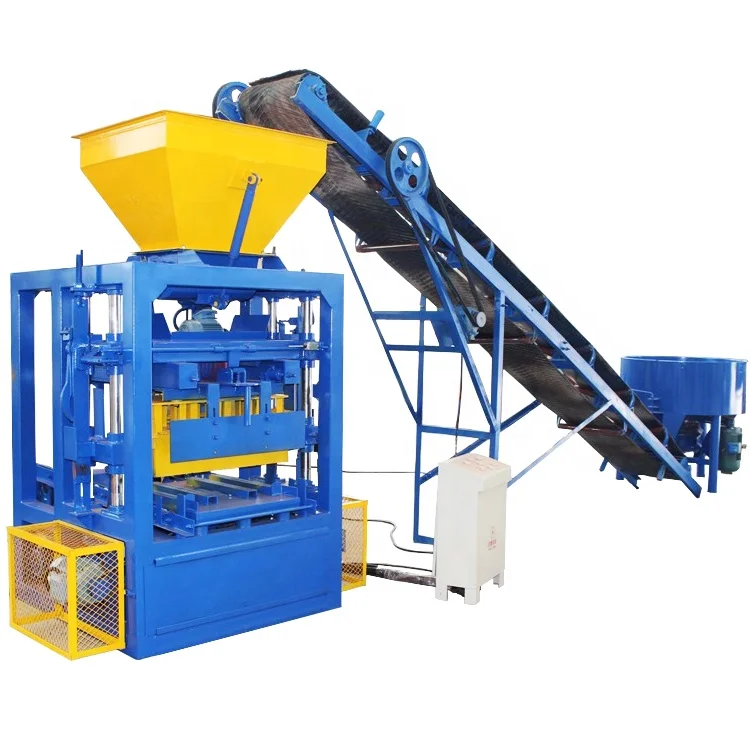 Stationary block machine