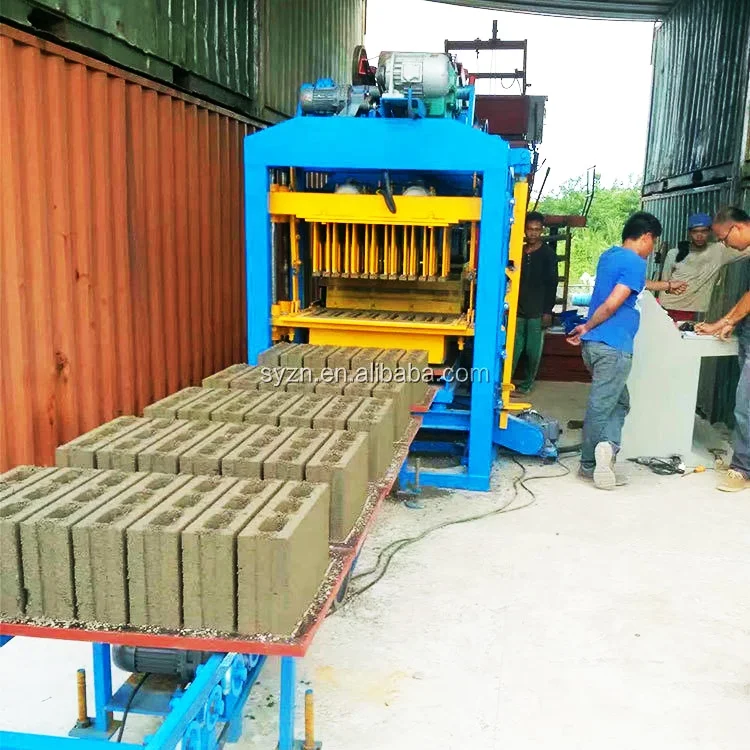
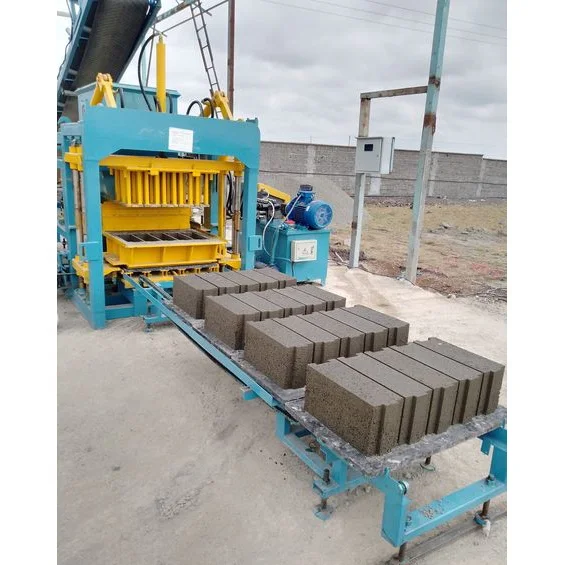
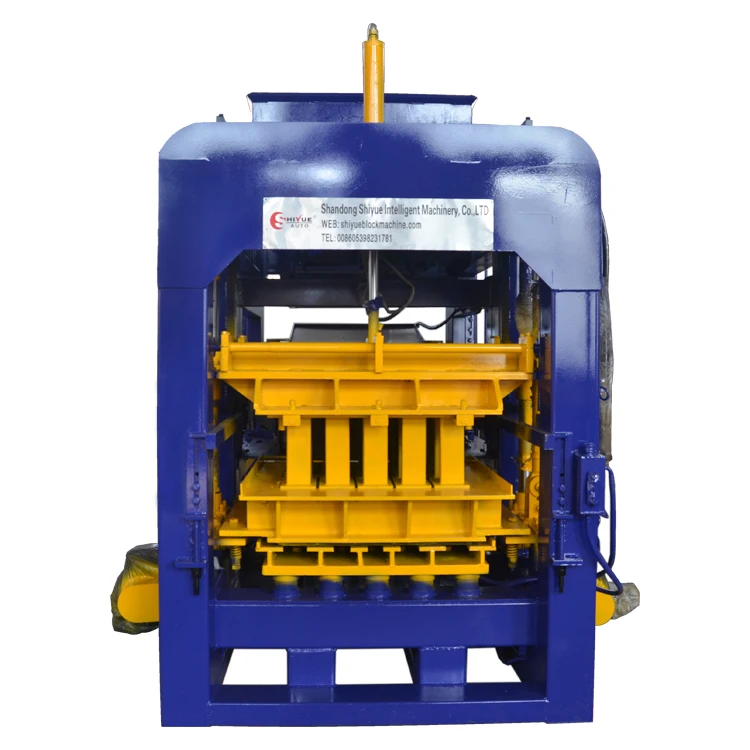
Matched System Design — machine, mould, pallet, and stacker specified together so the QT4-18 runs as one line, not separate components forced to work around each other.
Technical Specifications
| Parameter |
Value |
| Model |
QT4-18 |
| Product Type |
Semi-Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) |
3900×1600×2300 mm |
| Molding Cycle |
15–25 s |
| Vibration Force |
40–50 kN |
| Total Power |
24 kW |
| Mixer Model |
JQ350 |
| Pallet Size |
850×550×25 mm |
| Net Weight |
3 T |
| Hydraulic System |
Hydraulic station (pressure value to be confirmed) |
| Control System |
Available with PLC or MCC control (details to be confirmed) |
| Voltage & Frequency |
Configurable (to be confirmed before production) |
| Automation Level |
Semi-automatic with automatic stacker option |
| Applied Products |
Hollow block, solid brick, paver, curbstone |
Application Suitability
| Application |
Material or Output |
| Hollow block production for building walls |
Crushed stone, sand, cement, fly ash, stone dust |
| Solid brick manufacturing for load-bearing structures |
Sand, cement, stone dust blends |
| Paver production for walkways and yards |
Crushed stone, cement, pigment-added mixes |
| Curbstone forming for road and pavement edges |
Coarse aggregate, cement, high-density mixes |
| On-site contractor block production |
Locally sourced aggregate and cement |
What "1200 Pieces per Hour" Actually Means on a Block Making Machine Manufacturer Data Sheet
Capacity figures are meaningless unless the block format behind each number is stated in writing.
A quotation might show a single hourly output number, but that figure is always calculated on a specific block size, a specific mix, and a specific cycle time. When the machine arrives and the buyer runs a different format, the actual output can fall noticeably short of what was expected. I have seen lines stall because the capacity was quoted on a hollow block cycle while the buyer’s market demanded solid bricks — the cycle time difference alone changed the daily total. The QT4-18 output must be confirmed per format, per mix, before any production target is set. [NEED_CITE: block format cycle time variance in hydraulic press operations]

Where the QT4-18 Sits in the Shiyue Range
The QT4-18 is positioned at the semi-automatic tier, between entry-level mobile machines and fully automatic high-capacity lines. For a first-time plant owner or a contractor producing blocks on a project site, it offers hydraulic pressing and vibration without the investment of a full automatic stacker and cubing system. As production volume grows, the line can accept additional automation stations. A block making machine manufacturer that only sells one tier will push you toward that single option — having the full range visible lets you place yourself honestly.
Output Breakdown by Block Format
Honest capacity starts with naming the format. The QT4-18 is rated at 1200–1680 pieces per hour based on a 400×200×200 mm hollow block, and at 1800–2400 pieces per hour based on a 400×150×200 mm hollow block. For solid brick production at 240×115×53 mm, the rated output is 3240 pieces per hour. These figures assume an 8-hour shift and standard cycle times. If your local aggregate or mix design differs from the test conditions, actual throughput will shift — always request a capacity calculation tied to your specific block format and raw material. [NEED_CITE: aggregate moisture and density effect on block cycle time]
Vibration, Pressure, and Pallet Matching
The vibration force on the QT4-18 is rated at 40–50 kN, working alongside the hydraulic station to compact the mix into the mould cavity. These two forces must be balanced — too much vibration with insufficient hydraulic pressure produces blocks with weak edges, while excessive pressure without enough vibration leaves air pockets inside hollow blocks. The pallet size of 850×550×25 mm is a fixed dimension that must be checked against the buyer’s existing curing racks and forklift capacity before the line is finalized. Mismatched pallets cause bottlenecks at the stacking and curing stage, not at the press itself.
The Cost of Skipping Configuration Details
When voltage, frequency, and PLC display language are not confirmed before production, the machine arrives and sits idle while transformers are sourced or control panels are rewired. Commissioning delays of several weeks are common in these cases, and the buyer absorbs both the hardware cost and the lost production time. Pallet size chosen without checking the curing area means the buyer ends up restacking every pallet by hand — the automatic stacker in the line configuration becomes irrelevant if the pallets cannot move through the curing zone. [NEED_CITE: industrial equipment commissioning delays from voltage mismatch]
Why Source This Machine Here
Every QT4-18 line is specified as a matched system: press, mould, pallet, and handling equipment are selected together, not sourced from separate suppliers and forced to align on site. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default — this avoids the situation where a machine arrives tuned for a material the buyer cannot obtain. Mould design covers the formats the buyer’s market actually sells, with custom mould drawings available when standard formats do not match. Automation level is selectable, so the buyer can begin at semi-automatic and add stacking or cubing modules later without replacing the press. Installation includes on-site commissioning and operator training so the crew understands cycle settings and mould change procedures from day one.
Documentation & Verification
- Line layout and capacity calculation stating the exact block format behind each output figure
- Machine specification sheet with confirmed vibration force, hydraulic pressure, and pallet dimensions
- Mould drawing and format list showing every block type included in the quotation
- Voltage, frequency, and control language confirmation signed before production begins
- Factory test record documenting cycle time and block density on the buyer’s target format
- Packing photographs and customs documentation support for container loading
Installation, Commissioning & Support
- Foundation plan based on the 3900×1600 mm footprint and 3 T operating weight of the QT4-18
- Power supply specification for the 24 kW total load with dedicated circuit requirements
- Machine dismantled for container shipment and reassembled on site with alignment checks
- First-run commissioning with cycle time and vibration force adjusted to the buyer’s mix
- Operator training covering mould change procedure, pallet feeding, and daily maintenance routines
- Wear parts list and mould inventory provided so replacements are available when first needed
What to Include in Your Inquiry
Provide the block formats your market sells, including exact dimensions and target daily output for each. State your local raw materials — aggregate type, available sand gradation, and cement source — so the mix design can be matched to the machine. Confirm your site voltage, frequency, and preferred control language to avoid commissioning delays after arrival.
Frequently Asked Questions
Q: How is output capacity calculated, and which block format does each figure assume?
A: Each output figure on the QT4-18 is tied to a specific block format and cycle time. For example, the hollow block rating of 1200–1680 pieces per hour is based on the 400×200×200 mm format. If your target block is a different size, the cycle time changes and so does the hourly output. Always request a written capacity table that lists every format you plan to produce.
Q: Where does the QT4-18 sit in the range compared to automatic and mobile machines?
A: The QT4-18 occupies the semi-automatic tier, suited for first-time plants and on-site contractor production. It offers hydraulic pressing with vibration but requires more manual handling than a fully automatic line. Buyers who expect to scale volume can add automatic stacking and cubing modules later without replacing the host press.
Q: What voltage and frequency does the machine support, and is the PLC language configurable?
A: Voltage and frequency are configurable to match the buyer’s local supply, and the control language is set before production. These details must be confirmed in writing during the inquiry stage — arriving at the site with an incorrect voltage or unreadable PLC display delays commissioning by weeks.
Q: How long does a mould change take, and is a quick-change system available?
A: Mould change is performed by replacing the mould on the host machine. The exact time depends on the format and operator experience. A quick-change system may be available depending on the configuration selected. Buyers who plan to run multiple formats daily should discuss the mould change procedure during the specification stage.
Q: What supporting equipment is included versus optional in the quotation?
A: The QT4-18 line can include the JQ350 mixer, pallet feeding system, and automatic stacker as part of the configuration. However, the exact scope depends on the automation level chosen. Buyers should verify that the quotation lists every station from raw material feeding through to stacking, so no handling step is left to manual labor unexpectedly.

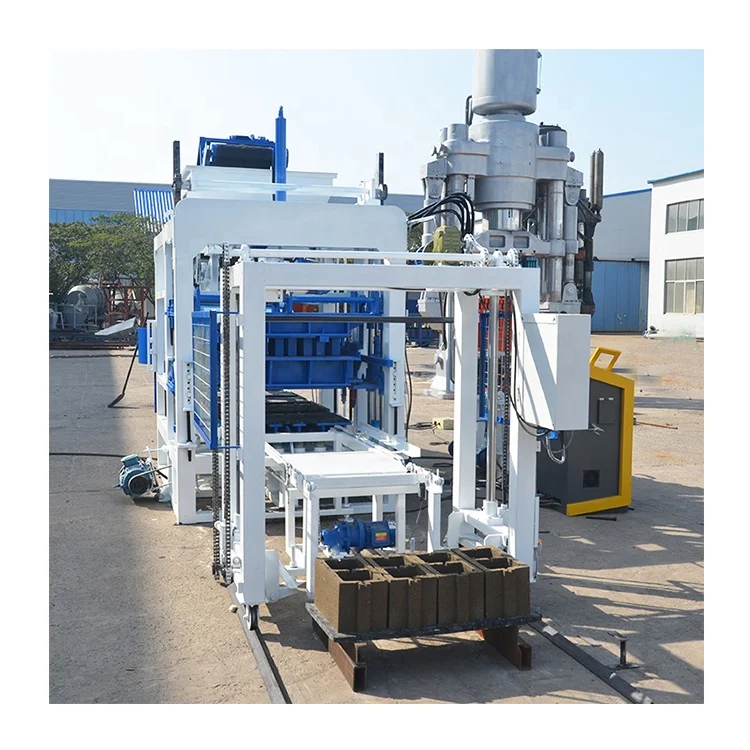
 High quality block machine